IN
₹
Apparel & Fashion
Description
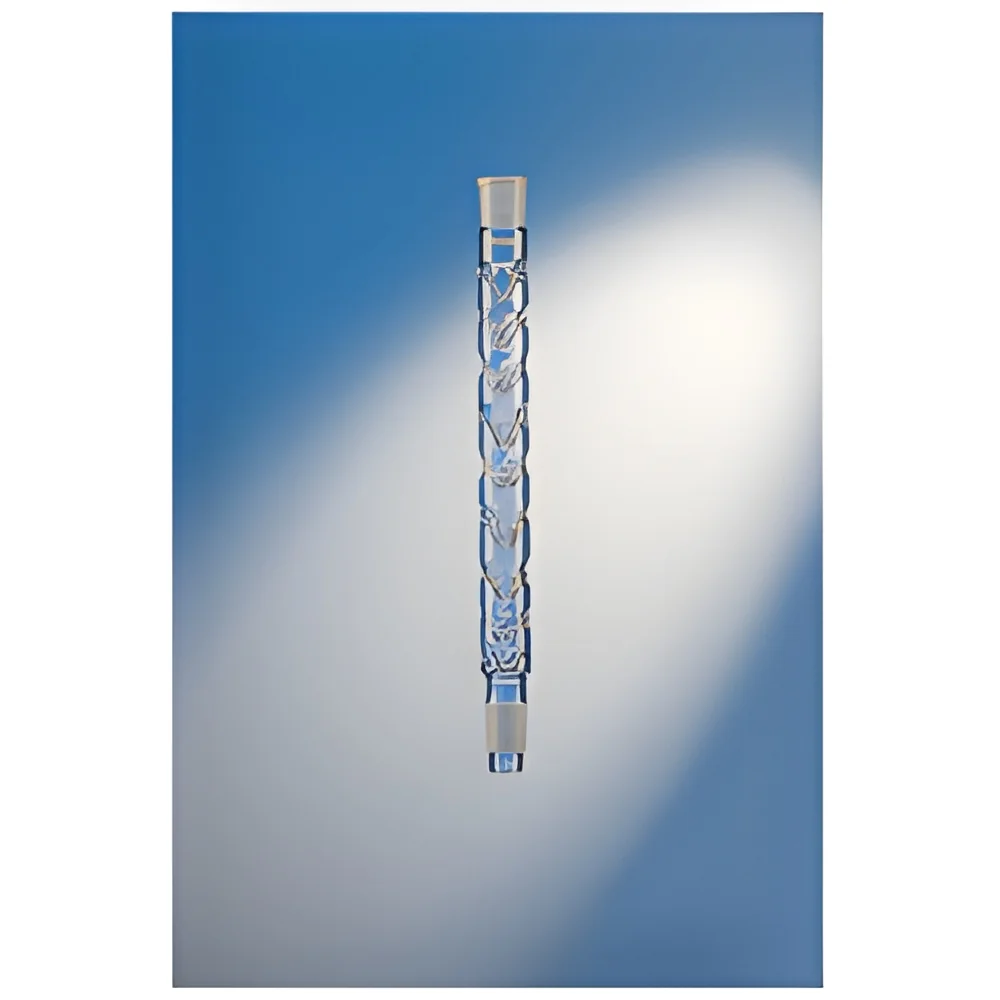
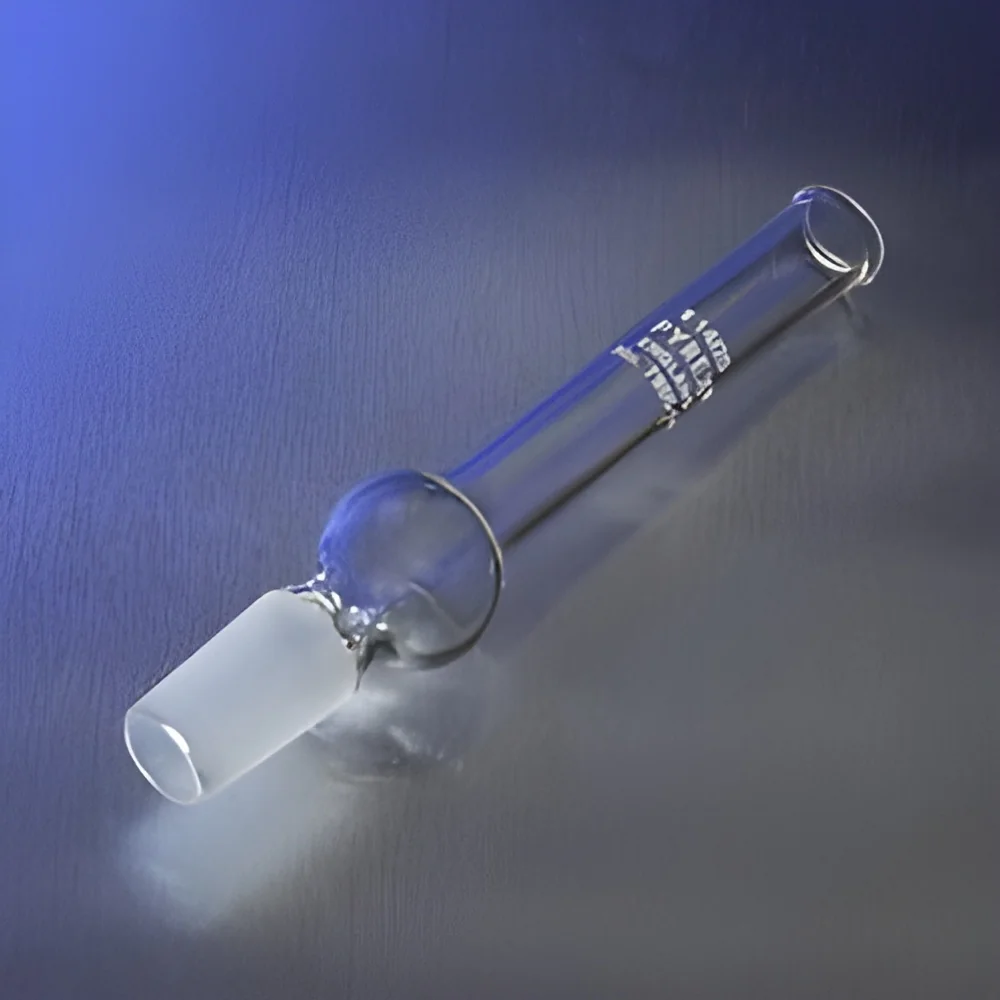
Our premium drying tubes deliver exceptional moisture control solutions for professional laboratory and industrial environments. Engineered with high-quality materials and advanced absorption technology, these tubes provide reliable performance in removing water vapor from gas streams and protected spaces. Each unit undergoes comprehensive quality testing to ensure consistent moisture absorption rates and dependable operation across various conditions. The standardized design allows for straightforward integration into existing systems while meeting specific operational requirements across different applications and industry settings.

These drying tubes serve vital functions across multiple sectors where moisture management is essential. In laboratory environments, they protect sensitive analytical instruments and ensure experimental accuracy by maintaining dry conditions. Pharmaceutical manufacturers rely on them for controlling humidity during drug production and packaging operation...
Our premium drying tubes deliver exceptional moisture control solutions for professional laboratory and industrial environments. Engineered with high-quality materials and advanced absorption technology, these tubes provide reliable performance in removing water vapor from gas streams and protected spaces. Each unit undergoes comprehensive quality testing to ensure consistent moisture absorption rates and dependable operation across various conditions. The standardized design allows for straightforward integration into existing systems while meeting specific operational requirements across different applications and industry settings.

These drying tubes serve vital functions across multiple sectors where moisture management is essential. In laboratory environments, they protect sensitive analytical instruments and ensure experimental accuracy by maintaining dry conditions. Pharmaceutical manufacturers rely on them for controlling humidity during drug production and packaging operations. Chemical processing facilities utilize them to prevent moisture-induced reactions, while electronics producers depend on them for creating moisture-free manufacturing environments. Healthcare institutions implement these tubes in sterilization units and storage areas to maintain sterile, dry conditions for medical equipment and supplies.

The operational value of our drying tubes lies in their proven reliability and cost efficiency. By effectively preventing moisture contamination, they significantly reduce equipment maintenance expenses and minimize product spoilage risks. Their durable construction ensures extended service life with consistent performance, delivering excellent long-term value. The standardized connections facilitate straightforward implementation, while the robust design provides dependable operation in critical applications where moisture control directly impacts process success and final product quality. These tubes offer operational confidence through demonstrated performance in applications where humidity management is crucial.

Key Features:
- High-quality materials ensure durability and extended service life
- Advanced absorption technology provides superior moisture control
- Comprehensive quality testing guarantees consistent performance
- Standardized design for straightforward system integration
- Robust construction for reliable operation in demanding environments

Benefits:
- Prevents moisture contamination and product degradation
- Reduces equipment maintenance costs and downtime
- Ensures consistent performance across various applications
- Easy integration into existing systems and processes
- Provides reliable protection for sensitive instruments and materials
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Drying tubes provide essential moisture control in laboratory environments where precise humidity management is critical. They effectively remove water vapor from gas streams during experiments and analytical processes, ensuring accurate results and protecting sensitive instrumentation from moisture damage. These tubes maintain optimal dry conditions in research facilities, quality control labs, and testing centers where moisture-sensitive materials require reliable protection against humidity.
In industrial and medical settings, drying tubes prevent moisture-related contamination and product degradation. They are widely implemented in pharmaceutical manufacturing, chemical processing, electronics production, and medical device sterilization. Their robust construction and consistent performance make them suitable for continuous operation in demanding environments where maintaining dry conditions is essential for process integrity and final product quality assurance.
- Laboratory gas purification systems for research and analytical processes
- Pharmaceutical manufacturing and packaging moisture protection
- Chemical processing plants requiring dry air and gas streams
- Electronics manufacturing cleanroom environmental control
- Medical equipment sterilization and storage facility protection
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhishek Scientific Company, Maharashtra
 Maharashtra, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Drying Tubes For Laboratory And Industrial Moisture Control
Premium drying tubes for precise moisture control in laboratory and industrial applications. High-quality, reliable performance for sensitive environments. Trusted globally for consistent results and durability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhishek Scientific Company
 Maharashtra, India
Electronics & ElectricalManufacturer