IN
₹
Apparel & Fashion

Description
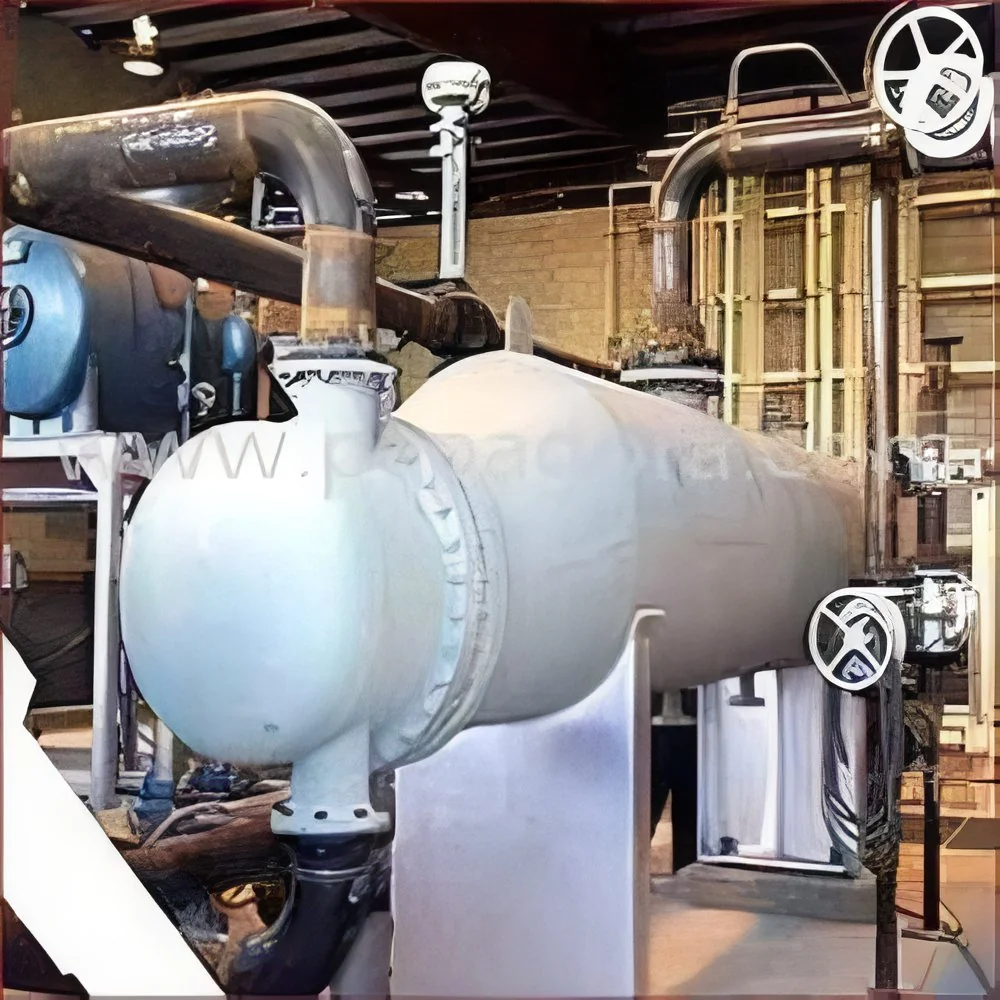
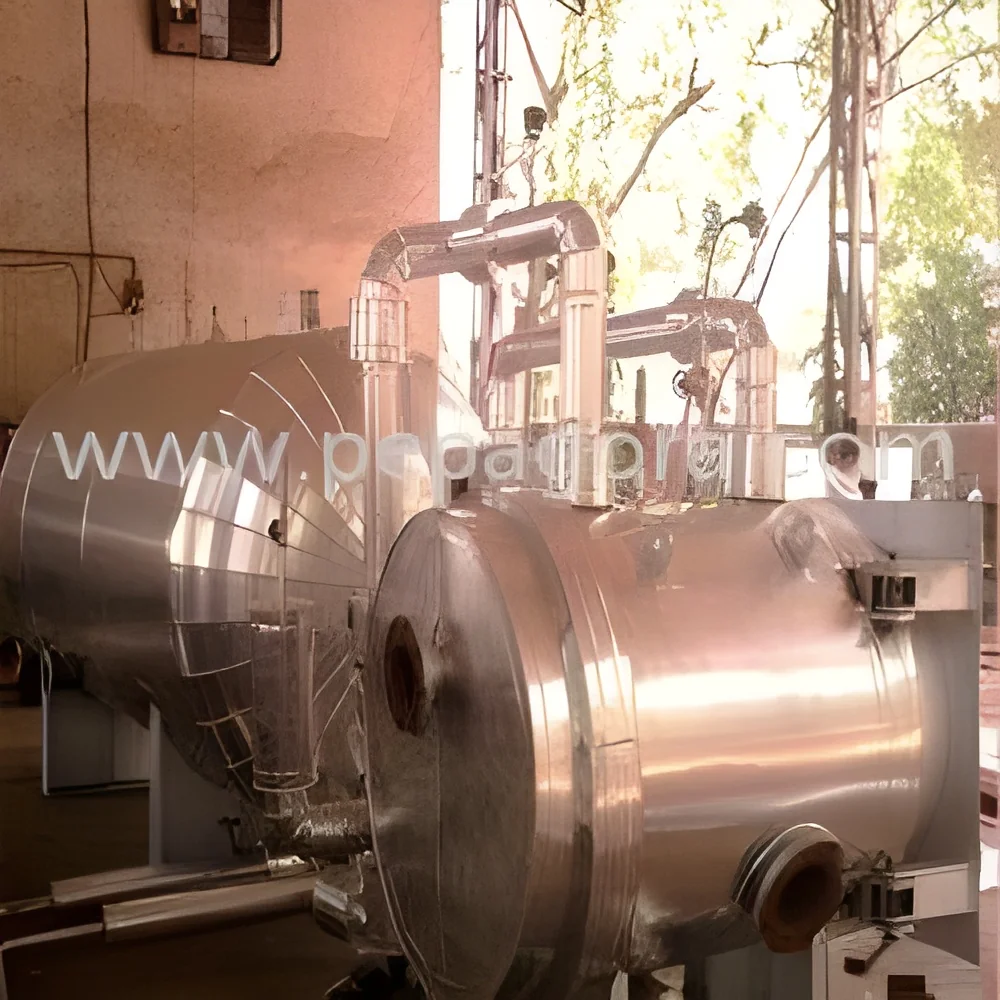
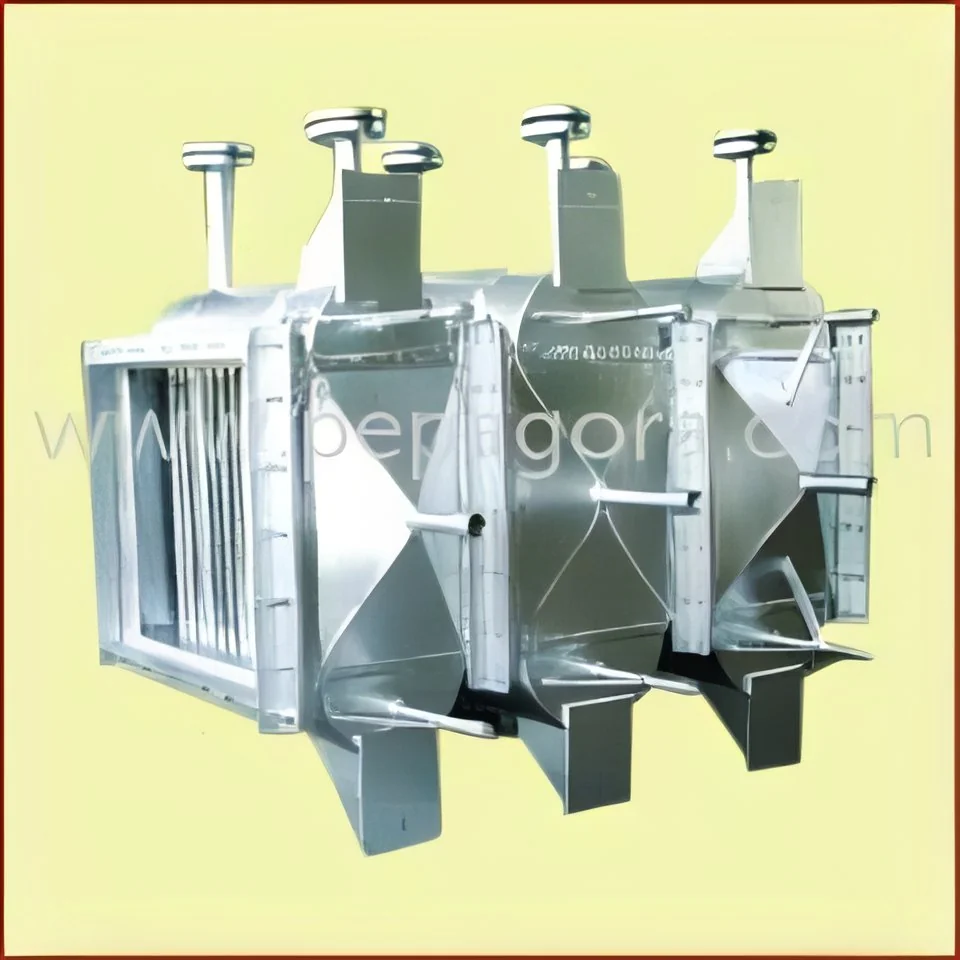
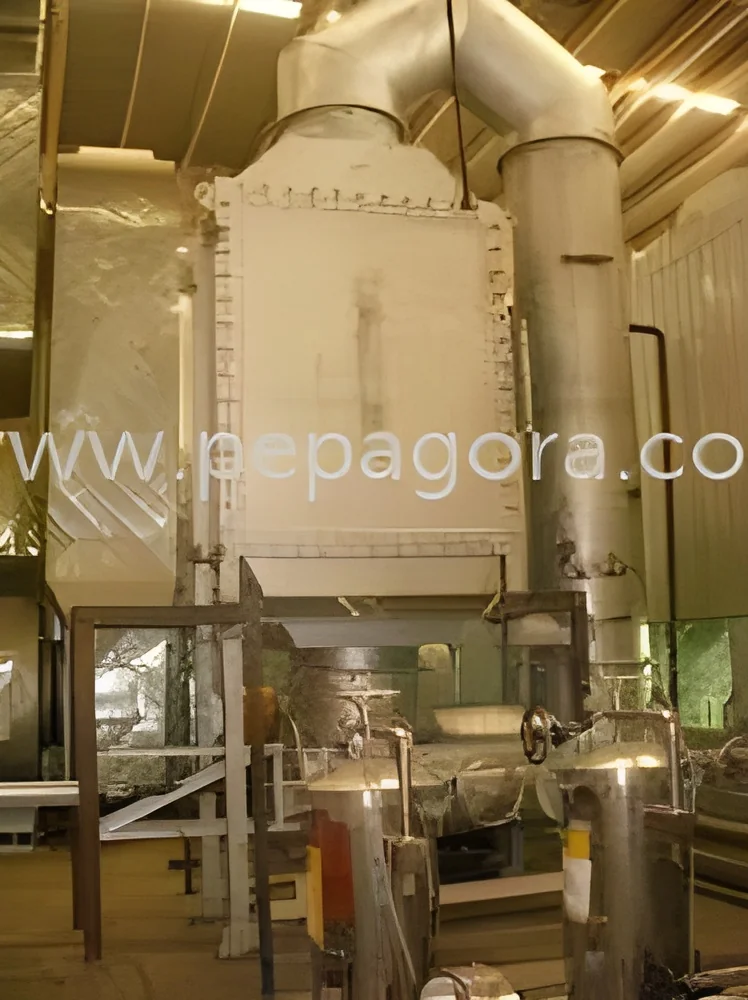
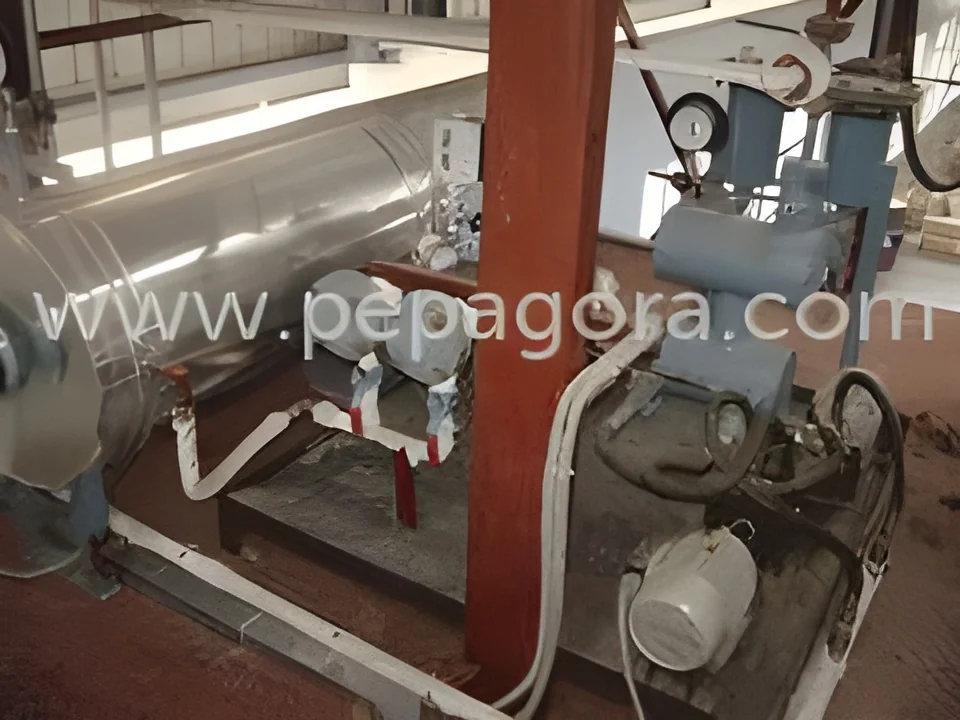
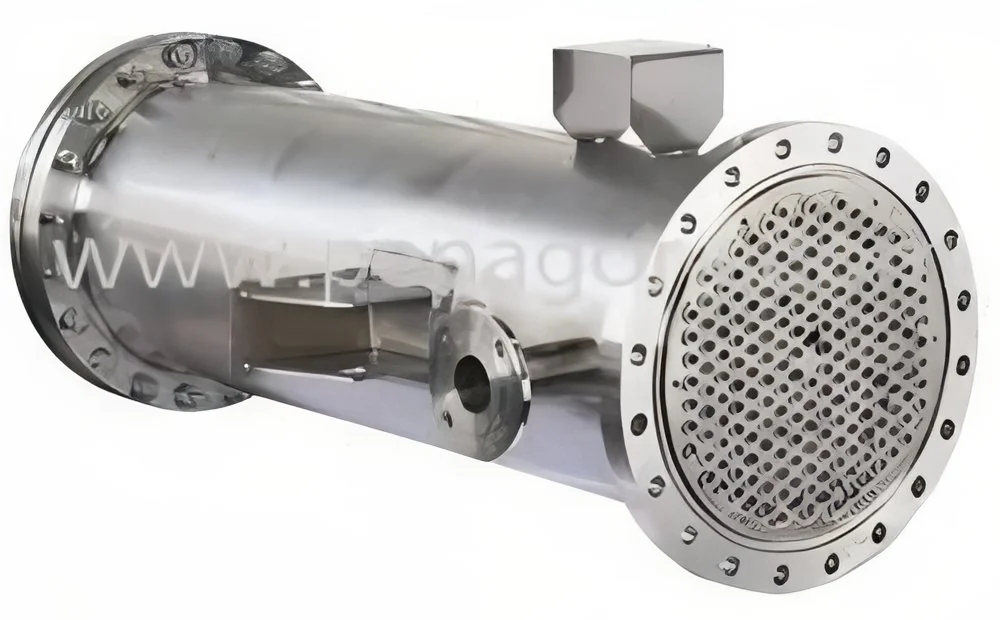
The Industrial HVAC Condensate Air Heating and Cooling Unit represents advanced climate control technology engineered specifically for demanding industrial applications. This integrated system combines both heating and cooling functions within a single robust unit, featuring precision temperature control through industrial-grade thermostats and energy-efficient operation that significantly reduces power consumption. Designed for continuous operation in challenging environments, the unit maintains consistent performance while minimizing maintenance requirements and operational costs. Its durable construction withstands harsh industrial conditions, providing reliable climate management where temperature stability is critical to operational success.

This heating and cooling solution serves essential functions across multiple industrial sectors. Manufacturing facilities utilize it to maintain optimal temperatures for production processes and equipment operation, ensuring consistent produc...
The Industrial HVAC Condensate Air Heating and Cooling Unit represents advanced climate control technology engineered specifically for demanding industrial applications. This integrated system combines both heating and cooling functions within a single robust unit, featuring precision temperature control through industrial-grade thermostats and energy-efficient operation that significantly reduces power consumption. Designed for continuous operation in challenging environments, the unit maintains consistent performance while minimizing maintenance requirements and operational costs. Its durable construction withstands harsh industrial conditions, providing reliable climate management where temperature stability is critical to operational success.

This heating and cooling solution serves essential functions across multiple industrial sectors. Manufacturing facilities utilize it to maintain optimal temperatures for production processes and equipment operation, ensuring consistent product quality and machinery performance. Pharmaceutical production environments rely on its precise climate control for clean room compliance and sensitive manufacturing processes. Food processing plants depend on its accurate temperature regulation for food safety and preservation, while data centers utilize its reliable temperature management for critical server protection and uptime. The system seamlessly integrates with existing HVAC infrastructure in warehouses, commercial complexes, and industrial plants requiring year-round temperature stability for various operational needs.

The business value of this condensate unit lies in its exceptional reliability, operational efficiency, and long-term cost-effectiveness. Engineered for continuous operation with minimal maintenance requirements, it reduces system downtime and operational expenses while delivering consistent performance. The robust construction ensures durability in harsh industrial environments, providing years of trouble-free service with reliable climate control. Its energy-efficient design translates to significant power savings over conventional systems, while the precise temperature control enhances process efficiency and product quality. This unit represents a strategic investment in climate control infrastructure that delivers measurable returns through reduced energy costs, improved operational reliability, and enhanced environmental management capabilities.

Key Features:
- Precision temperature control with industrial-grade thermostat for accurate climate management
- Dual heating and cooling operation in a single integrated unit for space efficiency
- Energy-efficient design that reduces power consumption and operational costs
- Robust construction built for continuous operation in demanding industrial environments
- Seamless integration capability with existing HVAC systems and infrastructure

Benefits:
- Maintains precise temperature control for sensitive industrial processes and equipment
- Reduces energy consumption and operational costs through efficient dual-function design
- Provides reliable continuous operation with minimal maintenance requirements
- Ensures durable performance in challenging industrial environments
- Offers flexible integration with various facility types and existing systems
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial-grade condensate air heating and cooling unit provides precise climate control for facilities where temperature stability directly impacts operations. It maintains consistent environmental conditions for both sensitive processes and personnel comfort, ensuring optimal performance in diverse industrial settings. The system's robust design handles continuous operation with minimal maintenance, making it ideal for demanding applications where reliability cannot be compromised.
Multiple industries benefit from this integrated heating and cooling solution, including manufacturing plants, pharmaceutical facilities, food processing operations, data centers, and large storage warehouses. The dual-function capability eliminates the need for separate systems while providing year-round climate control. Its precise temperature regulation protects equipment, preserves materials, and maintains ideal working conditions across various operational requirements.
- Manufacturing facilities requiring stable temperatures for production processes
- Pharmaceutical clean rooms needing precise climate control
- Food processing and storage areas for perishable goods preservation
- Data centers maintaining optimal server operating temperatures
- Large warehouses protecting temperature-sensitive inventory
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Nimotherm Engineering Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial HVAC Condensate Air Heating And Cooling Unit With Precise Temperature Control
Industrial HVAC Condensate Air Heating and Cooling Unit delivers precise temperature control for demanding industrial environments. This energy-efficient system provides reliable climate management with durable construction for continuous operation.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Nimotherm Engineering Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer