IN
₹

Description
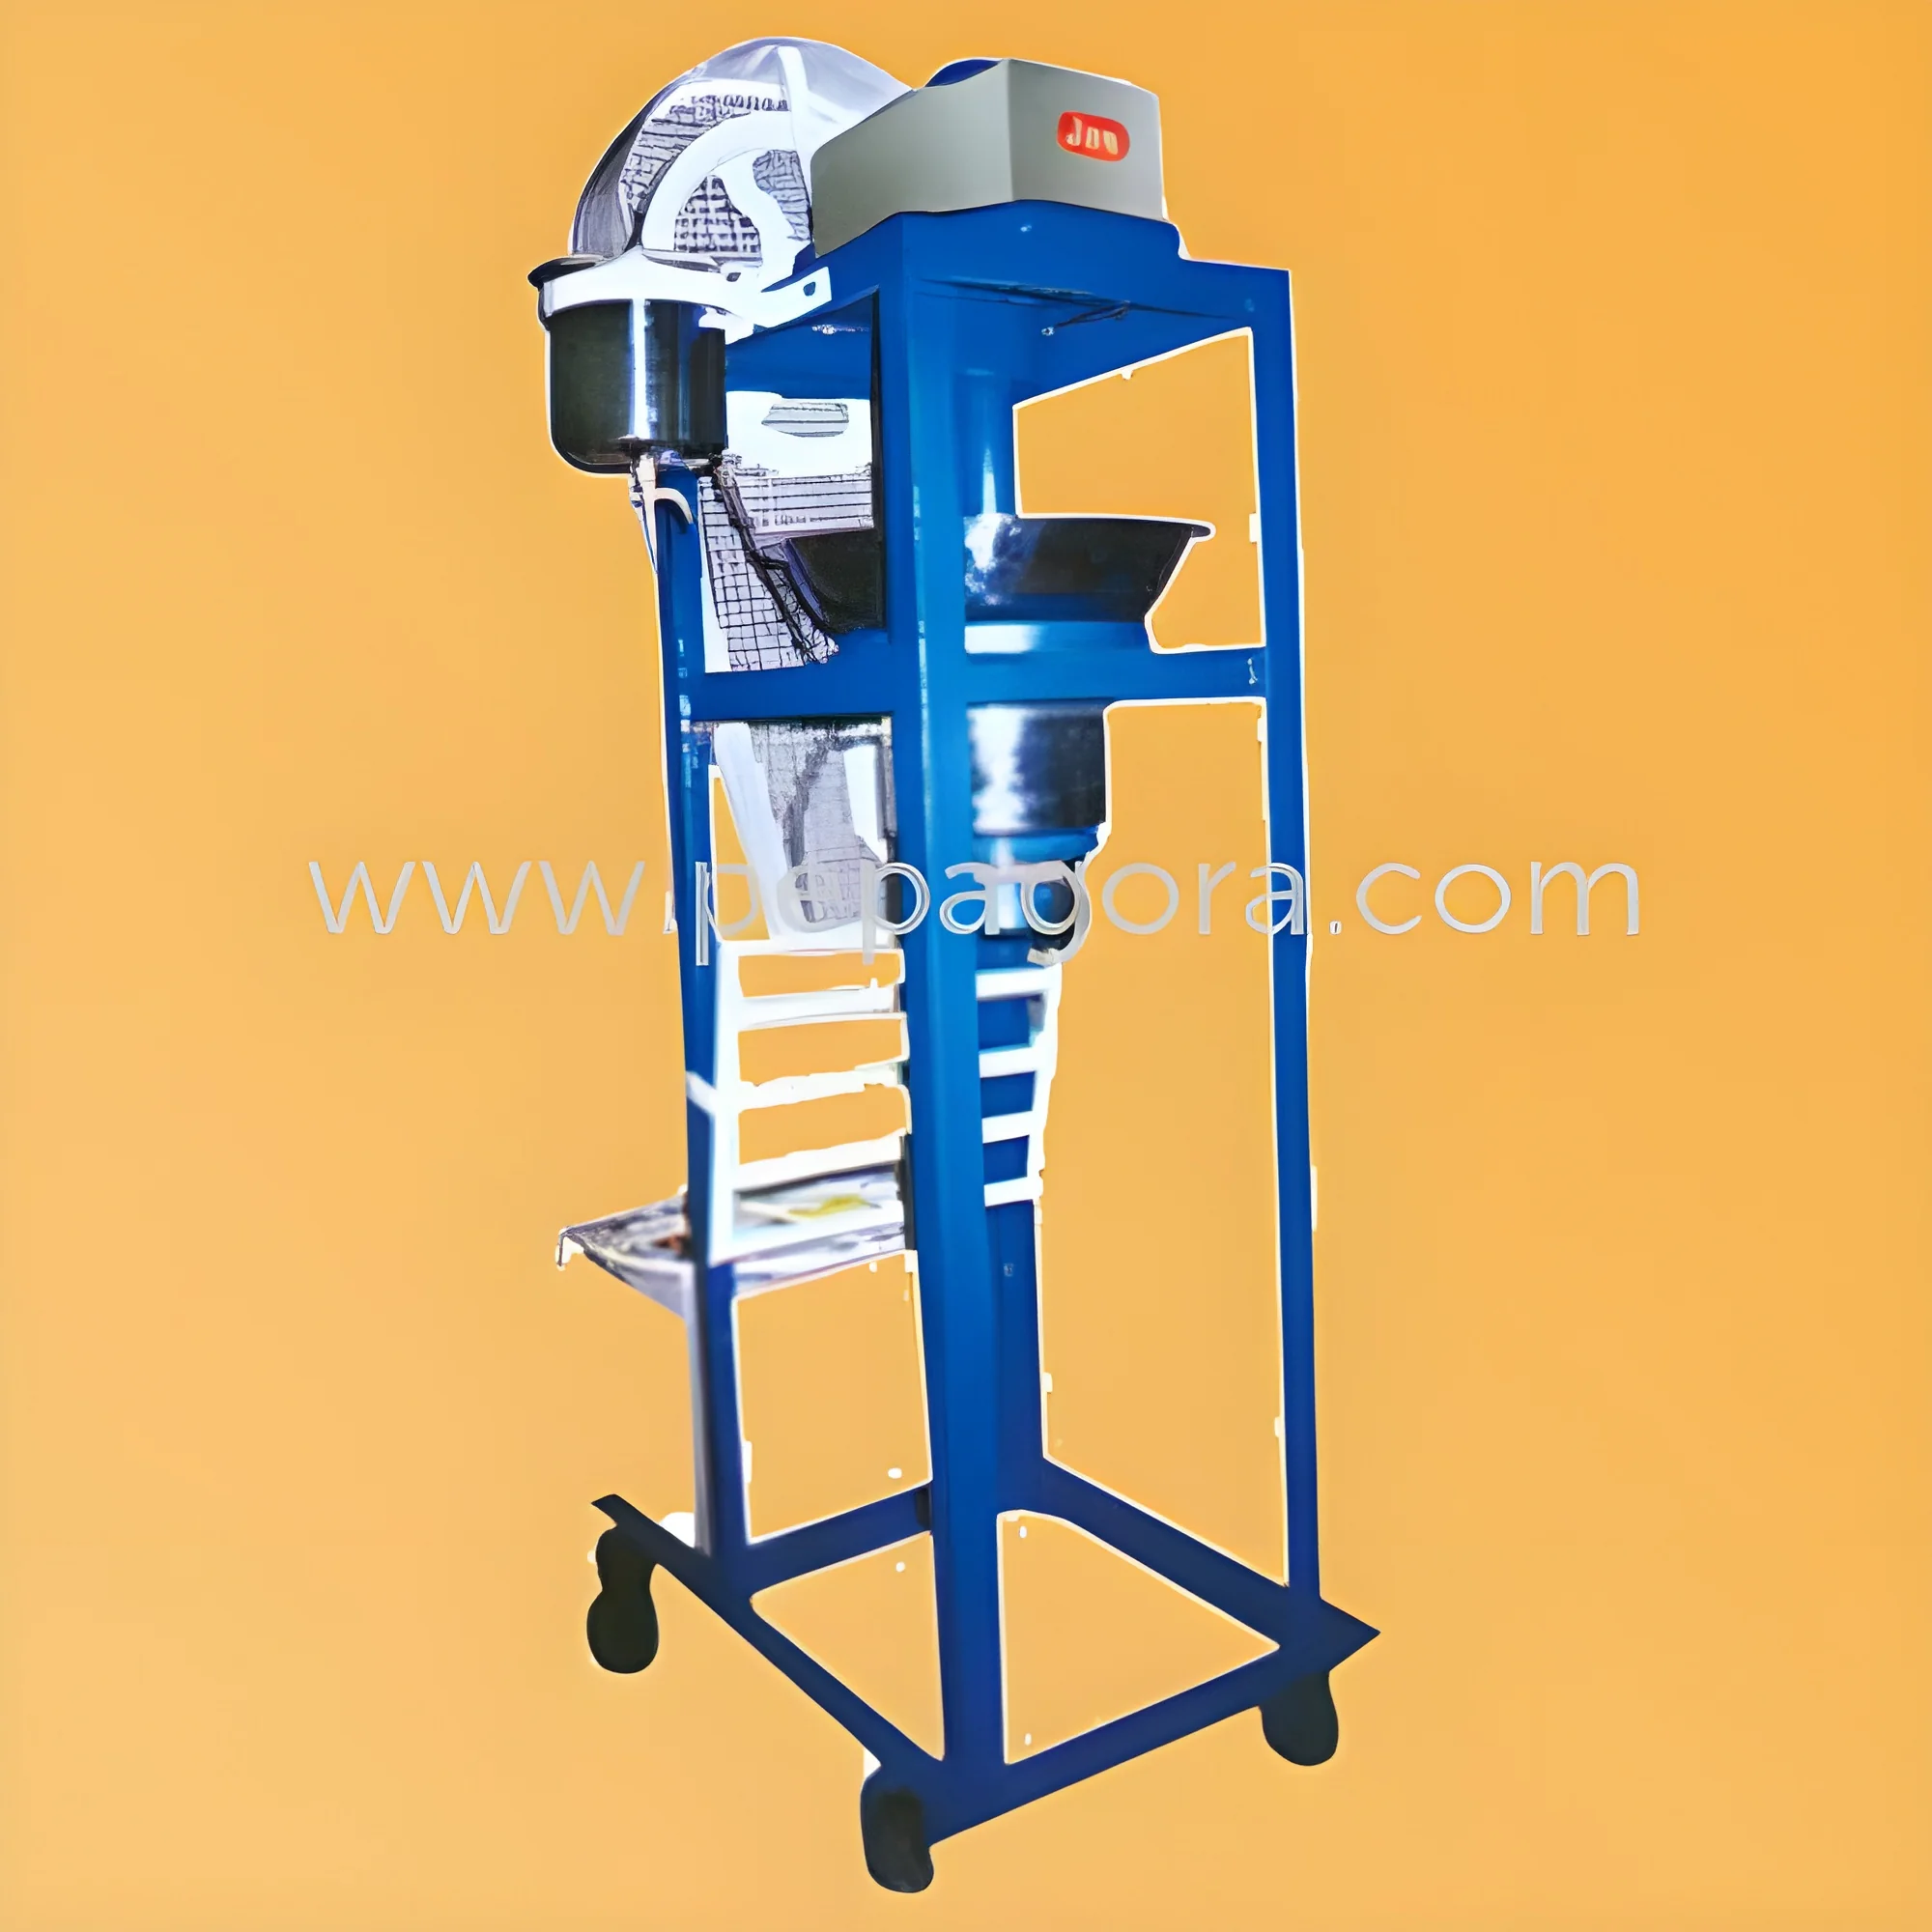
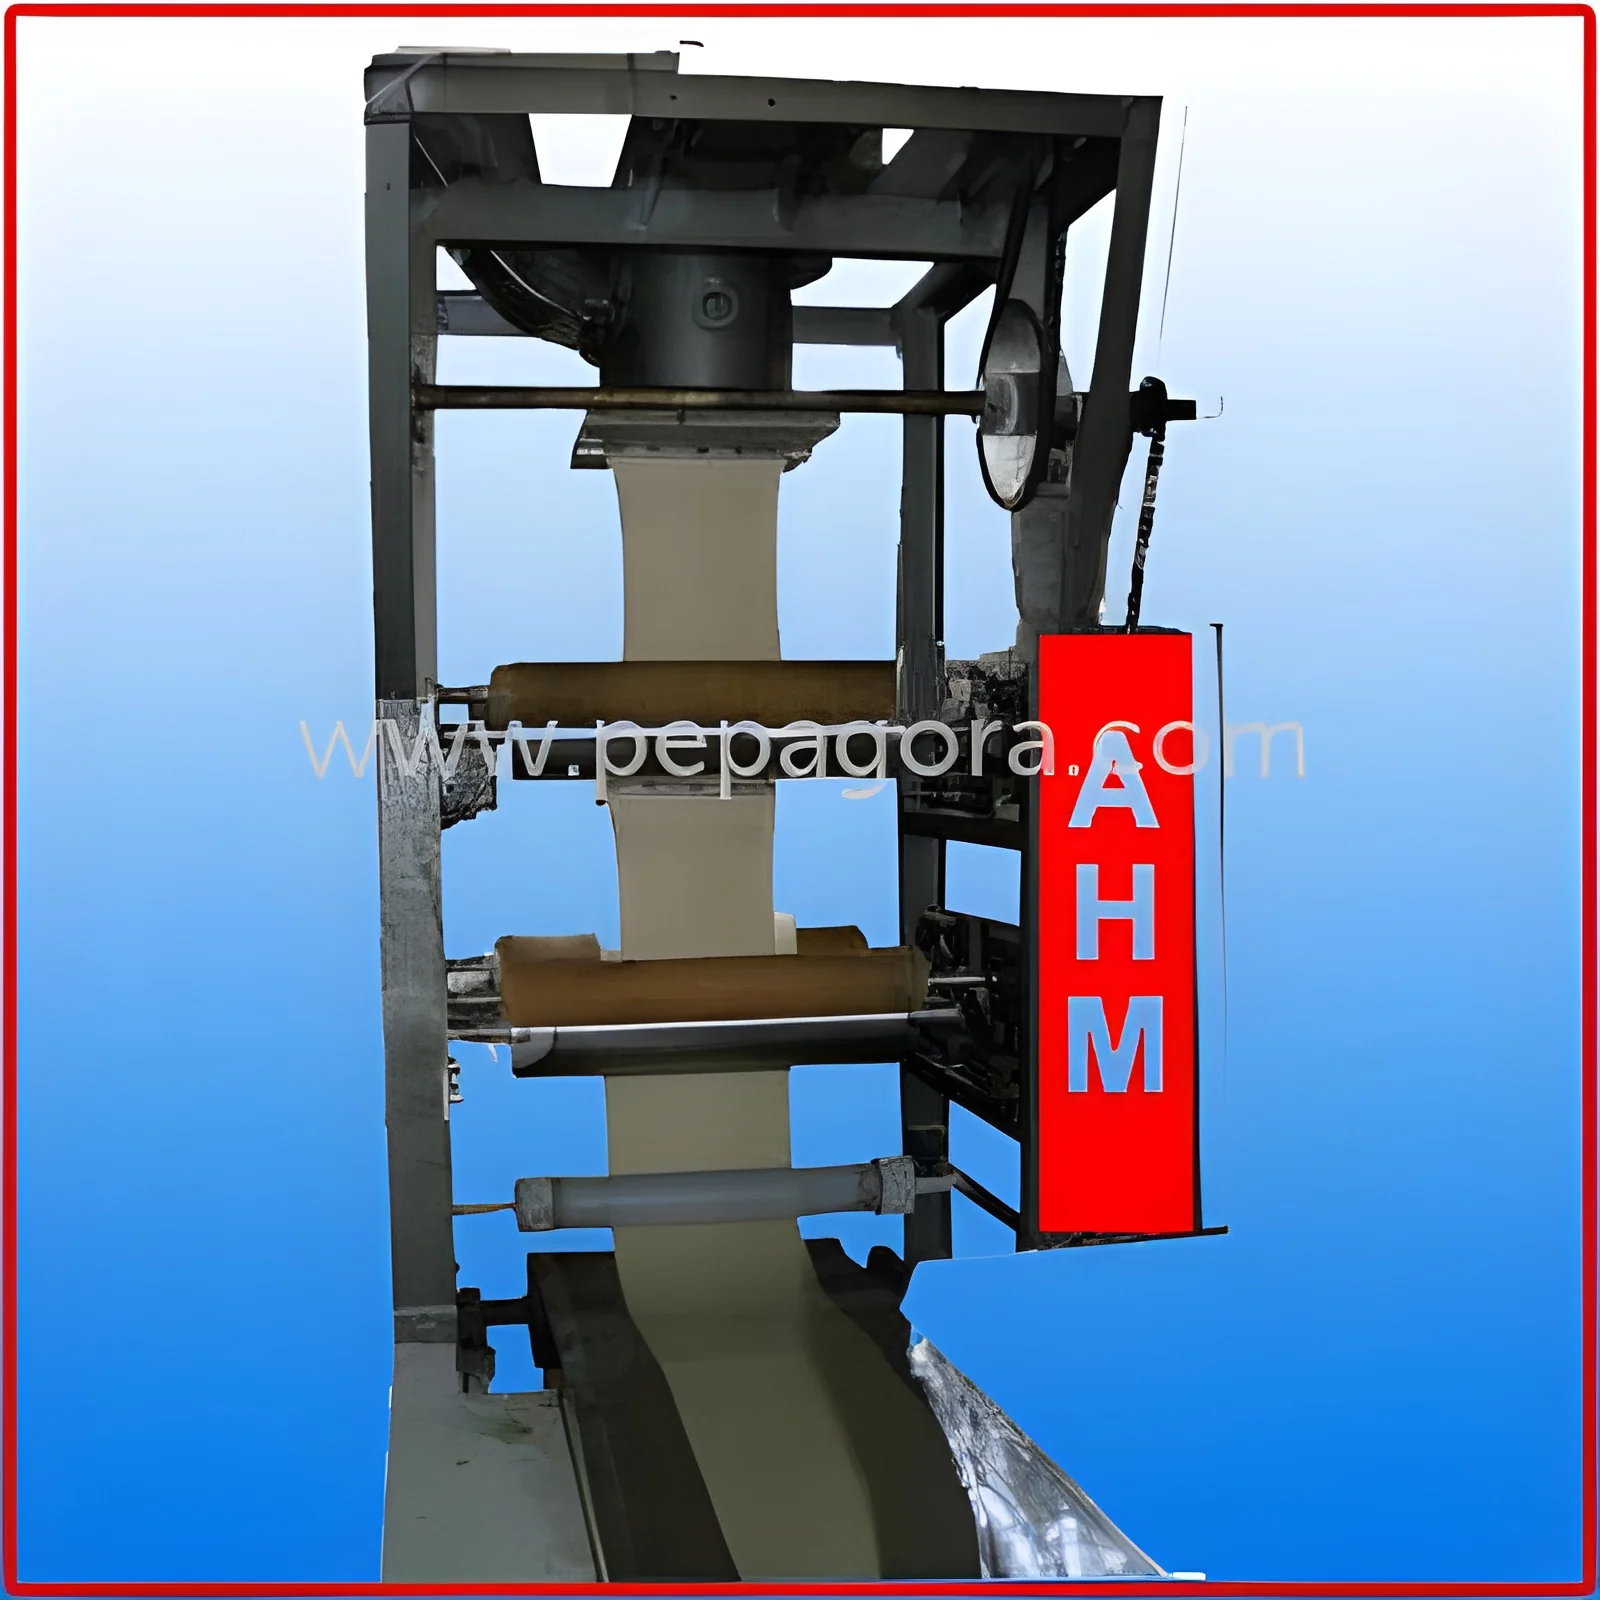
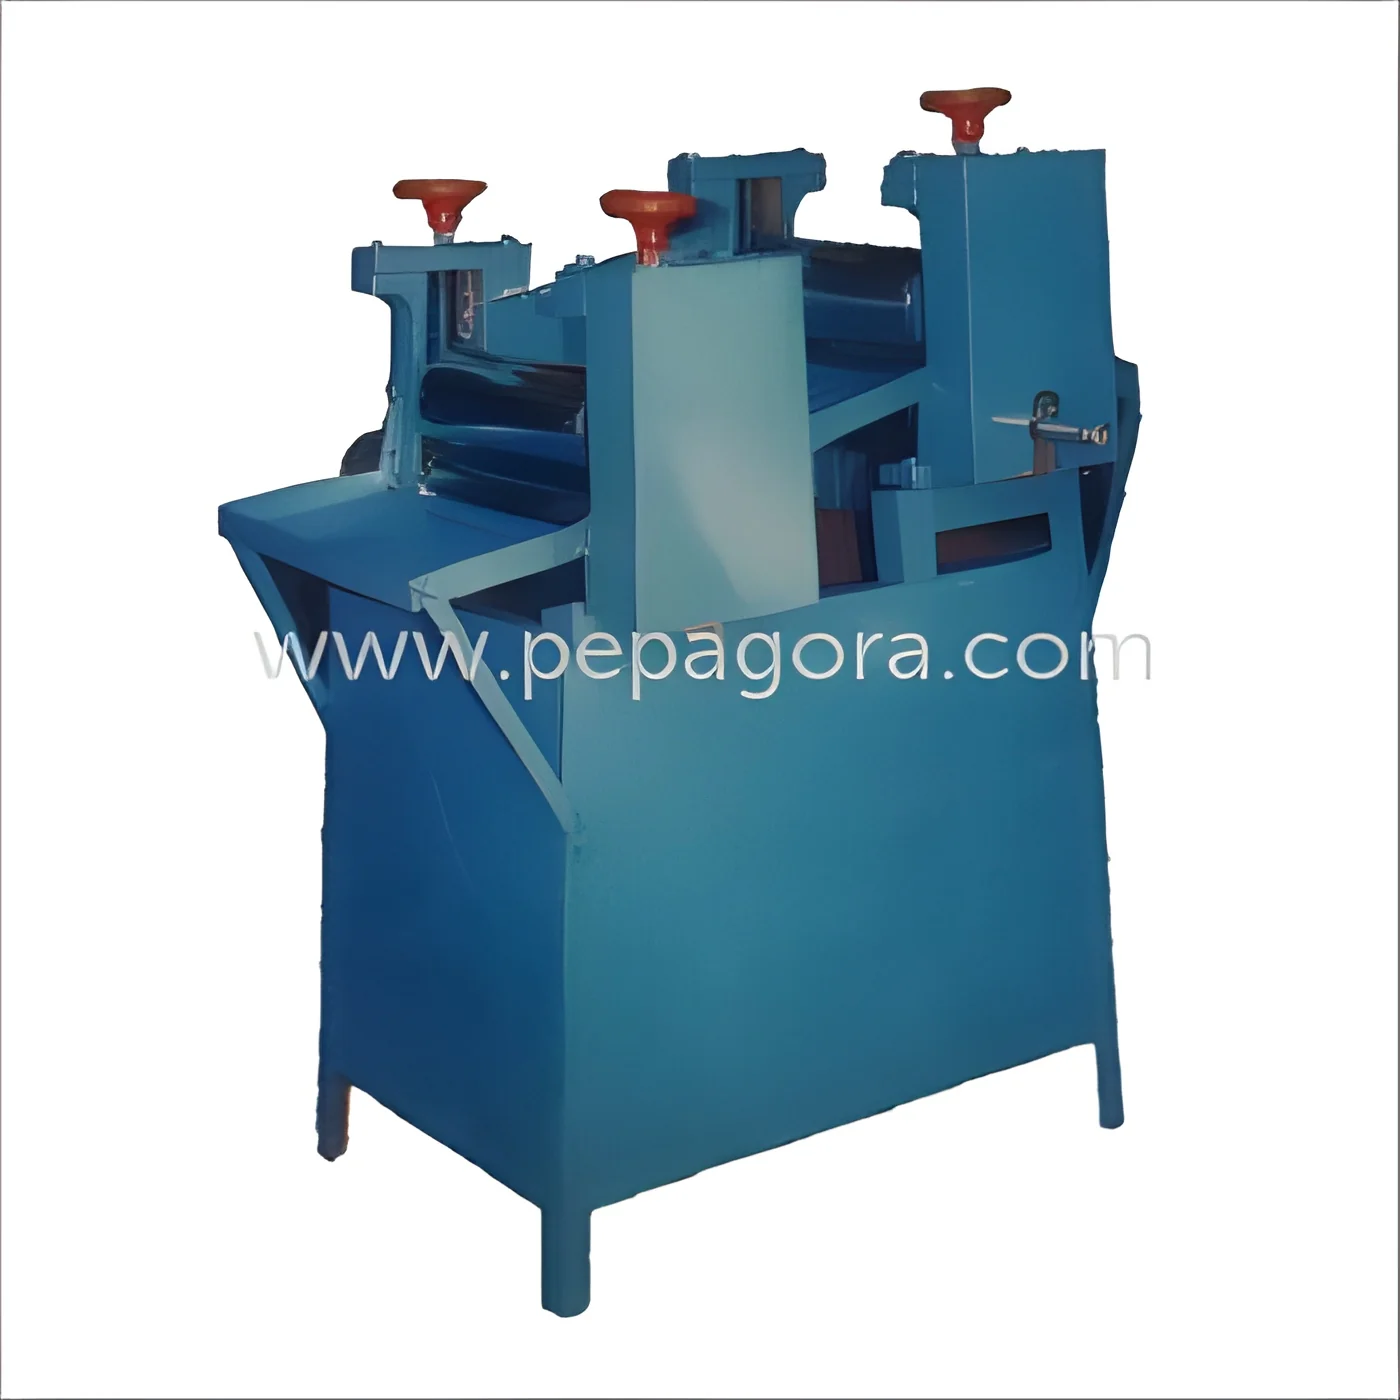
Our industrial belt conveyors represent heavy-duty material handling solutions designed for performance and reliability in demanding operational environments. Constructed with high-quality stainless steel, these systems provide exceptional resistance to corrosion, wear, and various environmental factors encountered in industrial settings. The fire-resistant belt material significantly enhances operational safety by reducing risks in environments where heat, sparks, or combustion hazards may be present. These conveyors are engineered to handle diverse load capacities and are built to withstand continuous operation in challenging industrial conditions, ensuring long-term performance and minimal maintenance requirements.

These belt conveyors find extensive application across multiple industries including manufacturing plants, warehousing and distribution centers, recycling facilities, logistics operations, and industrial packaging centers. In manufacturing environments, they facilitate s...
Our industrial belt conveyors represent heavy-duty material handling solutions designed for performance and reliability in demanding operational environments. Constructed with high-quality stainless steel, these systems provide exceptional resistance to corrosion, wear, and various environmental factors encountered in industrial settings. The fire-resistant belt material significantly enhances operational safety by reducing risks in environments where heat, sparks, or combustion hazards may be present. These conveyors are engineered to handle diverse load capacities and are built to withstand continuous operation in challenging industrial conditions, ensuring long-term performance and minimal maintenance requirements.

These belt conveyors find extensive application across multiple industries including manufacturing plants, warehousing and distribution centers, recycling facilities, logistics operations, and industrial packaging centers. In manufacturing environments, they facilitate seamless movement of raw materials and components between production stages and assembly lines. Warehouses utilize them for efficient sorting and transportation of packaged goods and cartons, while recycling facilities rely on their durability to handle abrasive materials and waste products. Logistics companies implement these systems for parcel sorting and distribution operations, and industrial facilities use them for product transfer between different processing stages. The versatility and robust construction make them suitable for both light and heavy-duty applications across these industrial sectors.

The business value of these conveyors lies in their ability to automate material handling processes, thereby reducing labor costs and increasing operational efficiency throughout industrial operations. Their reliable performance ensures consistent material flow with minimal downtime, while the low maintenance design translates to reduced operational expenses over the long term. The fire-resistant properties contribute to safer working environments, potentially lowering insurance costs and compliance risks associated with industrial safety regulations. The stainless steel construction ensures longevity and resistance to industrial wear and tear, providing excellent return on investment through extended service life and reduced replacement costs. The equipment's design focuses on operational efficiency and reliability, ensuring businesses can maintain consistent production flows and meet their material handling requirements effectively.

Key Features:
- Stainless steel construction for superior corrosion resistance
- Fire-resistant conveyor belt material for enhanced safety
- Heavy-duty frame design supporting high load capacities
- Simple control systems for easy operation and integration
- Durable components designed for continuous industrial use

Benefits:
- Enhanced operational safety with fire-resistant materials
- Reduced maintenance costs through durable construction
- Improved efficiency in material handling processes
- Long service life with corrosion-resistant materials
- Reliable performance in demanding industrial environments
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Fire Resistant |
| Structure | Belt Conveyor |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These commercial non-food grade belt conveyors are engineered for heavy-duty material transport in demanding industrial environments. The robust systems efficiently handle bulk items, packaged goods, and industrial components with consistent reliability and minimal operational downtime. Their sturdy stainless steel construction and fire-resistant properties ensure safe operations where durability and safety are essential requirements for continuous material flow.
These conveyors serve critical functions across manufacturing, warehousing, recycling, and logistics sectors by automating material movement and reducing manual handling. They streamline operations by transporting goods efficiently between processes, sorting stations, and storage areas while accommodating various load capacities and operational demands. The reliable performance ensures consistent material flow with minimal maintenance requirements, making them ideal for continuous industrial operations.
- Moving packaged goods and cartons in warehouse distribution centers
- Transporting raw materials and components in manufacturing plants
- Handling recyclable materials and waste in management facilities
- Sorting parcels and packages in logistics and shipping hubs
- Assembling and transferring products in industrial production lines
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Madurai |
Company Profile

ADHITHYA HITECH MACHINES, Tamil Nadu
 Tamil Nadu, India
Food & Agriculture•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Belt Conveyor Stainless Steel Fire Resistant Material Handling
Industrial belt conveyor with stainless steel construction and fire-resistant belts for safe material handling in warehouses, manufacturing, and logistics operations. Durable commercial non-food grade equipment.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ADHITHYA HITECH MACHINES
 Tamil Nadu, India
Food & AgricultureManufacturer