IN
₹
Apparel & Fashion

Description
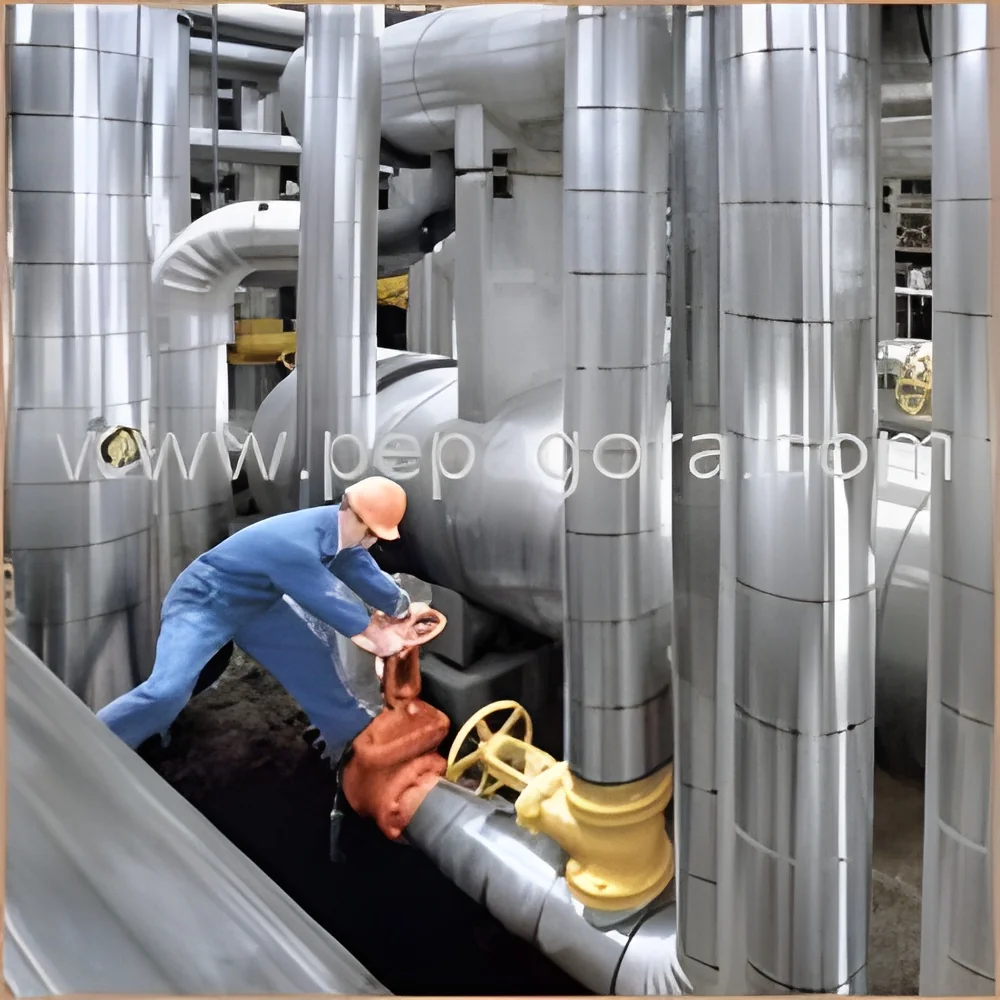
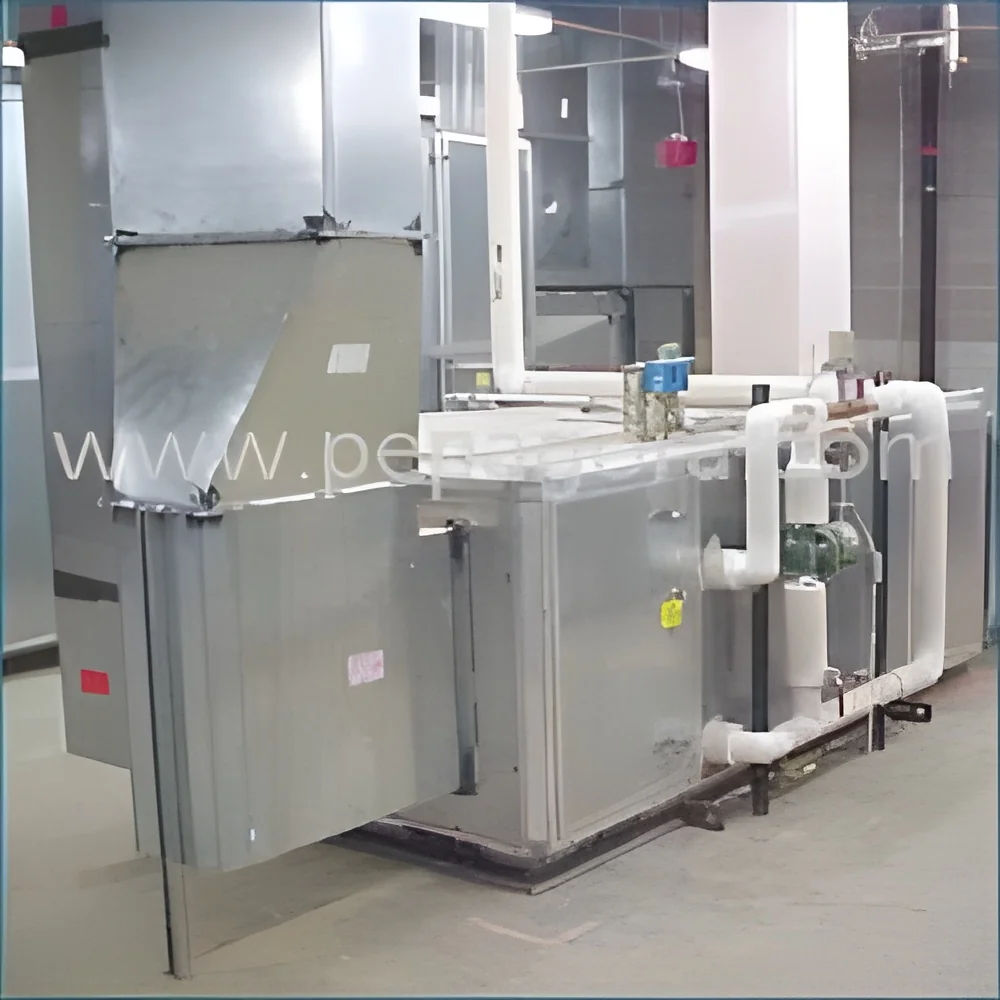
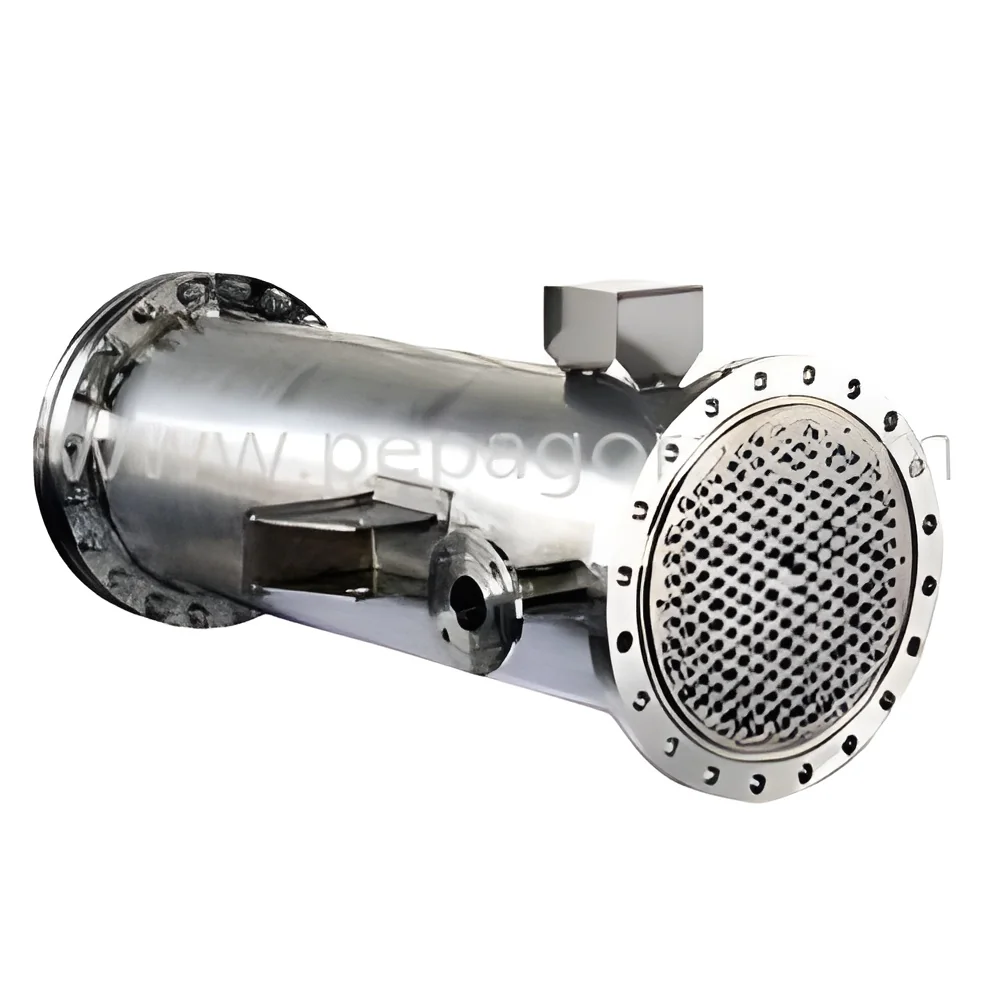
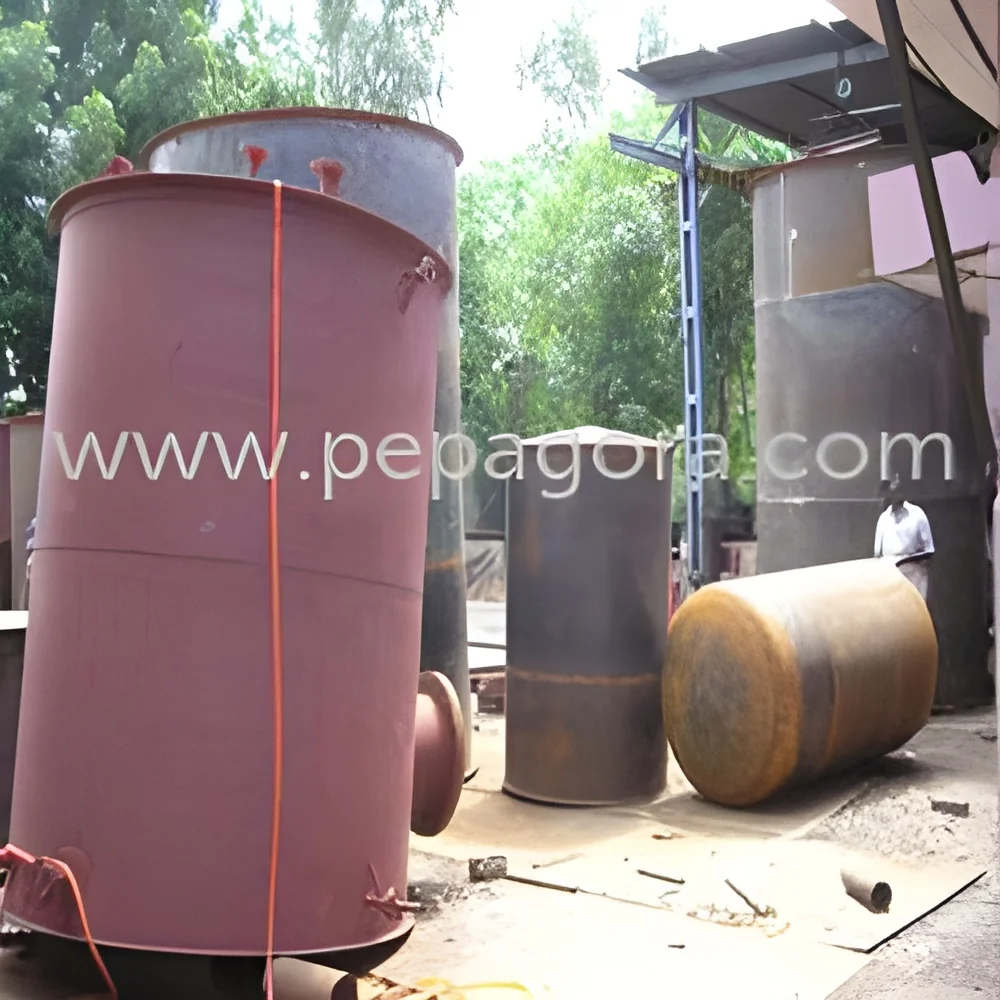
Industrial chemical reactors represent precision-engineered vessels designed for controlled chemical processing across manufacturing sectors. These systems feature customizable heating configurations including hot oil and steam options, providing optimal temperature management for diverse reaction requirements. Built with industrial-grade materials and advanced control systems, they ensure reliable performance during demanding production cycles while maintaining consistent quality output. Their design accommodates various volumes and process parameters, making them suitable for applications ranging from research and development to full-scale industrial manufacturing with exacting standards.

These reactors serve essential functions across multiple industrial sectors, particularly in pharmaceutical manufacturing where they facilitate drug synthesis, intermediate production, and API development under strictly controlled environments. In chemical manufacturing, they enable production of s...
Industrial chemical reactors represent precision-engineered vessels designed for controlled chemical processing across manufacturing sectors. These systems feature customizable heating configurations including hot oil and steam options, providing optimal temperature management for diverse reaction requirements. Built with industrial-grade materials and advanced control systems, they ensure reliable performance during demanding production cycles while maintaining consistent quality output. Their design accommodates various volumes and process parameters, making them suitable for applications ranging from research and development to full-scale industrial manufacturing with exacting standards.

These reactors serve essential functions across multiple industrial sectors, particularly in pharmaceutical manufacturing where they facilitate drug synthesis, intermediate production, and API development under strictly controlled environments. In chemical manufacturing, they enable production of specialty compounds, polymers, and industrial materials requiring precise reaction conditions. The agrochemical industry utilizes them for formulating fertilizers and crop protection products, while petrochemical operations employ them for catalytic processes and hydrocarbon treatment. Their versatility extends to material science, food ingredient processing, and environmental technology applications where controlled chemical reactions are fundamental to product quality and process efficiency.

The business value of these industrial chemical reactors lies in their operational reliability, process efficiency, and customization capabilities that directly impact production economics. Their robust construction minimizes downtime through consistent performance and reduced maintenance requirements, while energy-efficient designs lower operational costs over extended service life. Customization ensures perfect alignment with specific process needs, eliminating compatibility issues and maximizing productivity. Superior engineering delivers long-term value through extended equipment lifespan, consistent output quality, and enhanced manufacturing competitiveness, providing a solid foundation for scalable production operations with predictable performance outcomes.

Key Features:
- Customizable heating configurations with hot oil and steam options for precise temperature control
- Industrial-grade construction using corrosion-resistant materials for durability and long service life
- Advanced control systems for managing temperature, pressure, mixing, and reaction parameters
- Compatibility with both batch processing and continuous operation modes
- Scalable designs accommodating various vessel volumes from pilot scale to industrial production

Benefits:
- Enhanced process reliability through consistent performance and reduced operational downtime
- Improved product quality via precise control over reaction conditions and parameters
- Energy-efficient operation lowering production costs and environmental impact
- Customizable configurations ensuring perfect fit for specific manufacturing requirements
- Long-term value through durable construction, reduced maintenance, and extended equipment lifespan
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial chemical reactors provide precise control over critical reaction parameters like temperature, pressure, and mixing, enabling consistent production outcomes in both batch and continuous operations. Their robust design ensures stable performance during demanding chemical synthesis, polymerization, and material processing tasks, making them fundamental to modern chemical manufacturing workflows.
These versatile systems adapt to various production scales, from pilot plant development to full-scale manufacturing, supporting industries that require controlled reaction environments. Their engineering accommodates different heating methods and process configurations, allowing seamless integration into existing production lines while maintaining operational safety and efficiency standards.
- Pharmaceutical manufacturing for synthesizing active pharmaceutical ingredients (APIs) and drug intermediates under controlled conditions.
- Specialty chemical production for creating polymers, resins, adhesives, and advanced material compounds.
- Agrochemical formulation for producing fertilizers, pesticides, and crop protection chemicals through precise reactions.
- Petrochemical processing for catalytic reactions, hydrocarbon treatment, and refinery operations requiring temperature control.
- Industrial chemical manufacturing for batch production of dyes, pigments, surfactants, and industrial cleaning compounds.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Nimble Industries, Madhya Pradesh
 Madhya Pradesh, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Chemical Reactors For Pharmaceuticals And Manufacturing
Industrial chemical reactors for pharmaceuticals and manufacturing deliver reliable, efficient processing with customizable hot oil or steam heating options to meet specific production requirements across diverse industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Nimble Industries
 Madhya Pradesh, India
Industrial Equipment & MachineryManufacturer