IN
₹
Apparel & Fashion
Description
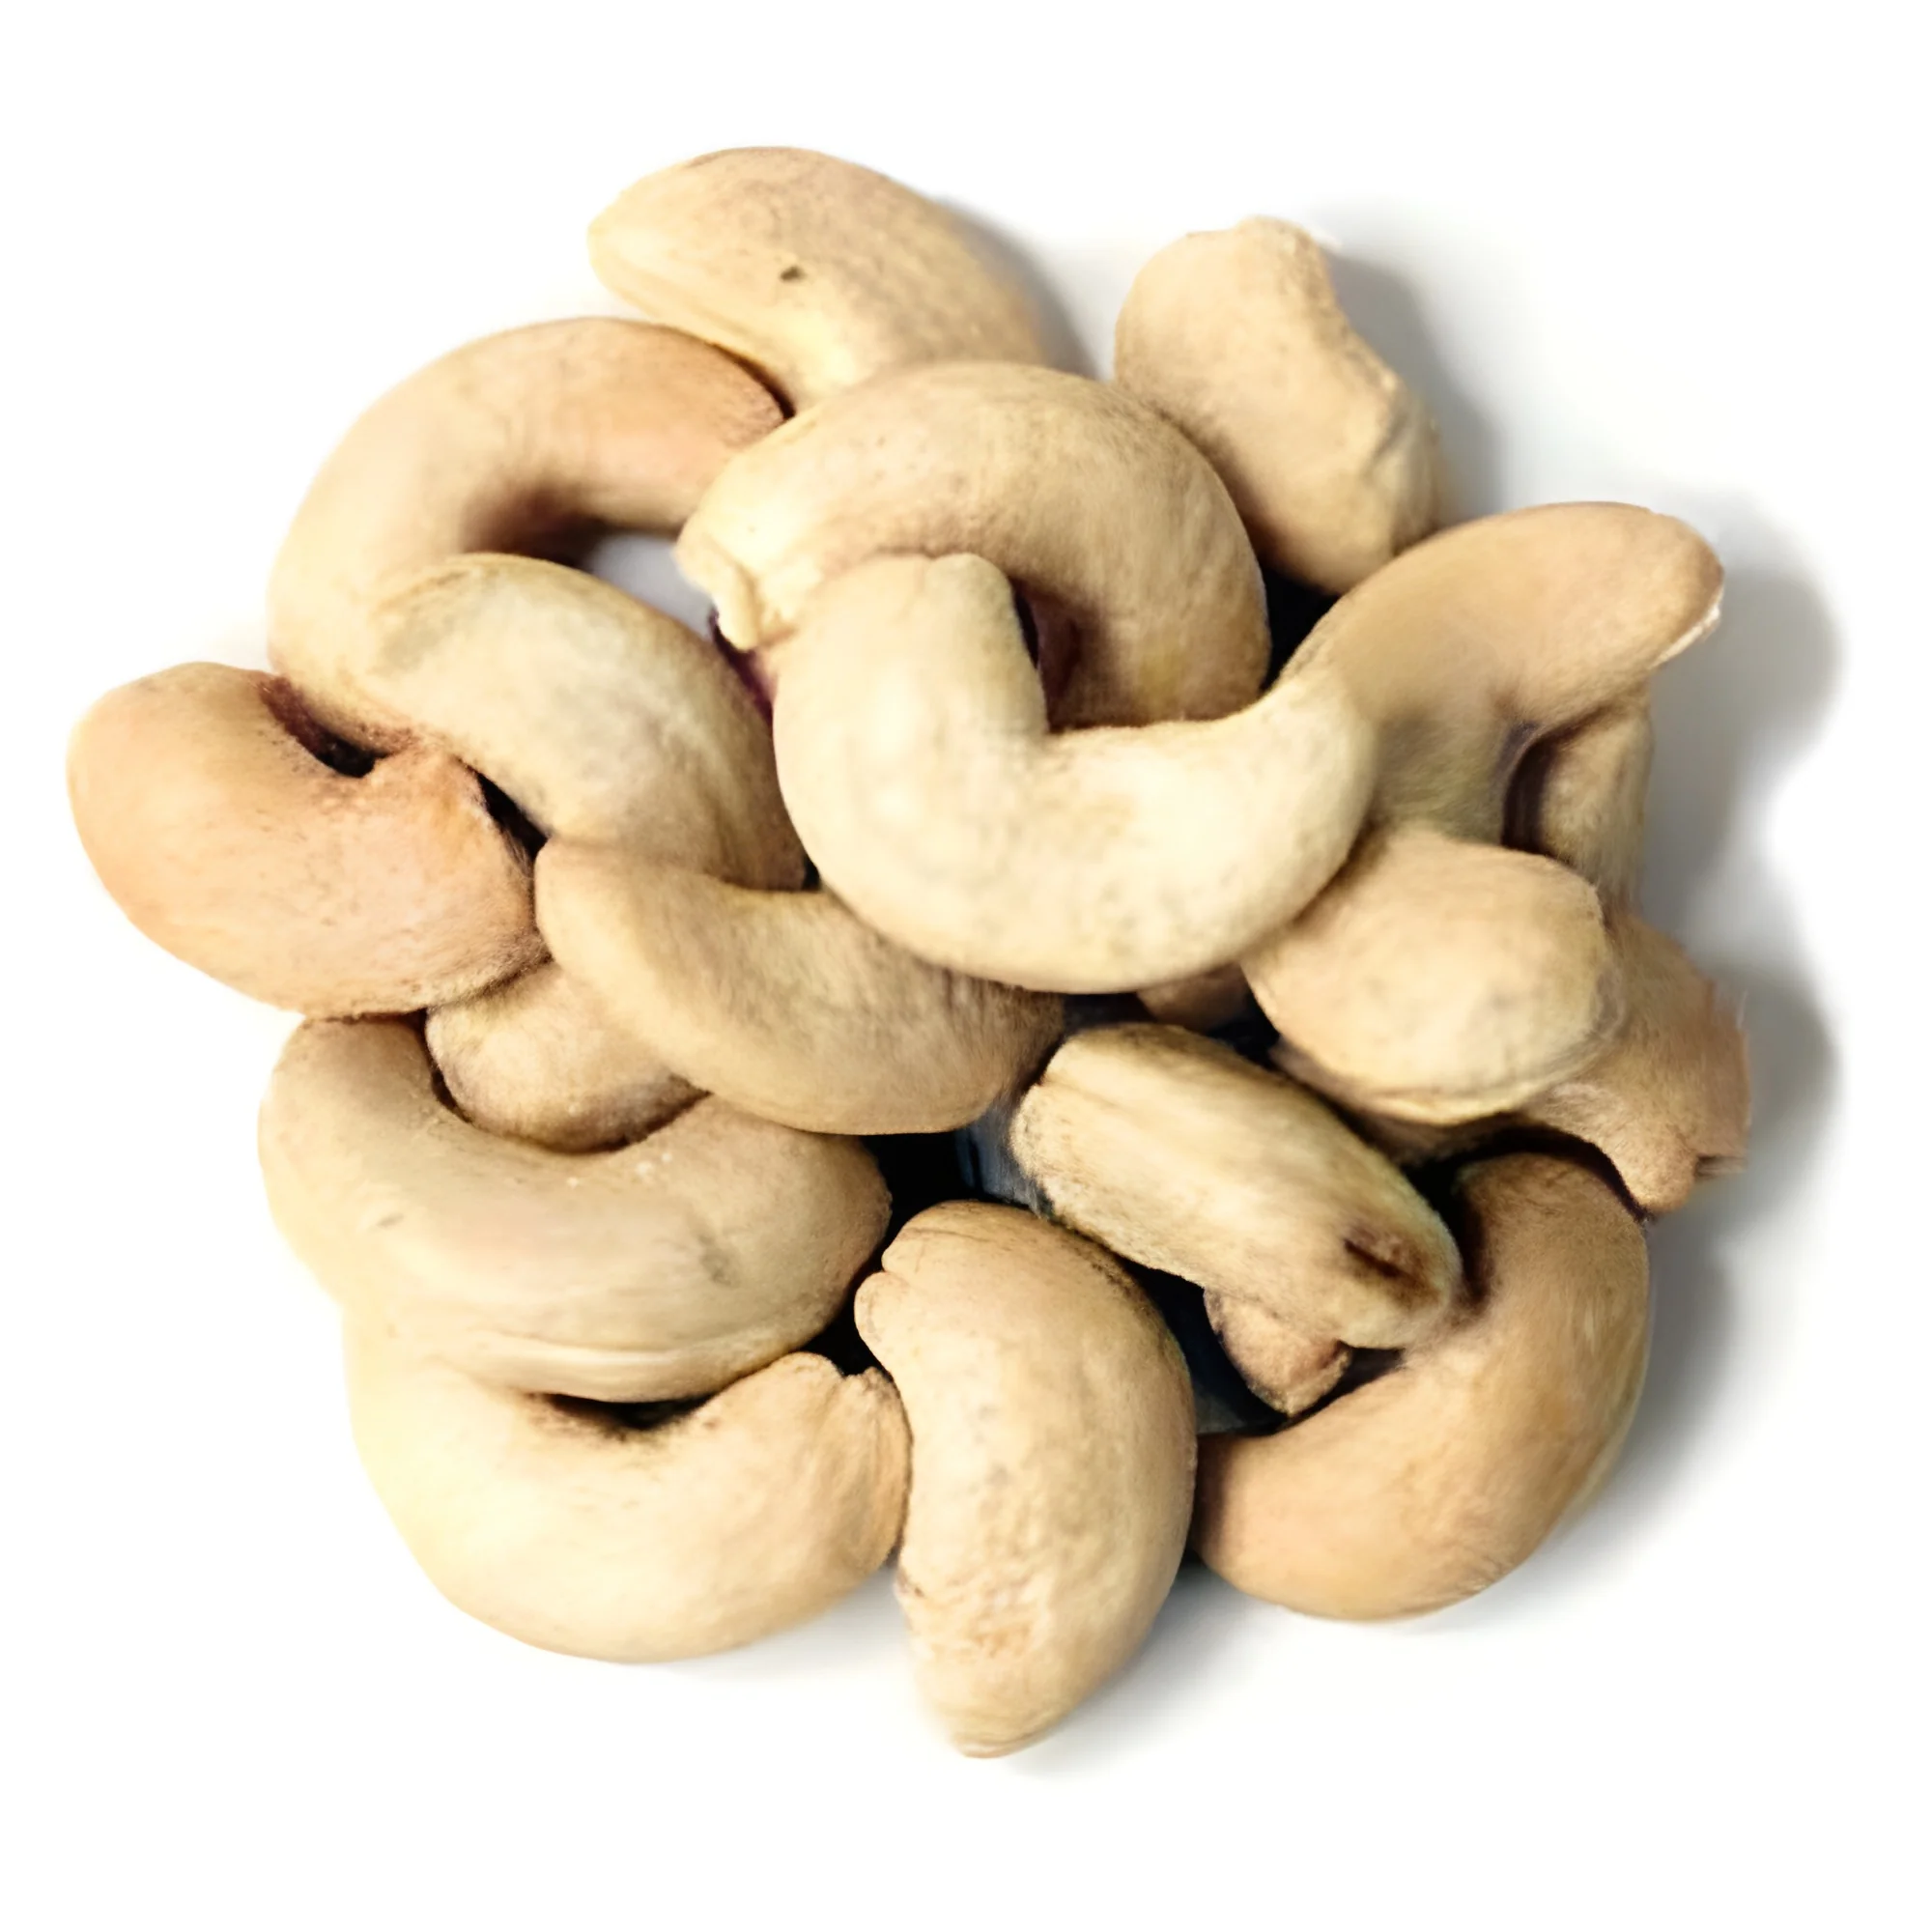
Premium Cashew SW320 Scorched Whole Kernels represent a superior grade of thermally processed cashews that maintain exceptional quality standards despite their scorched appearance. These USDA-grade kernels undergo carefully controlled roasting and drying processes that may cause slight darkening, but this characteristic doesn't compromise their nutritional value, flavor profile, or functional properties. With strict adherence to international food safety standards, these kernels are completely free from infestation, insect damage, and rancidity, ensuring they meet the highest requirements for commercial food production. The SW320 designation indicates consistent sizing between 300-320 kernels per 454 grams, providing the uniformity that food manufacturers require for automated processing, consistent product formulation, and efficient packaging operations. Each shipment includes comprehensive quality certifications and traceability documentation that verify origin, processing methods, a...
Premium Cashew SW320 Scorched Whole Kernels represent a superior grade of thermally processed cashews that maintain exceptional quality standards despite their scorched appearance. These USDA-grade kernels undergo carefully controlled roasting and drying processes that may cause slight darkening, but this characteristic doesn't compromise their nutritional value, flavor profile, or functional properties. With strict adherence to international food safety standards, these kernels are completely free from infestation, insect damage, and rancidity, ensuring they meet the highest requirements for commercial food production. The SW320 designation indicates consistent sizing between 300-320 kernels per 454 grams, providing the uniformity that food manufacturers require for automated processing, consistent product formulation, and efficient packaging operations. Each shipment includes comprehensive quality certifications and traceability documentation that verify origin, processing methods, and compliance with global food safety regulations.

This product serves numerous industrial sectors including food manufacturing, bakery and confectionery production, food service distribution, and wholesale ingredient supply. Food processing facilities utilize SW320 cashews in automated production lines for snack bars, baked goods, ready-to-eat meals, and packaged foods where consistent sizing ensures even distribution in mixed products and reliable performance in manufacturing equipment. The hospitality and food service industry values these cashews for culinary applications where they're incorporated into sauces, desserts, main dishes, and specialty menu items. Bulk ingredient suppliers and distributors stock SW320 for their commercial kitchen clients who require reliable quality in high-volume operations, while exporters and importers favor this grade for its competitive pricing, consistent availability, and compliance with international trade requirements.

Businesses selecting Premium Cashew SW320 gain significant value through reliable supply chain partnerships and consistent product quality that reduces production variances and minimizes waste. The slightly scorched characteristics provide cost advantages without sacrificing taste, nutritional content, or functional properties, making them an intelligent choice for buyers who balance quality requirements with budget considerations. The product's compliance with international food safety standards ensures smooth customs clearance and market acceptance across global destinations, while comprehensive documentation supports quality assurance programs and regulatory compliance. With transparent pricing structures and reliable availability, businesses can accurately forecast ingredient costs, maintain competitive pricing in their markets, and build consistent product quality that strengthens brand reputation and customer loyalty.

Key Features:
- USDA grade SW320 designation ensuring compliance with quality standards and specifications
- Consistent sizing of 300-320 kernels per 454 grams for processing uniformity and reliable performance
- Maximum 5% moisture content preventing spoilage during storage, transport, and shelf life
- Strict quality control with maximum 5% broken pieces and 7.5% non-specified categories
- Comprehensive documentation including traceability, food safety certifications, and quality assurance records

Benefits:
- Reliable performance in automated processing equipment due to consistent sizing and quality
- Cost-effective solution for food manufacturing without compromising taste or nutritional value
- Reduced production variances and minimized waste through consistent quality and specifications
- Smooth customs clearance and market acceptance with international compliance documentation
- Transparent supply chain with traceability from origin to final destination for quality assurance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Premium Cashew SW320 Scorched Whole Kernels are engineered for food manufacturers and bulk ingredient suppliers who prioritize consistent quality and cost-effectiveness. The controlled roasting process creates a slightly darkened appearance that doesn't compromise flavor or texture, making these kernels perfect for applications where taste matters more than visual perfection. With strict adherence to industry standards including maximum 5% broken pieces, these cashews deliver reliable performance in production environments where consistency is critical for automated processing and packaging operations.
These versatile kernels serve multiple sectors within the food industry, from confectionery and bakery production to ready-to-eat meal manufacturing. Their thermal processing characteristics make them particularly suitable for applications requiring additional cooking or roasting, as they maintain structural integrity throughout production processes. Food service providers and industrial kitchens also utilize this grade for culinary preparations where cashews are incorporated into cooked dishes rather than served as standalone snack items, providing both flavor enhancement and nutritional value to finished products.
- Baking industry applications including cookies, cakes, pastries, and bread products
- Confectionery production for chocolate coatings, nut clusters, energy bars, and sweets
- Culinary uses in restaurants and food service for sauces, curries, and stir-fry dishes
- Processed food manufacturing in ready-to-eat meals, snack mixes, and packaged foods
- Bulk ingredient preparation for industrial food processing and packaging operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | cochin port |
Company Profile
AASHRAY INCORPORATION, Gujarat
 Gujarat, India
Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Cashew SW320 Scorched Whole Kernels USDA Grade
Premium Cashew SW320 Scorched Whole Kernels offer USDA-grade quality with 5% max moisture, ideal for food manufacturing and bulk ingredient supply. These scorched kernels provide consistent sizing and reliable performance for industrial applications.
Min. Order Quantity: 15 Metric
Price₹6650-₹7150
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
AASHRAY INCORPORATION
 Gujarat, India
Manufacturer