IN
₹
Apparel & Fashion
Description
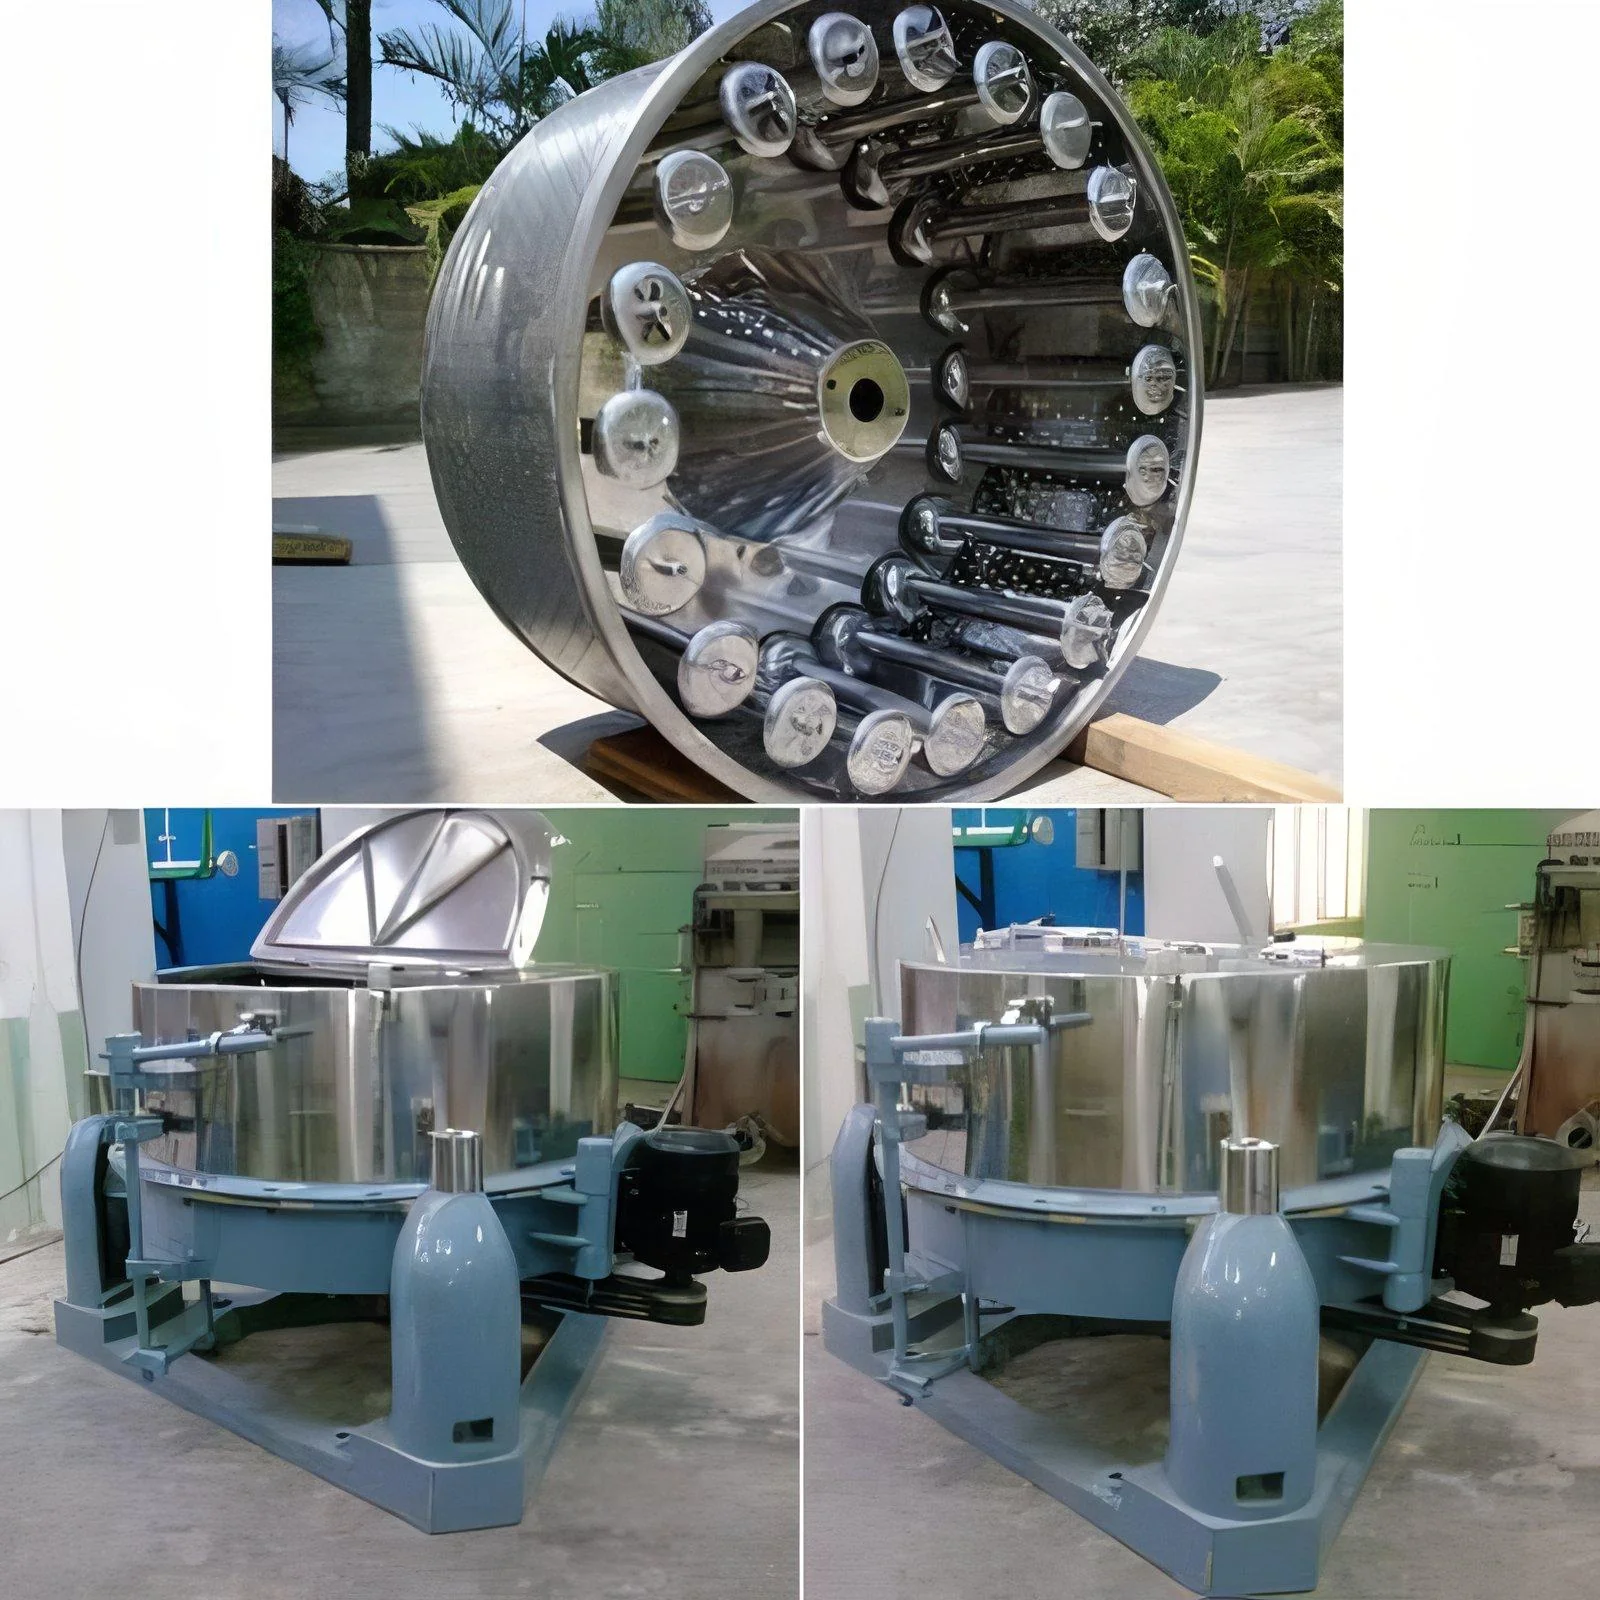
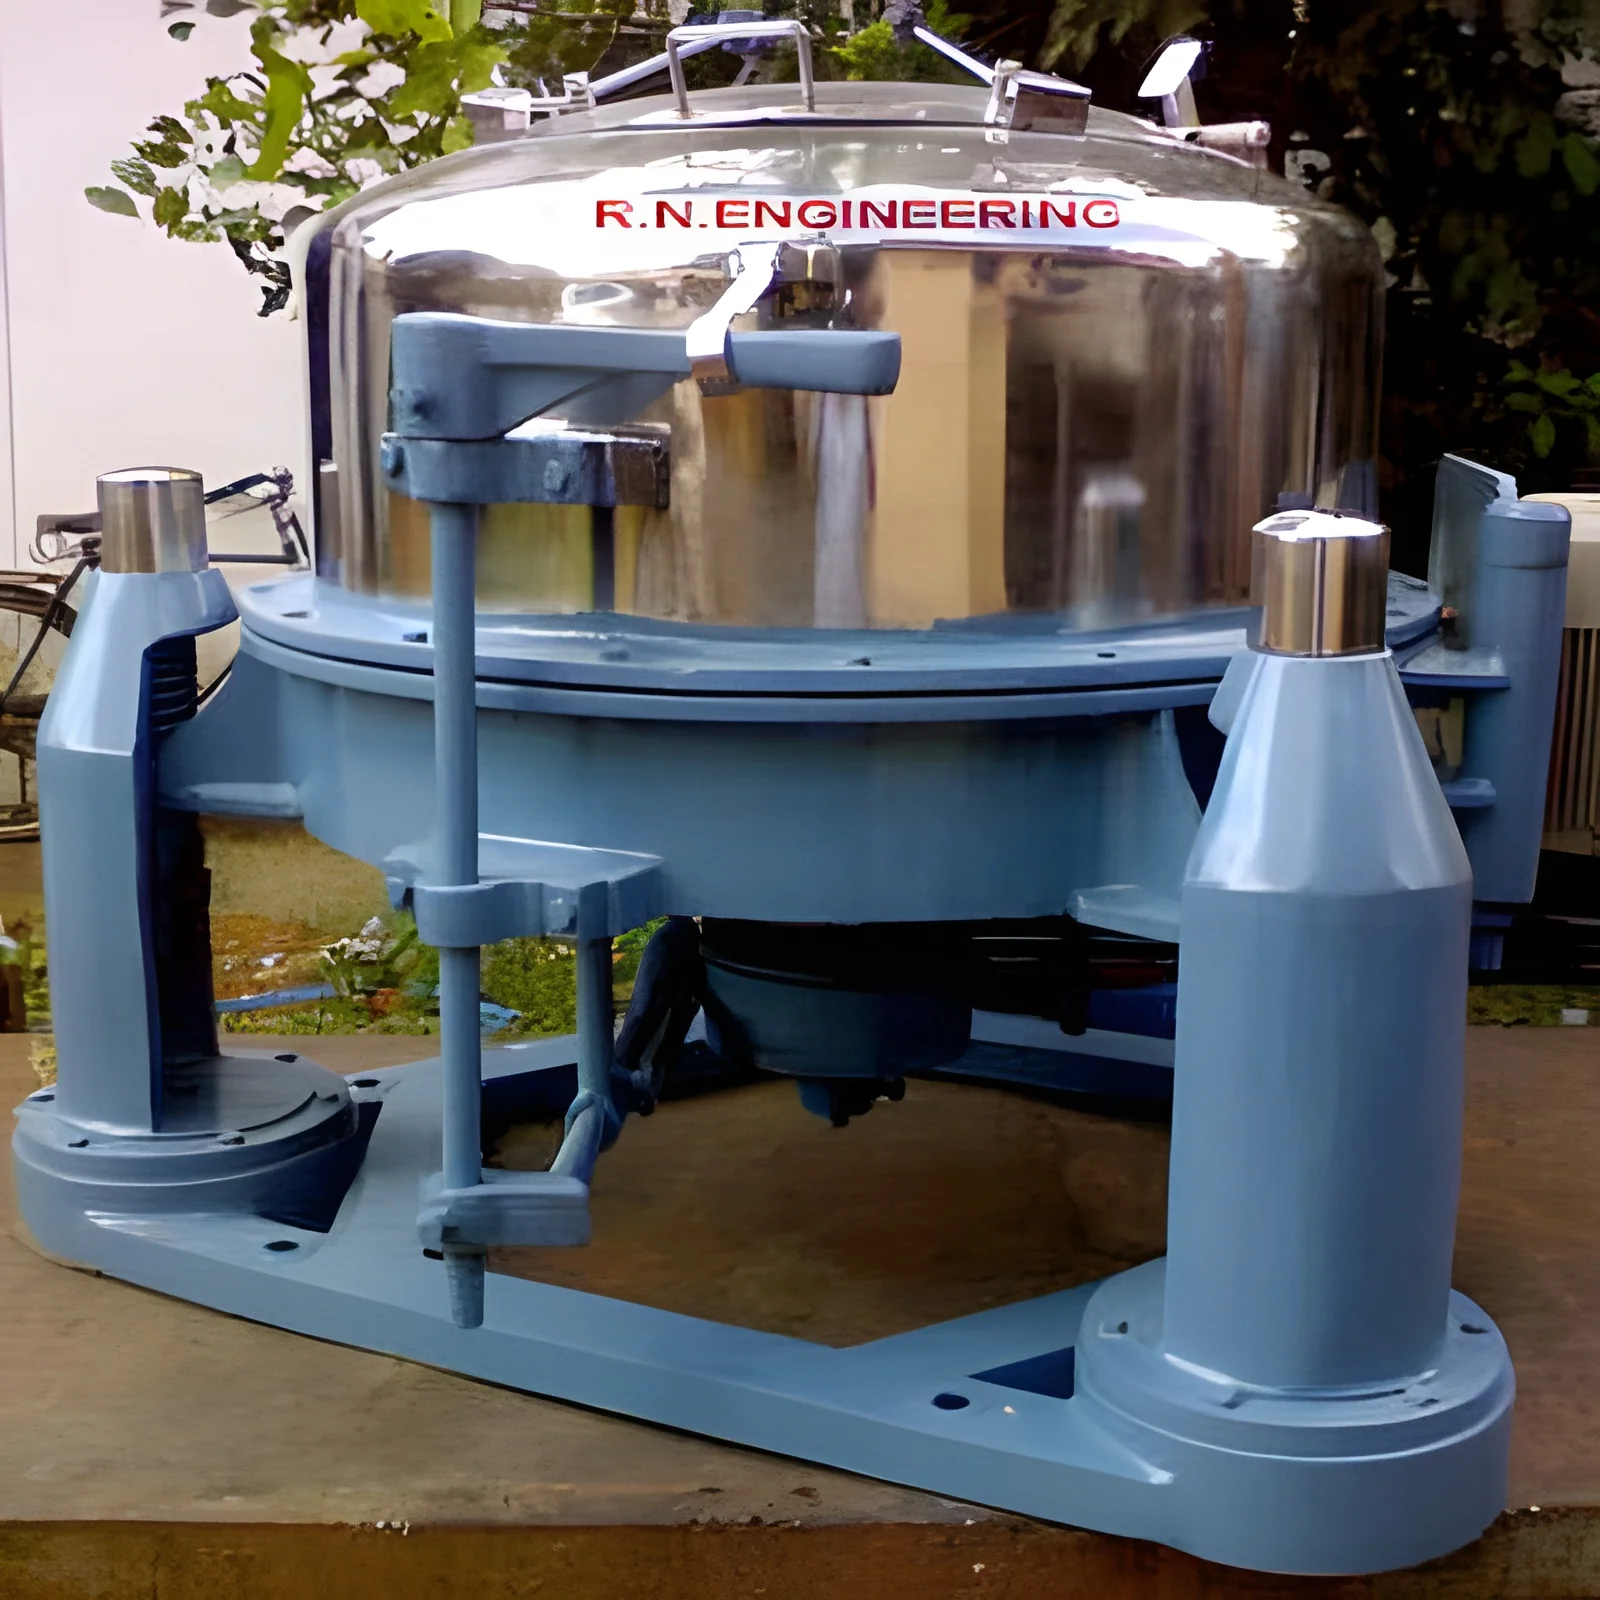
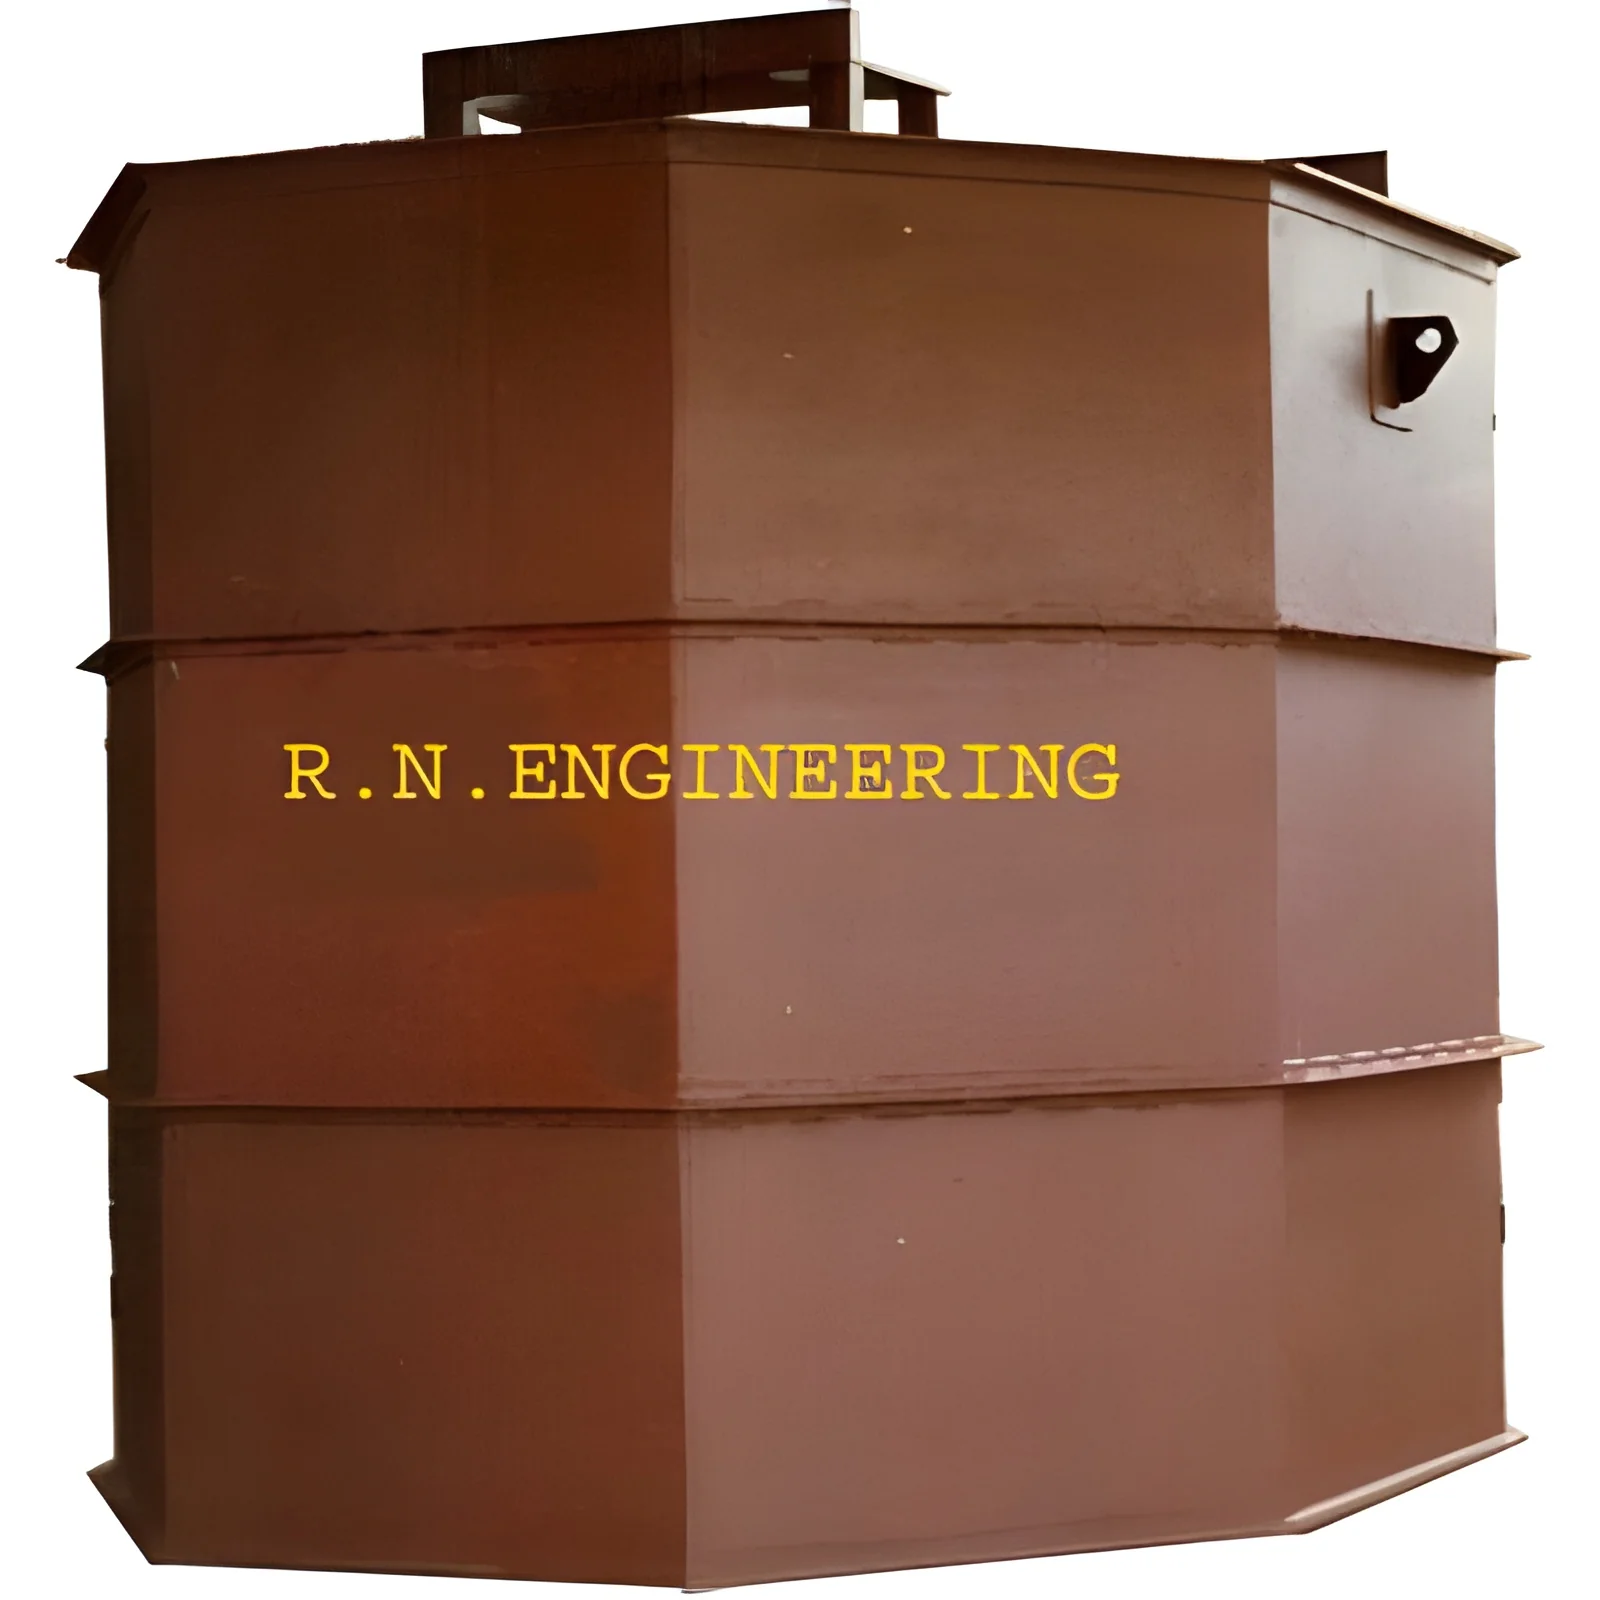
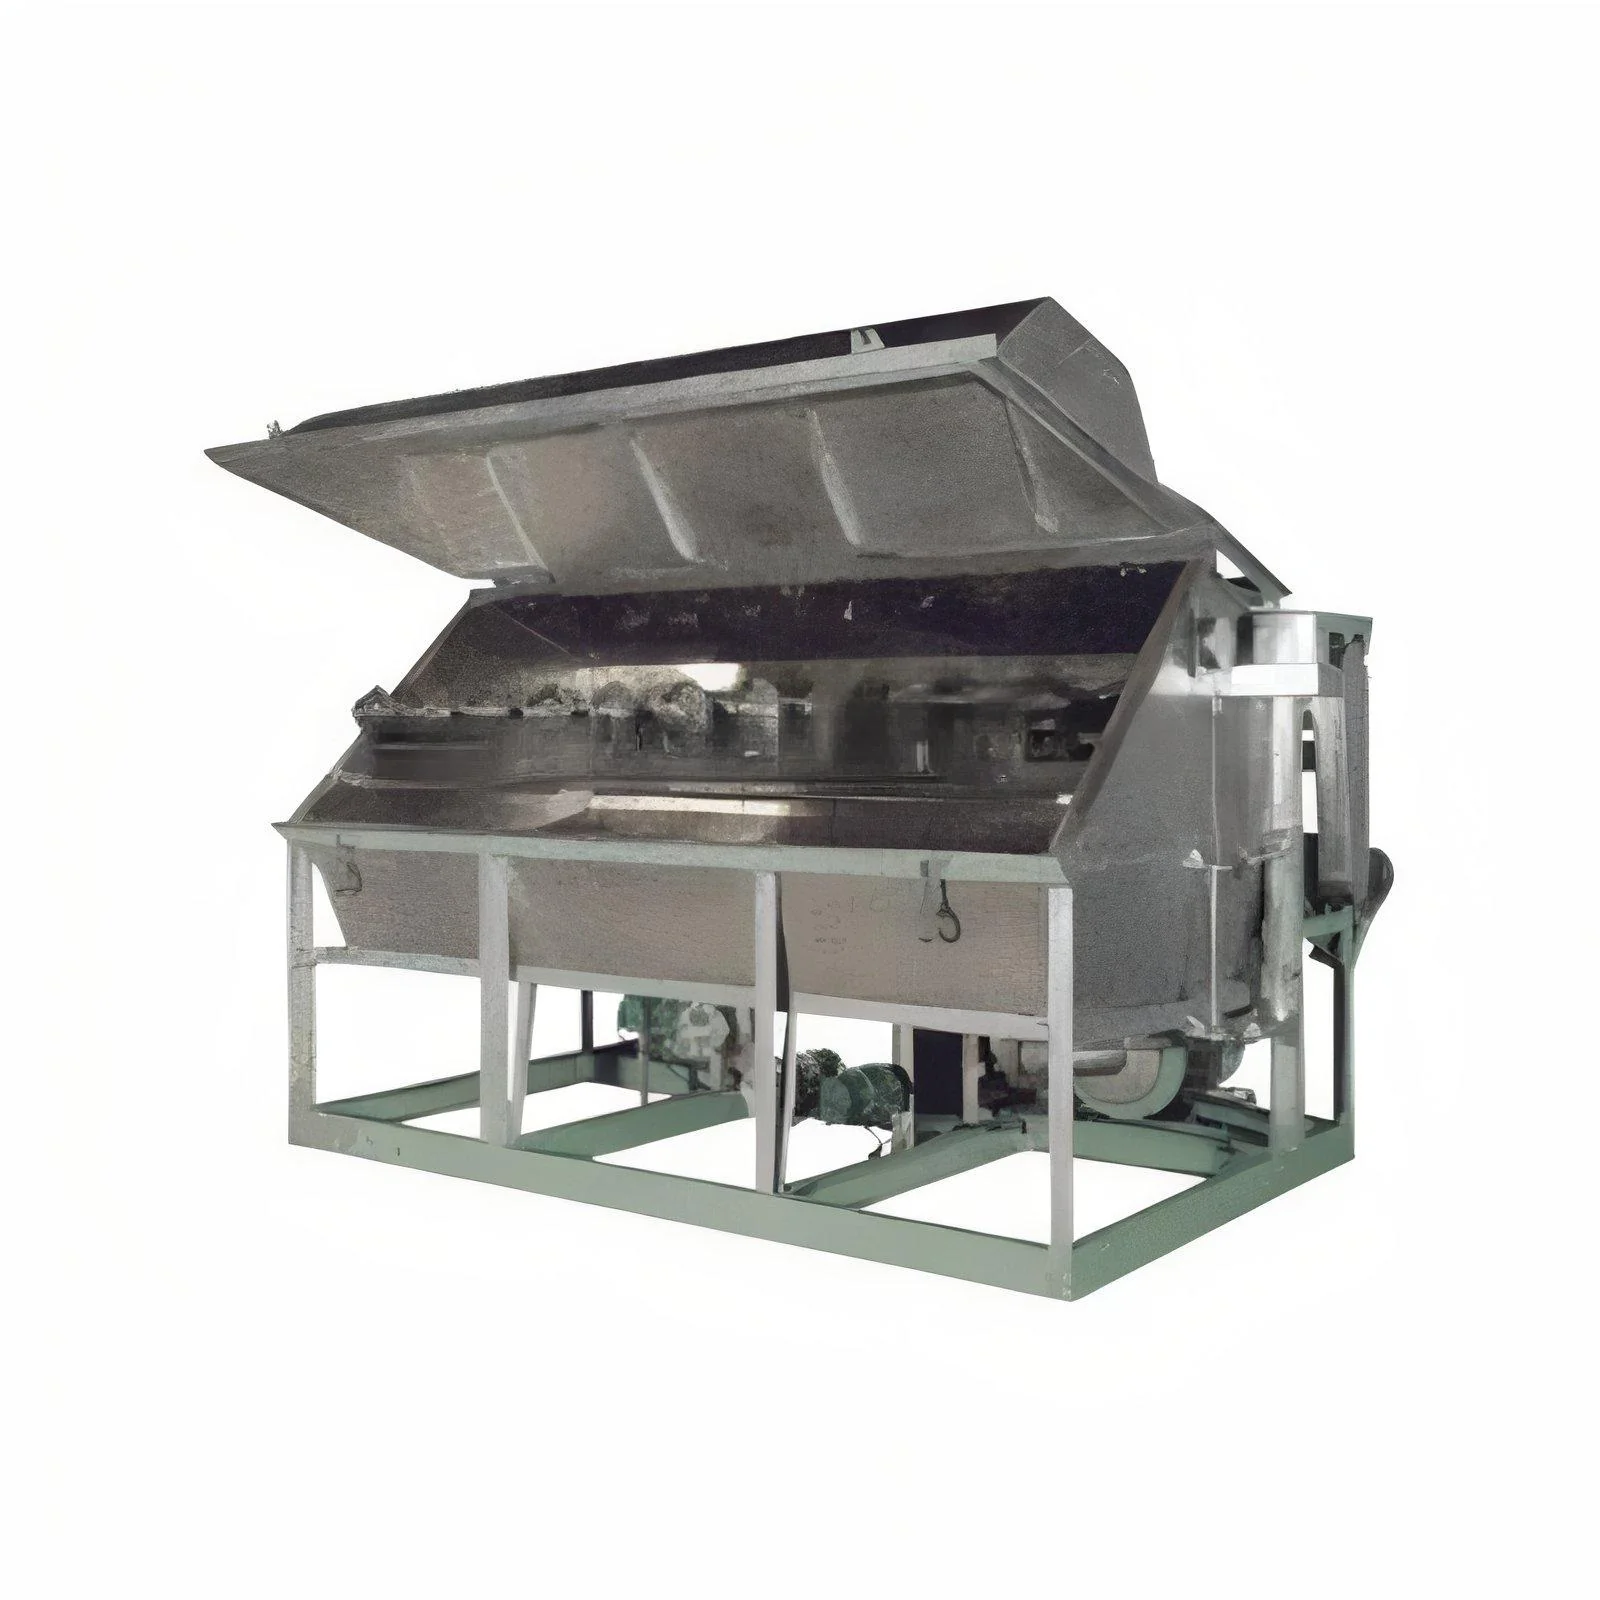
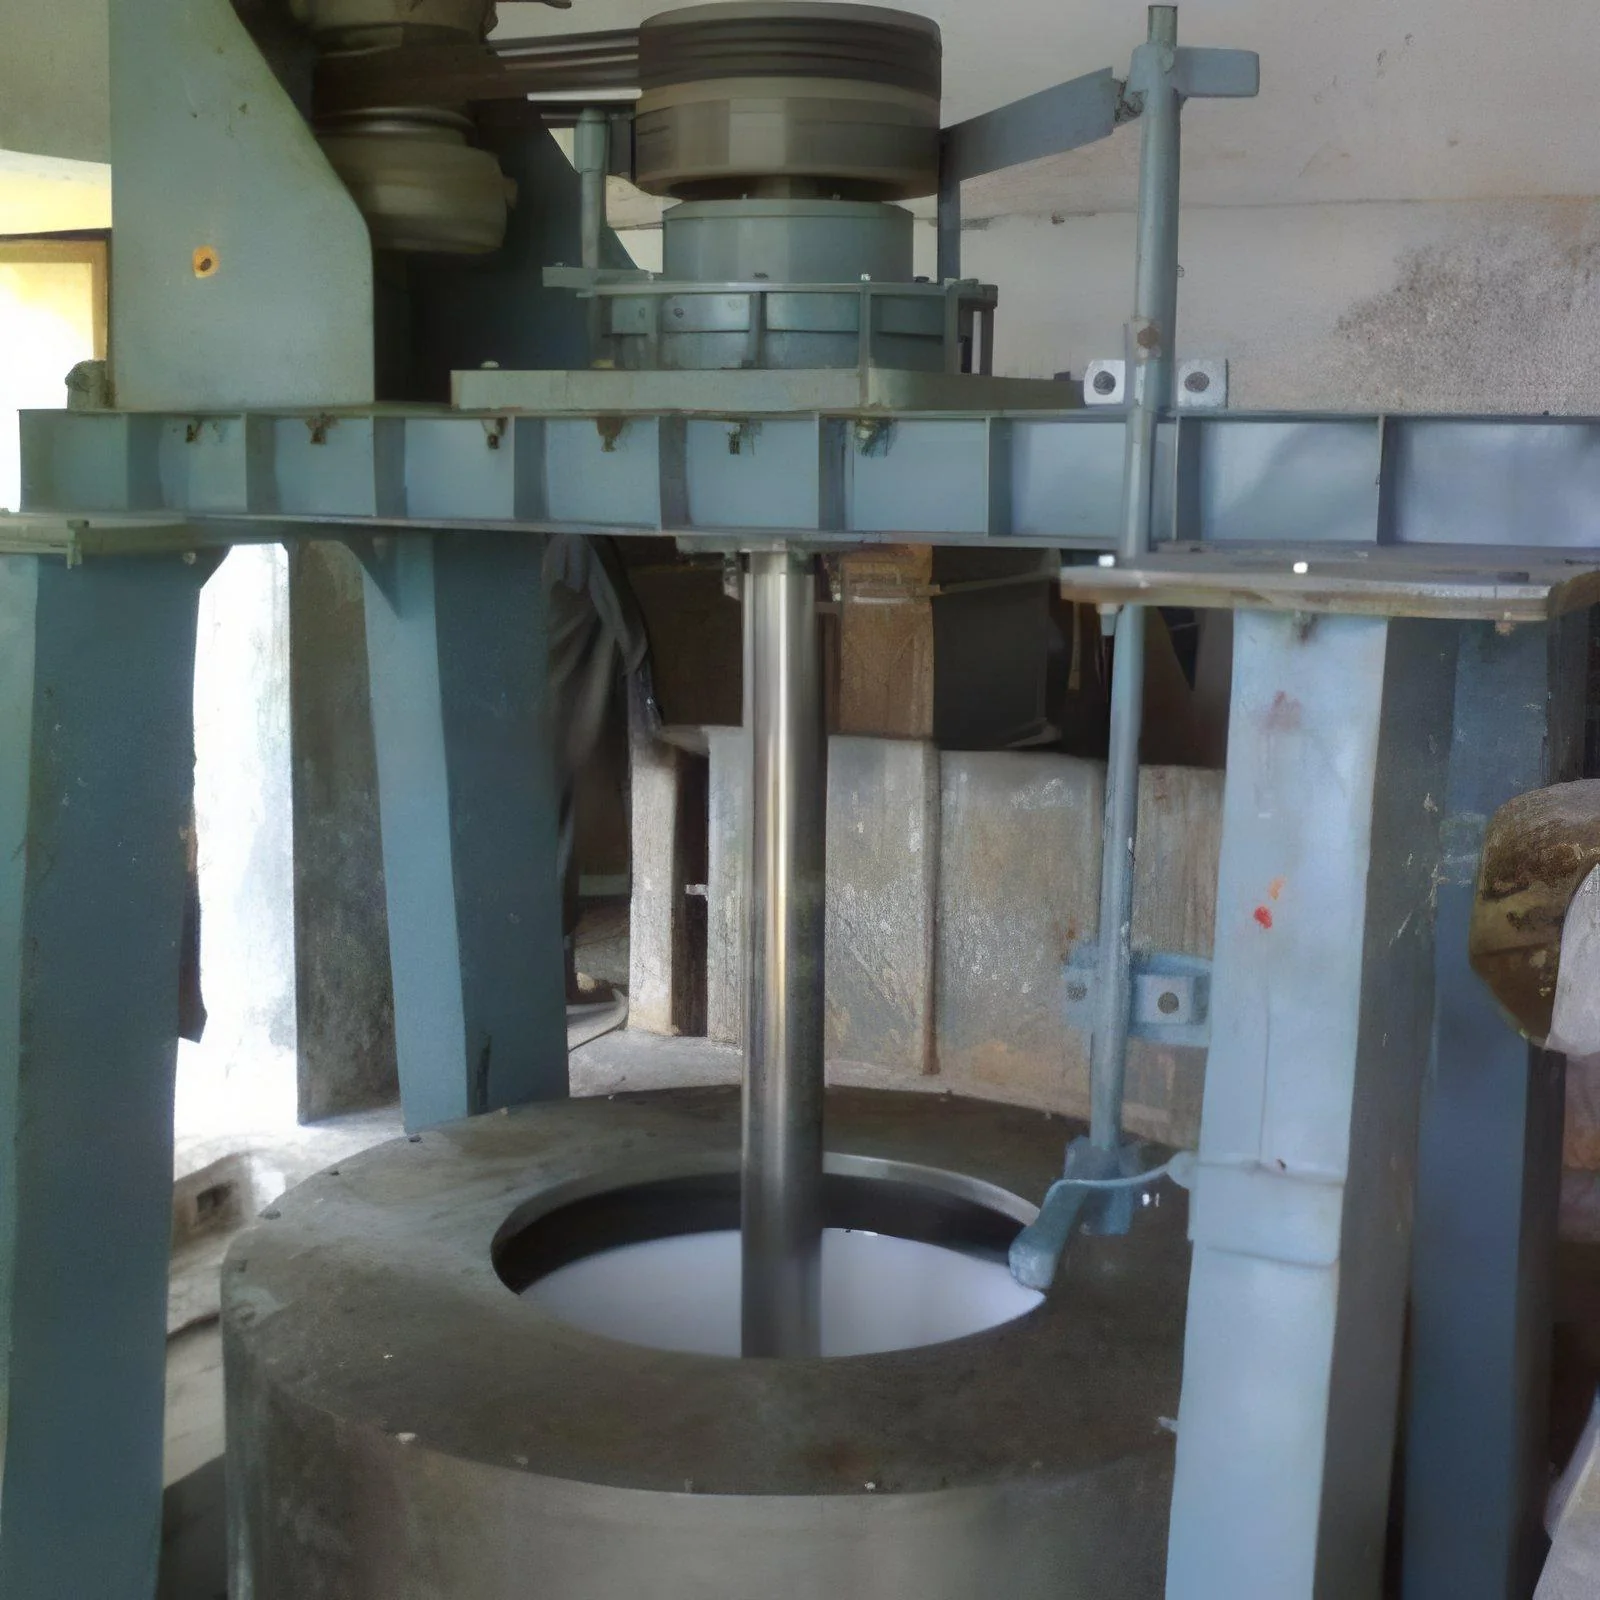
R.N. Engineering's Bottom Discharge Centrifuge Machine represents advanced separation technology specifically engineered for industrial applications requiring efficient solid-liquid separation. This machine combines robust engineering principles with user-friendly operation to deliver consistent, high-performance results in the most demanding processing environments. The centrifuge features an innovative bottom discharge mechanism that ensures smooth, continuous operation without interrupting the separation process, making it ideal for operations where production continuity is critical. The superior construction quality and reliable components ensure that this machine can handle heavy-duty industrial applications across multiple sectors with consistent performance and minimal maintenance requirements.

This industrial centrifuge serves multiple sectors including chemical processing plants for catalyst recovery and product separation, pharmaceutical manufacturing for active ingredient p...
R.N. Engineering's Bottom Discharge Centrifuge Machine represents advanced separation technology specifically engineered for industrial applications requiring efficient solid-liquid separation. This machine combines robust engineering principles with user-friendly operation to deliver consistent, high-performance results in the most demanding processing environments. The centrifuge features an innovative bottom discharge mechanism that ensures smooth, continuous operation without interrupting the separation process, making it ideal for operations where production continuity is critical. The superior construction quality and reliable components ensure that this machine can handle heavy-duty industrial applications across multiple sectors with consistent performance and minimal maintenance requirements.

This industrial centrifuge serves multiple sectors including chemical processing plants for catalyst recovery and product separation, pharmaceutical manufacturing for active ingredient purification, wastewater treatment facilities for sludge dewatering, food processing operations for product clarification, and mining operations for mineral recovery. Each industry benefits from the machine's ability to handle varying material characteristics and processing requirements while maintaining high separation efficiency. The equipment's versatility across different applications makes it a valuable asset for operations requiring reliable solid-liquid separation technology that can adapt to diverse processing needs and material characteristics.

The business value of this centrifuge machine lies in its operational reliability, continuous processing capability, and long-term cost efficiency. The bottom discharge mechanism eliminates the need for production stoppages, significantly increasing throughput and operational efficiency. Superior construction using industrial-grade materials ensures extended service life with minimal maintenance requirements, reducing total cost of ownership. The easy-to-use design minimizes training time and operational complexity, while the multiple size options provide flexibility to match specific processing capacity requirements without compromising performance or efficiency.

Key Features:
- Available in three standard sizes: 24, 36, and 48 inch configurations
- Power range of 30-45 Kw for efficient and reliable operation
- Bottom discharge mechanism enabling continuous processing without interruption
- Superior quality construction using durable, industrial-grade materials
- Easy-to-use design with straightforward operation and minimal training requirements

Benefits:
- Continuous operation capability increases production throughput and efficiency
- Robust construction ensures long service life with minimal maintenance needs
- Multiple size options provide flexibility for different processing capacities
- User-friendly design reduces operator training time and operational complexity
- Reliable performance across various industrial applications and material types
Specifications
| Key Attributes | |
|---|---|
| Condition | New |
| Dimension(L*W*H) | Machine Model |
| Power(W) | Kilowatt,5 |
| Product Type | Fertilizer |
| Type | Bottom Discharge Centrifuge Machine |
| Voltage | Volt,380 |
| Weight | 50 to 100 Kg |
| Sizes | 24â€, 36†and 48†|
| Centrifuge | Three Foot Centrifuge |
| Type | Centrifuge |
| Condition | New |
| Dimension | According to The Machine |
| Power | 30-45 Kw |
| Feature | Easy to Use |
| Quality | Superior |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The Bottom Discharge Centrifuge Machine provides superior solid-liquid separation performance across demanding industrial environments. Its robust engineering ensures consistent reliability and operational efficiency even under continuous processing conditions, making it ideal for heavy-duty applications where production continuity is essential. This industrial centrifuge is specifically designed for applications requiring precise separation and uninterrupted operation. Industries benefit from multiple sizing options, superior build quality, and straightforward maintenance procedures that support long-term operational excellence and cost-effective performance in various processing scenarios.
Real-world applications:
- Chemical manufacturing plants for efficient separation of catalysts and reaction products
- Pharmaceutical production facilities for precise active ingredient recovery and purification
- Wastewater treatment plants for effective sludge dewatering and processing operations
- Food and beverage processing units for product purification and clarification processes
- Mining and mineral operations for valuable material recovery and processing applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Bangalore |
Company Profile

R.N. Engineering, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Bottom Discharge Centrifuge Machine 24 48 Inch 30 45 Kw
R.N. Engineering Industrial Bottom Discharge Centrifuge Machine delivers efficient solid-liquid separation for chemical, pharmaceutical, and wastewater treatment. Available in 24, 36, 48 inch sizes with 30-45 Kw power for reliable continuous processing.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
R.N. Engineering
 Karnataka, India
Industrial Equipment & MachineryManufacturer