IN
₹
Description
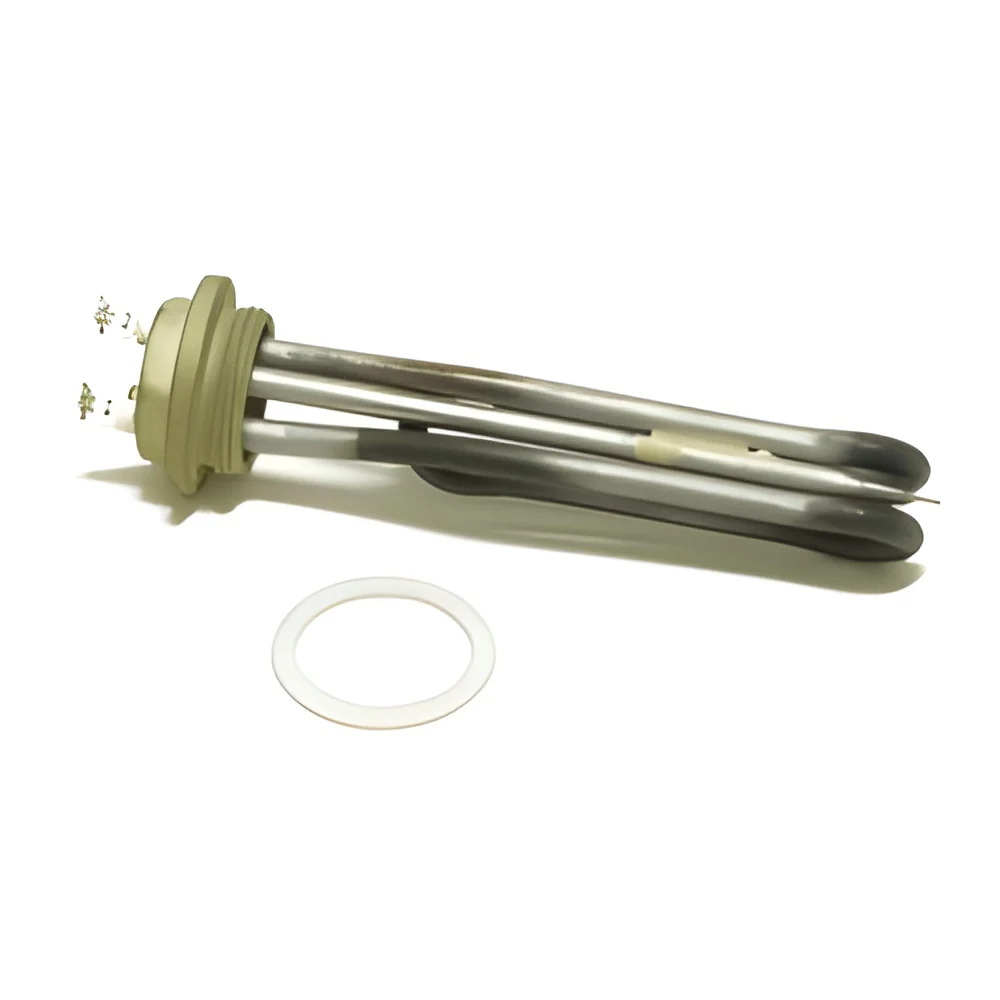
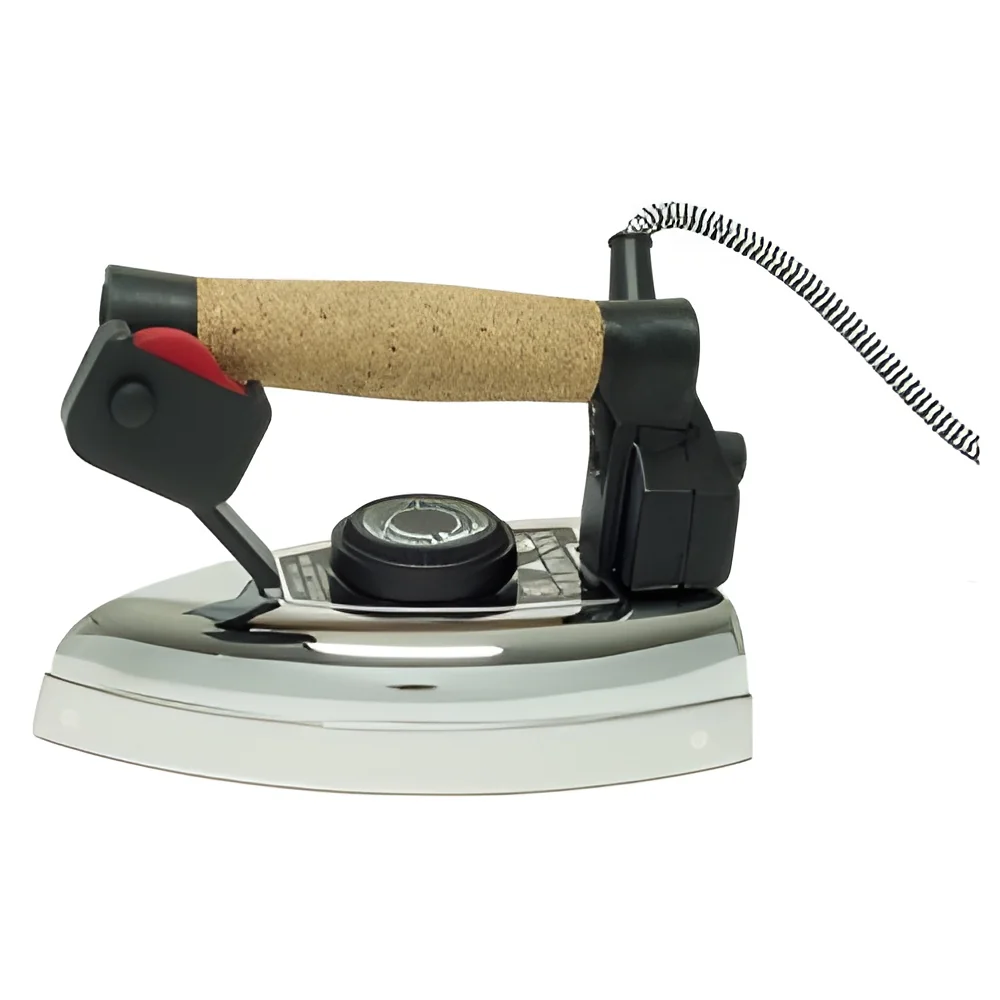
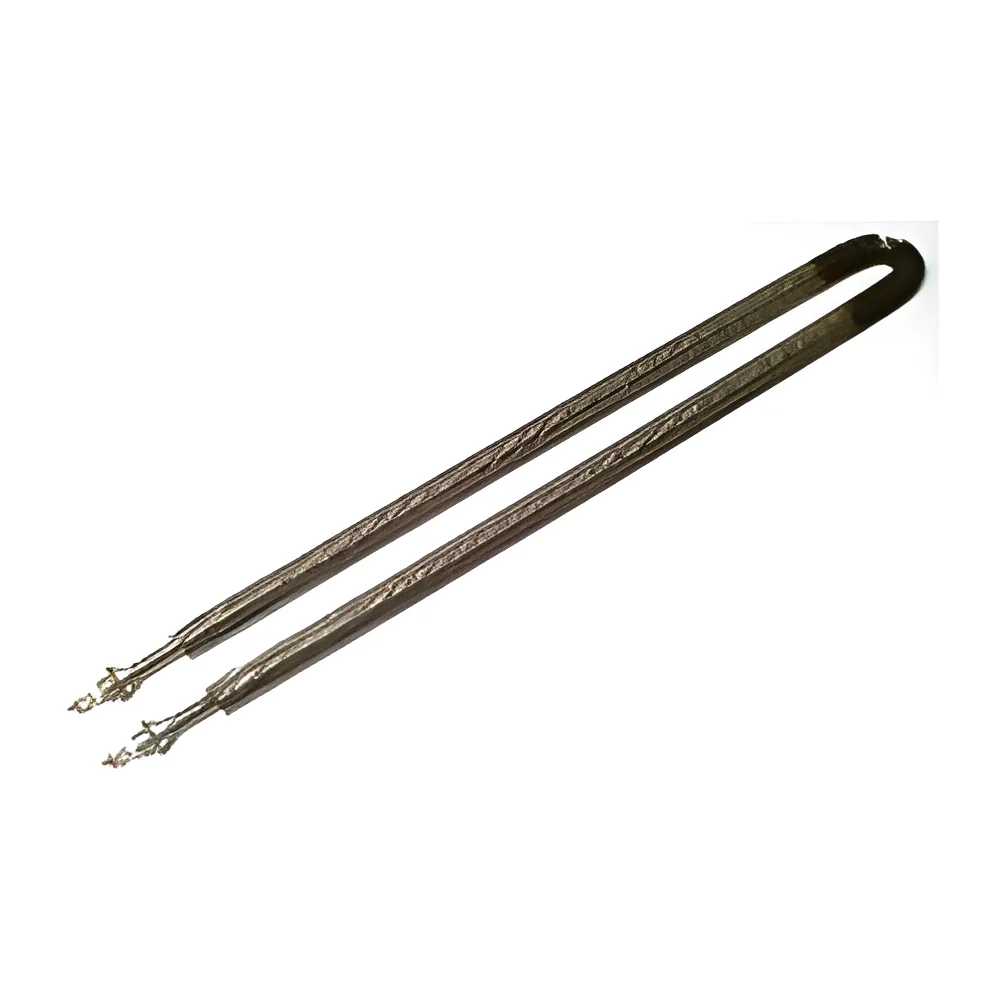
Our industrial boiler heaters represent precision engineering solutions designed for demanding thermal applications across various industrial sectors. These robust heating systems deliver consistent performance while maintaining operational reliability in challenging environments. Built with durability as a core principle, each unit undergoes comprehensive quality verification to ensure optimal performance in industrial settings. The heaters incorporate advanced thermal efficiency technology that maximizes heat transfer while reducing energy consumption, making them economically viable and environmentally responsible choices for businesses seeking sustainable heating solutions.

These boiler heaters serve extensive applications across multiple industries including manufacturing, processing, chemical production, and commercial heating sectors. Manufacturing plants utilize them for essential process heat in production lines and equipment operations. The food processing industry depends o...
Our industrial boiler heaters represent precision engineering solutions designed for demanding thermal applications across various industrial sectors. These robust heating systems deliver consistent performance while maintaining operational reliability in challenging environments. Built with durability as a core principle, each unit undergoes comprehensive quality verification to ensure optimal performance in industrial settings. The heaters incorporate advanced thermal efficiency technology that maximizes heat transfer while reducing energy consumption, making them economically viable and environmentally responsible choices for businesses seeking sustainable heating solutions.

These boiler heaters serve extensive applications across multiple industries including manufacturing, processing, chemical production, and commercial heating sectors. Manufacturing plants utilize them for essential process heat in production lines and equipment operations. The food processing industry depends on these heaters for steam generation and temperature maintenance throughout various production stages. Chemical and pharmaceutical manufacturers rely on them for accurate temperature control in sensitive manufacturing processes. Commercial facilities implement them for space heating and hot water supply in large-scale operations. The versatility of these units makes them suitable for both primary heating systems and supplementary heat support in complex industrial environments.

The operational value of these boiler heaters extends beyond basic heating functionality to include long-term reliability and cost efficiency. Their sturdy construction ensures minimal operational interruptions and reduced maintenance expenses, while the energy-efficient design translates to significant operational cost savings. The units are engineered to meet industry standards and safety regulations, providing confidence for facility managers and operational teams. The reliability of these heaters supports continuous production processes, making them valuable assets for businesses where uninterrupted operation is crucial to productivity and customer satisfaction. Their design focuses on delivering consistent performance while minimizing environmental impact through efficient energy utilization.

Key Features:
- High-performance thermal technology for efficient heat transfer and distribution
- Durable construction using industrial-grade materials for extended service life
- Reliable operation designed for continuous industrial use and demanding conditions
- Compliance with industry standards and safety regulations for operational security
- Flexible installation options suitable for various industrial configurations and spaces

Benefits:
- Consistent thermal performance ensures reliable process heating and temperature control
- Reduced maintenance requirements lower operational costs and minimize downtime
- Energy-efficient operation decreases fuel consumption and utility expenses
- Long service life provides excellent return on investment and operational value
- Safe and compliant design ensures workplace safety and regulatory adherence
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial boiler heaters provide consistent thermal performance for demanding commercial and manufacturing heating requirements. Engineered to maintain precise temperature control in challenging environments, these units ensure operational reliability and process efficiency across multiple industrial sectors. They are particularly valuable where accurate heat management is essential for production quality and safety standards.
These robust heating solutions serve diverse industrial applications with reliable performance and minimal maintenance needs. From large-scale manufacturing facilities to specialized processing plants, our boiler heaters deliver dependable service in complex industrial setups. The units are designed to handle both primary heating systems and auxiliary heat support requirements efficiently and effectively.
- Providing essential process heat for chemical manufacturing and petroleum refining operations
- Supporting steam generation requirements in food processing and beverage production facilities
- Maintaining precise temperature control in pharmaceutical manufacturing environments
- Delivering heating solutions for textile industry dyeing and finishing processes
- Supporting district heating systems for commercial complexes and industrial parks
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Delhi Steam System Co., New Delhi
 New Delhi, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Boiler Heaters High Performance Durable Construction
Industrial boiler heaters deliver high-performance thermal solutions for manufacturing plants and processing units. Featuring durable construction and reliable operation for demanding industrial heating applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Delhi Steam System Co.
 New Delhi, India
Manufacturer