IN
₹
Apparel & Fashion
Description
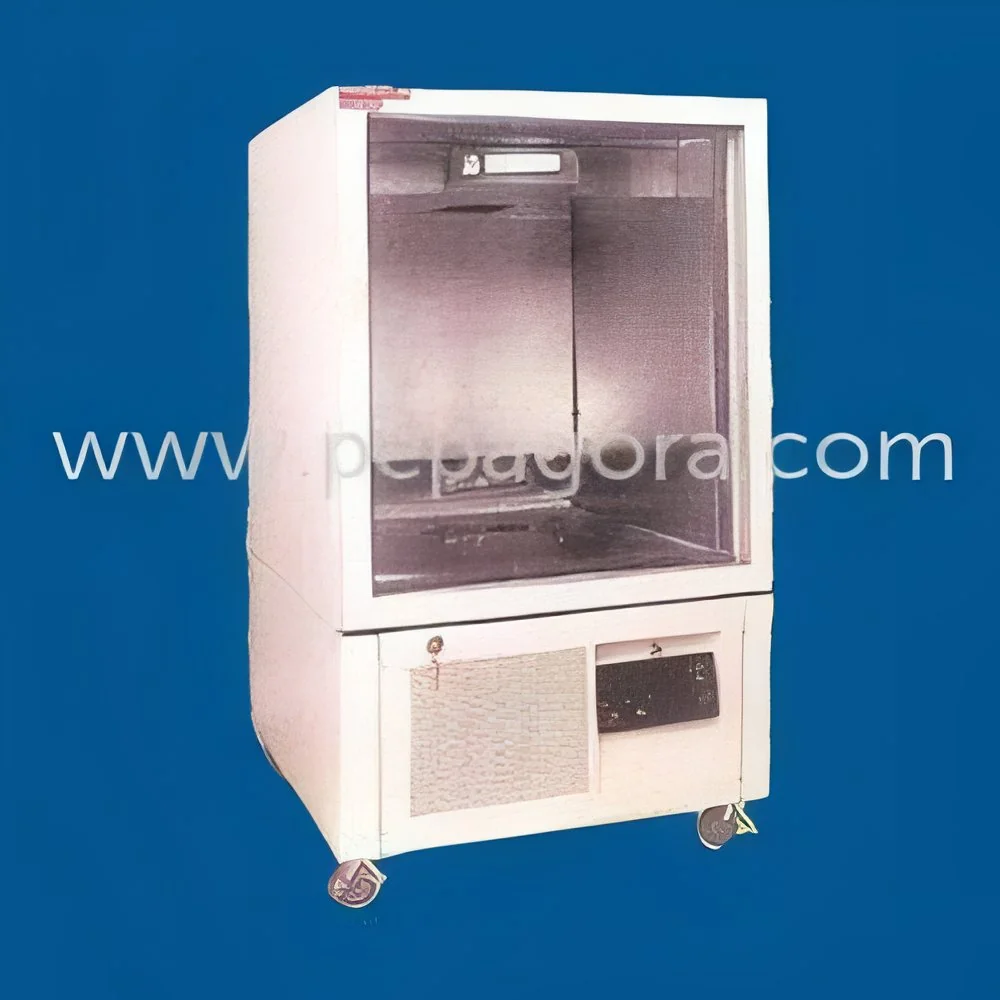
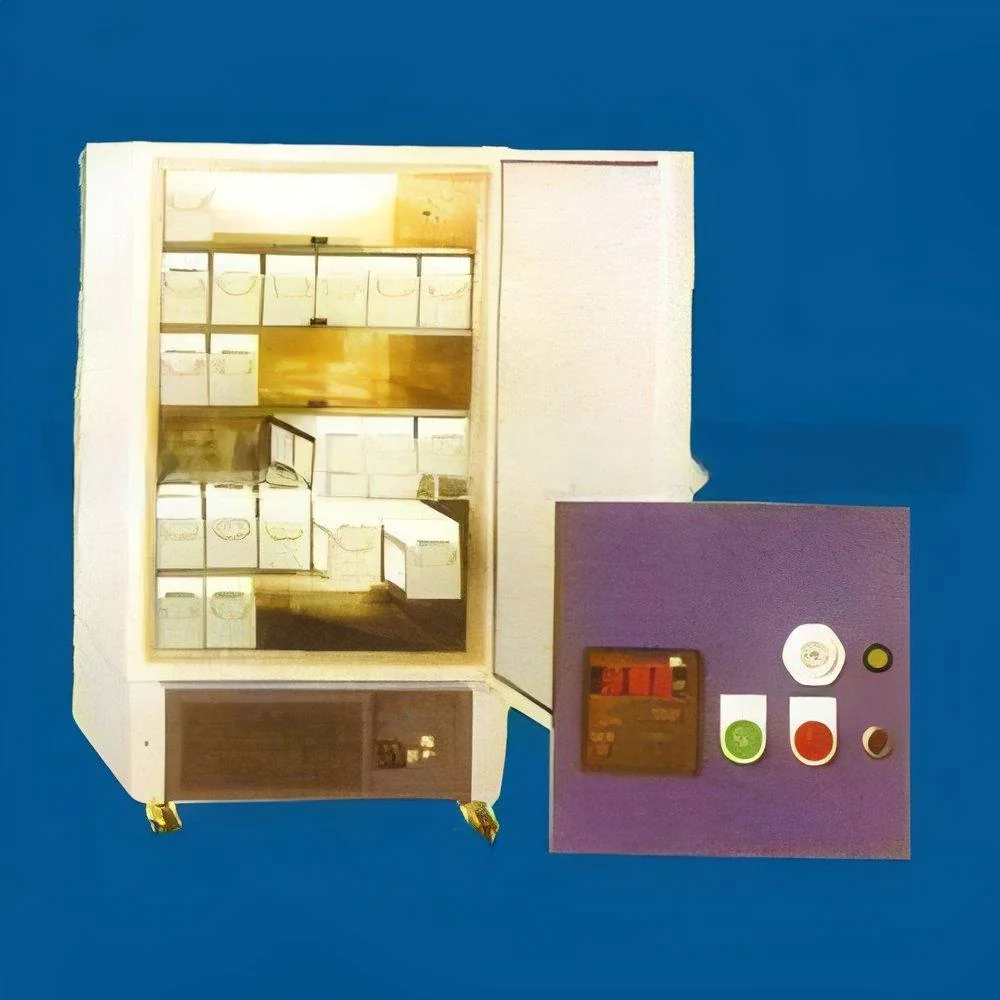
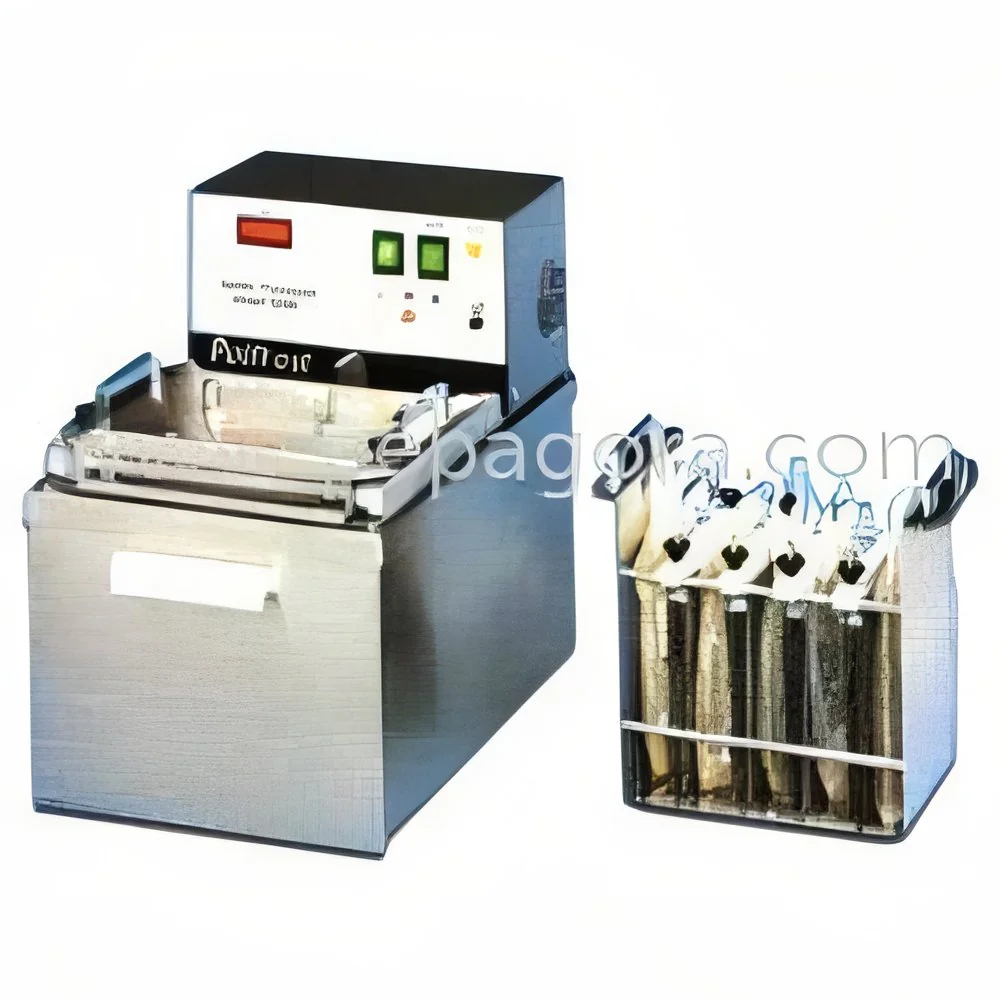
Our premium blood bank equipment represents the highest standard in medical device manufacturing, engineered specifically for reliable blood storage and collection operations. The comprehensive product range includes advanced blood bag tube sealers, precision weighing scales, and medical-grade refrigerators, all designed with healthcare professionals in mind. Each unit undergoes rigorous quality control and testing to ensure compliance with international medical device regulations, providing absolute confidence in critical environments where blood safety cannot be compromised. The robust construction and precision engineering guarantee consistent performance even in demanding medical settings.

This specialized equipment serves vital roles across multiple healthcare sectors including hospital blood banks, clinical laboratories, blood donation centers, and emergency medical facilities. It supports essential medical procedures ranging from routine blood collection drives to urgent transf...
Our premium blood bank equipment represents the highest standard in medical device manufacturing, engineered specifically for reliable blood storage and collection operations. The comprehensive product range includes advanced blood bag tube sealers, precision weighing scales, and medical-grade refrigerators, all designed with healthcare professionals in mind. Each unit undergoes rigorous quality control and testing to ensure compliance with international medical device regulations, providing absolute confidence in critical environments where blood safety cannot be compromised. The robust construction and precision engineering guarantee consistent performance even in demanding medical settings.

This specialized equipment serves vital roles across multiple healthcare sectors including hospital blood banks, clinical laboratories, blood donation centers, and emergency medical facilities. It supports essential medical procedures ranging from routine blood collection drives to urgent transfusion requirements, ensuring blood products remain at optimal storage conditions throughout their lifecycle. The medical industry, emergency response services, and clinical research institutions rely on our solutions to maintain blood integrity, minimize product waste, and enhance operational efficiency in high-stakes environments where precision and reliability are non-negotiable.

Healthcare facilities benefit significantly from our blood bank equipment through enhanced operational reliability, reduced clinical risks, and consistent compliance with health safety standards. The equipment's durable construction and precision components ensure long-term value by minimizing maintenance requirements and operational downtime. This focus on quality engineering and dependable performance builds lasting trust among medical professionals who require equipment that performs flawlessly during critical moments, ultimately supporting better patient outcomes through reliable blood management systems.

Key Features:
- ISO-certified manufacturing processes ensuring consistent quality and compliance
- Portable designs with rechargeable battery options for mobile operations
- Precision sealing technology for secure blood bag closure and integrity
- Medical-grade refrigeration maintaining optimal temperature control
- Robust construction designed for durability in demanding medical environments

Benefits:
- Enhanced blood safety through reliable storage and handling systems
- Improved operational efficiency with user-friendly equipment interfaces
- Reduced product waste through precise temperature and sealing control
- Long-term reliability minimizing maintenance and replacement costs
- Compliance with international medical standards and regulatory requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our blood bank equipment provides critical support for blood collection, storage, and management in healthcare facilities. These devices maintain blood integrity from donation to transfusion while meeting strict medical standards and regulatory requirements for safety and reliability across various medical environments and operational scenarios.
Hospitals, clinics, and blood donation centers depend on our equipment for daily operations including sealing blood bags, precise weighing, and temperature-controlled storage. The portable and rechargeable options enhance flexibility for mobile blood drives and emergency setups, ensuring consistent performance where reliable blood management is essential.
- Hospital blood banks requiring safe storage and organized access to blood units
- Blood donation camps needing portable and dependable collection equipment
- Emergency clinics and trauma centers for rapid blood transfusion readiness
- Laboratory facilities processing and handling blood samples for testing
- Medical research institutions studying blood preservation techniques
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Polfrost Aircon Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Blood Bank Equipment For Hospitals And Clinics
Premium blood bank equipment including ISO-certified blood bag sealers, precision scales, and medical refrigerators for reliable blood storage and collection in hospitals and clinics.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Polfrost Aircon Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer