IN
₹
Apparel & Fashion
Description
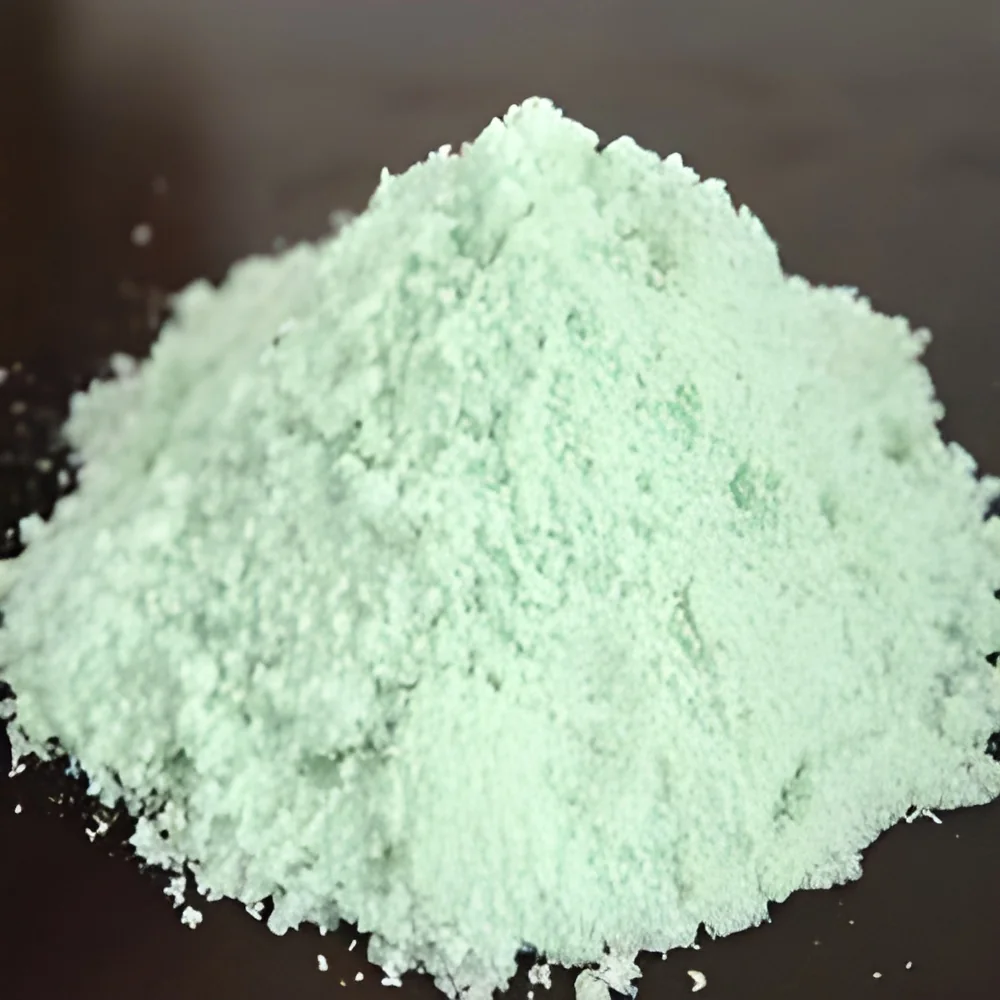
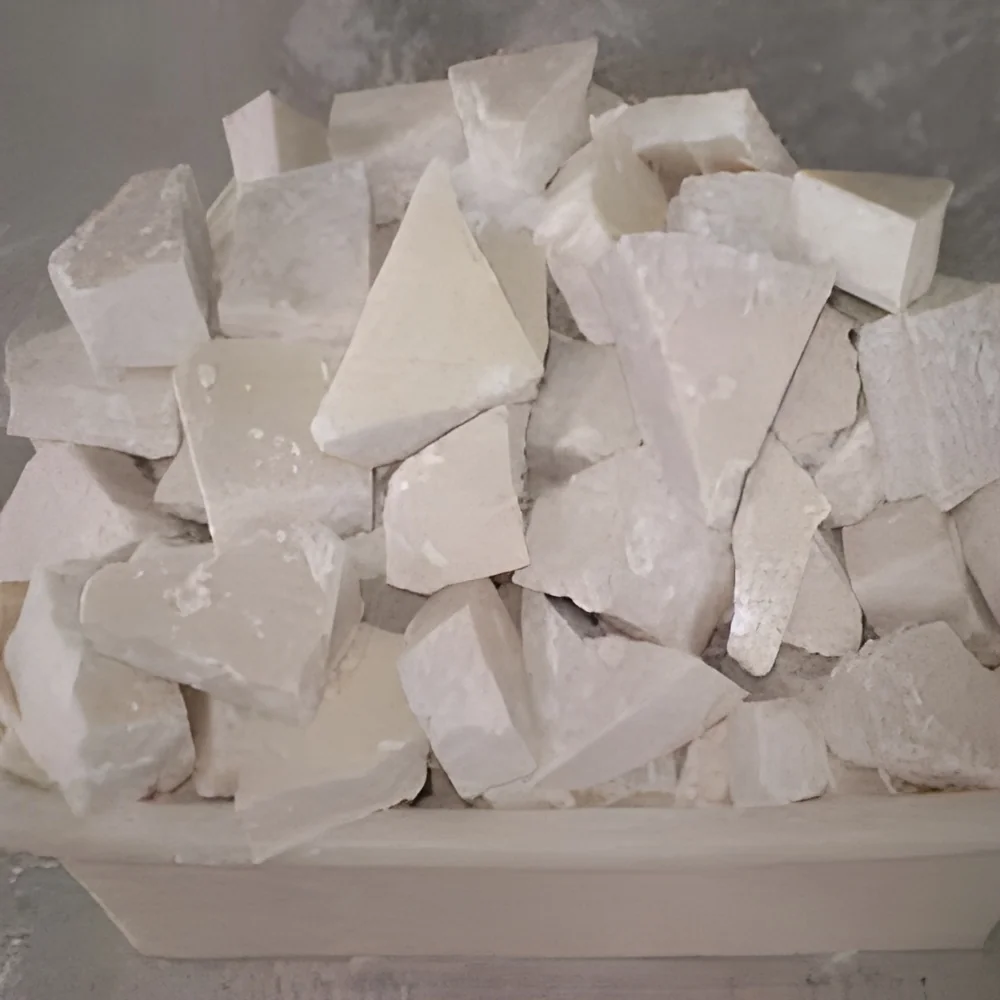
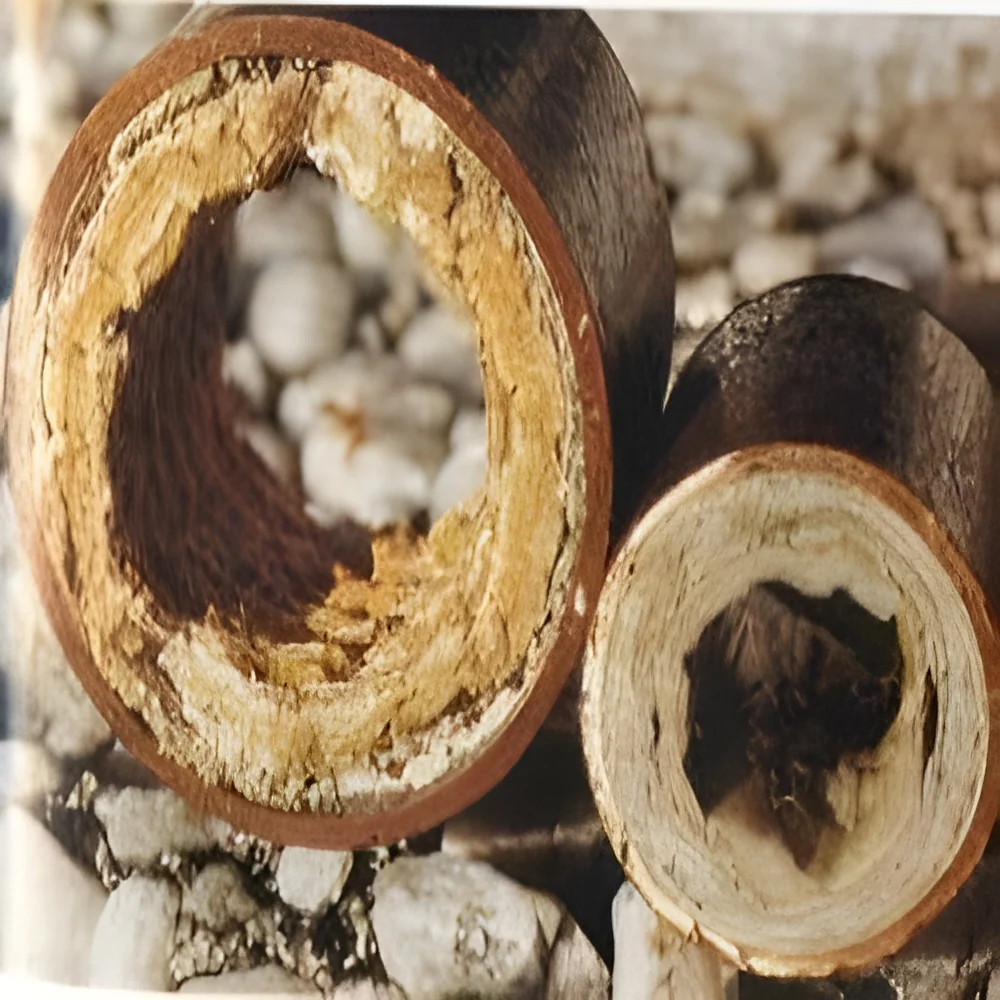
Our premium antiscalant chemicals represent advanced water treatment solutions specifically engineered to control and prevent all forms of scale formation, including challenging inorganic compounds, metal scales, and colloidal suspensions, even under high saturation conditions. These formulations maintain exceptional stability across extreme pH levels and temperature variations, ensuring reliable performance in the most demanding industrial environments where consistent water quality and system protection are critical for uninterrupted operations and production efficiency.

These antiscalants serve vital roles across multiple industries including power generation, manufacturing, food and beverage production, and municipal water treatment facilities. In power plants, they protect boiler systems from scale accumulation that reduces heat transfer efficiency. Manufacturing facilities rely on them to maintain cooling tower performance, while food processing plants utilize these chemicals to...
Our premium antiscalant chemicals represent advanced water treatment solutions specifically engineered to control and prevent all forms of scale formation, including challenging inorganic compounds, metal scales, and colloidal suspensions, even under high saturation conditions. These formulations maintain exceptional stability across extreme pH levels and temperature variations, ensuring reliable performance in the most demanding industrial environments where consistent water quality and system protection are critical for uninterrupted operations and production efficiency.

These antiscalants serve vital roles across multiple industries including power generation, manufacturing, food and beverage production, and municipal water treatment facilities. In power plants, they protect boiler systems from scale accumulation that reduces heat transfer efficiency. Manufacturing facilities rely on them to maintain cooling tower performance, while food processing plants utilize these chemicals to ensure production equipment operates at peak efficiency without contamination risks. The versatility of our formulations makes them suitable for both general industrial applications and sensitive processes requiring strict compliance with safety and purity standards.

For buyers seeking reliable scale prevention solutions, our antiscalants deliver unmatched value through unique quality assurance protocols and proven reliability. They significantly reduce operational costs by minimizing downtime, extending equipment lifespan, and lowering energy consumption. The proven reliability of these chemicals translates into predictable maintenance schedules and reduced emergency repairs, providing peace of mind for operations managers and plant engineers who depend on consistent water system performance for their production outcomes.

Key Features:
- Prevents scale formation in RO systems, boilers, and cooling towers
- Effective against inorganic, metal, and colloidal scales at high saturation
- Maintains stability in extreme pH levels and temperature variations
- High-quality industrial grade with consistent performance reliability
- Formulated for demanding industrial water treatment applications

Benefits:
- Extends equipment lifespan and reduces maintenance frequency
- Lowers energy consumption by maintaining optimal heat transfer
- Minimizes system downtime and production interruptions
- Reduces operational costs through efficient scale prevention
- Ensures consistent water quality and system performance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial antiscalant chemicals are essential for maintaining operational efficiency in water-intensive processes by protecting critical equipment from damaging scale buildup. They ensure consistent system performance, reduce unexpected downtime, and lower maintenance costs across various high-demand industrial environments where water purity and equipment longevity are non-negotiable priorities for continuous production.
These specialized chemicals are trusted across multiple sectors to prevent scale-related damage and avoid costly repairs. They are particularly vital in industries where even minor scale accumulation can lead to significant efficiency losses, increased energy consumption, and potential equipment failure, making them a fundamental component of proactive maintenance strategies.
- Reverse osmosis membrane protection in desalination and water purification plants
- Boiler water treatment systems in power generation and thermal plants
- Cooling water circuits in manufacturing facilities and HVAC systems
- Food and beverage processing water lines and production equipment
- Potable water treatment facilities and distribution systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aqua Phoenix Solutions, Maharashtra
 Maharashtra, India
Raw Materials & Chemicals•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Antiscalant Chemicals For RO Systems And Boilers
Premium industrial antiscalant chemicals prevent scale formation in RO systems, boilers, and cooling towers. Effective against inorganic, metal, and colloidal scales at high saturation, stable in extreme pH and temperatures for reliable water treatment.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aqua Phoenix Solutions
 Maharashtra, India
Raw Materials & ChemicalsManufacturer