IN
₹
Apparel & Fashion
Description
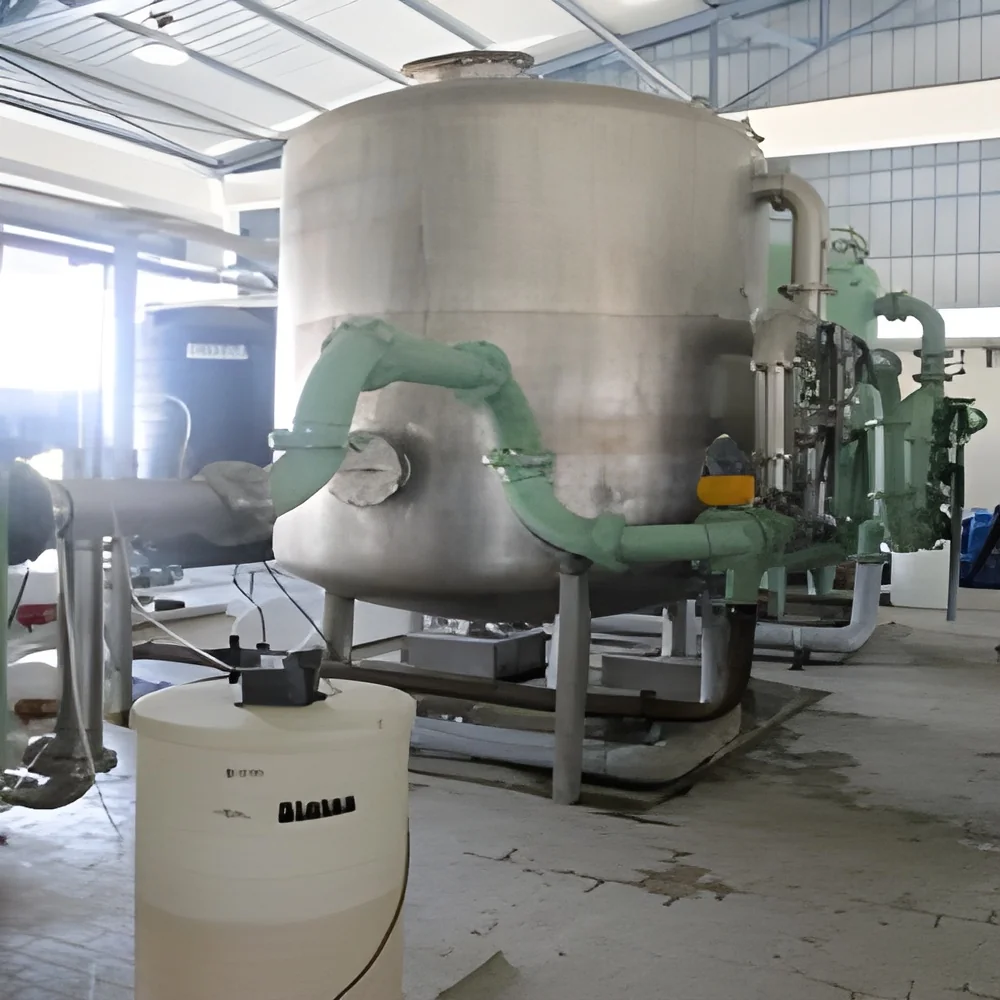
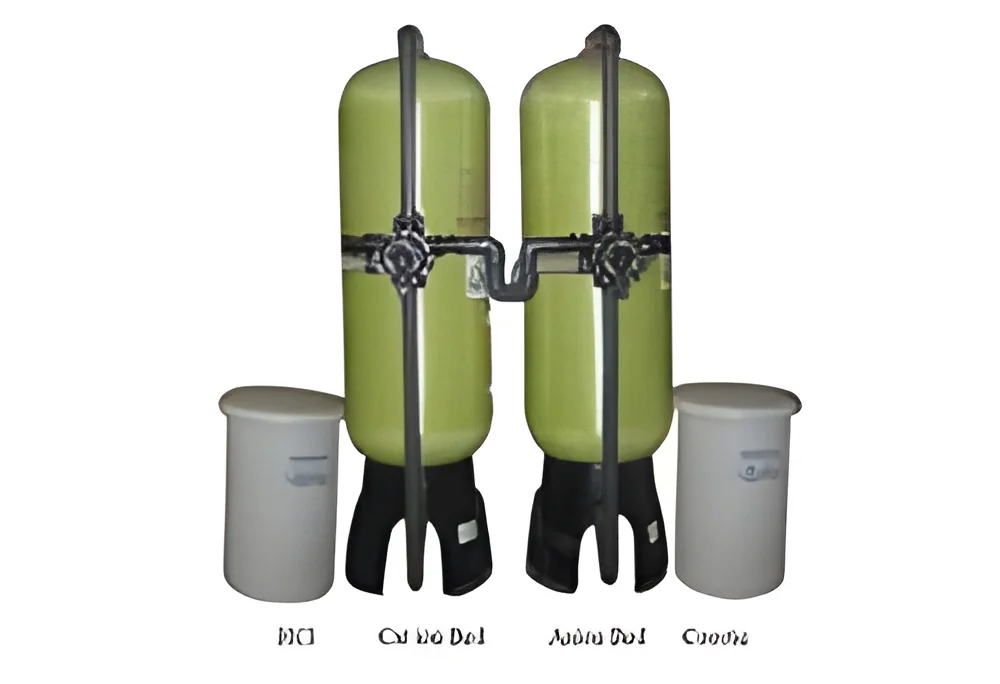
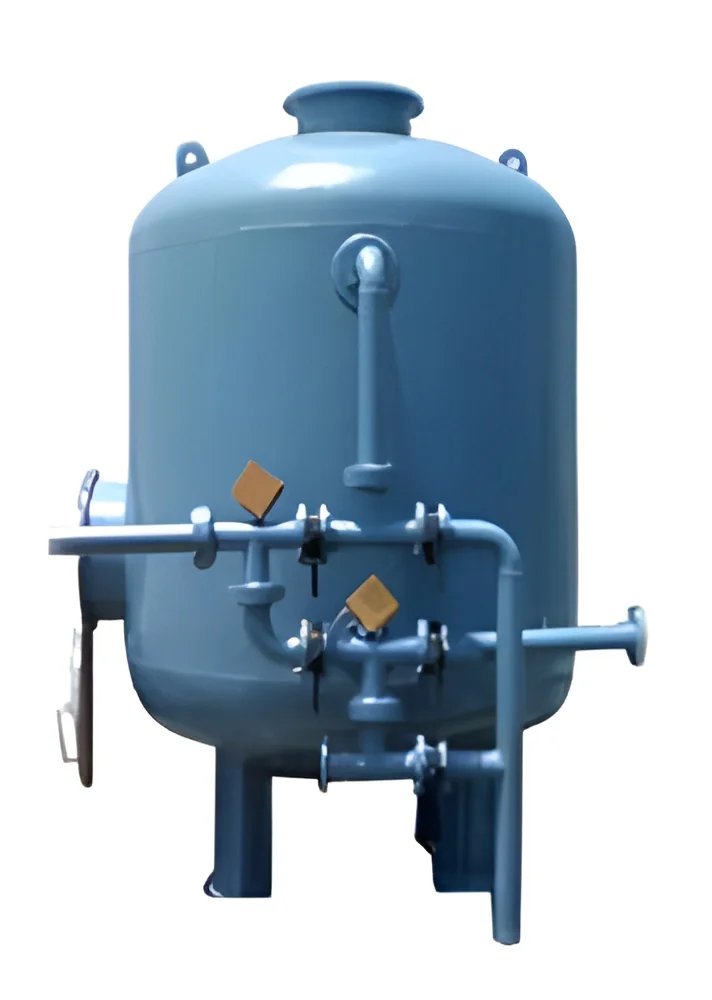
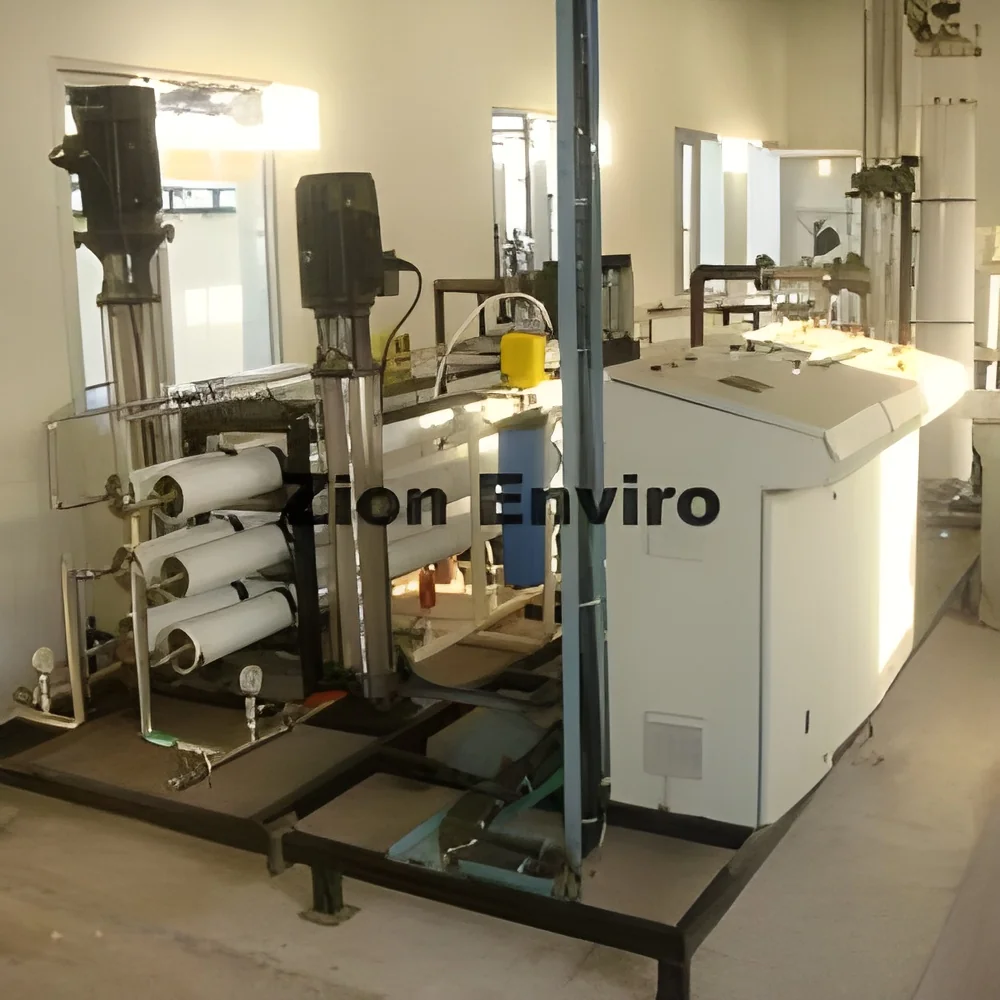
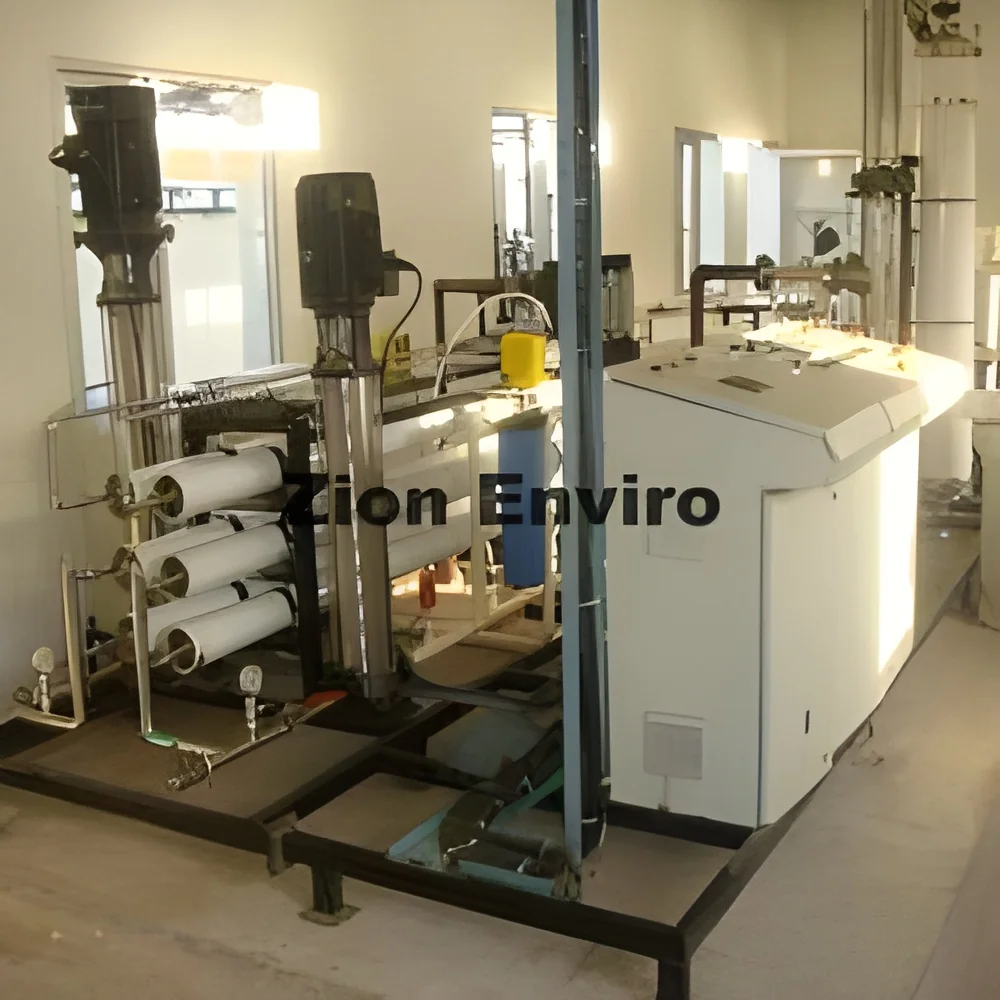
Hard water containing dissolved calcium and magnesium salts presents significant operational challenges for businesses by causing scale buildup and reducing overall efficiency. Our industrial water softener effectively removes these hardness ions through a proven ion-exchange process, transforming hard water into soft water that is ideal for commercial and industrial applications. This system is engineered for high-capacity usage, ensuring a consistent supply of treated water that prevents the negative effects of mineral deposits on equipment and processes. It serves as an essential solution for any facility seeking to protect its infrastructure and improve water-dependent operations without constant maintenance concerns, providing reliable water treatment that meets the demands of commercial and industrial environments.

Water softeners find extensive application across multiple industries where water quality is critical to operational success and compliance. In manufacturing environm...
Hard water containing dissolved calcium and magnesium salts presents significant operational challenges for businesses by causing scale buildup and reducing overall efficiency. Our industrial water softener effectively removes these hardness ions through a proven ion-exchange process, transforming hard water into soft water that is ideal for commercial and industrial applications. This system is engineered for high-capacity usage, ensuring a consistent supply of treated water that prevents the negative effects of mineral deposits on equipment and processes. It serves as an essential solution for any facility seeking to protect its infrastructure and improve water-dependent operations without constant maintenance concerns, providing reliable water treatment that meets the demands of commercial and industrial environments.

Water softeners find extensive application across multiple industries where water quality is critical to operational success and compliance. In manufacturing environments, they prevent scale accumulation in boilers and cooling systems, ensuring optimal energy efficiency and minimizing production downtime. The hospitality sector depends on them to protect plumbing infrastructure, enhance laundry services, and improve guest experiences through better water quality. Healthcare facilities utilize soft water to maintain sterile environments and protect sensitive medical equipment from mineral damage. Additionally, industries including food processing, textiles, and pharmaceuticals rely on softened water to maintain product consistency, meet regulatory standards, and prevent contamination from scale particles that could compromise product quality and safety.

Investing in our industrial water softener delivers substantial business value by significantly reducing maintenance expenses and extending the operational life of costly equipment. Our systems are constructed for maximum reliability, featuring robust components that ensure continuous operation even under demanding conditions and high-volume usage. The proven technology provides consistent performance that translates into reduced operational risks and long-term cost savings, making our water softeners an intelligent choice for buyers who prioritize durability and efficiency in their water treatment investments. The reliable performance ensures that your operations continue uninterrupted while protecting your valuable equipment from the damaging effects of hard water minerals.

Key Features:
- Ion-exchange resin technology for effective removal of calcium and magnesium ions
- High-capacity design suitable for commercial and industrial water volumes
- Durable construction with corrosion-resistant materials for long service life
- Automated regeneration system for consistent performance with minimal manual intervention
- Robust components engineered for continuous operation under high-demand conditions

Benefits:
- Prevents scale buildup in pipes and equipment, reducing maintenance requirements
- Extends the lifespan of water-using equipment and appliances significantly
- Improves energy efficiency by maintaining heat transfer effectiveness
- Reduces operational costs through decreased energy and maintenance expenses
- Ensures consistent water quality for various industrial processes and applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial water softeners are essential for facilities where water quality directly impacts operations and equipment performance. They effectively prevent scale formation in boilers, cooling towers, and piping systems, which significantly reduces maintenance costs and energy consumption. This makes them a critical investment for manufacturing plants, hotels, hospitals, and food processing units that require consistent, high-quality water for their daily operations and long-term equipment protection.
Beyond heavy industrial use, these water treatment systems are vital for commercial laundries, textile manufacturing, and pharmaceutical production where water hardness can directly affect product quality and process efficiency. They also protect water-using appliances and equipment in large facilities, extending their operational lifespan and ensuring optimal performance throughout their service life. Businesses choose our water softeners for their proven reliability and ability to handle high-volume water treatment needs seamlessly across various applications.
- Prevents scaling in industrial boilers and heat exchangers, maintaining energy efficiency and reducing fuel costs
- Protects plumbing systems in large commercial buildings like hotels and hospitals from corrosion and blockages
- Improves lathering and cleaning efficiency in commercial laundries and car wash facilities
- Ensures consistent water quality for food and beverage production processes and product consistency
- Extends the lifespan of water-using equipment in manufacturing plants, reducing replacement costs
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Zion Enviro Systems Pvt Ltd, Tamil Nadu
 Tamil Nadu, India
Construction•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Water Softener For Manufacturing And Commercial Facilities
Industrial water softener removes calcium and magnesium salts from hard water, preventing scale buildup and improving efficiency for manufacturing, hospitality, and commercial facilities with reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Zion Enviro Systems Pvt Ltd
 Tamil Nadu, India
ConstructionImporter / Exporter