IN
₹
Apparel & Fashion
Description
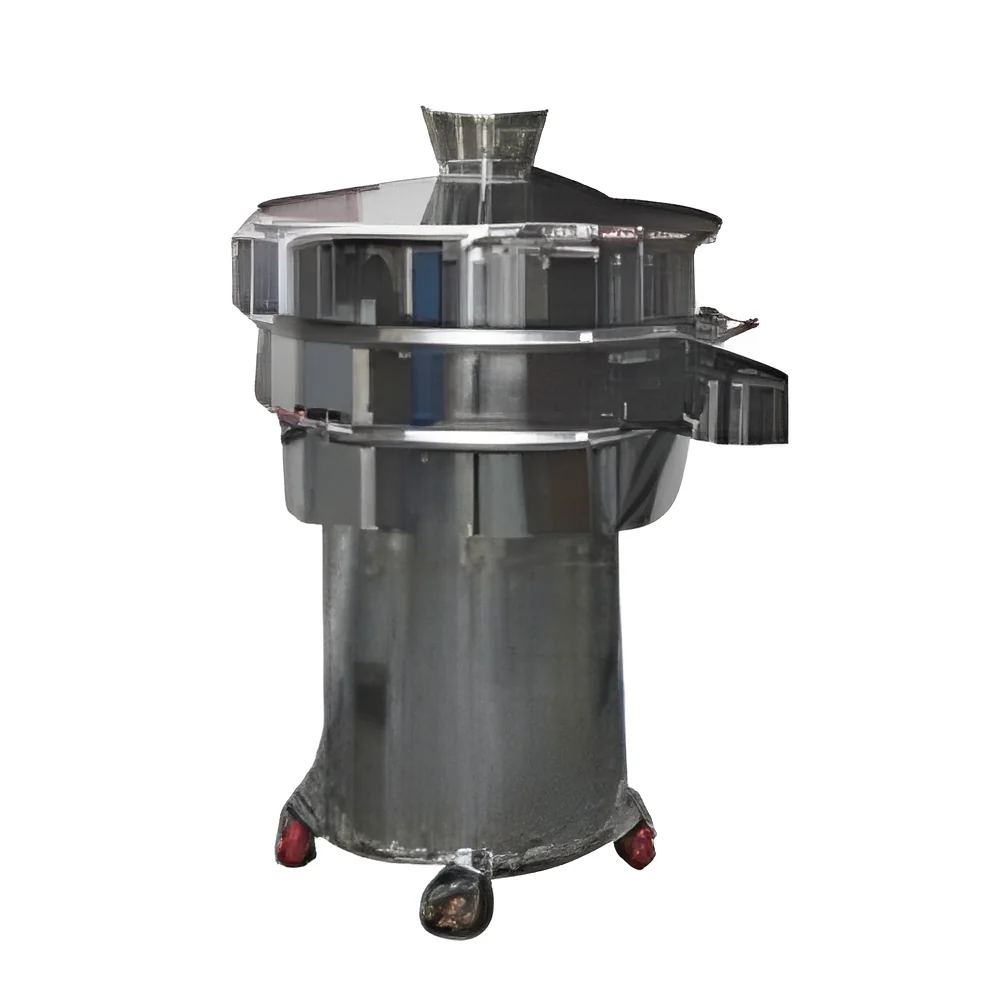
The Industrial Vibro Sifter represents advanced sieving technology designed for precise particle separation in demanding industrial environments. Utilizing efficient vibratory motion, this machine ensures accurate grading of materials from fine powders to granular substances. Engineered for reliability and consistent performance, it maintains optimal sieving efficiency while handling various material types. The machine's construction focuses on durability and operational stability, making it suitable for continuous production requirements across different industry sectors. Its design incorporates precision engineering to deliver uniform results batch after batch, supporting quality assurance protocols in manufacturing processes.

In pharmaceutical manufacturing, these sifters are indispensable for achieving uniform particle distribution in active pharmaceutical ingredients and excipients. Food processing facilities rely on them for ensuring ingredient purity by removing foreign particl...
The Industrial Vibro Sifter represents advanced sieving technology designed for precise particle separation in demanding industrial environments. Utilizing efficient vibratory motion, this machine ensures accurate grading of materials from fine powders to granular substances. Engineered for reliability and consistent performance, it maintains optimal sieving efficiency while handling various material types. The machine's construction focuses on durability and operational stability, making it suitable for continuous production requirements across different industry sectors. Its design incorporates precision engineering to deliver uniform results batch after batch, supporting quality assurance protocols in manufacturing processes.

In pharmaceutical manufacturing, these sifters are indispensable for achieving uniform particle distribution in active pharmaceutical ingredients and excipients. Food processing facilities rely on them for ensuring ingredient purity by removing foreign particles and achieving consistent texture in final products. Chemical plants utilize vibro sifters for precise grading of compounds, pigments, and specialty chemicals where particle size directly impacts product performance. The mining industry employs these machines for mineral separation and abrasive material classification, while recycling operations benefit from efficient material sorting capabilities. Each industry application demands specific performance characteristics that these sifters deliver through their adaptable design and reliable operation.

The business value of Industrial Vibro Sifters extends beyond basic sieving functions to encompass significant operational advantages. These machines enhance production efficiency by reducing manual sorting requirements and minimizing material waste through precise separation. Their reliable performance translates to reduced downtime and lower maintenance costs, contributing to improved overall equipment effectiveness. The consistent output quality supports compliance with industry standards and customer specifications, strengthening market competitiveness. Long-term operational reliability ensures predictable performance that supports production planning and quality management systems. This combination of efficiency, reliability, and quality assurance makes vibro sifters a strategic investment for businesses focused on operational excellence and product quality.

Key Features:
- High-efficiency vibratory sieving system for precise particle separation
- Robust construction with durable components for long service life
- Multiple mesh size options for versatile application requirements
- Easy-access design for simplified maintenance and cleaning procedures
- Stable operation with minimal vibration transmission to supporting structures

Benefits:
- Consistent particle size distribution improves final product quality
- Reduced operational downtime through reliable performance and easy maintenance
- Versatile application across multiple material types and industry sectors
- Enhanced production efficiency with continuous high-capacity operation
- Long-term cost savings through durable construction and minimal maintenance requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial Vibro Sifters provide precise particle separation for materials ranging from fine powders to coarse granules. These machines maintain consistent quality control by efficiently removing impurities and ensuring uniform particle size distribution across various production processes. Their robust design handles continuous operation while minimizing maintenance requirements.
The versatility of these sifters makes them essential across multiple sectors where material purity and precise grading are critical. From food safety compliance to pharmaceutical quality standards, these machines deliver reliable performance in demanding environments. Their efficient operation supports high-volume production while maintaining strict quality parameters throughout the sieving process.
- Pharmaceutical powder sieving for uniform particle size in tablet and capsule production
- Food ingredient processing to remove contaminants from flour, sugar, and spices
- Chemical compound grading for consistent pigment and resin quality control
- Mineral and abrasive material separation in mining and metalworking industries
- Recycling operations for efficient material sorting and waste management processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anmol Pharma Equipments, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Vibro Sifter for Precise Sieving in Food Pharma Chemicals
Industrial Vibro Sifter delivers precise sieving and grading for food, pharmaceutical, and chemical industries. This reliable machine ensures high-quality particle separation with consistent performance for diverse industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anmol Pharma Equipments
 Maharashtra, India
Industrial Equipment & MachineryManufacturer