IN
₹
Apparel & Fashion
Description
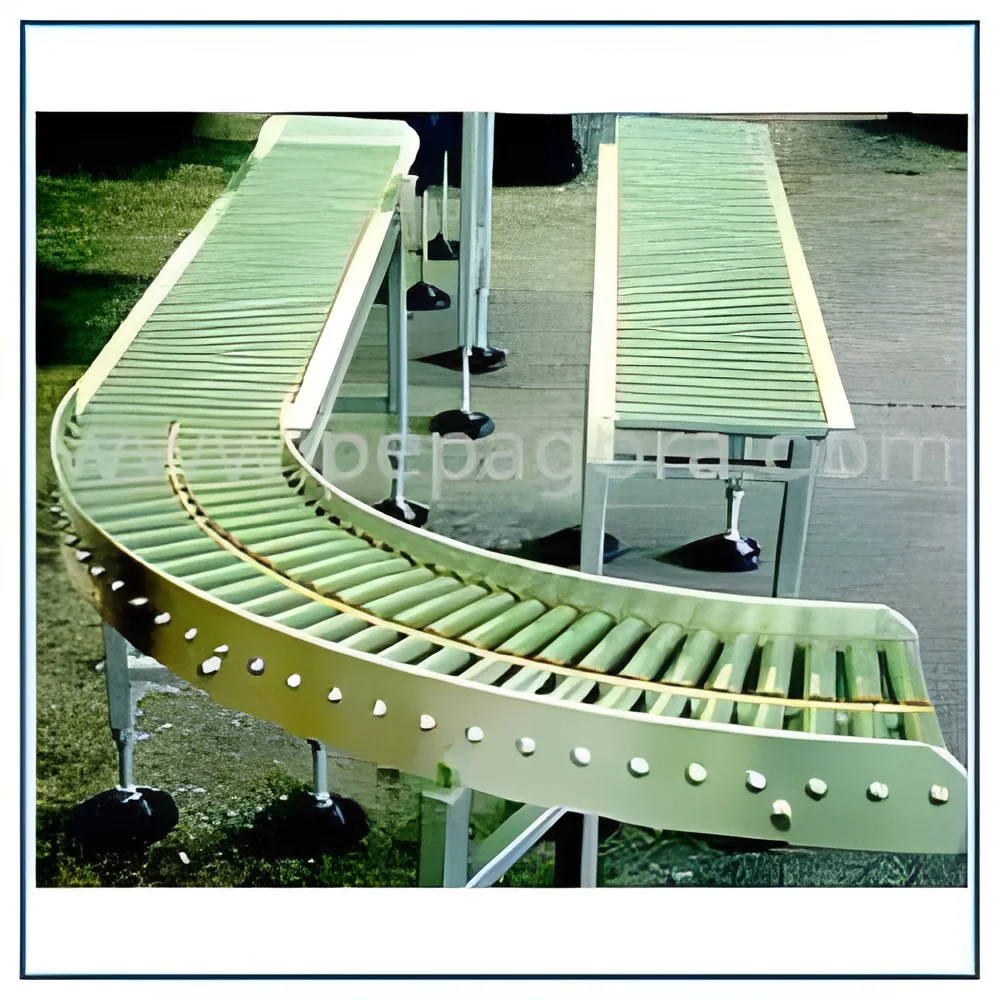
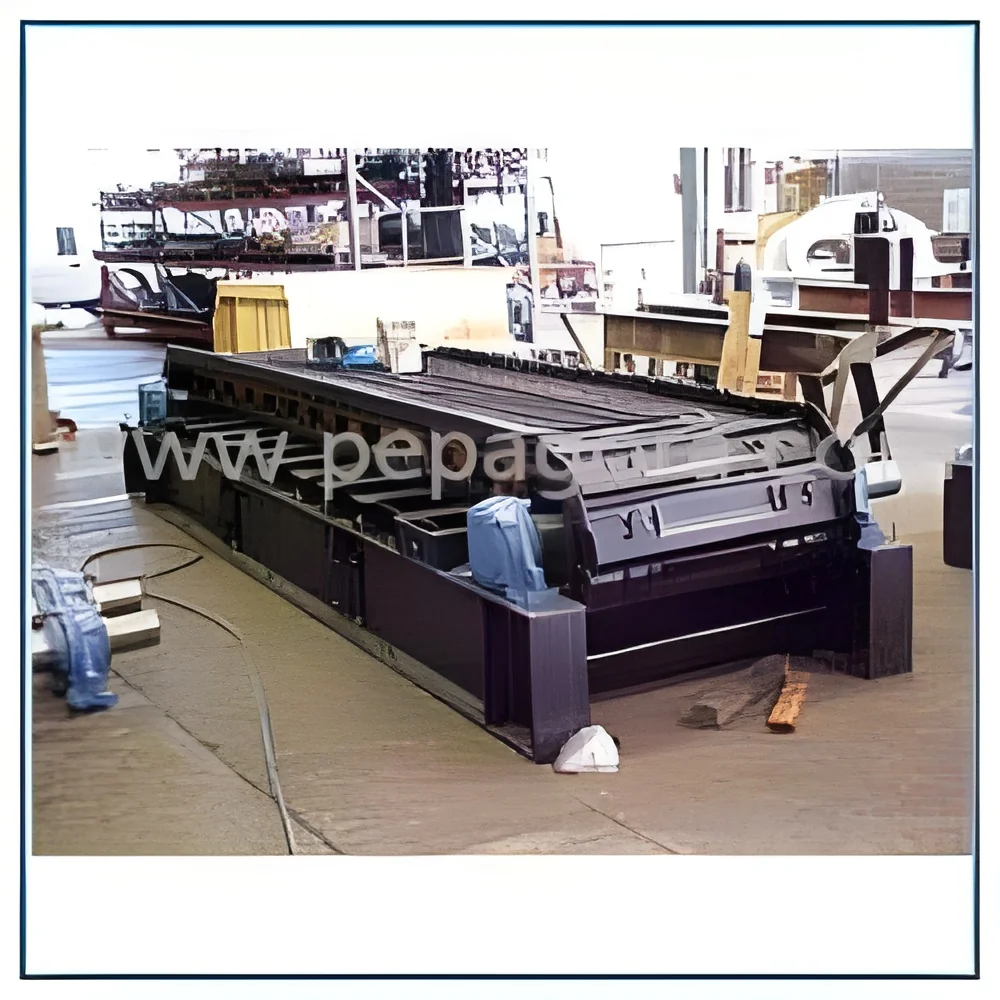
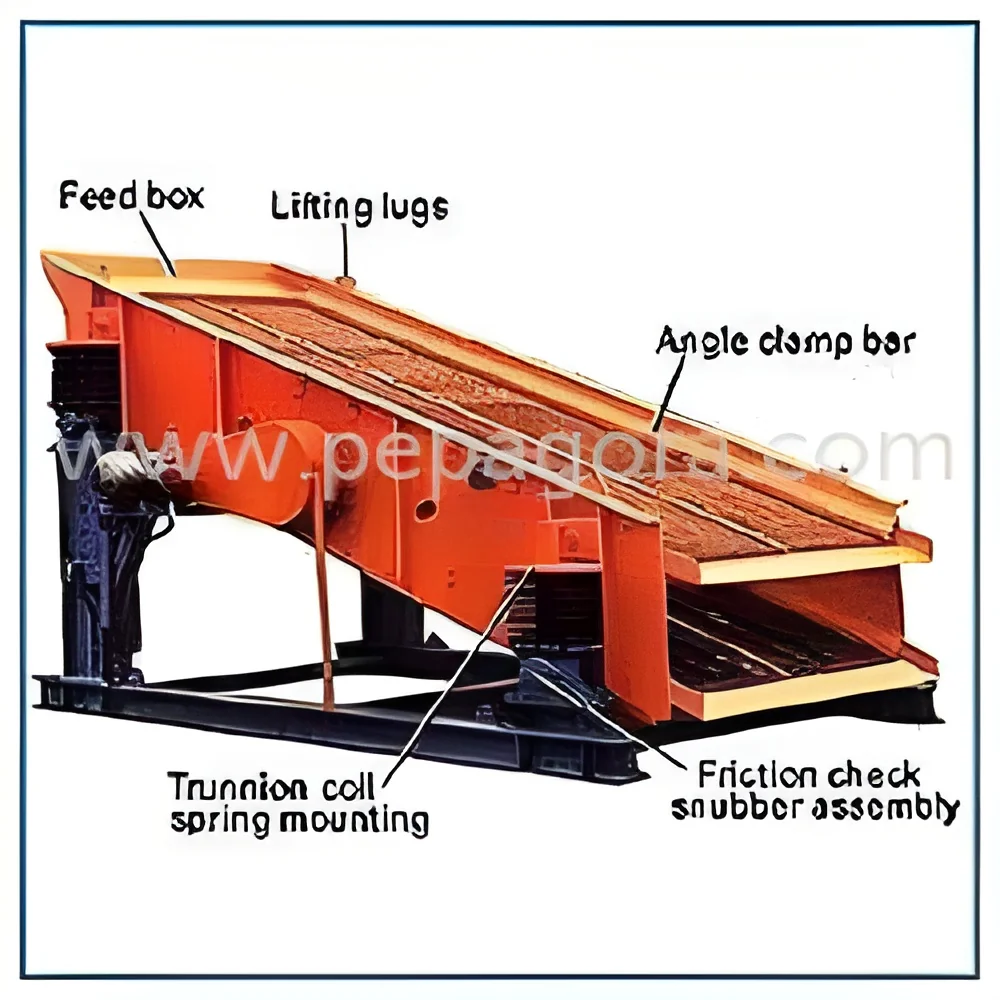
Our industrial vibrating screens are precision-engineered for rigorous grading and sieving, delivering unmatched performance in high-capacity material processing. Built with a focus on durability and reliability, they feature robust construction designed for continuous operation in tough industrial settings. These screens provide exceptional accuracy in particle separation, ensuring your output meets strict quality specifications. Their design prioritizes operational efficiency, making them a cornerstone for any serious material handling and processing operation that values consistency and throughput.

These versatile screens are indispensable across a broad spectrum of industries. In mining and quarrying, they are critical for efficiently sorting and grading ores, minerals, and aggregates. The construction sector relies on them for precise classification of sand, gravel, and crushed stone. Agriculture and food processing plants utilize these screens for cleaning and sizing grains, see...
Our industrial vibrating screens are precision-engineered for rigorous grading and sieving, delivering unmatched performance in high-capacity material processing. Built with a focus on durability and reliability, they feature robust construction designed for continuous operation in tough industrial settings. These screens provide exceptional accuracy in particle separation, ensuring your output meets strict quality specifications. Their design prioritizes operational efficiency, making them a cornerstone for any serious material handling and processing operation that values consistency and throughput.

These versatile screens are indispensable across a broad spectrum of industries. In mining and quarrying, they are critical for efficiently sorting and grading ores, minerals, and aggregates. The construction sector relies on them for precise classification of sand, gravel, and crushed stone. Agriculture and food processing plants utilize these screens for cleaning and sizing grains, seeds, and raw ingredients. Furthermore, they play a vital role in recycling facilities by separating materials and in chemical production for processing powders and slurries, proving their utility in virtually any operation requiring size-based material separation.

The business value of investing in our vibrating screens is clear: enhanced productivity and significant operational cost savings. Their reliable performance and high screening capacity minimize costly downtime, while their durable build reduces long-term maintenance and replacement expenses. This reliability ensures a consistent, high-quality output, directly supporting your ability to meet production targets and maintain a competitive edge. By integrating seamlessly into your process, these screens represent a smart, long-term investment in operational efficiency, scalability, and sustained growth for your business.

Key Features:
- Robust, heavy-duty construction ensures long-term durability and resistance to wear.
- High-capacity design enables efficient processing of large material volumes.
- Available in versatile single, double, and multi-deck configurations for various grading needs.
- Precision-engineered screen decks and vibration mechanisms for accurate particle separation.
- Designed for easy integration and low-maintenance operation in industrial settings.

Benefits:
- Maximizes productivity and throughput with efficient, high-volume screening.
- Reduces operational costs through reliable performance and minimal downtime.
- Delivers consistent, high-quality output by ensuring precise grading and sieving.
- Offers long-term value with a durable build that lowers total cost of ownership.
- Enhances process flexibility and can be tailored to fit specific material handling requirements.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial vibrating screens are engineered for high-volume, precise particle separation, ensuring consistent output in the most demanding operational environments. Their robust construction guarantees durability and continuous performance, handling heavy loads with minimal downtime to keep your processing line running efficiently and cost-effectively.
Available in single, double, or triple deck configurations, these screens offer the adaptability needed for specific grading tasks. They integrate seamlessly into existing systems, enhancing workflow and boosting overall productivity for operations that require reliable and accurate size classification of bulk materials.
- Separating and grading crushed stone, sand, and gravel in mining and construction aggregate production.
- Sizing and classifying ores and minerals in mineral beneficiation and processing plants.
- Cleaning, sorting, and sizing grains, seeds, and pulses in agricultural and food processing facilities.
- Sorting recyclable materials like plastics, metals, and glass by size in waste management and recycling operations.
- Dewatering, filtering, and classifying slurries and powders in chemical, pharmaceutical, and ceramic manufacturing.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Merger System, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Vibrating Screens For Precise Grading And Sieving
Industrial Vibrating Screens from our premium range deliver precise grading and sieving for high-capacity material processing. Engineered for reliability and built robustly to meet diverse operational demands across mining, construction, and food processing industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Merger System
 West Bengal, India
Industrial Equipment & MachineryManufacturer