IN
₹
Apparel & Fashion
Description
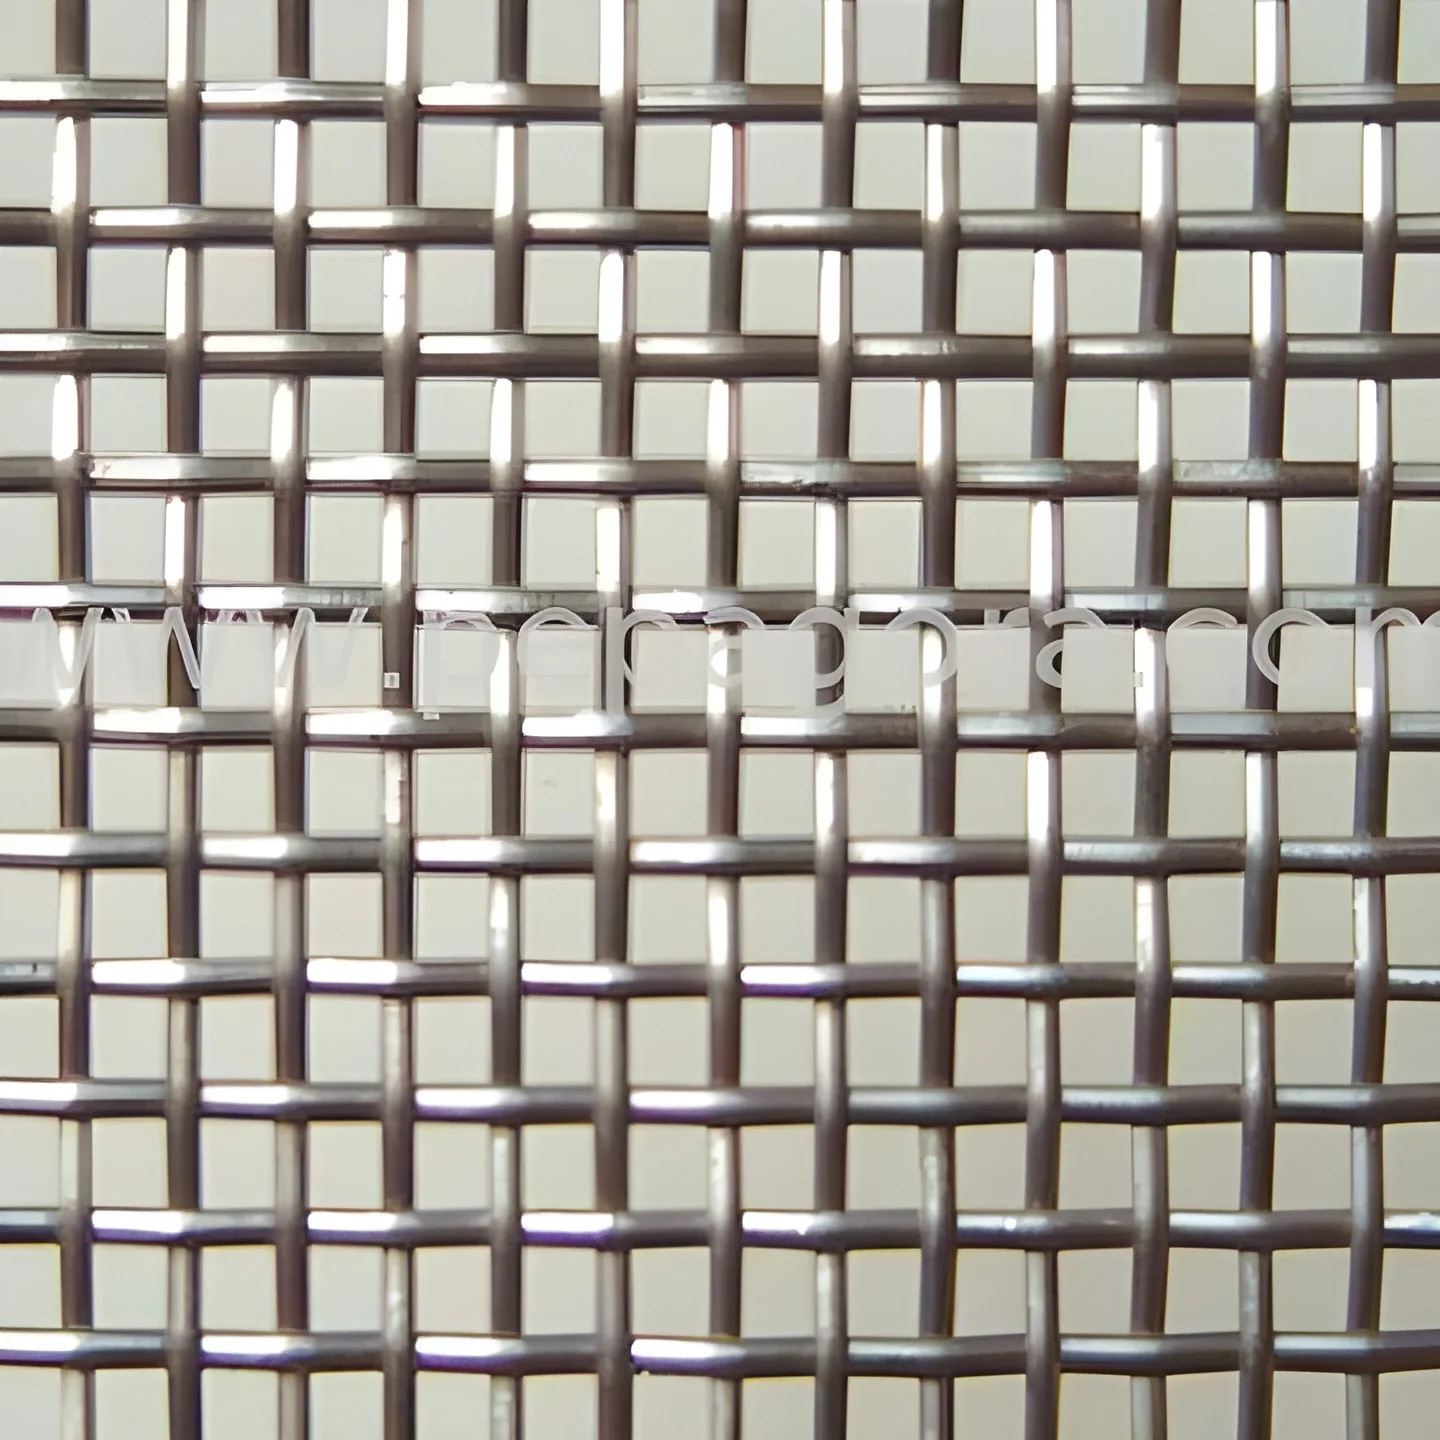
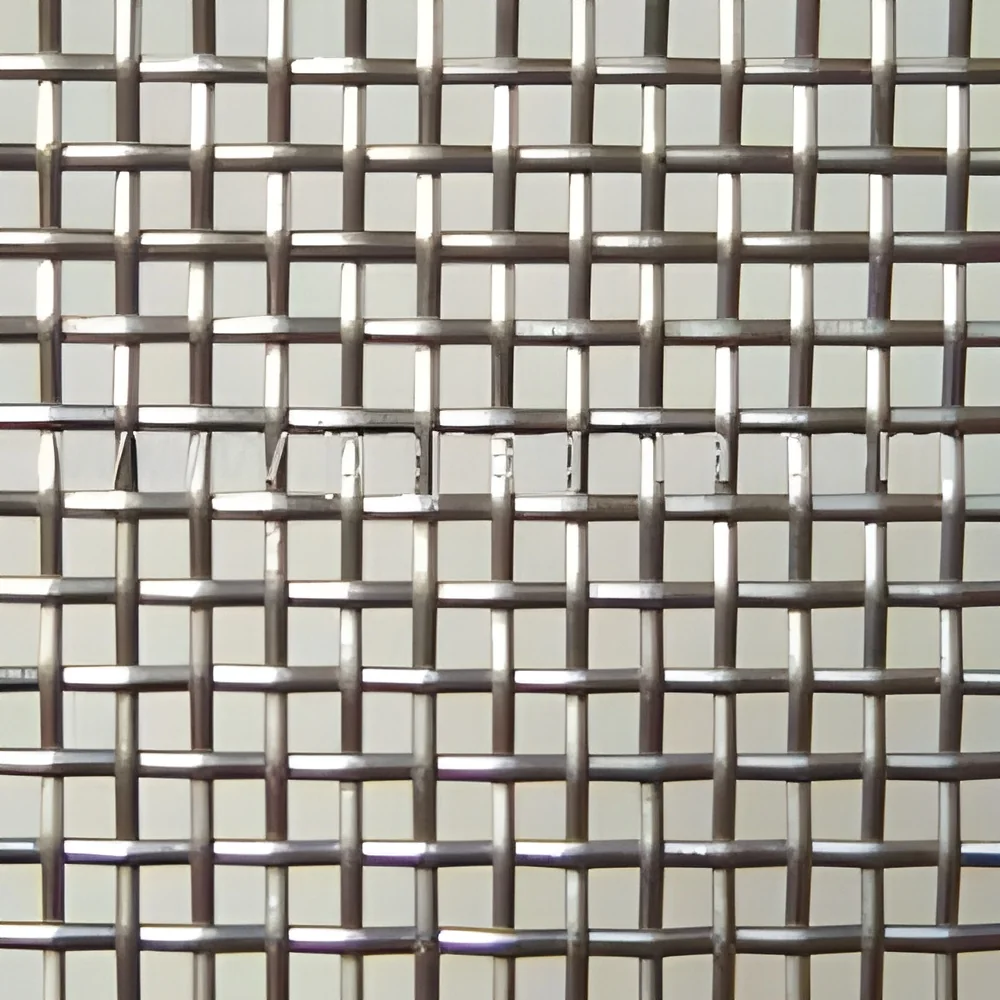
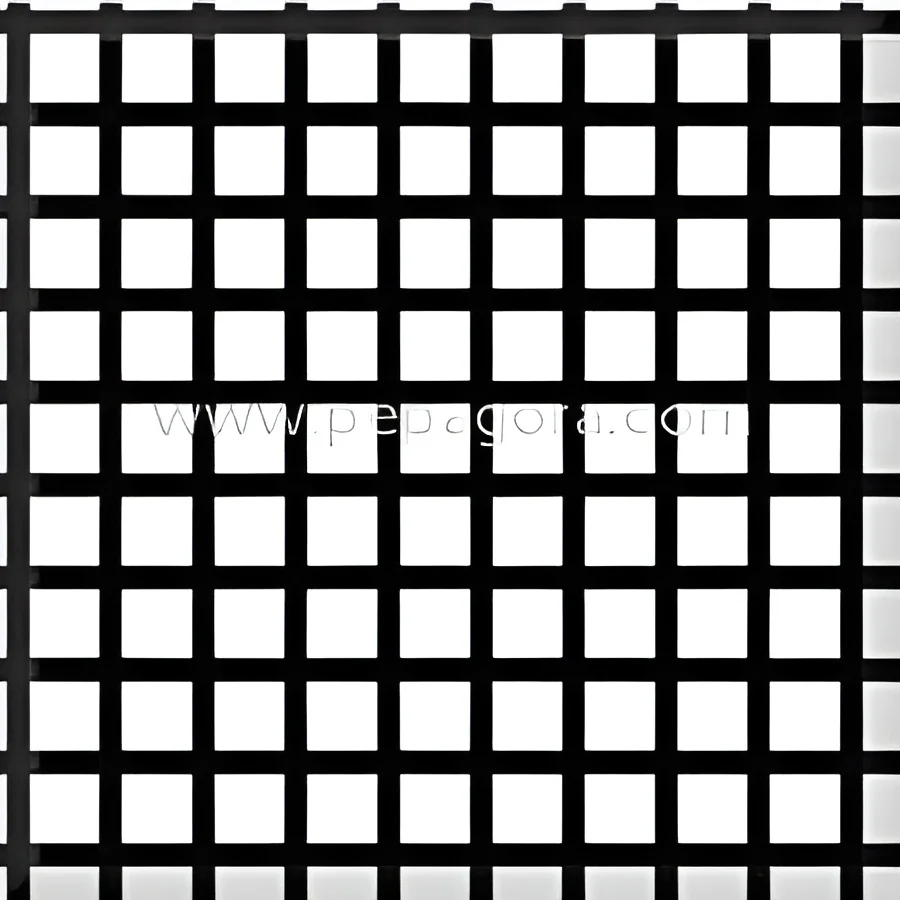
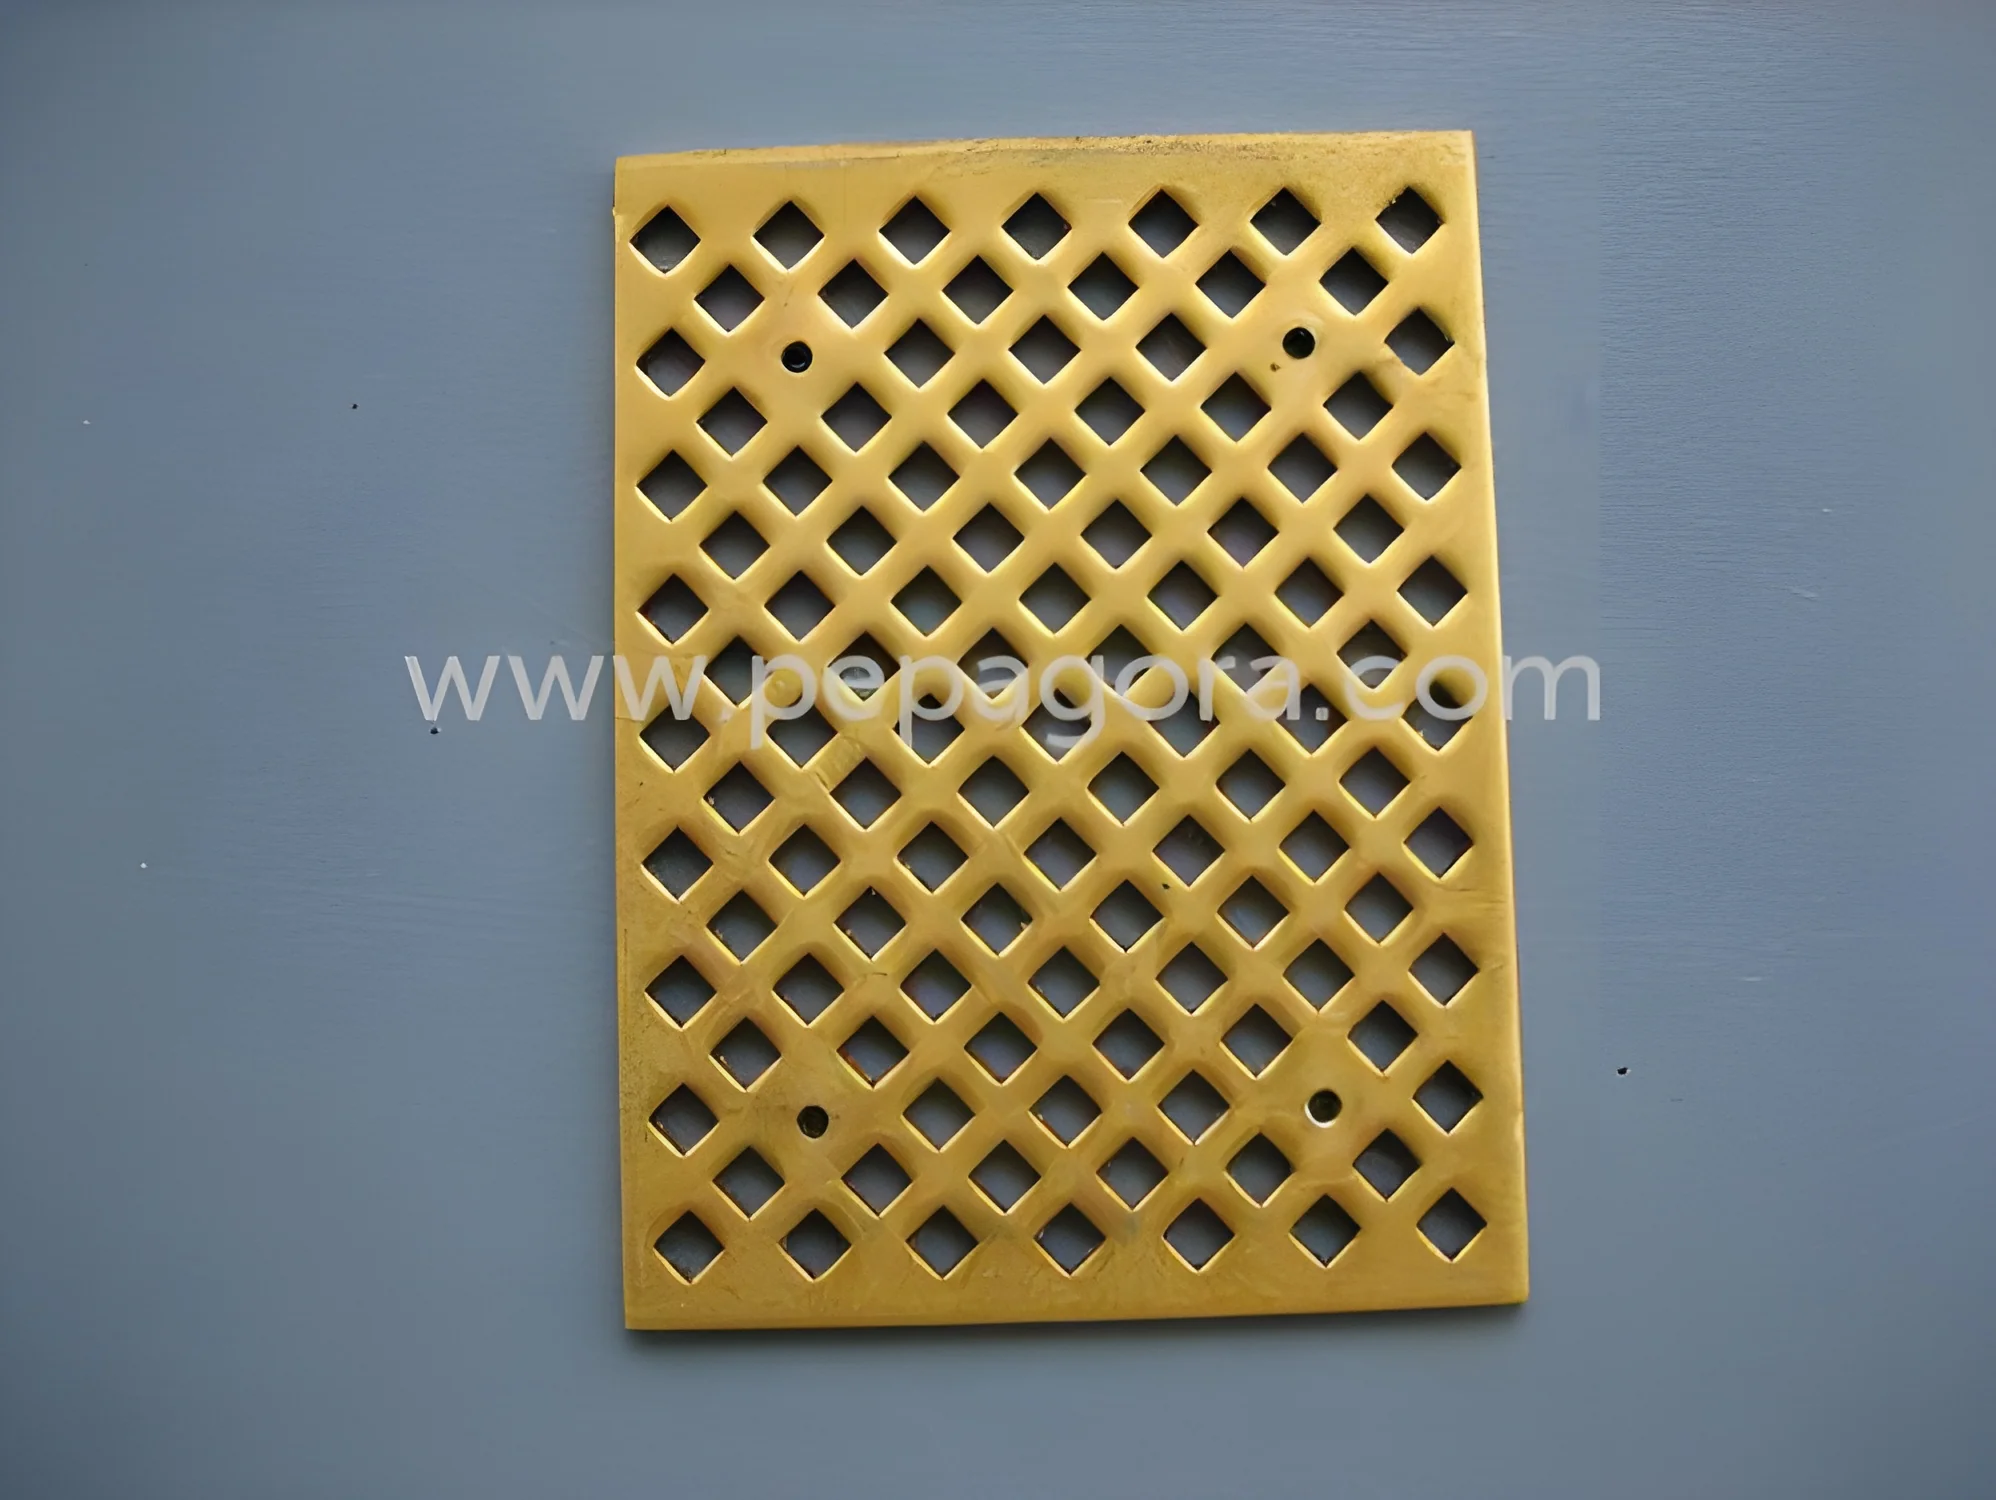
Our industrial square vibrating screens represent advanced material separation technology designed for operations demanding uncompromising performance and durability. These screens feature perforated galvanized surfaces that provide exceptional corrosion resistance and longevity, even in the most challenging industrial environments. Constructed through precision forging techniques, these strong and sturdy screens deliver superior efficiency with minimal maintenance requirements, making them the optimal choice for operations where consistent performance and maximum uptime are critical success factors.

These versatile vibrating screens serve essential functions across multiple heavy industries, particularly in mining, construction aggregates, and recycling sectors. Mining operations utilize them for efficient separation and classification of various minerals and ores by particle size, ensuring optimal downstream processing efficiency. Construction companies rely on these screens for pre...
Our industrial square vibrating screens represent advanced material separation technology designed for operations demanding uncompromising performance and durability. These screens feature perforated galvanized surfaces that provide exceptional corrosion resistance and longevity, even in the most challenging industrial environments. Constructed through precision forging techniques, these strong and sturdy screens deliver superior efficiency with minimal maintenance requirements, making them the optimal choice for operations where consistent performance and maximum uptime are critical success factors.

These versatile vibrating screens serve essential functions across multiple heavy industries, particularly in mining, construction aggregates, and recycling sectors. Mining operations utilize them for efficient separation and classification of various minerals and ores by particle size, ensuring optimal downstream processing efficiency. Construction companies rely on these screens for precise grading of aggregates to meet concrete and asphalt production specifications. Recycling facilities employ them for effective material sorting, while chemical and pharmaceutical manufacturers depend on their accurate particle size distribution capabilities for production quality control. The agricultural and food processing sectors also benefit from these screens for sorting grains and other bulk materials with precision.

The operational value of these vibrating screens extends beyond their primary separation function to deliver significant business advantages. Their robust construction and galvanized surface treatment translate to reduced maintenance costs and extended service intervals, providing superior total cost of ownership. The reliability engineered into every component ensures consistent performance that safeguards production output and maintains quality standards. These screens represent not just equipment but a strategic investment in operational efficiency, productivity enhancement, and long-term profitability. Their durable design minimizes downtime while maximizing separation accuracy across diverse industrial applications.

Key Features:
- Square shape design with precision perforations for optimal material flow
- Galvanized surface treatment providing enhanced corrosion resistance
- Customizable dimensions including length, size, and thickness specifications
- Forging processed construction ensuring exceptional strength and durability
- Engineered for maximum efficiency with minimal maintenance requirements

Benefits:
- Enhanced material separation accuracy for improved product quality
- Reduced maintenance costs and extended equipment service life
- Consistent performance reliability across diverse industrial applications
- Corrosion-resistant construction suitable for harsh operating environments
- Custom sizing options for seamless integration into existing production systems
Specifications
| Key Attributes | |
|---|---|
| Type | Vibrating Screen |
| Shape | Square |
| Technique | Perforated |
| Surface | Galvanized |
| Price | Negotiable |
| Quality | Best |
| Processed Type | Forging |
| Construction | Strong And Sturdy |
| Efficiency | More |
| Maintenance | Minimum |
| Length | As per customer requirement |
| Size | As per customer requirement |
| Thickness | As per customer requirement |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our square vibrating screens deliver high-performance material separation across demanding industrial environments. The perforated galvanized surface provides superior durability and corrosion resistance, making these screens ideal for harsh operating conditions. Custom sizing options ensure seamless integration into existing production lines without compromising efficiency or output quality.
These robust vibrating screens handle materials ranging from fine powders to coarse aggregates with consistent precision. The forging construction guarantees long-term reliability with minimal maintenance needs. Industries depend on these screens for critical separation processes where consistent particle size distribution is essential for maintaining quality standards and operational continuity.
- Separating and grading crushed stones in construction aggregate production
- Sorting minerals and ores by size in mining and quarrying operations
- Removing contaminants and sizing materials in recycling facilities
- Classifying pharmaceutical powders and chemical compounds in manufacturing
- Filtering and dewatering agricultural products in food processing operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Indian Engi-Fab Corporation, Maharashtra
 Maharashtra, India
Tools & Hardware•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Mid East
Southern Europe
South Asia
Industrial Square Vibrating Screen Perforated Galvanized Forging
Industrial square vibrating screen with perforated galvanized surface for efficient material separation in mining, aggregates, and recycling operations. Heavy-duty construction ensures maximum reliability with minimal maintenance requirements.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Indian Engi-Fab Corporation
 Maharashtra, India
Tools & HardwareManufacturer