IN
₹
Apparel & Fashion

Description
Our high-performance vibrating screen represents the pinnacle of material separation technology, engineered specifically for demanding industrial applications. Built with precision engineering and robust construction, this equipment delivers exceptional screening efficiency across various material types and operating conditions. The vibrating screen features advanced vibration mechanisms that ensure consistent material flow and accurate particle separation, even under continuous heavy-duty operation. With customizable deck configurations and mesh materials, each unit can be tailored to specific processing requirements, providing optimal performance for your unique operational needs. The durable design minimizes maintenance requirements while maximizing uptime, making it a reliable long-term investment for serious B2B buyers seeking quality industrial equipment.

Across multiple industries, vibrating screens prove indispensable for material processing and quality control. In mining and ...
Our high-performance vibrating screen represents the pinnacle of material separation technology, engineered specifically for demanding industrial applications. Built with precision engineering and robust construction, this equipment delivers exceptional screening efficiency across various material types and operating conditions. The vibrating screen features advanced vibration mechanisms that ensure consistent material flow and accurate particle separation, even under continuous heavy-duty operation. With customizable deck configurations and mesh materials, each unit can be tailored to specific processing requirements, providing optimal performance for your unique operational needs. The durable design minimizes maintenance requirements while maximizing uptime, making it a reliable long-term investment for serious B2B buyers seeking quality industrial equipment.

Across multiple industries, vibrating screens prove indispensable for material processing and quality control. In mining and quarrying operations, they efficiently separate ores, coal, and aggregates by size, ensuring only properly graded materials proceed to subsequent processing stages. The construction industry relies on these screens for producing precisely sized sand, gravel, and crushed stone for concrete and asphalt production. Chemical and fertilizer manufacturers utilize vibrating screens for accurate particle classification and impurity removal. Food processing facilities depend on them for sorting grains, powders, and ingredients to maintain product quality and safety standards. Recycling plants employ these screens for efficient waste material separation and recovery operations.

The business value of our vibrating screen extends beyond mere equipment functionality to deliver tangible operational advantages and reliability. Investing in our screening solution means acquiring a partner in productivity enhancement and cost reduction. The robust construction and premium components ensure extended service life with minimal downtime, directly impacting your bottom line through reduced maintenance costs and consistent output quality. Our screens differentiate through superior engineering that maintains precise screening accuracy even after years of continuous operation. The customizable features allow perfect integration with your existing processes, while the reliable performance builds trust through consistent delivery of expected results. This equipment represents not just a purchase but a strategic investment in operational excellence and long-term business growth.

Key Features:
- Heavy-duty construction with reinforced frames for extended durability
- Precision vibration mechanisms ensuring consistent screening accuracy
- Customizable deck configurations and mesh materials for specific applications
- Efficient motor systems designed for continuous operation with minimal energy consumption
- Easy maintenance access points and replaceable wear components

Benefits:
- Increased processing throughput and operational efficiency
- Reduced maintenance costs and extended equipment lifespan
- Consistent product quality through precise particle separation
- Customizable solutions tailored to specific industry requirements
- Reliable performance in demanding industrial environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | 106 |
Application
Vibrating screens serve as critical equipment across multiple industries where precise material separation is required. These robust machines handle everything from coarse aggregates to fine powders, maintaining consistent performance under heavy operational demands. Their versatility makes them indispensable in processing facilities worldwide.
From mining operations to food processing plants, vibrating screens provide reliable grading and classification solutions. They efficiently separate materials by size, remove impurities, and handle dewatering tasks. Customizable configurations ensure optimal performance across different material types and production requirements, making them valuable assets for industrial buyers. Real-world applications:
Real-world applications:
- Mining operations for separating ores, coal, and minerals by particle size
- Aggregate plants for grading sand, gravel, and crushed stone materials
- Food processing facilities for sorting grains, powders, and food ingredients
- Chemical and fertilizer industries for precise particle classification
- Recycling plants for sorting and separating waste materials efficiently
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | chennai |
Company Profile
CALCUTTA WIRE NETTING COMPANY, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
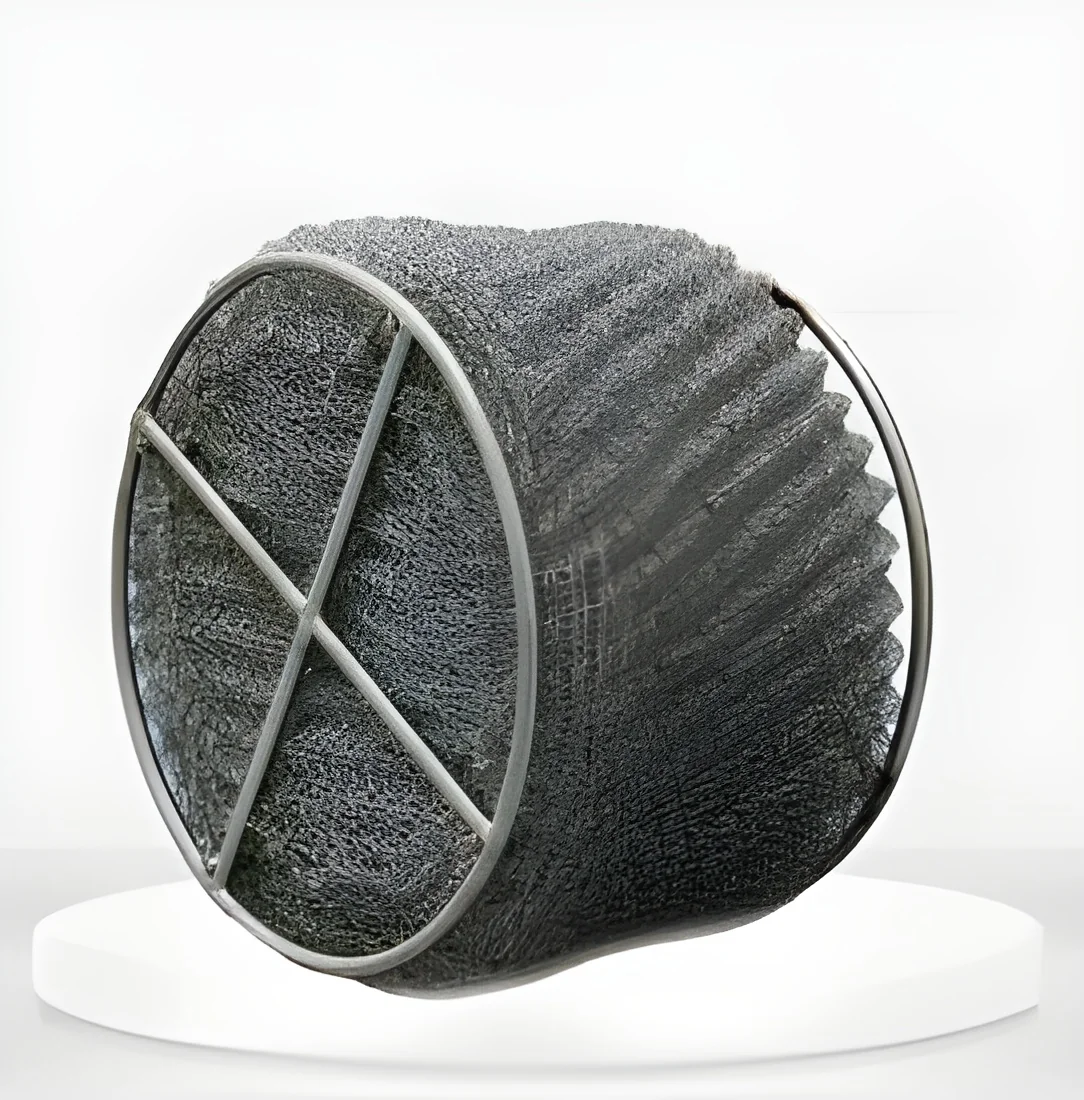
Industrial Vibrating Screen For Mining Aggregate Processing
High-performance vibrating screen for precise material separation in mining, aggregate, and industrial processing. Delivers durability, reliability, and high throughput for demanding B2B operations.
Min. Order Quantity: 1
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
CALCUTTA WIRE NETTING COMPANY
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer