IN
₹
Description
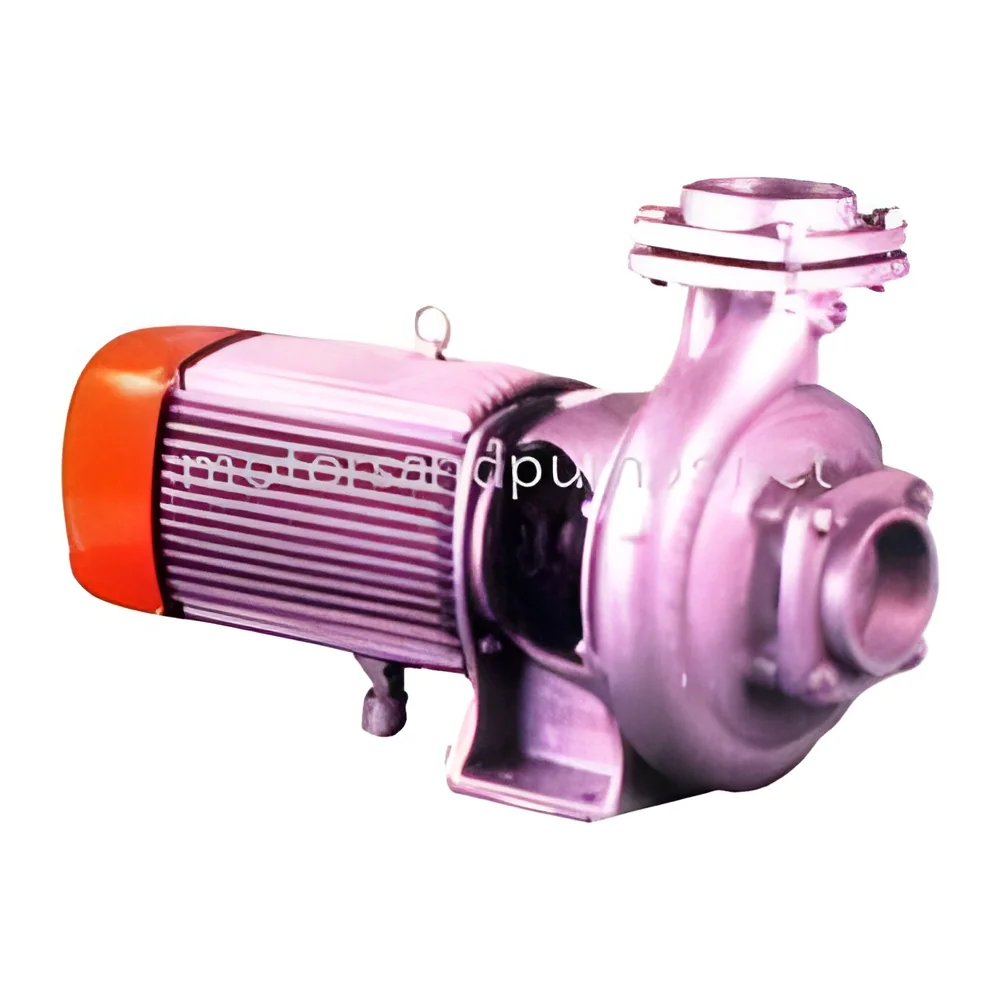
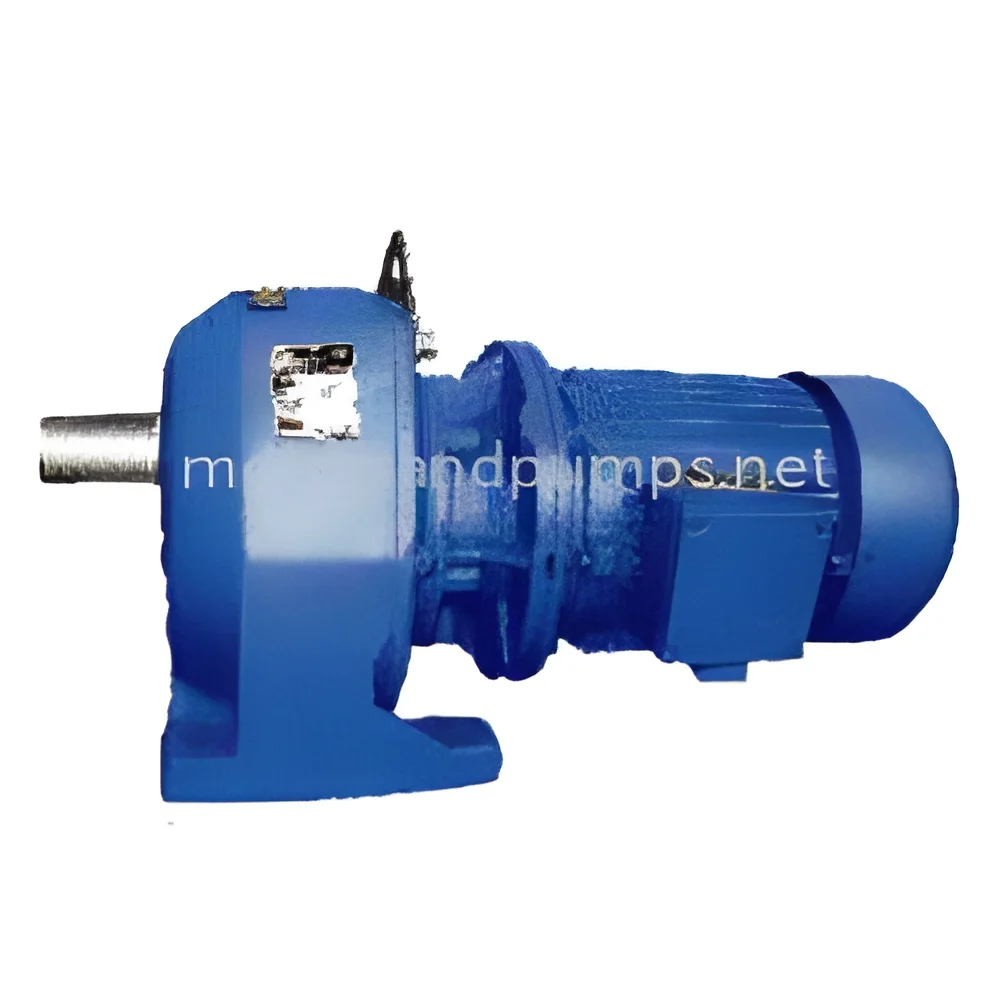
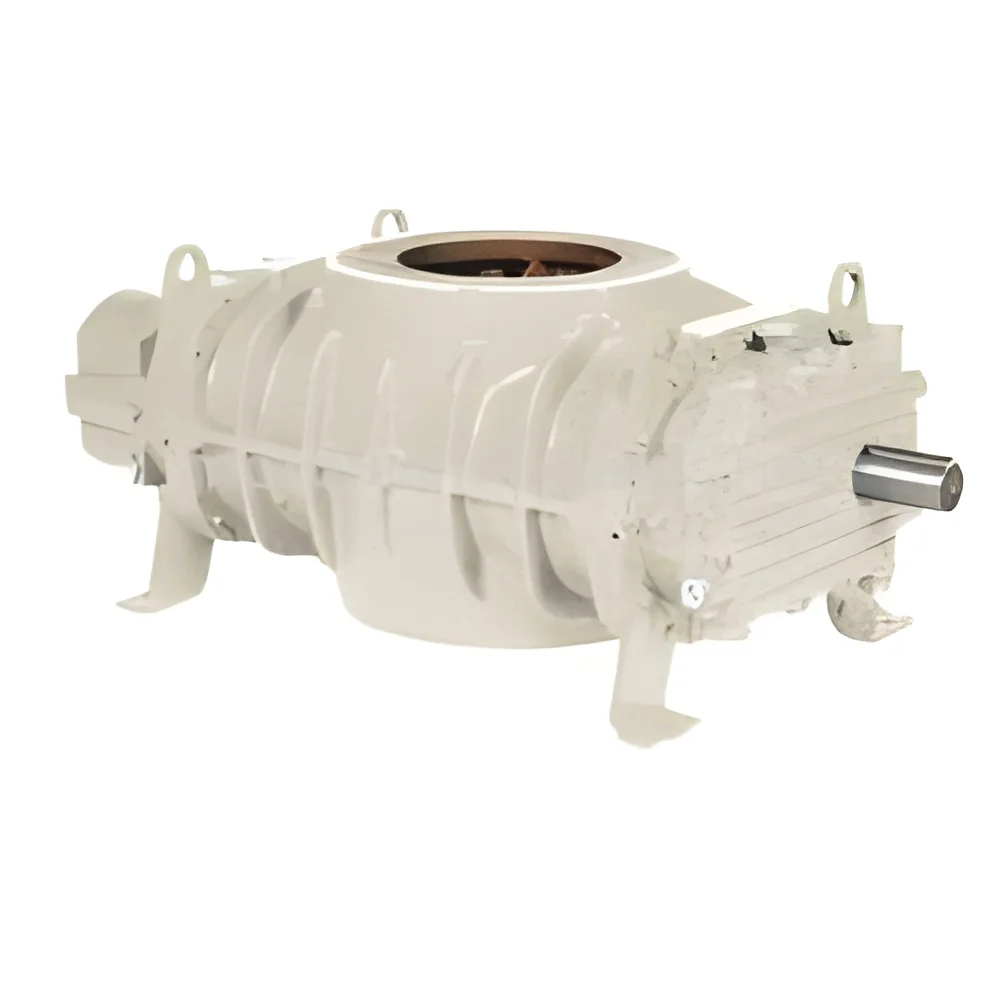
The Industrial Twin Lobe Vacuum Pump represents a reliable, high-performance solution for industrial vacuum requirements. This electric-powered, single-stage pump is specifically designed to deliver consistent high-pressure performance and is constructed for compatibility with water-based applications. Its core twin lobe technology ensures smooth, pulsation-free operation, which is critical for maintaining stable vacuum levels in sensitive processes. Built with durability and long service life in mind, it features precision-engineered components that work in harmony to provide dependable operation under continuous industrial use. This pump is the go-to choice for operations that cannot afford interruptions, offering proven reliability and the ability to meet diverse operational demands efficiently.

This vacuum pump serves as a vital component across a spectrum of industries. In manufacturing, it is integral to plastic molding, extrusion processes, and automated material handling syste...
The Industrial Twin Lobe Vacuum Pump represents a reliable, high-performance solution for industrial vacuum requirements. This electric-powered, single-stage pump is specifically designed to deliver consistent high-pressure performance and is constructed for compatibility with water-based applications. Its core twin lobe technology ensures smooth, pulsation-free operation, which is critical for maintaining stable vacuum levels in sensitive processes. Built with durability and long service life in mind, it features precision-engineered components that work in harmony to provide dependable operation under continuous industrial use. This pump is the go-to choice for operations that cannot afford interruptions, offering proven reliability and the ability to meet diverse operational demands efficiently.

This vacuum pump serves as a vital component across a spectrum of industries. In manufacturing, it is integral to plastic molding, extrusion processes, and automated material handling systems, where consistent vacuum is crucial for product formation and transfer. The packaging sector relies on it for vacuum packaging machines, carton erectors, and labeling systems to ensure secure and efficient product packaging. Chemical processing plants utilize its capabilities for distillation, filtration, and evaporation tasks, handling various vapors reliably. Furthermore, the medical and laboratory fields employ these pumps to provide the stable vacuum necessary for diagnostic equipment, research instruments, and sterilization processes. Its design ensures it performs effectively across both light and heavy industrial settings.

Investing in this twin lobe vacuum pump delivers tangible business value through enhanced operational efficiency and reliability. The pump's efficient design minimizes energy consumption while maintaining consistent vacuum output, leading to significant reductions in long-term operating costs. Its robust construction and proven twin lobe mechanism result in minimal unscheduled downtime and lower maintenance requirements, directly boosting productivity and throughput. This reliability ensures consistent product quality in manufacturing and reduces material waste. The pump's standard, ready-to-integrate configuration and adaptability allow for flexible deployment across multiple processes, maximizing utility. Ultimately, its long service life and dependable performance provide operational predictability and a strong return on investment.

Key Features:
- Electric-powered operation ensures consistent, controllable performance.
- Single-stage design capable of delivering high-pressure vacuum output.
- Water-compatible construction allows for use in diverse industrial applications.
- Twin lobe technology provides smooth, low-pulsation operation for process stability.
- Standard configuration designed for straightforward industrial integration.

Benefits:
- Reliable, consistent vacuum generation enhances process stability and product quality.
- Robust construction and efficient design reduce maintenance needs and operational downtime.
- Energy-efficient operation helps lower overall power consumption and running costs.
- Versatile, water-compatible application suitability across multiple industries.
- Standard design ensures easy installation and integration into existing systems.
Specifications
| Key Attributes | |
|---|---|
| Power | Electric |
| Pressure | High Pressure |
| Standardor Nonstandard | Standard |
| Structure | Single-stage Pump |
| Theory | Vacuum Pump |
| Usage | Water |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This robust twin lobe vacuum pump is engineered for continuous, demanding industrial operations where consistent vacuum generation is non-negotiable. Its electric-powered, single-stage design provides reliable high-pressure performance, making it a cornerstone for systems that handle gases and vapors with precision. The water-compatible construction ensures versatility across various process environments, from material handling to automated production lines, offering seamless integration and dependable duty cycles.
Industries leverage this pump's efficiency and low-maintenance design to enhance operational reliability and reduce downtime. Its adaptability to different conditions and consistent output make it suitable for integration into existing setups without extensive modifications. The pump's performance supports critical processes that depend on stable vacuum levels, ensuring product quality and process integrity in applications ranging from packaging to chemical transfer.
- Vacuum packaging and sealing systems within food processing and pharmaceutical production lines.
- Plastic thermoforming, extrusion, and injection molding processes for consistent material handling.
- Operation of printing presses, paper converting equipment, and laminating machinery.
- Chemical processing applications including solvent recovery, distillation, and filtration systems.
- Medical and laboratory equipment requiring stable vacuum for diagnostic and analytical instruments.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Twin Lobe Vacuum Pump Electric High Pressure Single Stage
Industrial Twin Lobe Vacuum Pump delivers high-pressure, single-stage electric performance for water-compatible applications in manufacturing, packaging, and processing industries requiring reliable vacuum generation.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company