IN
₹
Description
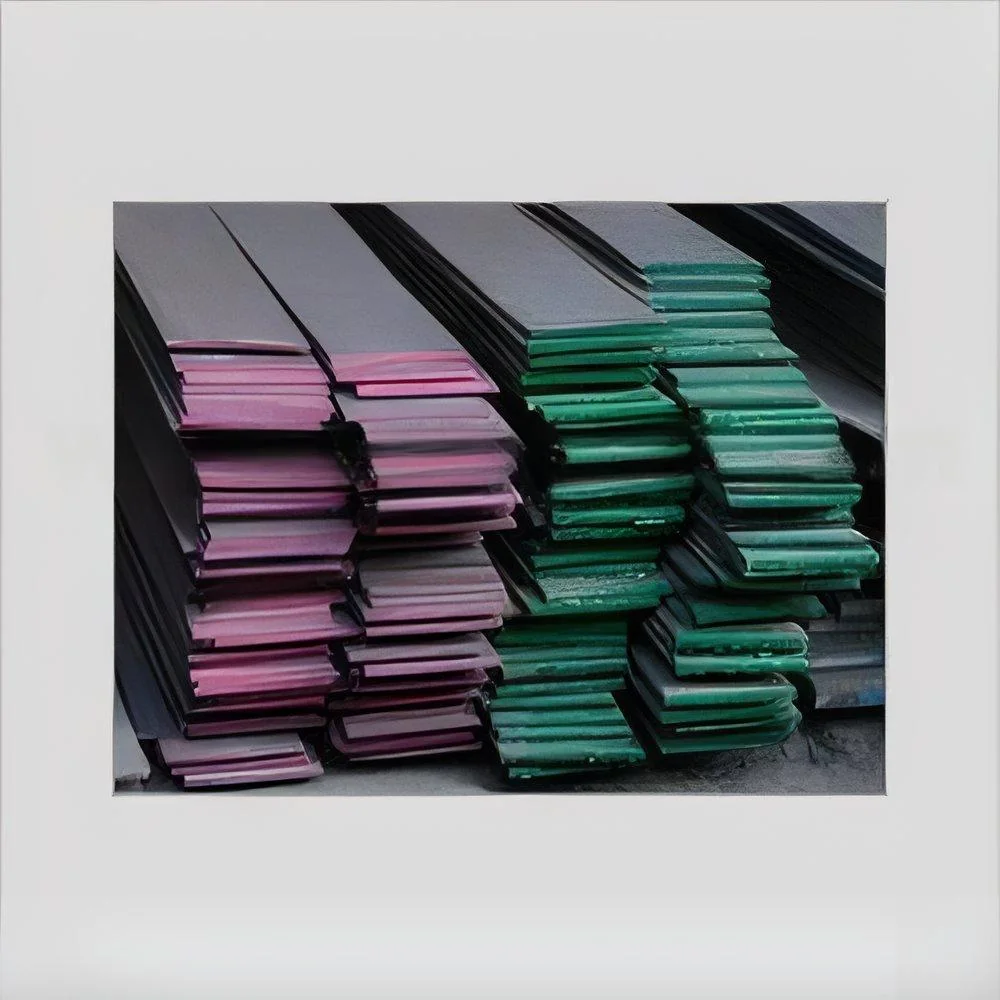
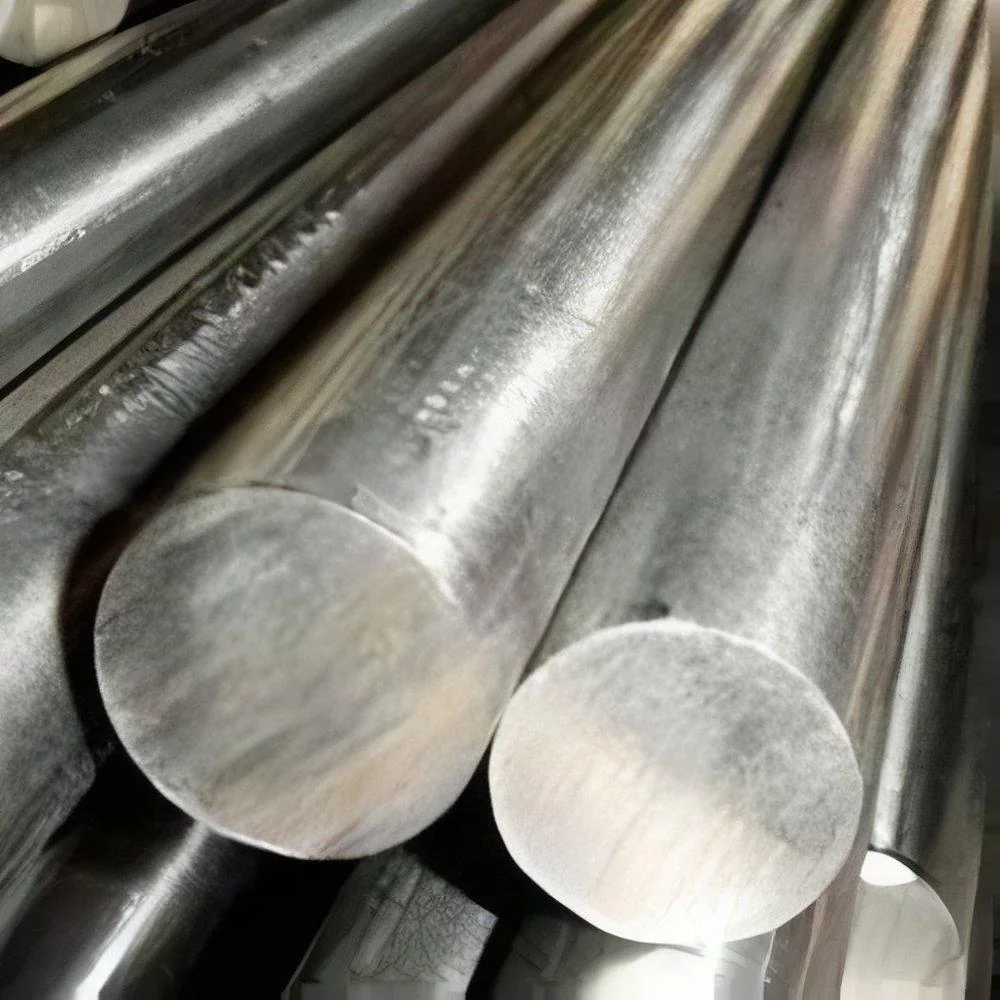
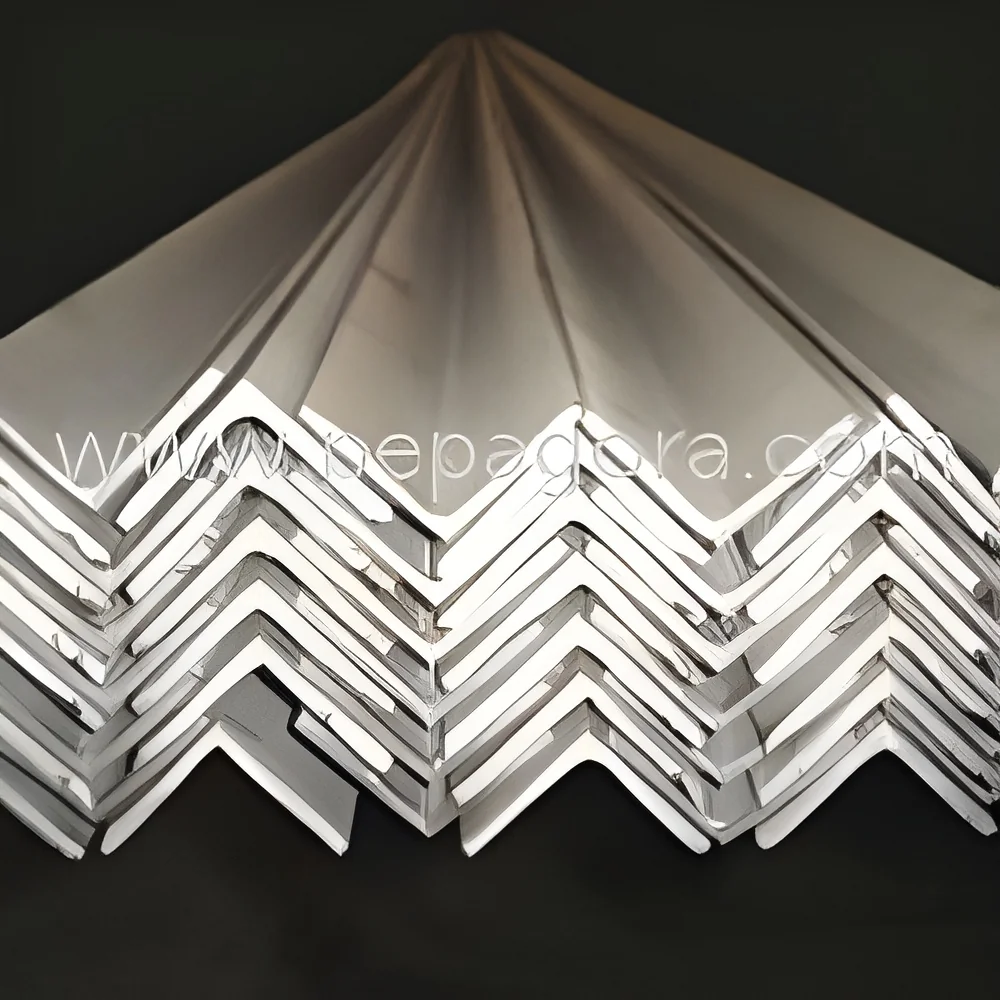
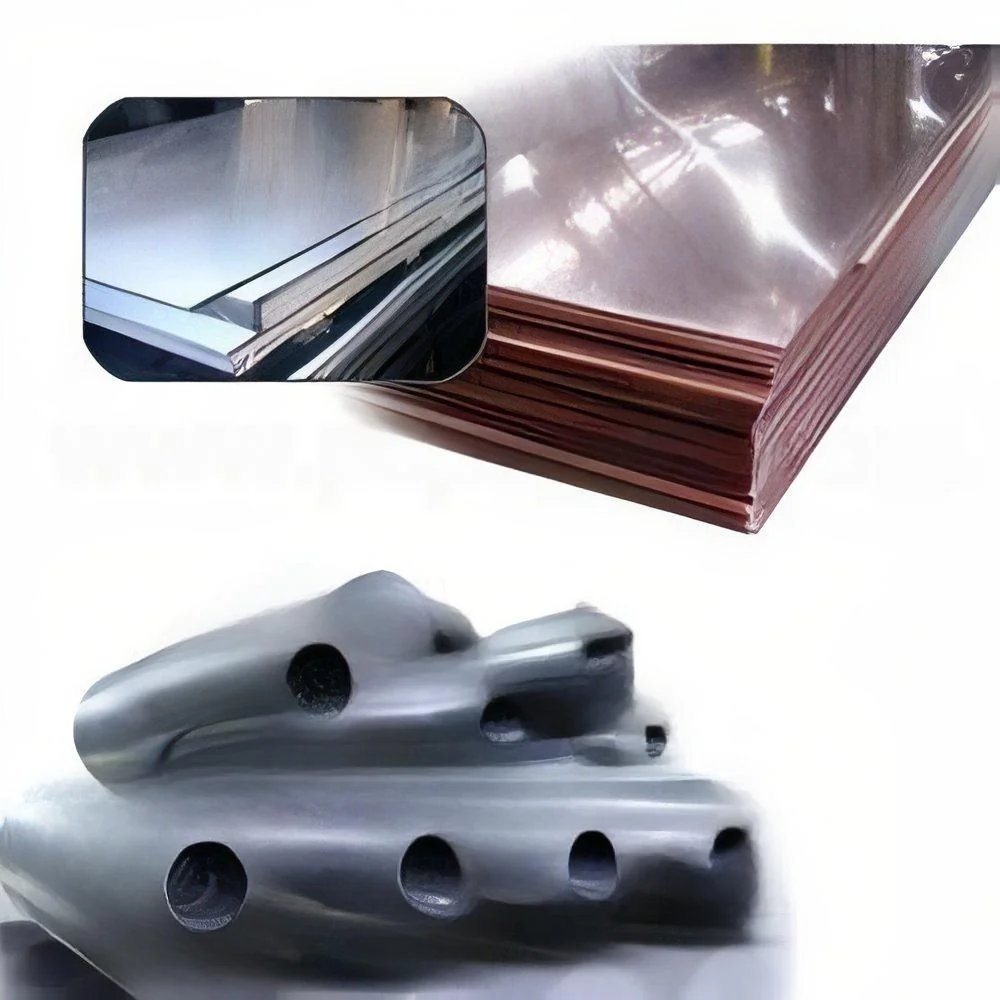
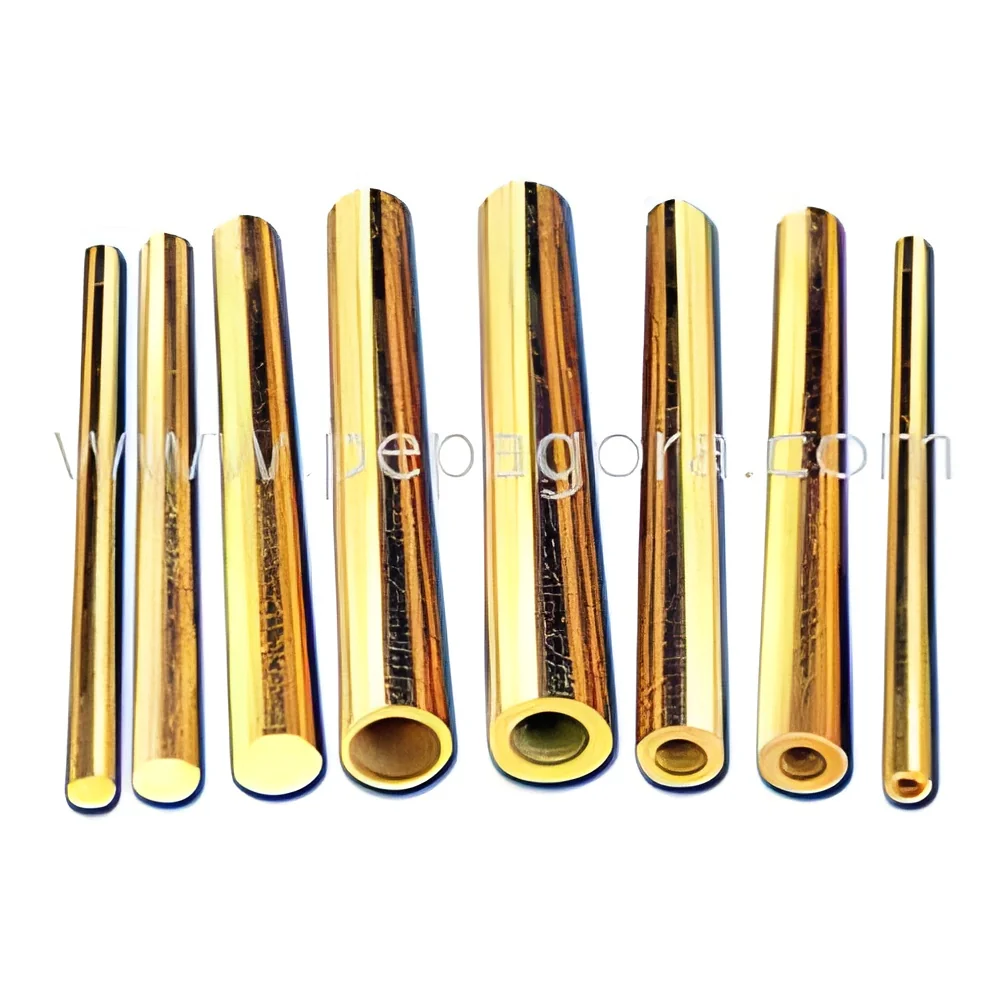
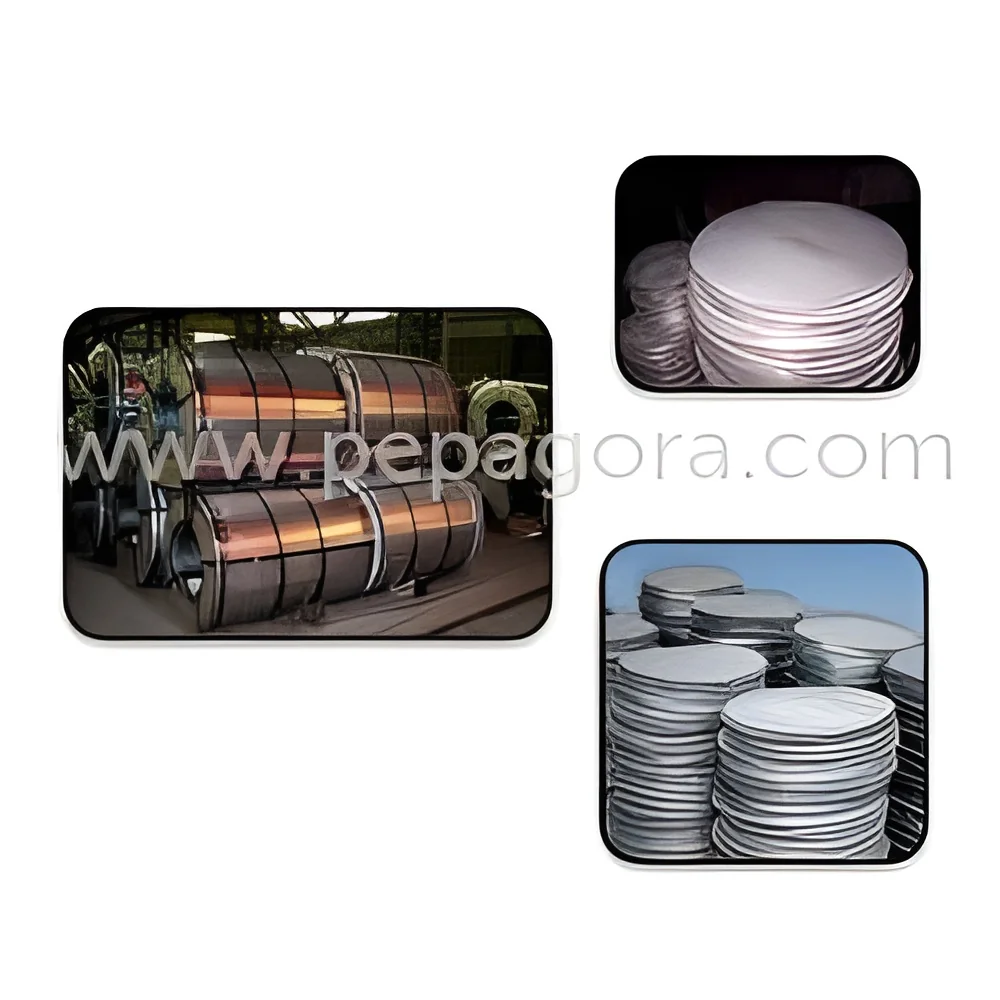
Industrial titanium metal products in coral grade represent premium materials engineered for maximum corrosion resistance and reliability in demanding environments. These products maintain structural integrity when exposed to aggressive chemicals, high temperatures, and mechanical stress, making them suitable for critical applications where material failure is not an option. Manufactured to consistent quality standards, these titanium products deliver predictable performance and long service life, reducing the risk of unexpected downtime and maintenance issues. The coral grade specification ensures optimal material properties for industrial applications requiring exceptional durability and resistance to degradation.

These titanium products serve vital roles across multiple industrial sectors where material performance directly impacts operational safety and efficiency. In chemical processing industries, they're used in reactors, heat exchangers, and piping systems that handle corrosiv...
Industrial titanium metal products in coral grade represent premium materials engineered for maximum corrosion resistance and reliability in demanding environments. These products maintain structural integrity when exposed to aggressive chemicals, high temperatures, and mechanical stress, making them suitable for critical applications where material failure is not an option. Manufactured to consistent quality standards, these titanium products deliver predictable performance and long service life, reducing the risk of unexpected downtime and maintenance issues. The coral grade specification ensures optimal material properties for industrial applications requiring exceptional durability and resistance to degradation.

These titanium products serve vital roles across multiple industrial sectors where material performance directly impacts operational safety and efficiency. In chemical processing industries, they're used in reactors, heat exchangers, and piping systems that handle corrosive substances. Aerospace applications benefit from their high strength-to-weight ratio in engine components and structural parts. Marine engineering utilizes titanium for shipbuilding and offshore structures exposed to saltwater environments. Power generation facilities rely on these materials for turbines and heat exchangers operating under extreme temperatures, while medical equipment manufacturers value their biocompatibility and corrosion resistance for surgical instruments and devices.

The business value of these titanium metal products lies in their ability to reduce total cost of ownership through extended equipment lifespan and minimized maintenance requirements. Their exceptional corrosion resistance prevents material degradation, lowering replacement costs and reducing operational downtime. The reliability of these materials ensures consistent performance in critical processes, enhancing safety and operational efficiency. Quality assurance processes guarantee material consistency and performance predictability, making these products a strategic investment for businesses prioritizing long-term operational excellence and cost management.

Key Features:
- Coral grade titanium providing superior corrosion resistance in aggressive environments
- High strength-to-weight ratio for lightweight yet durable component construction
- Excellent mechanical properties maintained across wide temperature ranges
- Consistent material quality ensuring predictable performance and reliability
- Long service life with minimal degradation in demanding operating conditions

Benefits:
- Reduced maintenance costs through exceptional corrosion resistance and durability
- Extended equipment lifespan lowering total cost of ownership and replacement expenses
- Enhanced operational safety through reliable performance in critical applications
- Improved efficiency with materials that maintain properties under extreme conditions
- Long-term value investment with predictable performance and reduced downtime
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Titanium metal products in coral grade deliver critical performance where corrosion resistance and structural integrity are essential. These materials withstand aggressive chemicals, high temperatures, and mechanical stress while maintaining their properties over extended service periods. Their reliability reduces maintenance needs and extends equipment lifespan across multiple industrial sectors.
These titanium solutions serve industries requiring materials that perform under extreme conditions without compromising safety or efficiency. From chemical processing equipment to aerospace components, marine structures, and power generation systems, titanium's unique properties address the most challenging operational requirements. The consistent quality ensures predictable performance in critical applications where failure is not an option.
- Chemical processing equipment including reactors, heat exchangers, and piping systems handling corrosive substances
- Aerospace components such as engine parts, fasteners, and structural elements requiring strength and lightweight properties
- Marine applications including propeller shafts, hull components, and offshore platform parts exposed to saltwater
- Power generation equipment like turbines, condensers, and heat exchangers operating under high temperatures
- Medical devices and equipment where biocompatibility and corrosion resistance are essential requirements
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Mahendra Steel India, Karnataka
 Karnataka, India
Construction•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Titanium Metal Products Coral Grade High Corrosion Resistance
Industrial titanium metal products in coral grade offer high corrosion resistance for demanding applications across chemical, aerospace, marine, and power generation industries. These reliable materials ensure long-term performance in aggressive environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Mahendra Steel India
 Karnataka, India
ConstructionDistributor / Wholesaler