IN
₹
Description
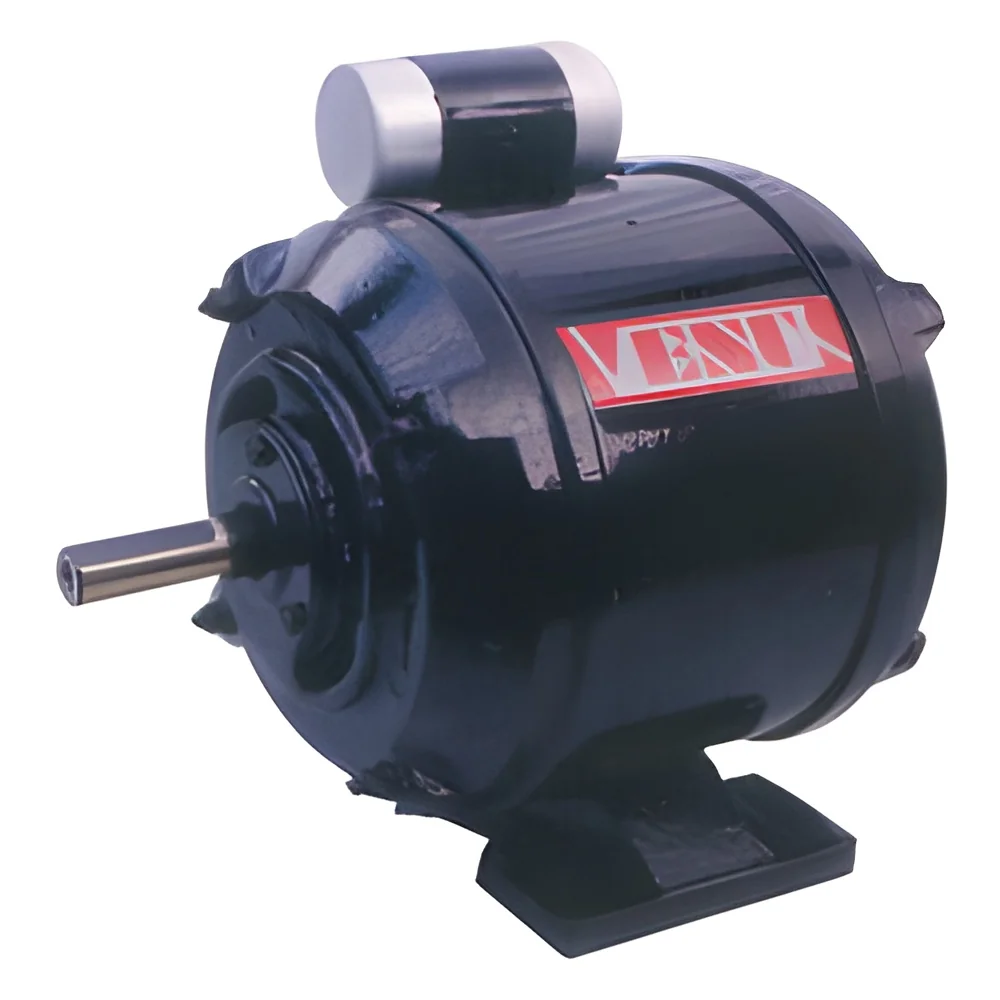
Our premium three phase flame proof induction motors are specifically engineered for maximum safety and performance in hazardous environments where explosive atmospheres are present. These motors feature certified flameproof enclosures that prevent internal sparks or explosions from igniting surrounding flammable gases, vapors, or dust. Designed to meet stringent international standards including ATEX and IECEx certifications, they provide reliable operation where conventional motors would create significant safety risks. The robust construction ensures complete containment of any internal ignition, protecting both personnel and equipment while maintaining continuous operational efficiency in the most challenging industrial conditions.

These motors serve critical roles across multiple high-risk industries including oil and gas extraction, refining facilities, chemical processing plants, pharmaceutical manufacturing, mining operations, and grain handling facilities. In oil and gas appl...
Our premium three phase flame proof induction motors are specifically engineered for maximum safety and performance in hazardous environments where explosive atmospheres are present. These motors feature certified flameproof enclosures that prevent internal sparks or explosions from igniting surrounding flammable gases, vapors, or dust. Designed to meet stringent international standards including ATEX and IECEx certifications, they provide reliable operation where conventional motors would create significant safety risks. The robust construction ensures complete containment of any internal ignition, protecting both personnel and equipment while maintaining continuous operational efficiency in the most challenging industrial conditions.

These motors serve critical roles across multiple high-risk industries including oil and gas extraction, refining facilities, chemical processing plants, pharmaceutical manufacturing, mining operations, and grain handling facilities. In oil and gas applications, they power essential equipment in classified hazardous zones where flammable substances are present. Chemical plants utilize them for mixing, pumping, and ventilation systems where explosive vapors may accumulate. Mining operations depend on these motors for conveyor systems and ventilation in underground environments with combustible dust. Pharmaceutical manufacturers employ them in processes involving flammable solvents, while grain facilities use them in elevators and processing equipment where dust explosions are a constant concern.

The business value of these flame proof motors lies in their exceptional reliability, reduced downtime, and long-term operational safety. They are built with premium materials including heavy-duty cast iron construction that ensures durability and extended service life even in corrosive environments. Advanced thermal protection systems prevent overheating, while high-efficiency designs reduce energy consumption and operating costs. Each motor undergoes rigorous testing and quality assurance procedures to guarantee performance, safety, and compliance before delivery, providing businesses with confidence in their critical operations.

Key Features:
- Certified flameproof enclosure designed for explosive atmospheres meeting international standards
- Robust cast iron construction ensuring durability and corrosion resistance in harsh environments
- High efficiency design reducing energy consumption and operating costs significantly
- Customizable power ratings and mounting configurations for specific operational needs
- Advanced thermal protection systems preventing overheating and ensuring operational safety

Benefits:
- Enhanced workplace safety through certified explosion-proof protection in hazardous zones
- Reduced operational costs through energy-efficient performance and minimal maintenance requirements
- Extended equipment lifespan with durable construction suitable for harsh industrial environments
- Reliable continuous operation minimizing production downtime and maintenance interruptions
- Compliance with international safety standards ensuring regulatory approval and operational confidence
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial flame proof induction motors are specifically engineered for environments where flammable gases, vapors, or combustible dust create explosive atmospheres. They provide critical operational safety and uninterrupted power in demanding conditions where standard motors would pose significant ignition risks and safety hazards to personnel and facilities.
Ideal for oil and gas facilities, chemical processing plants, mining operations, pharmaceutical manufacturing, and grain processing units. These motors ensure compliance with international safety standards while delivering consistent performance in applications requiring certified explosion-proof equipment and reliable continuous operation in classified hazardous zones.
- Powering pumps and compressors in petrochemical refineries and offshore platforms
- Operating conveyor systems in underground mining and coal handling plants
- Driving ventilation fans in chemical processing facilities and paint manufacturing units
- Running mixers and agitators in pharmaceutical production and chemical synthesis processes
- Operating crushers, grinders, and elevators in grain silos and food processing facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Bestow International, Tamil Nadu
 Tamil Nadu, India
Construction•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Flame Proof Induction Motors For Hazardous Environments
Premium three phase flame proof induction motors deliver reliable explosion-proof power for hazardous environments. Robust construction, certified safety, and custom ratings ensure efficient operation in industries requiring ignition-protected solutions.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bestow International
 Tamil Nadu, India
ConstructionManufacturer