IN
₹
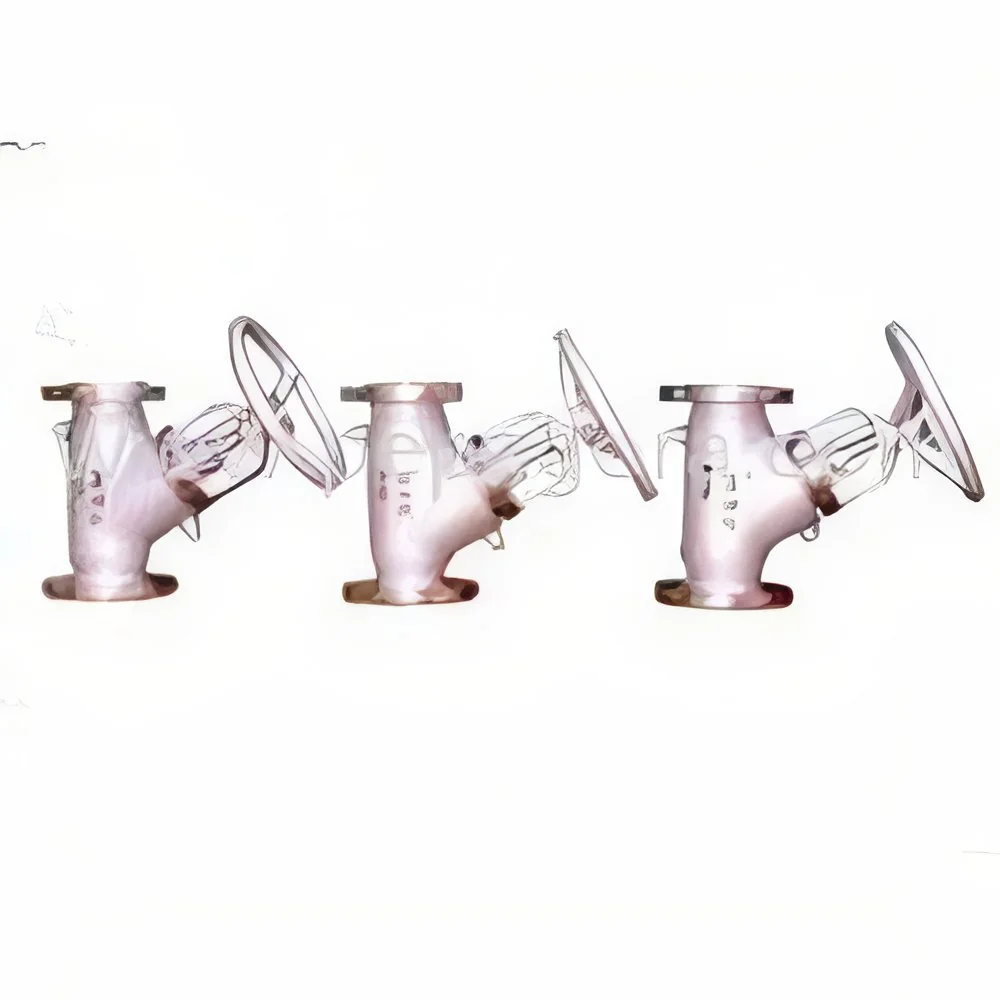
Description
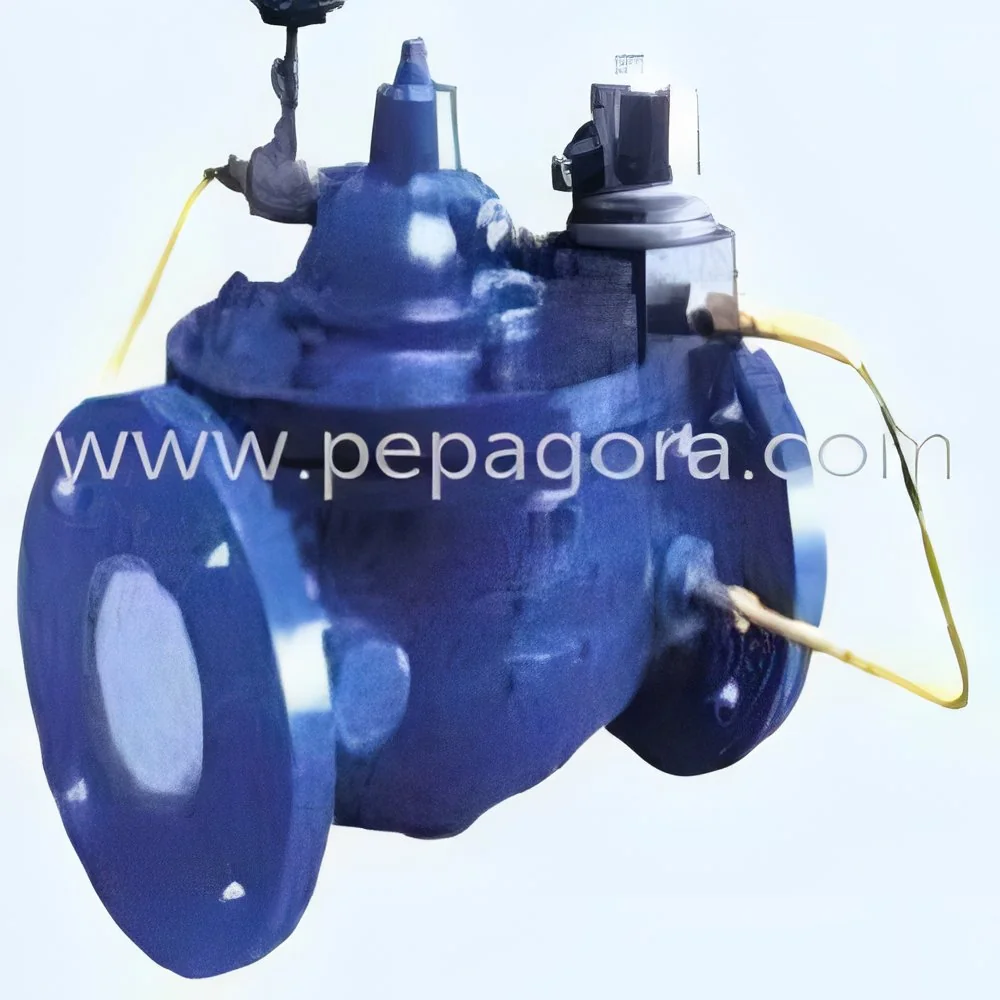
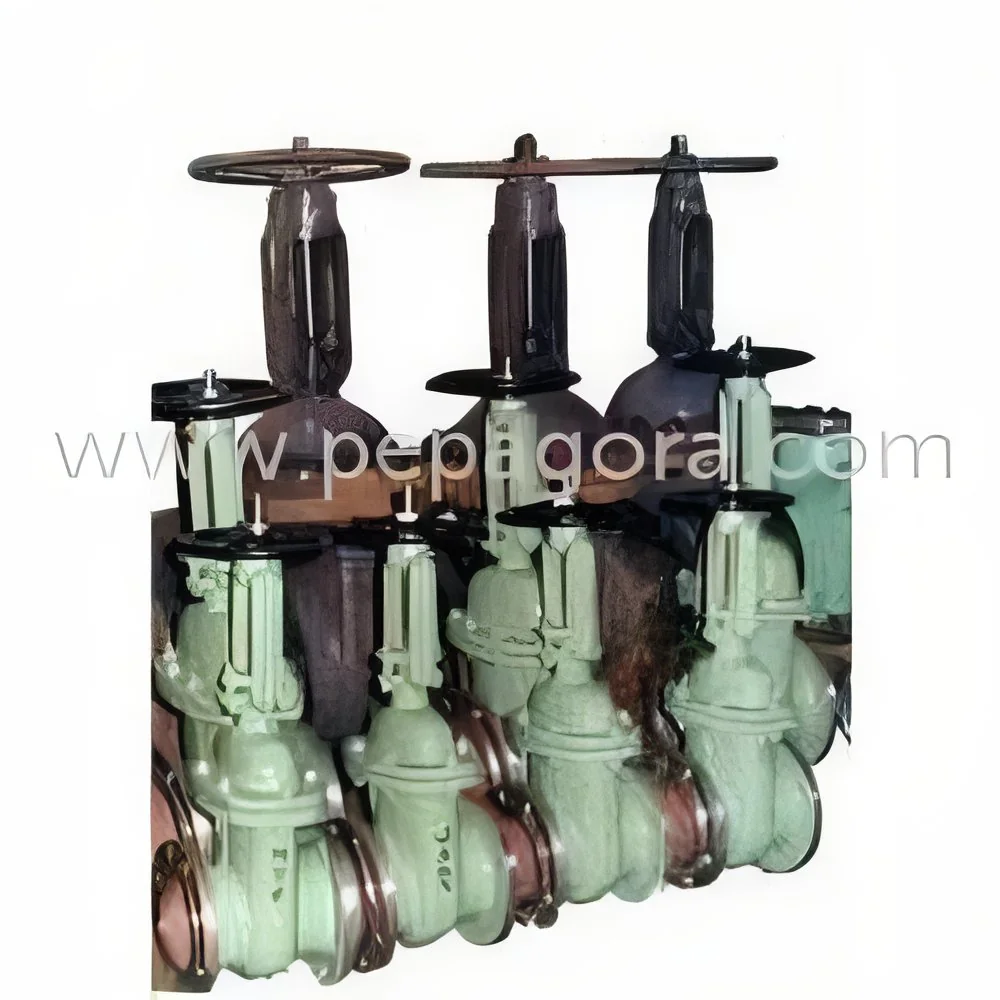
Our industrial steam globe valves represent premium engineering solutions specifically designed for high-temperature and high-pressure steam control in demanding industrial environments. Constructed from superior quality materials offering exceptional corrosion resistance and mechanical strength, these valves ensure reliable performance even under continuous operation in harsh conditions. The precision-engineered design guarantees exact dimensional accuracy and superior sealing capabilities, effectively preventing steam leakage while maintaining optimal system efficiency and safety. Manufactured to international standards and subjected to rigorous quality testing protocols, these valves deliver consistent performance where reliability cannot be compromised.

These valves serve as critical components across multiple heavy industries where steam constitutes an essential utility for various processes. In steel plants and metal processing facilities, they regulate steam for heating treatme...
Our industrial steam globe valves represent premium engineering solutions specifically designed for high-temperature and high-pressure steam control in demanding industrial environments. Constructed from superior quality materials offering exceptional corrosion resistance and mechanical strength, these valves ensure reliable performance even under continuous operation in harsh conditions. The precision-engineered design guarantees exact dimensional accuracy and superior sealing capabilities, effectively preventing steam leakage while maintaining optimal system efficiency and safety. Manufactured to international standards and subjected to rigorous quality testing protocols, these valves deliver consistent performance where reliability cannot be compromised.

These valves serve as critical components across multiple heavy industries where steam constitutes an essential utility for various processes. In steel plants and metal processing facilities, they regulate steam for heating treatments and cleaning operations. Paper and pulp mills depend on them for drying cylinders and sterilization processes, while sugar processing plants utilize them extensively in evaporation and crystallization systems. Chemical and pharmaceutical industries employ these valves for precise steam control in reactors, distillation columns, and sterilization autoclaves. Power generation facilities rely on them for boiler feed systems, turbine bypass arrangements, and auxiliary steam applications, ensuring efficient and uninterrupted energy production.

The business value of these steam globe valves lies in their exceptional reliability and suitability for mission-critical applications. They significantly enhance operational safety by providing secure shut-off capabilities and precise flow control, substantially reducing the risk of accidents and system failures. Their robust construction and quality materials minimize maintenance requirements and unexpected downtime, resulting in considerable cost savings throughout the valve's operational lifecycle. The energy efficiency achieved through precise steam management translates to lower operational expenses and reduced environmental impact. These valves deliver long-term value through dependable performance and extended service life in any industrial setting.

Key Features:
- Premium quality materials for exceptional corrosion resistance and durability
- Precision engineering for exact dimensional accuracy and tight sealing
- Multiple size options and pressure ratings to match system requirements
- Rigorous quality testing and international standard compliance
- Robust construction suitable for continuous operation in harsh conditions

Benefits:
- Enhanced operational safety through secure shut-off capabilities
- Reduced maintenance requirements and unexpected downtime
- Long-term cost savings through extended operational lifecycle
- Energy efficiency through precise steam flow management
- Dependable performance in mission-critical industrial applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial steam globe valves deliver precise regulation and secure isolation in high-pressure steam systems across demanding industrial environments. They maintain system integrity under extreme temperatures and pressures, ensuring operational safety and efficiency in continuous production processes. These valves serve as fundamental components where steam functions as a critical utility for heating, processing, and power generation applications, providing consistent performance where reliability is essential for plant operations.
Manufacturing facilities depend on these valves for critical steam management in boiler systems, turbine operations, and process heating applications. Their robust construction withstands harsh conditions found in power generation plants, chemical processing units, and heavy industrial sectors. The valves ensure minimal leakage and maximum durability, supporting uninterrupted production cycles while reducing maintenance requirements across various steam-dependent industrial operations.
- Regulating steam flow in industrial boilers and main steam distribution lines
- Isolation and control applications in thermal power generation facilities
- Process steam systems in chemical and pharmaceutical manufacturing plants
- Heating and drying systems in paper mills and sugar processing operations
- Steam tracing and auxiliary applications in oil, gas, and refinery processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Metropolitan Industries, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Steam Globe Valves For High Pressure High Temperature Control
Industrial steam globe valves provide precise high-pressure high-temperature steam control for demanding industrial applications. These reliable valves feature quality construction for steel plants, paper mills, sugar mills, and chemical industries with superior performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Metropolitan Industries
 West Bengal, India
Industrial Equipment & MachineryManufacturer