IN
₹
Apparel & Fashion

Description
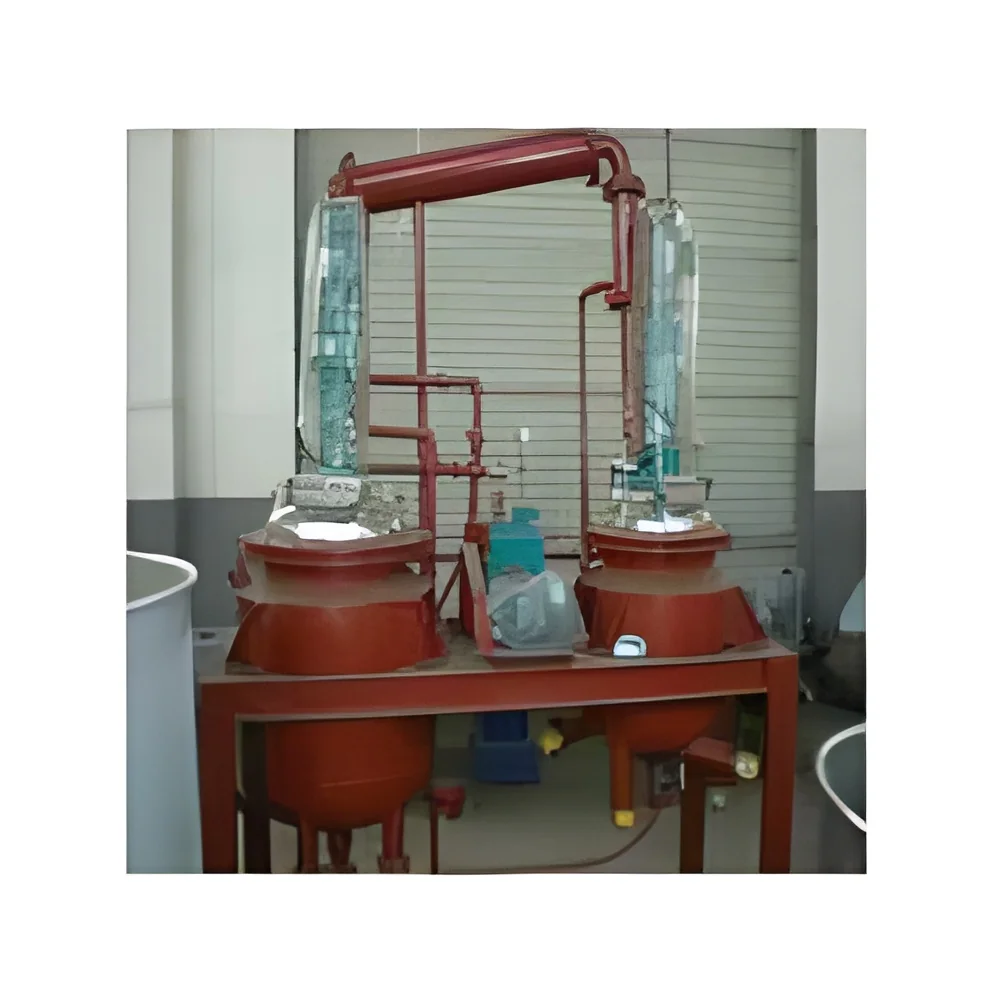
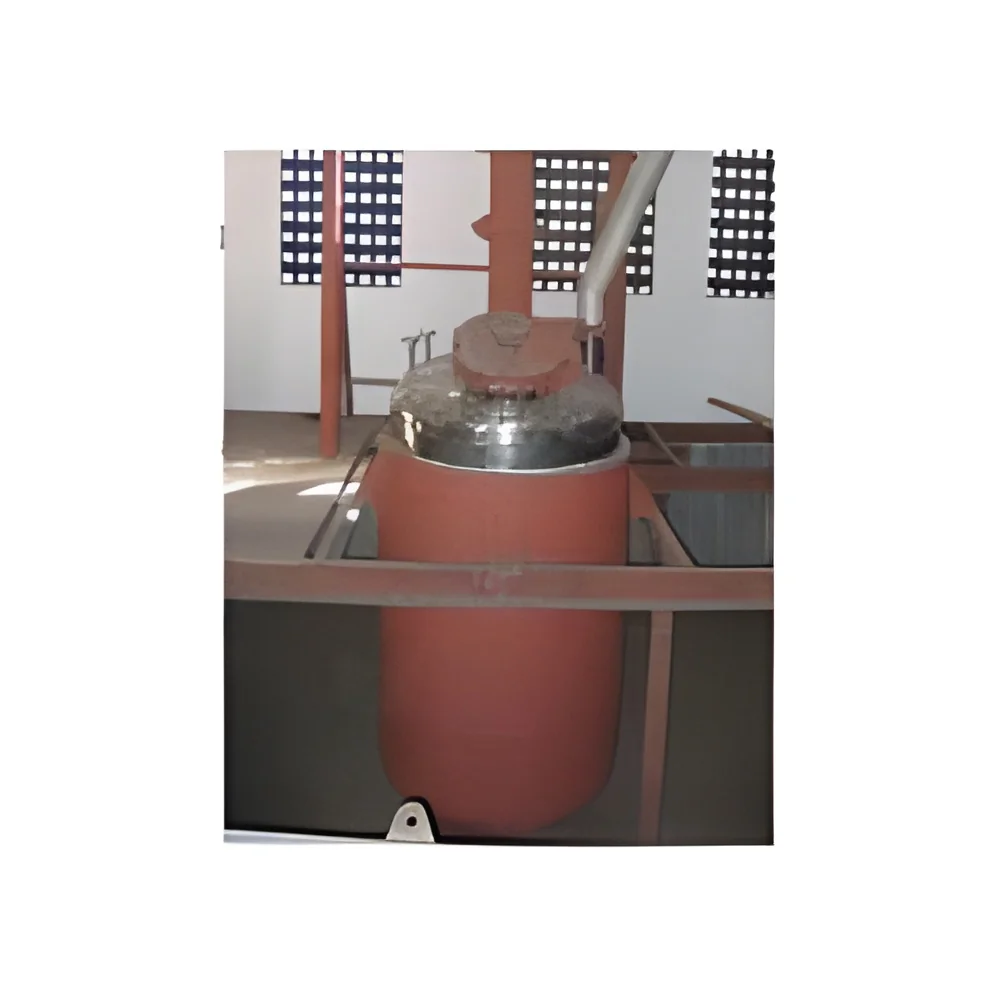
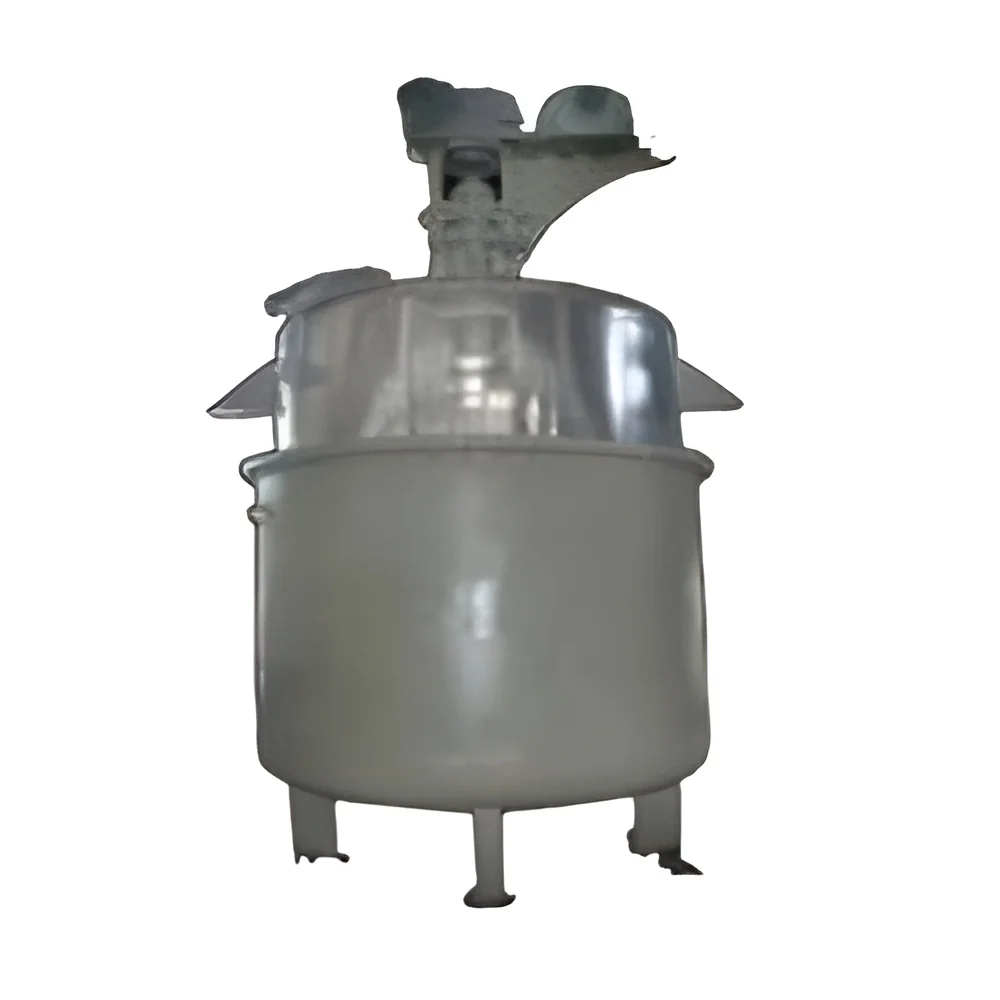
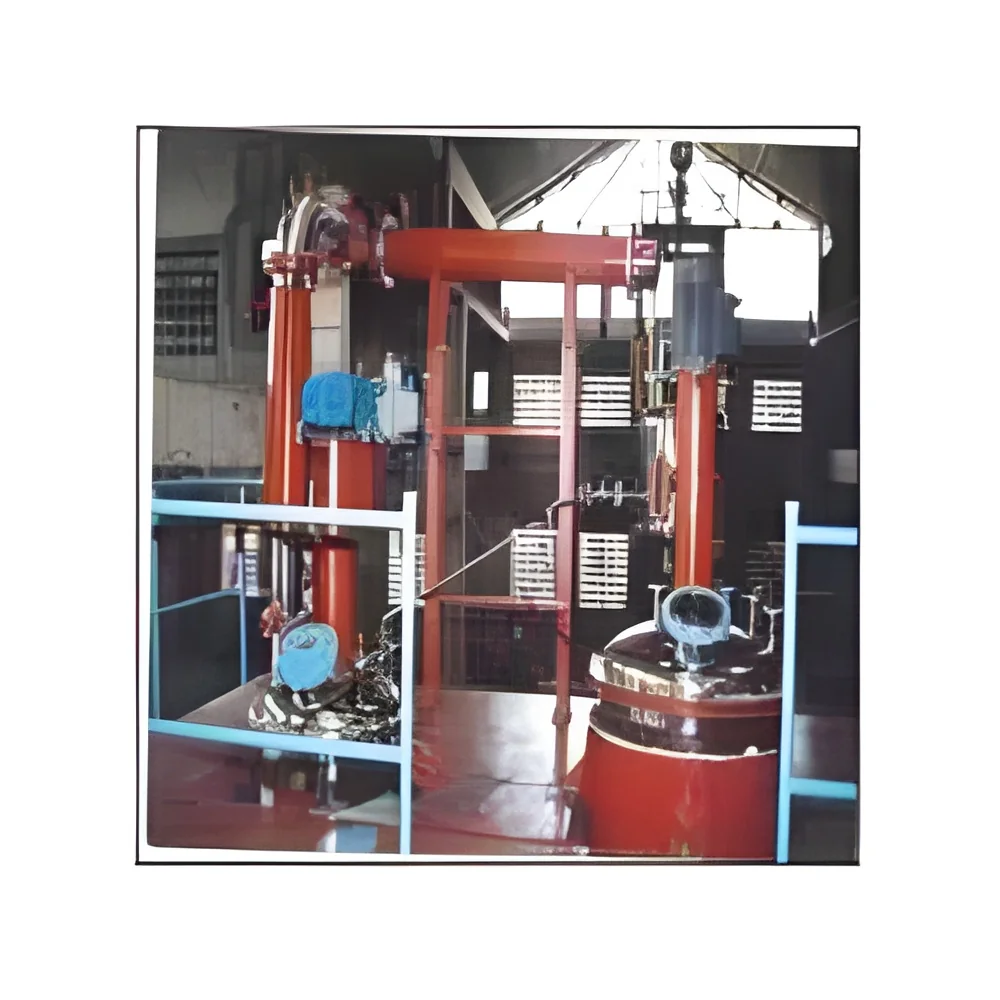
Our multipurpose solvent extraction units represent advanced processing technology designed for extracting valuable compounds from natural materials efficiently. These systems utilize both solvent-based and water-based extraction techniques to recover oils, essences, and active ingredients from various raw materials with precision. Engineered for consistent performance, the units ensure high extraction yields while maintaining the quality and purity of final products. Built with durability as a priority, these extraction systems offer reliable operation and are designed to meet specific production requirements and space constraints, providing dependable processing solutions for industrial applications.

These extraction units serve multiple industries including food processing, pharmaceuticals, nutraceuticals, cosmetics, and chemical manufacturing with equal effectiveness. In the food industry, they extract edible oils from oilseeds and essential flavors from spices for various food pr...
Our multipurpose solvent extraction units represent advanced processing technology designed for extracting valuable compounds from natural materials efficiently. These systems utilize both solvent-based and water-based extraction techniques to recover oils, essences, and active ingredients from various raw materials with precision. Engineered for consistent performance, the units ensure high extraction yields while maintaining the quality and purity of final products. Built with durability as a priority, these extraction systems offer reliable operation and are designed to meet specific production requirements and space constraints, providing dependable processing solutions for industrial applications.

These extraction units serve multiple industries including food processing, pharmaceuticals, nutraceuticals, cosmetics, and chemical manufacturing with equal effectiveness. In the food industry, they extract edible oils from oilseeds and essential flavors from spices for various food products. Pharmaceutical companies utilize them to isolate active compounds from medicinal plants for drug formulations, while cosmetic manufacturers extract natural essences and oils for skincare and beauty products. The chemical industry employs these units for processing natural raw materials into valuable industrial compounds and specialty ingredients, demonstrating their versatility across different sectors.

The business value of these solvent extraction units lies in their proven reliability, operational efficiency, and consistent performance. They deliver repeatable extraction results that reduce material waste while maximizing product yield and quality. The units are designed for straightforward operation and maintenance, minimizing downtime and operational costs through user-friendly interfaces and accessible components. Their adaptability to different materials and processes makes them a valuable long-term investment that can accommodate evolving business needs, providing excellent return on investment through improved production efficiency and consistent product quality that meets industry standards.

Key Features:
- Multipurpose design handles various natural materials and extraction requirements
- Compatible with multiple solvents and water-based extraction techniques
- Configurable to suit specific production needs and space limitations
- High-efficiency extraction system ensures maximum yield and product quality
- Robust construction with durable materials for long-term reliable operation

Benefits:
- Versatile processing capability reduces need for multiple specialized systems
- Flexible solvent compatibility supports diverse extraction methodologies
- Adaptable configurations optimize production workflow and facility utilization
- Enhanced extraction efficiency improves yield and reduces material waste
- Durable construction minimizes maintenance requirements and extends equipment lifespan
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our multipurpose solvent extraction units efficiently extract oils, essences, and active compounds from various natural materials including seeds, herbs, and botanical matter. These systems deliver consistent results across different production scales while handling diverse raw material types with precision and reliability for industrial processing requirements.
The equipment adapts seamlessly to multiple solvents and extraction techniques, supporting both water-based and solvent-based processes. This operational flexibility allows businesses to process different materials without investing in separate specialized equipment, maximizing operational efficiency and return on investment while maintaining consistent product quality across various applications.
- Extracting edible oils from oilseeds including sunflower, soybean, and canola for food production
- Producing essential oils and botanical extracts from herbs and spices for pharmaceutical applications
- Isolating active compounds from medicinal plants for nutraceutical and cosmetic formulations
- Recovering valuable compounds from industrial byproducts and waste materials
- Processing marine and animal sources for omega-3 oils and specialty lipid products
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Alphamech, Maharashtra
 Maharashtra, India
Manufacturer
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Multipurpose Solvent Extraction Units For Natural Materials Processing
Multipurpose solvent extraction units efficiently process natural materials using solvents and water. Ideal for food, pharmaceutical, and chemical industries requiring reliable extraction solutions with consistent performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Alphamech
 Maharashtra, India
Manufacturer