IN
₹
Apparel & Fashion
Description
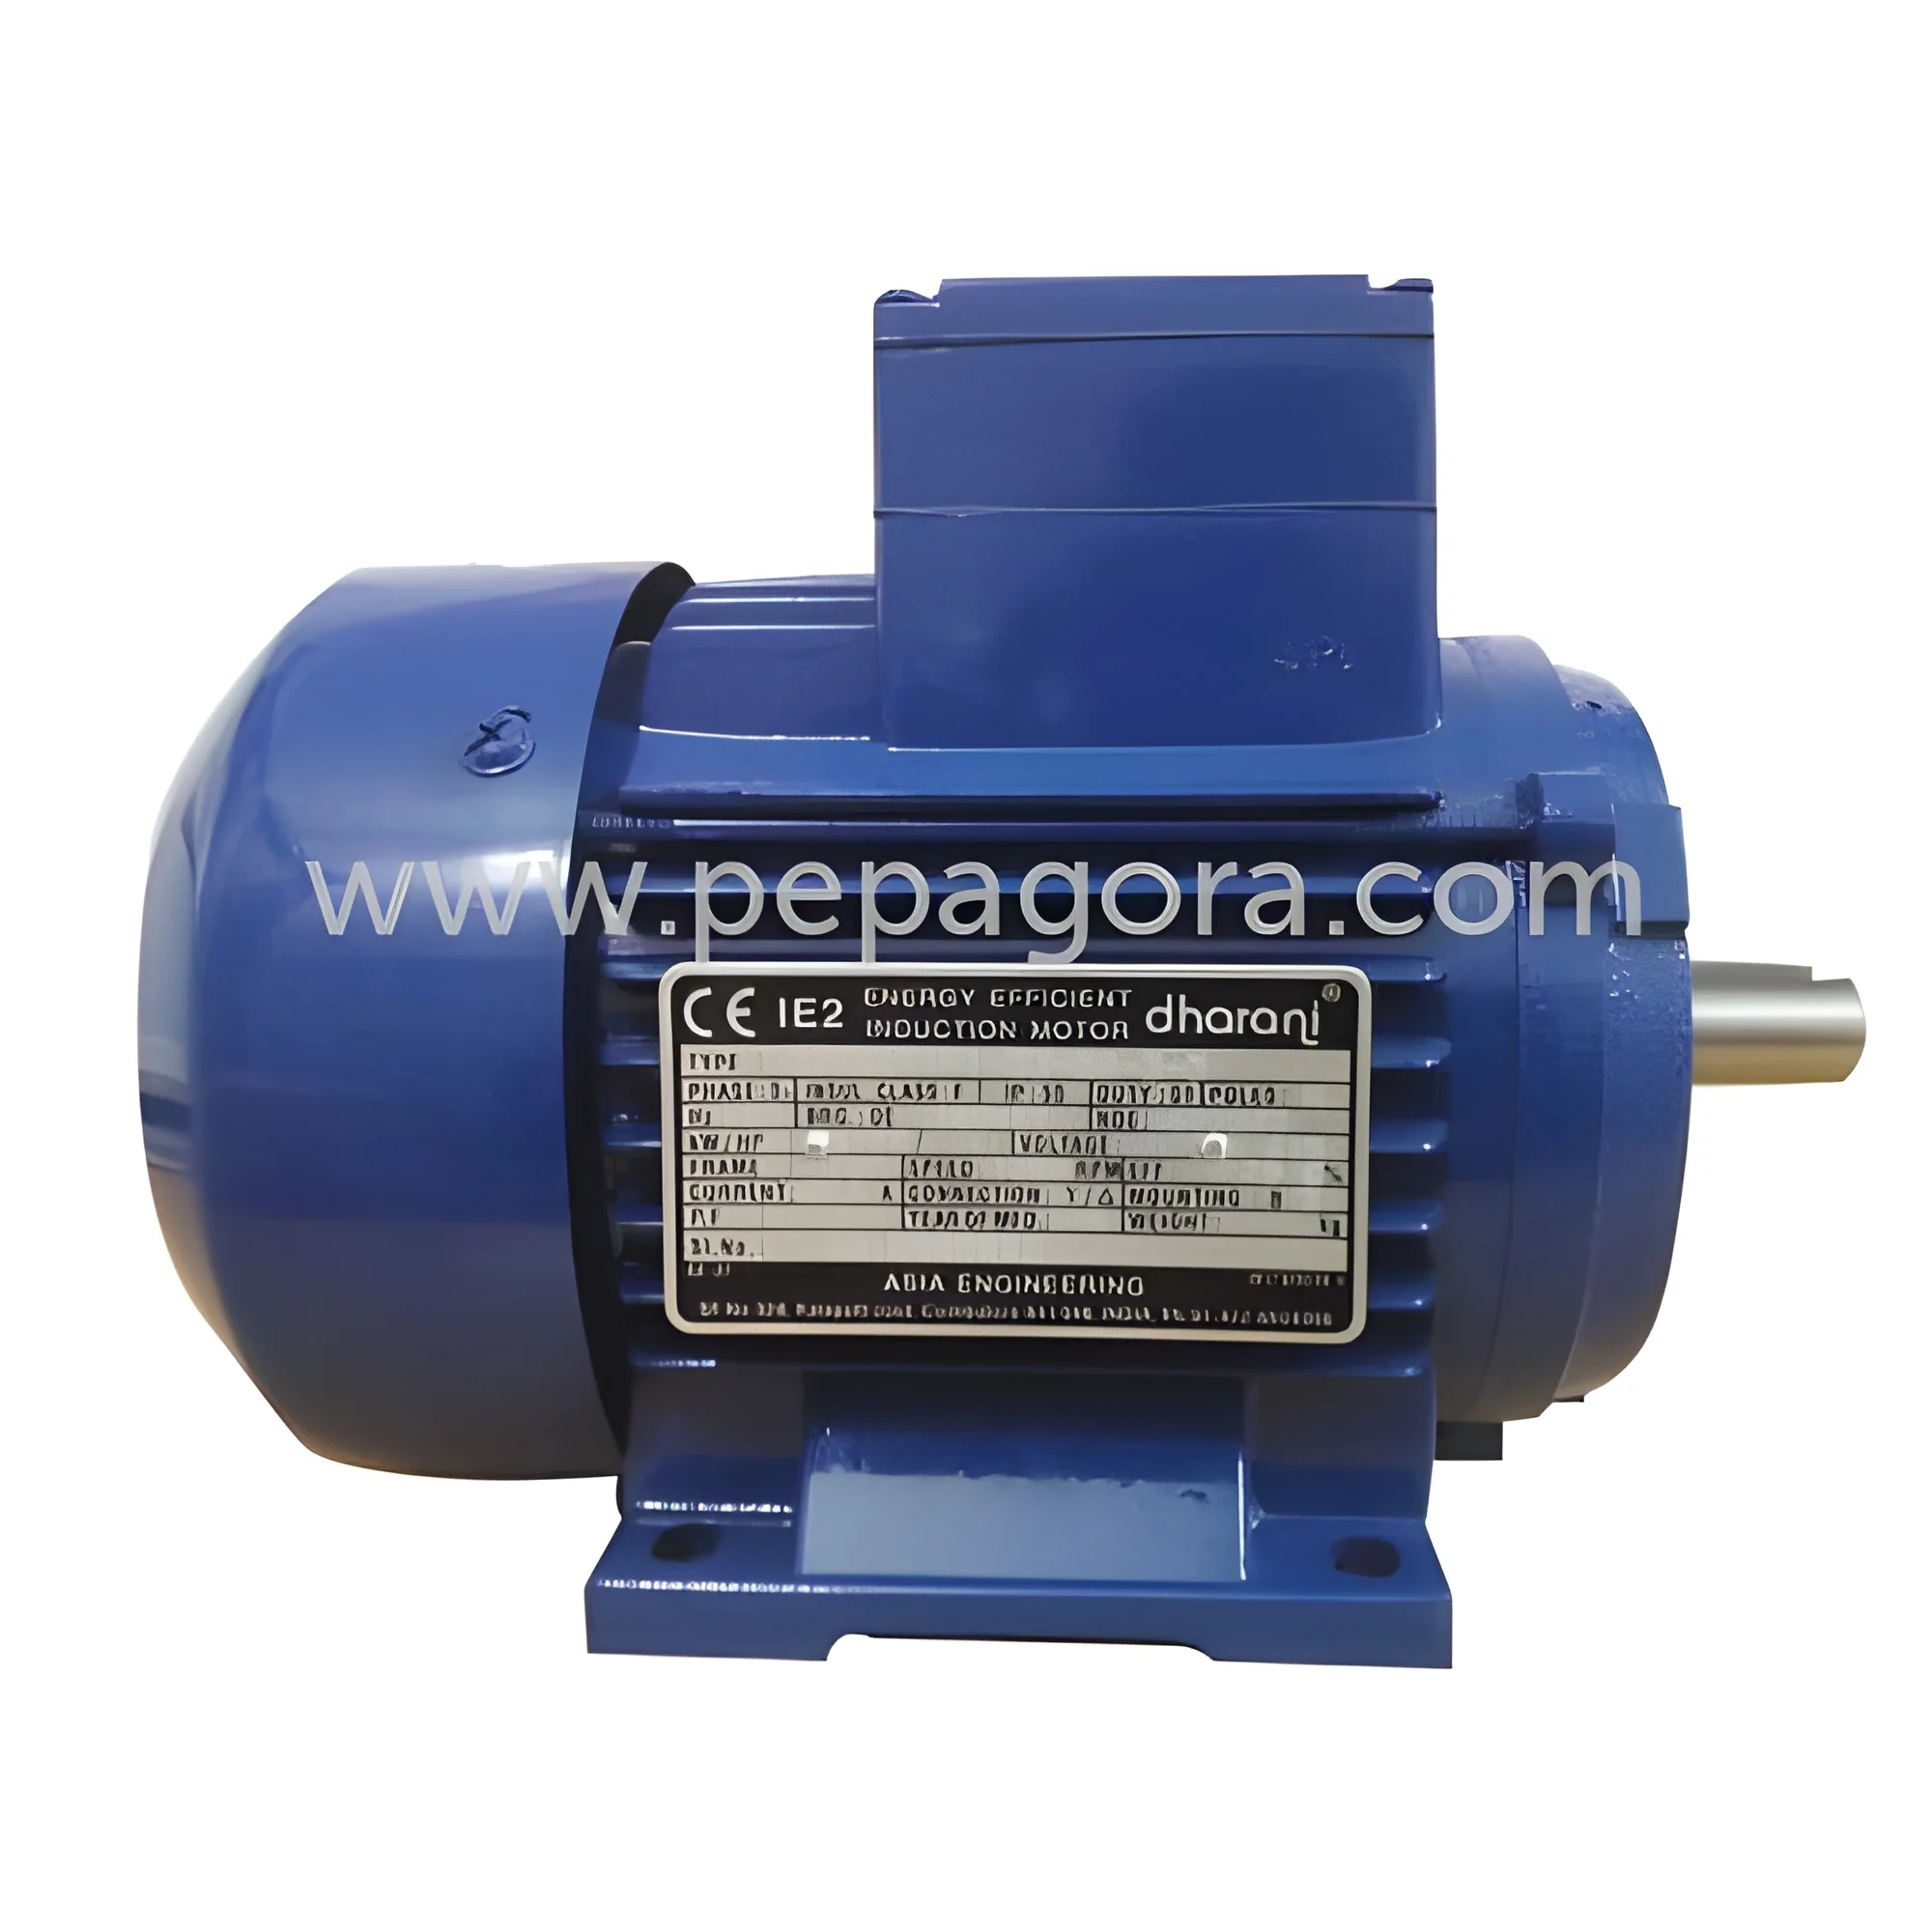
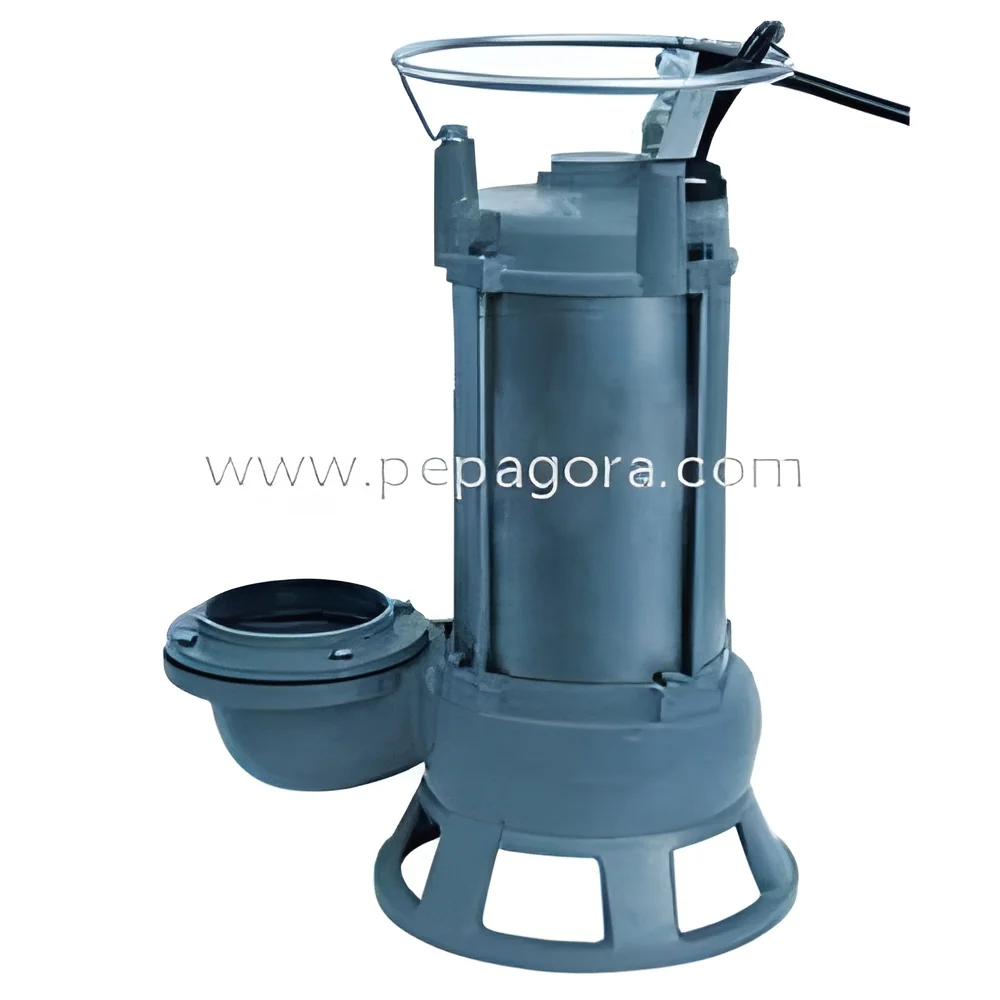
Our heavy-duty sludge pumps represent reliability in industrial fluid handling applications. Engineered with sturdy construction and precision manufacturing, these pumps are specifically designed to manage thick, abrasive slurries and viscous materials that would damage conventional pumping systems. Built to withstand demanding industrial environments, each pump undergoes quality testing to ensure optimal performance and longevity. The design allows for adaptation to specific operational requirements, ensuring integration into existing systems while delivering consistent flow rates and pressure maintenance. With OEM supply capabilities, we provide solutions that meet specifications for various challenging industrial applications.

These sludge pumps serve critical functions across multiple industries including mining, wastewater treatment, construction, and chemical processing. In mining operations, they efficiently handle tailings and abrasive slurry transfer from extraction processes...
Our heavy-duty sludge pumps represent reliability in industrial fluid handling applications. Engineered with sturdy construction and precision manufacturing, these pumps are specifically designed to manage thick, abrasive slurries and viscous materials that would damage conventional pumping systems. Built to withstand demanding industrial environments, each pump undergoes quality testing to ensure optimal performance and longevity. The design allows for adaptation to specific operational requirements, ensuring integration into existing systems while delivering consistent flow rates and pressure maintenance. With OEM supply capabilities, we provide solutions that meet specifications for various challenging industrial applications.

These sludge pumps serve critical functions across multiple industries including mining, wastewater treatment, construction, and chemical processing. In mining operations, they efficiently handle tailings and abrasive slurry transfer from extraction processes. Wastewater treatment facilities rely on them for moving settled solids and thick sludge through various treatment stages. Construction sites utilize these pumps for dewatering excavations and managing sediment-laden water during foundation work. Chemical plants employ them for transferring viscous byproducts and waste materials between processing units. The robust design ensures reliable performance across these diverse applications, making them essential equipment for operations dealing with challenging fluid handling requirements.

The business value of our sludge pumps extends beyond initial equipment cost to encompass long-term operational reliability and reduced maintenance expenses. Their sturdy construction minimizes downtime and repair costs, while the features ensure suitability for specific operational needs. The OEM supply model provides businesses with solutions that integrate into existing processes, enhancing overall operational efficiency. With negotiable pricing and guaranteed on-time delivery, we offer value proposition for businesses seeking reliable fluid handling solutions. The pumps ability to handle abrasive materials extends equipment lifespan and reduces replacement frequency, delivering cost savings over time while maintaining consistent performance in demanding industrial environments.

Key Features:
- Heavy-duty construction for handling abrasive slurries and viscous materials
- Specifications adaptable for specific operational requirements
- OEM supply capabilities for system integration
- Reliable performance with consistent flow rates and pressure maintenance
- Sturdy design built to withstand demanding industrial environments

Benefits:
- Reduced maintenance costs and minimized downtime
- Long operational lifespan with reliable performance
- Seamless integration into existing industrial processes
- Consistent handling of thick and abrasive materials
- Cost-effective solution for challenging fluid transfer applications
Specifications
| Key Attributes | |
|---|---|
| Type | Sludge Pump |
| Condition | New |
| Application | Industrial Applications |
| Supply Type | OEM |
| Feature | Sturdy construction |
| Price | Negotiable |
| Delivery | On Time Delivery |
| Dimension | Customized |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial sludge pumps are engineered to handle challenging abrasive and viscous materials across multiple sectors. The robust construction and reliable performance make them indispensable for operations where conventional pumps fail, ensuring continuous operation with minimal clogging and wear even with high-solid content slurries and thick industrial waste materials. These versatile pumps maintain consistent flow rates while withstanding demanding environments, providing dependable solutions for material transfer and waste management applications. Their specifications allow for adaptation to various industrial processes, making them ideal for OEM supply partnerships and tailored system integrations.
Real-world applications:
- Pumping mining tailings and abrasive slurry from extraction processes
- Handling wastewater treatment plant sludge and settled solids
- Transferring industrial byproducts and chemical plant waste materials
- Managing construction site dewatering and sediment removal operations
- Processing viscous fluids and abrasive mixtures in manufacturing plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Moto Drives, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Sludge Pump New OEM Sturdy Construction On Time Delivery
Industrial sludge pump with sturdy construction handles thick abrasive slurries for mining, wastewater, and chemical processing applications. OEM supply with reliable performance and on-time delivery.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Moto Drives
 Tamil Nadu, India
Electronics & ElectricalManufacturer