IN
₹

Description
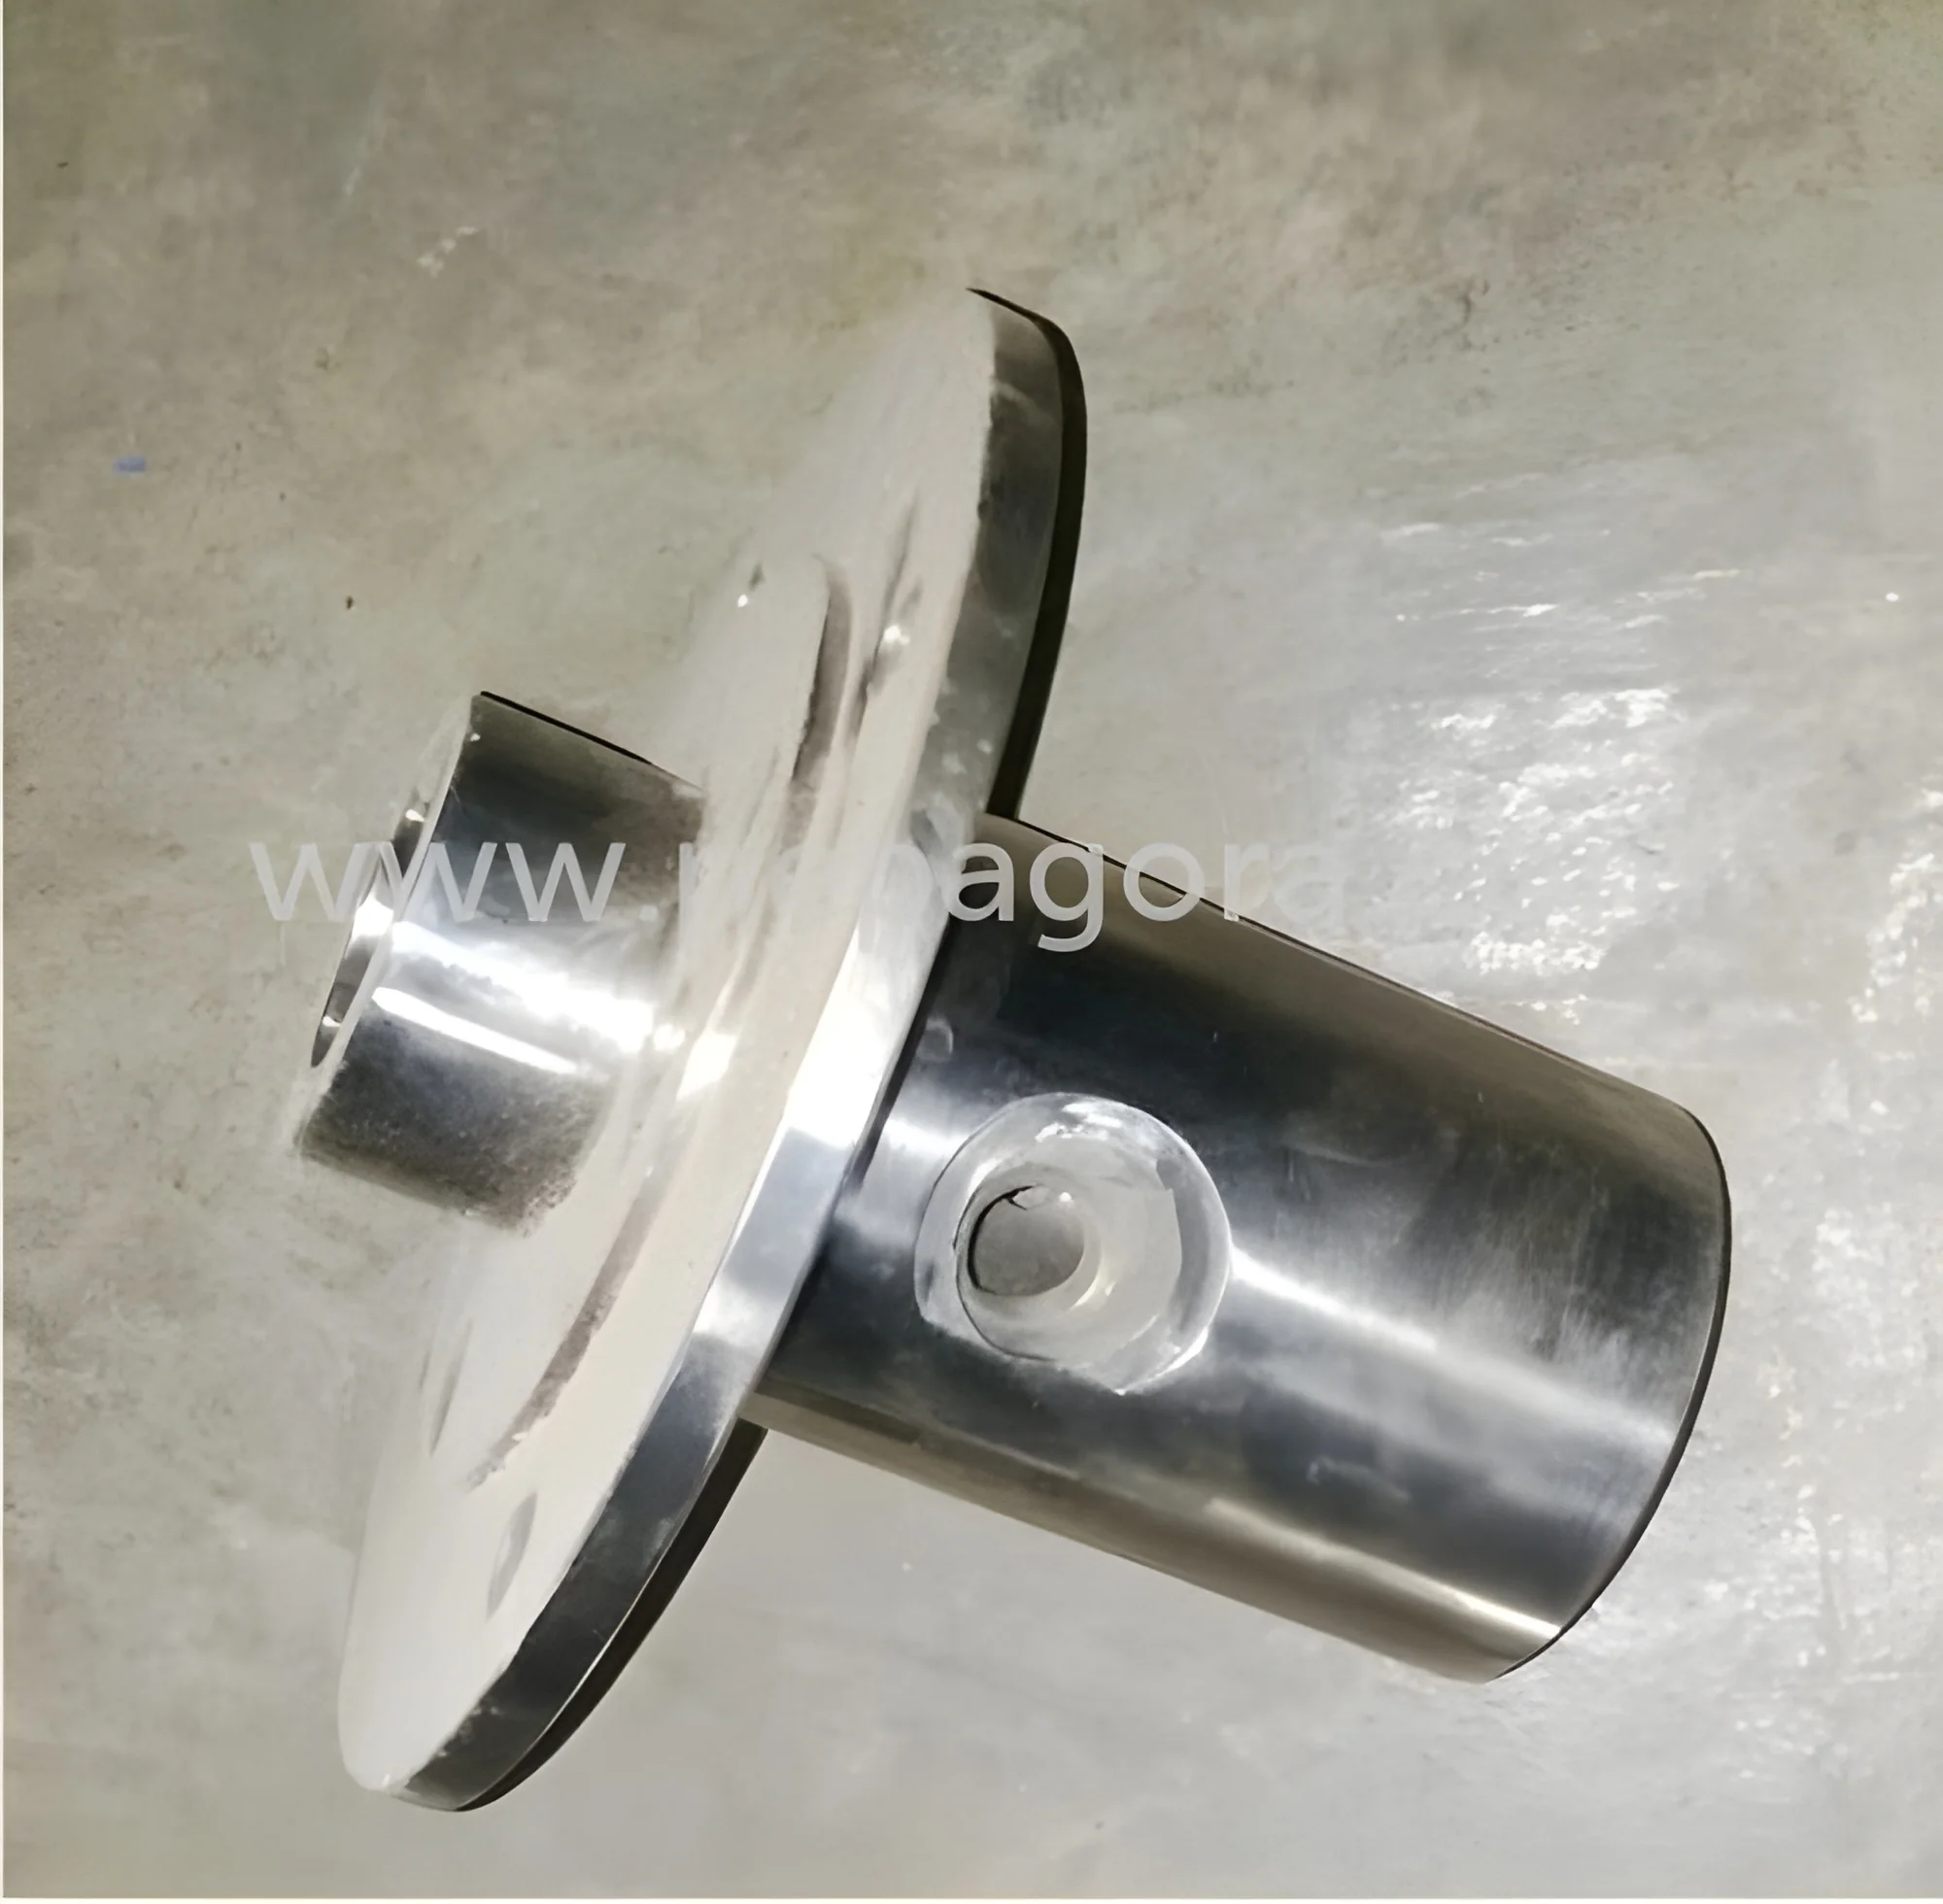
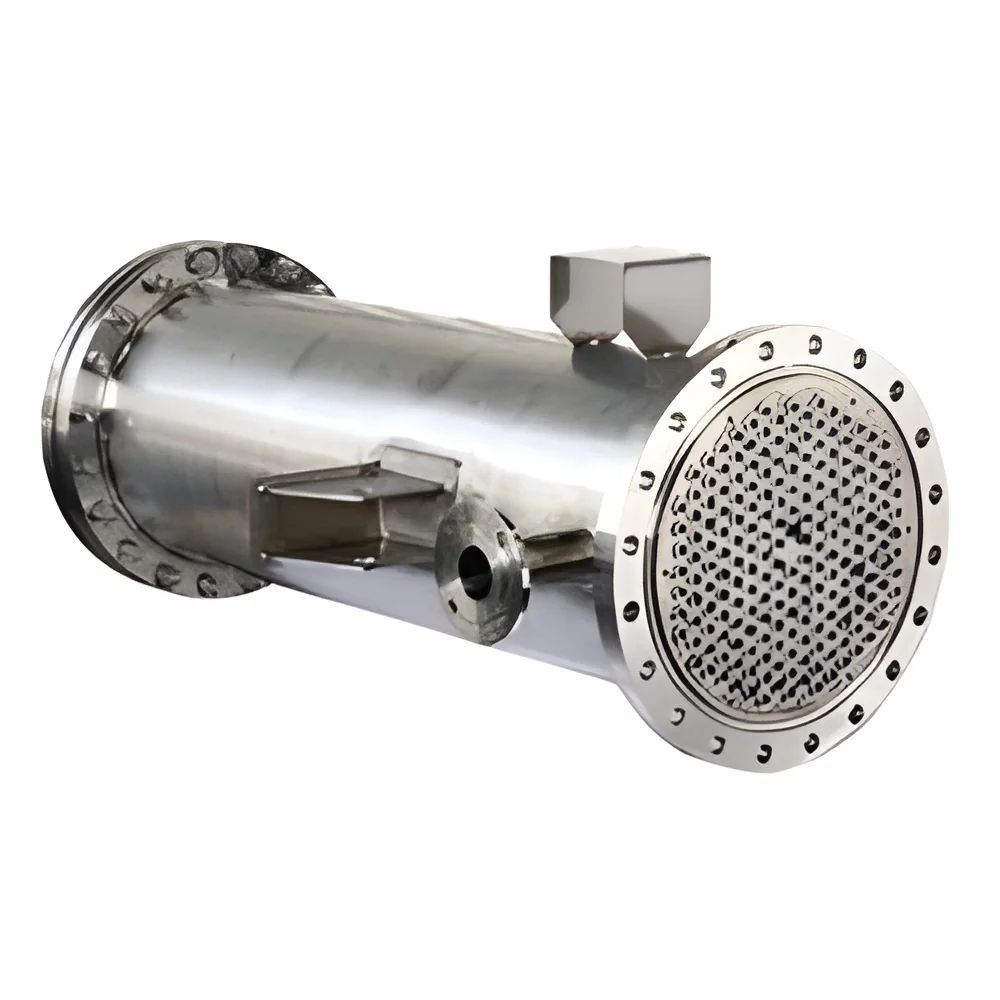
Our industrial shell and tube heat exchangers represent engineering excellence in thermal management solutions for demanding industrial applications. These units feature a classic design consisting of a bundle of tubes enclosed within a cylindrical shell, facilitating efficient heat transfer between two separate fluids. The parallel U-tube configuration allows for thermal expansion compensation while maintaining structural integrity under varying operating conditions. Manufactured using high-grade materials including carbon steel, stainless steel, and specialized alloys, our heat exchangers deliver reliable performance in challenging environments. Each unit undergoes rigorous quality checks to ensure compliance with industry standards and client specifications, providing dependable thermal management for continuous industrial operations.

These heat exchangers serve essential functions across numerous industrial sectors including chemical processing, oil and gas operations, power gener...
Our industrial shell and tube heat exchangers represent engineering excellence in thermal management solutions for demanding industrial applications. These units feature a classic design consisting of a bundle of tubes enclosed within a cylindrical shell, facilitating efficient heat transfer between two separate fluids. The parallel U-tube configuration allows for thermal expansion compensation while maintaining structural integrity under varying operating conditions. Manufactured using high-grade materials including carbon steel, stainless steel, and specialized alloys, our heat exchangers deliver reliable performance in challenging environments. Each unit undergoes rigorous quality checks to ensure compliance with industry standards and client specifications, providing dependable thermal management for continuous industrial operations.

These heat exchangers serve essential functions across numerous industrial sectors including chemical processing, oil and gas operations, power generation facilities, and manufacturing plants. In chemical processing facilities, they safely handle corrosive fluids and high-temperature processes while maintaining precise temperature control. Power generation plants utilize them for condenser systems and turbine cooling applications to ensure optimal equipment performance. The oil and gas industry depends on them for crude oil heating and product cooling circuits during refining operations. Manufacturing facilities integrate them into process heating and cooling systems for production efficiency, while HVAC applications benefit from their heat recovery capabilities in large commercial buildings, ensuring energy-efficient temperature management.

The operational value of our shell and tube heat exchangers lies in their proven reliability, energy efficiency, and extended service life. These units significantly reduce operational costs through optimized heat transfer efficiency and minimal maintenance requirements, delivering substantial savings over their operational lifespan. Their robust construction ensures continuous operation even under demanding conditions, minimizing production downtime and associated losses. The design flexibility allows for seamless integration into existing systems, while standardized components ensure straightforward maintenance and readily available replacement parts. These combined factors deliver exceptional return on investment through improved process efficiency, reduced energy consumption, and lower total cost of ownership for industrial operations.

Key Features:
- Parallel U-tube design for effective thermal expansion compensation
- High-grade material construction using carbon steel and stainless steel
- Configurable designs to meet specific industrial process requirements
- Robust shell construction suitable for high-pressure applications
- Optimized heat transfer surface design for maximum efficiency

Benefits:
- Enhanced operational reliability through durable construction and design
- Improved energy efficiency reducing overall operating costs
- Long service life with minimal maintenance requirements
- Flexible integration capabilities for various industrial systems
- Consistent performance under challenging operating conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Shell and tube heat exchangers provide critical temperature control in process industries where handling diverse fluids like water, oils, chemicals, and gases is essential. Their robust construction ensures reliable performance under high pressure and temperature conditions, making them ideal for continuous operation environments that demand consistent thermal management and operational stability across various industrial settings.
These versatile units serve multiple sectors including chemical processing, power generation, HVAC systems, and manufacturing plants. The modular design allows for adaptation to specific process requirements while maintaining durable construction for long-term reliability. Their configuration flexibility makes them suitable for both heating and cooling applications, ensuring optimal performance across different industrial operations and fluid handling needs.
- Chemical processing plants for reactor cooling and distillation column temperature control
- Power generation facilities for turbine lube oil cooling and condenser water systems
- HVAC installations in commercial buildings for efficient heat recovery operations
- Refinery operations for crude oil heating and petroleum product cooling circuits
- Food processing plants for pasteurization systems and process heating applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bhakti Engineering, Gujarat
 Gujarat, India
Food & Agriculture•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Shell And Tube Heat Exchangers For Efficient Fluid Heating Cooling
Industrial shell and tube heat exchangers deliver efficient fluid heating and cooling with robust U-tube designs for superior thermal performance in demanding industrial applications, ensuring reliable operation across various sectors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bhakti Engineering
 Gujarat, India
Food & AgricultureManufacturer