IN
₹
Apparel & Fashion
Description
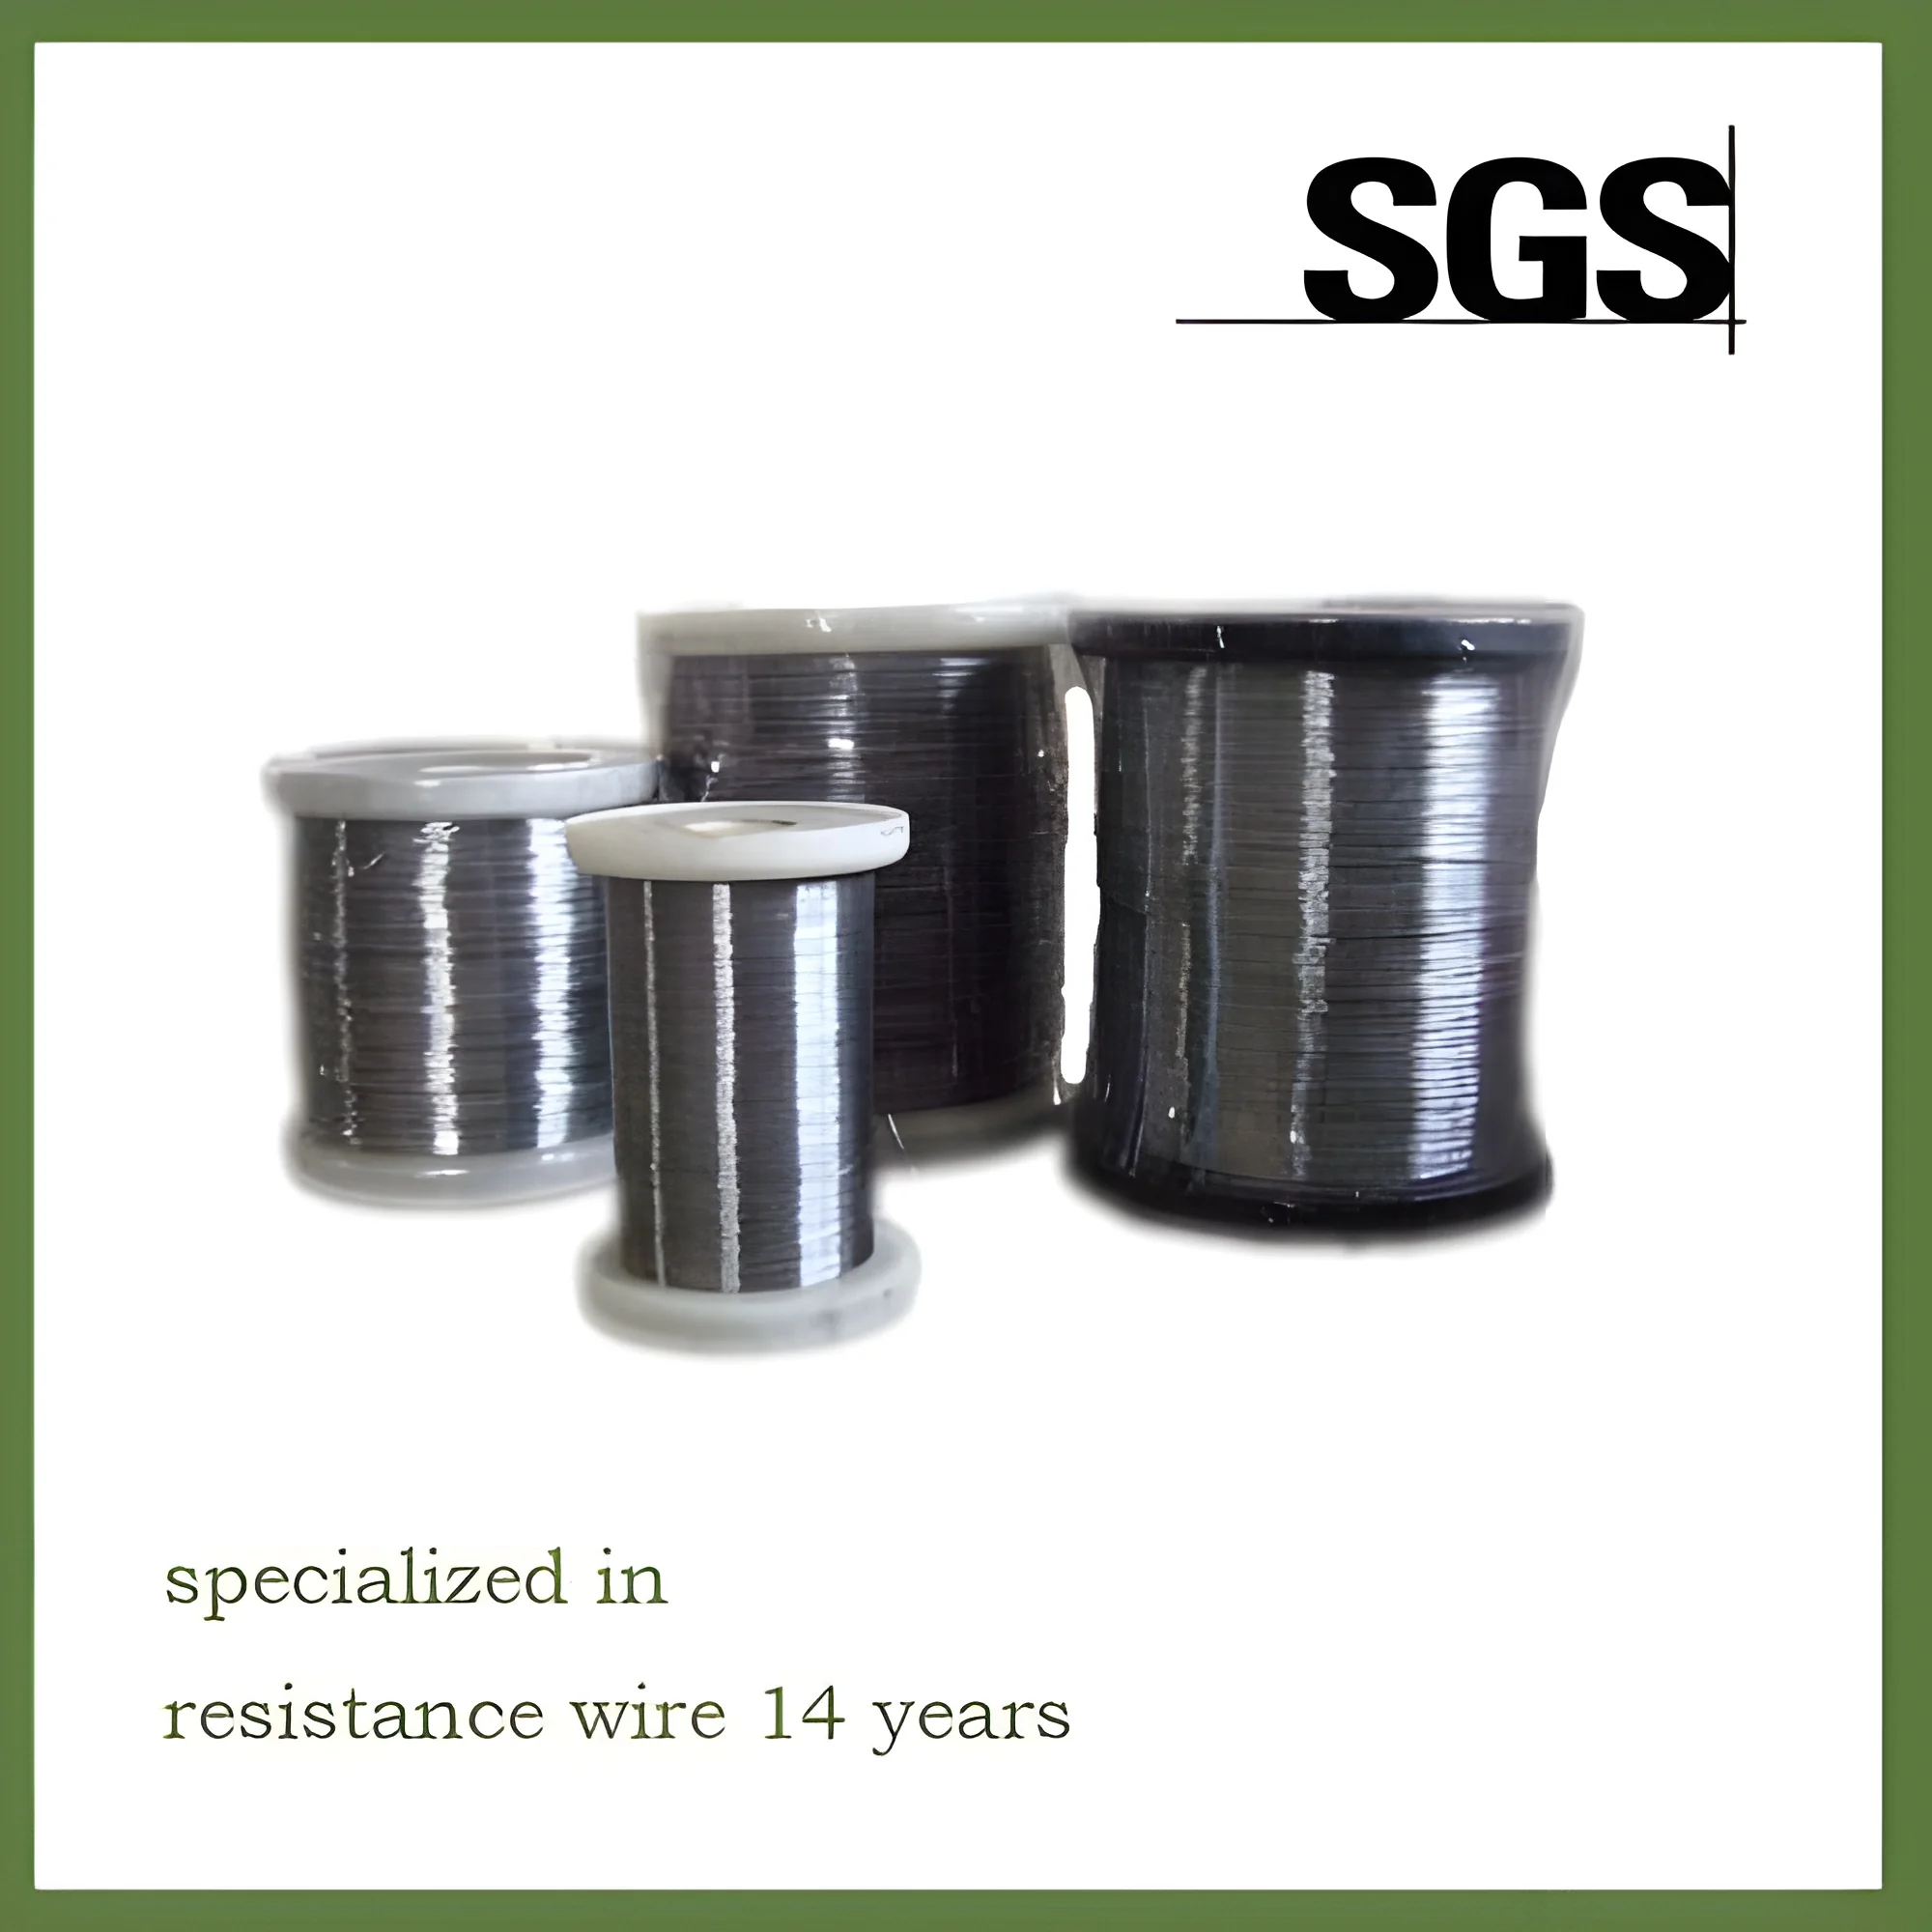
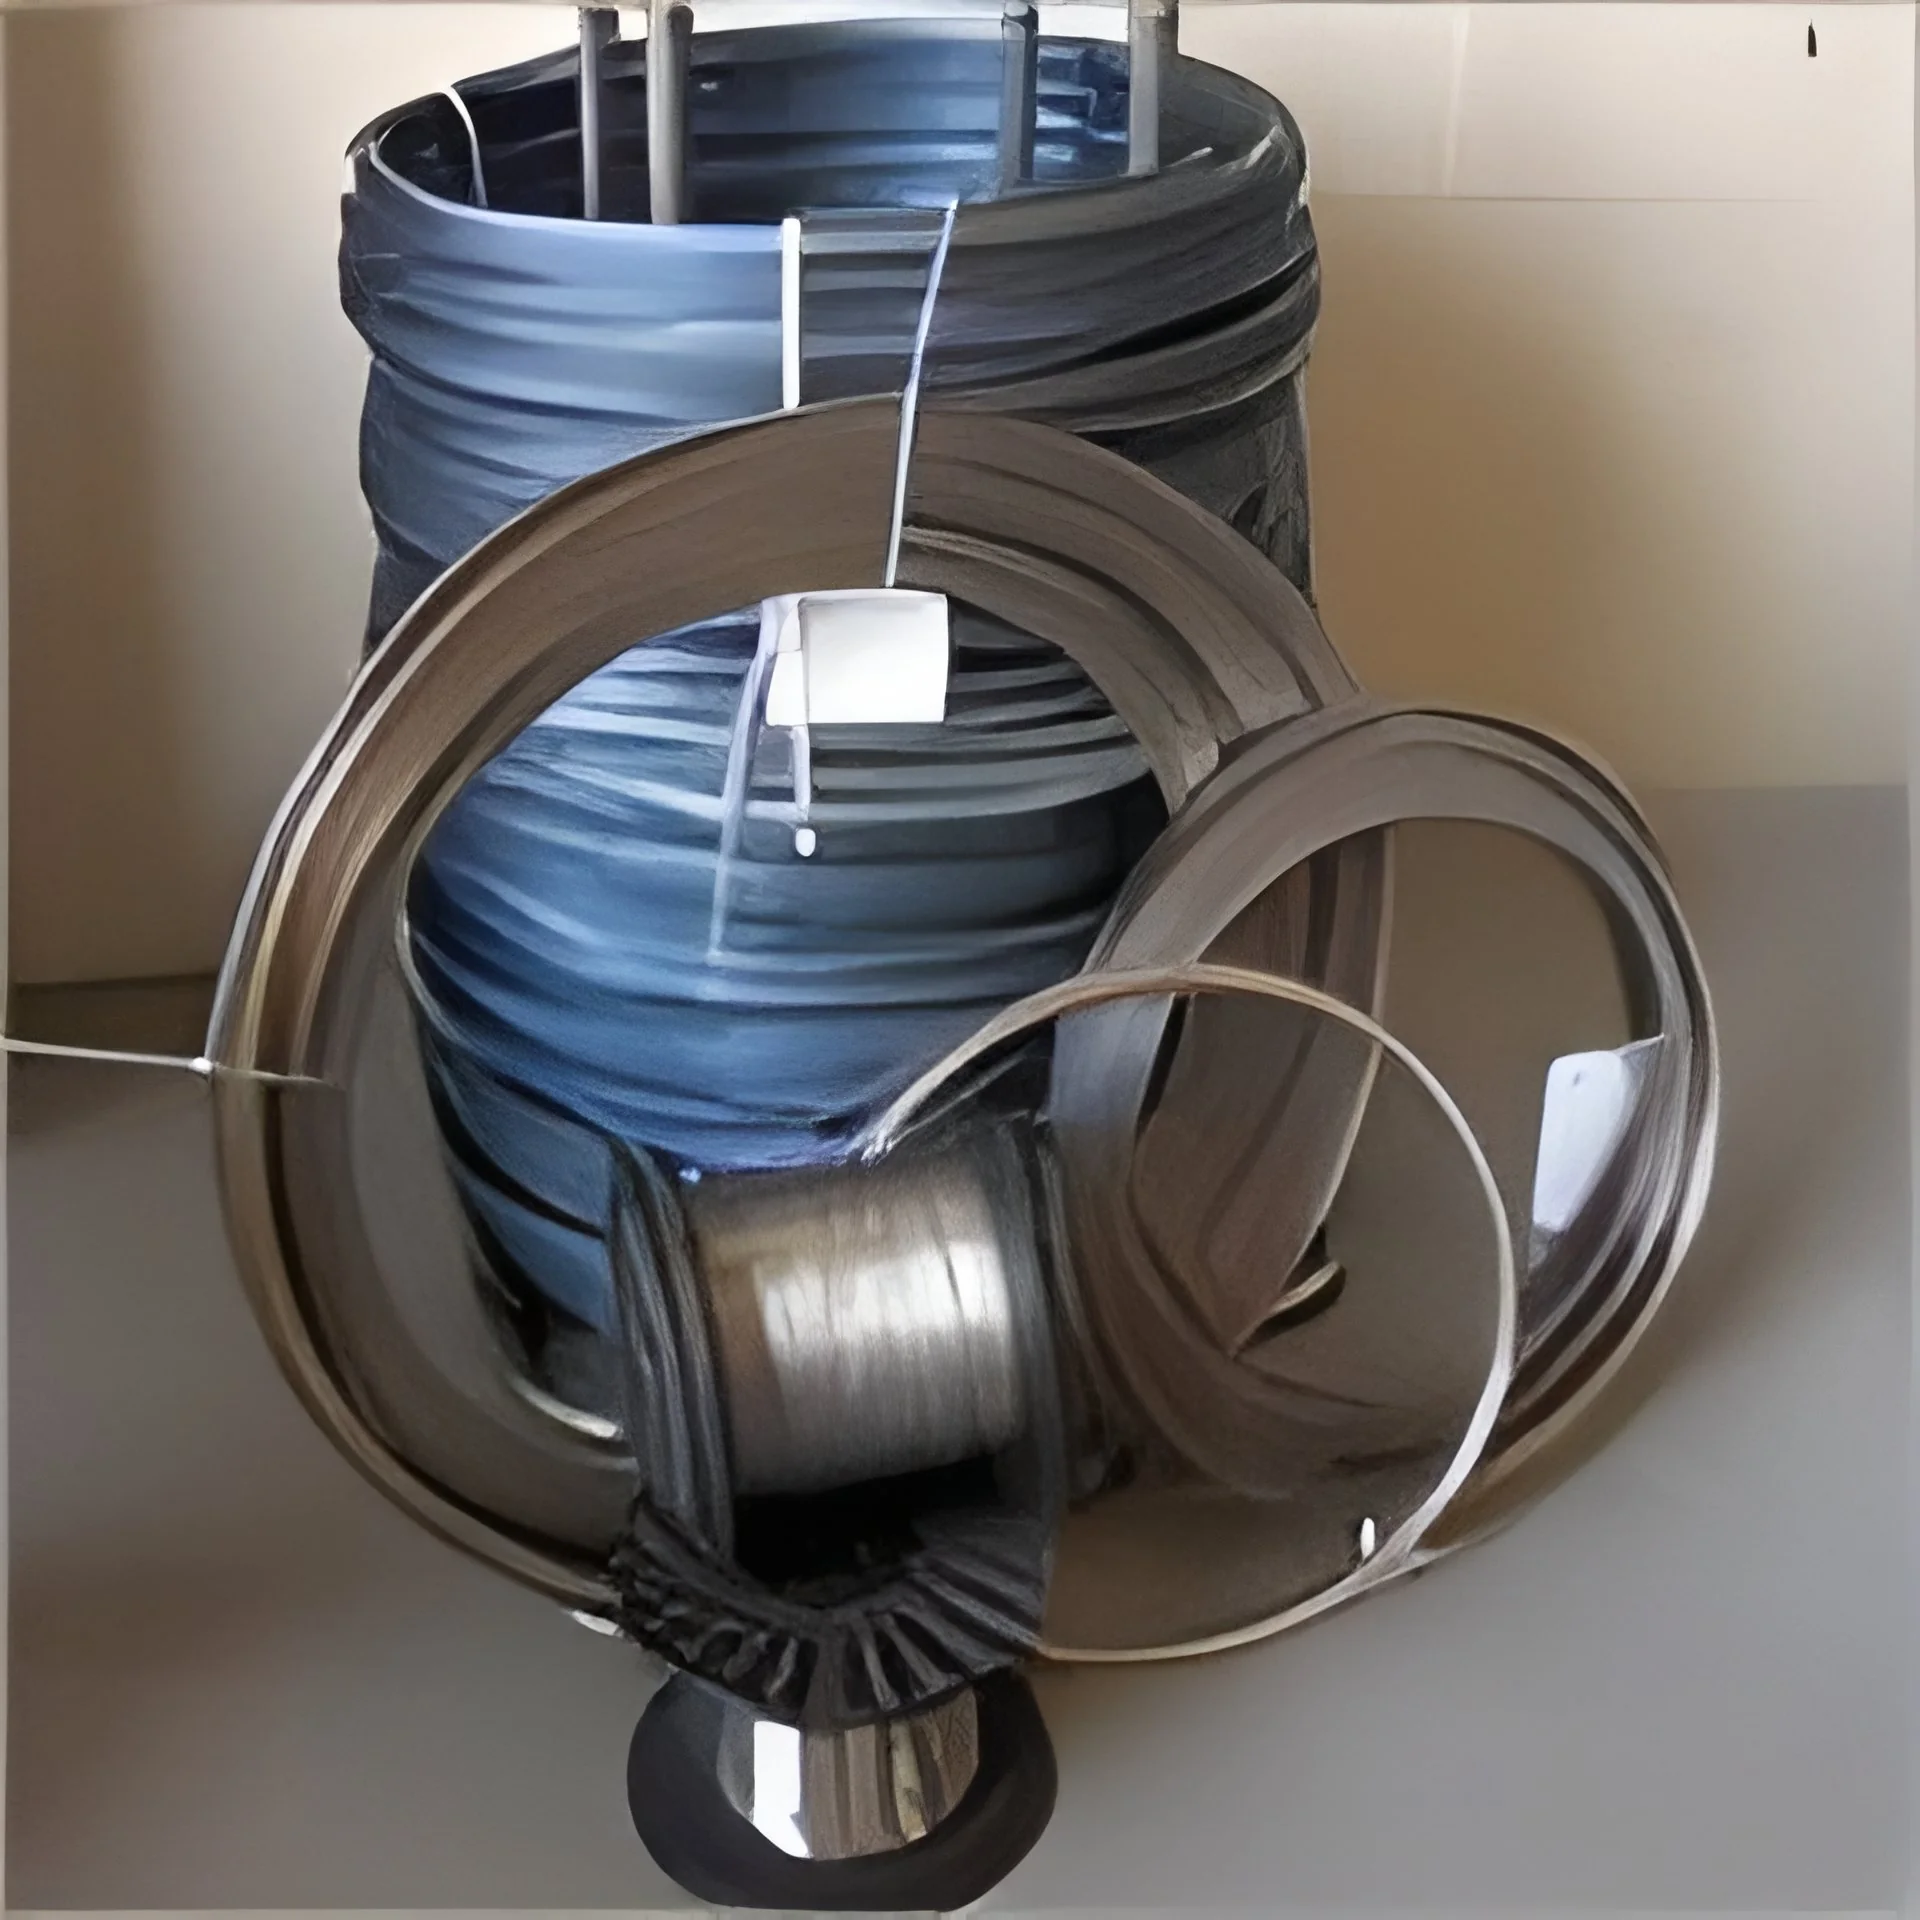
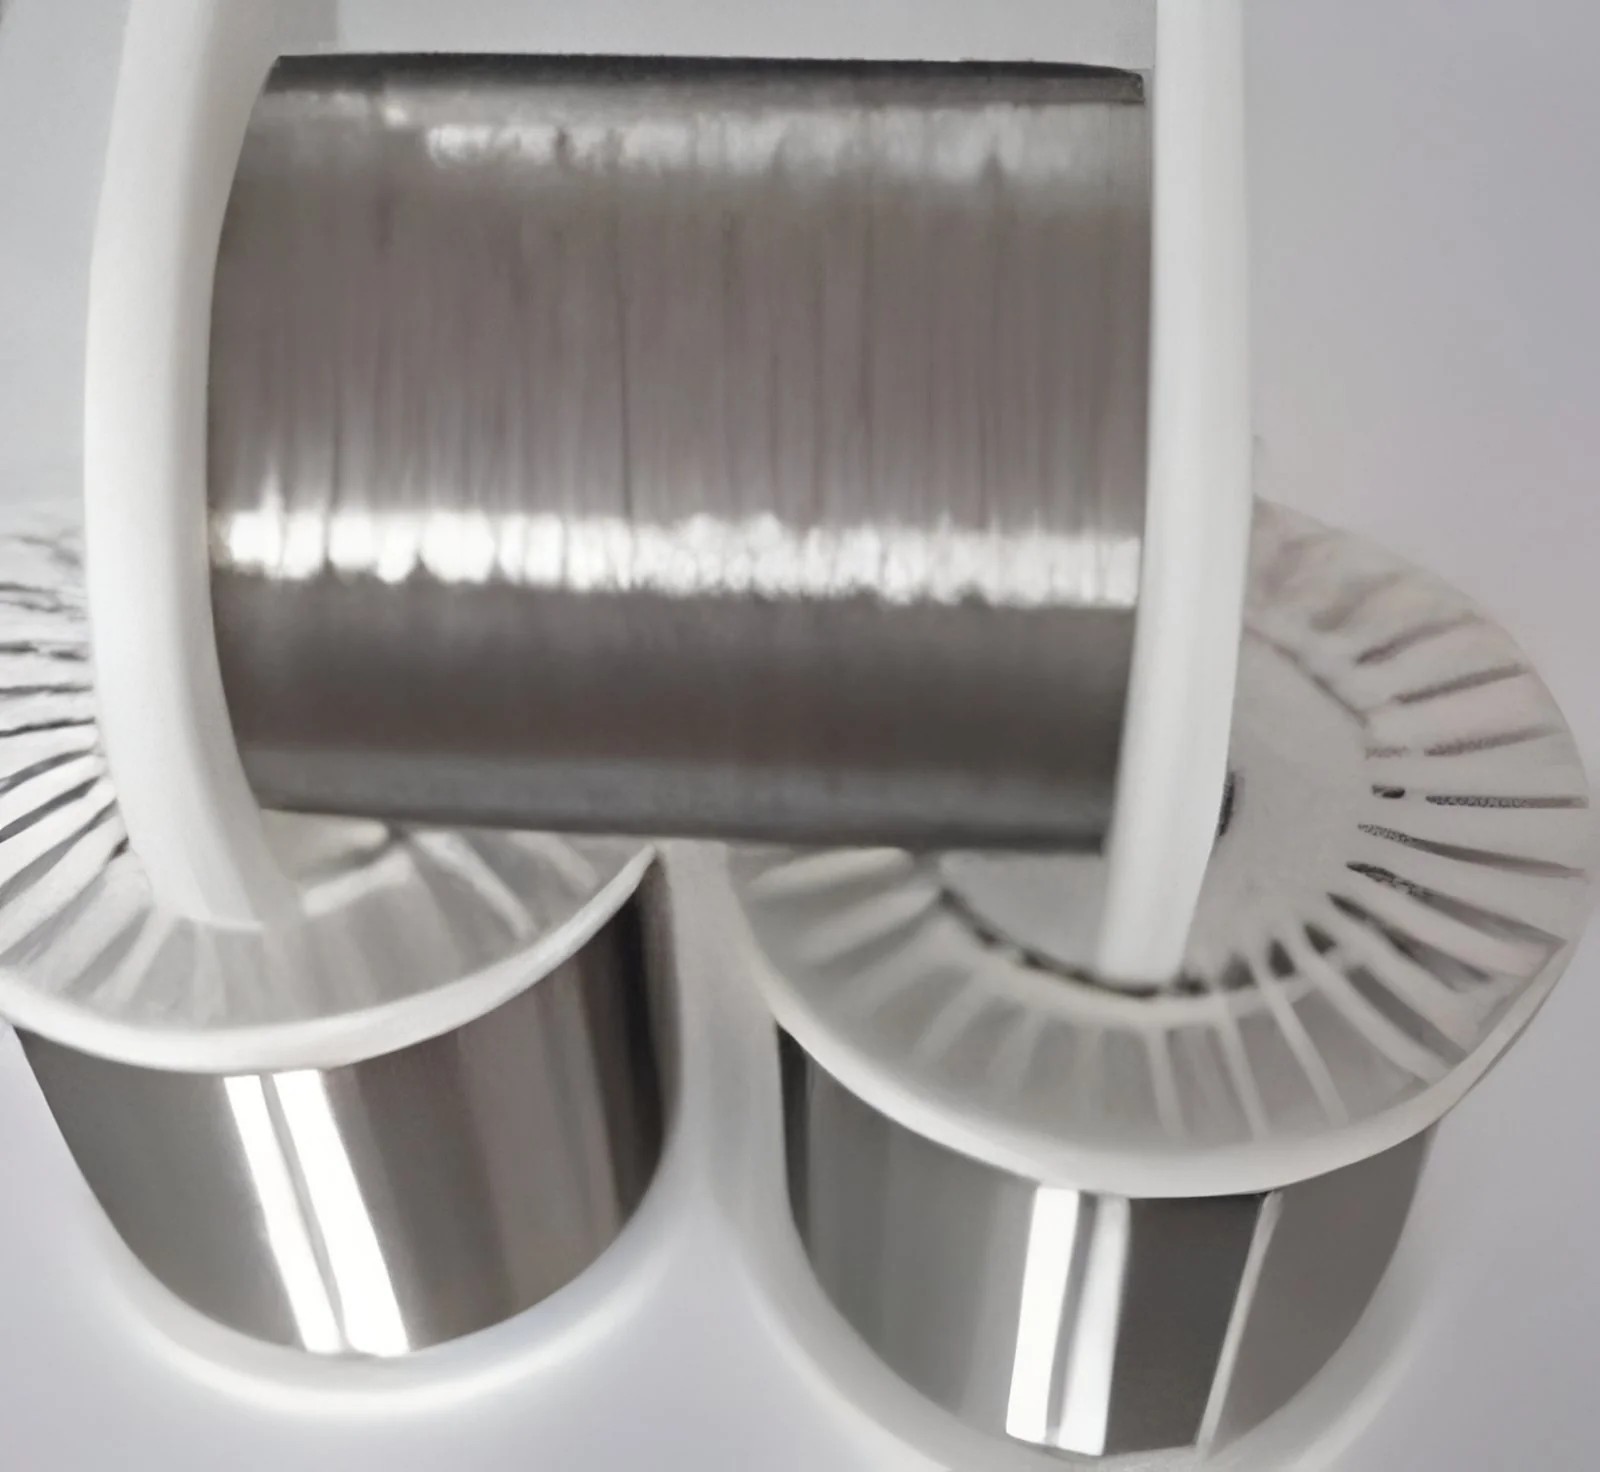
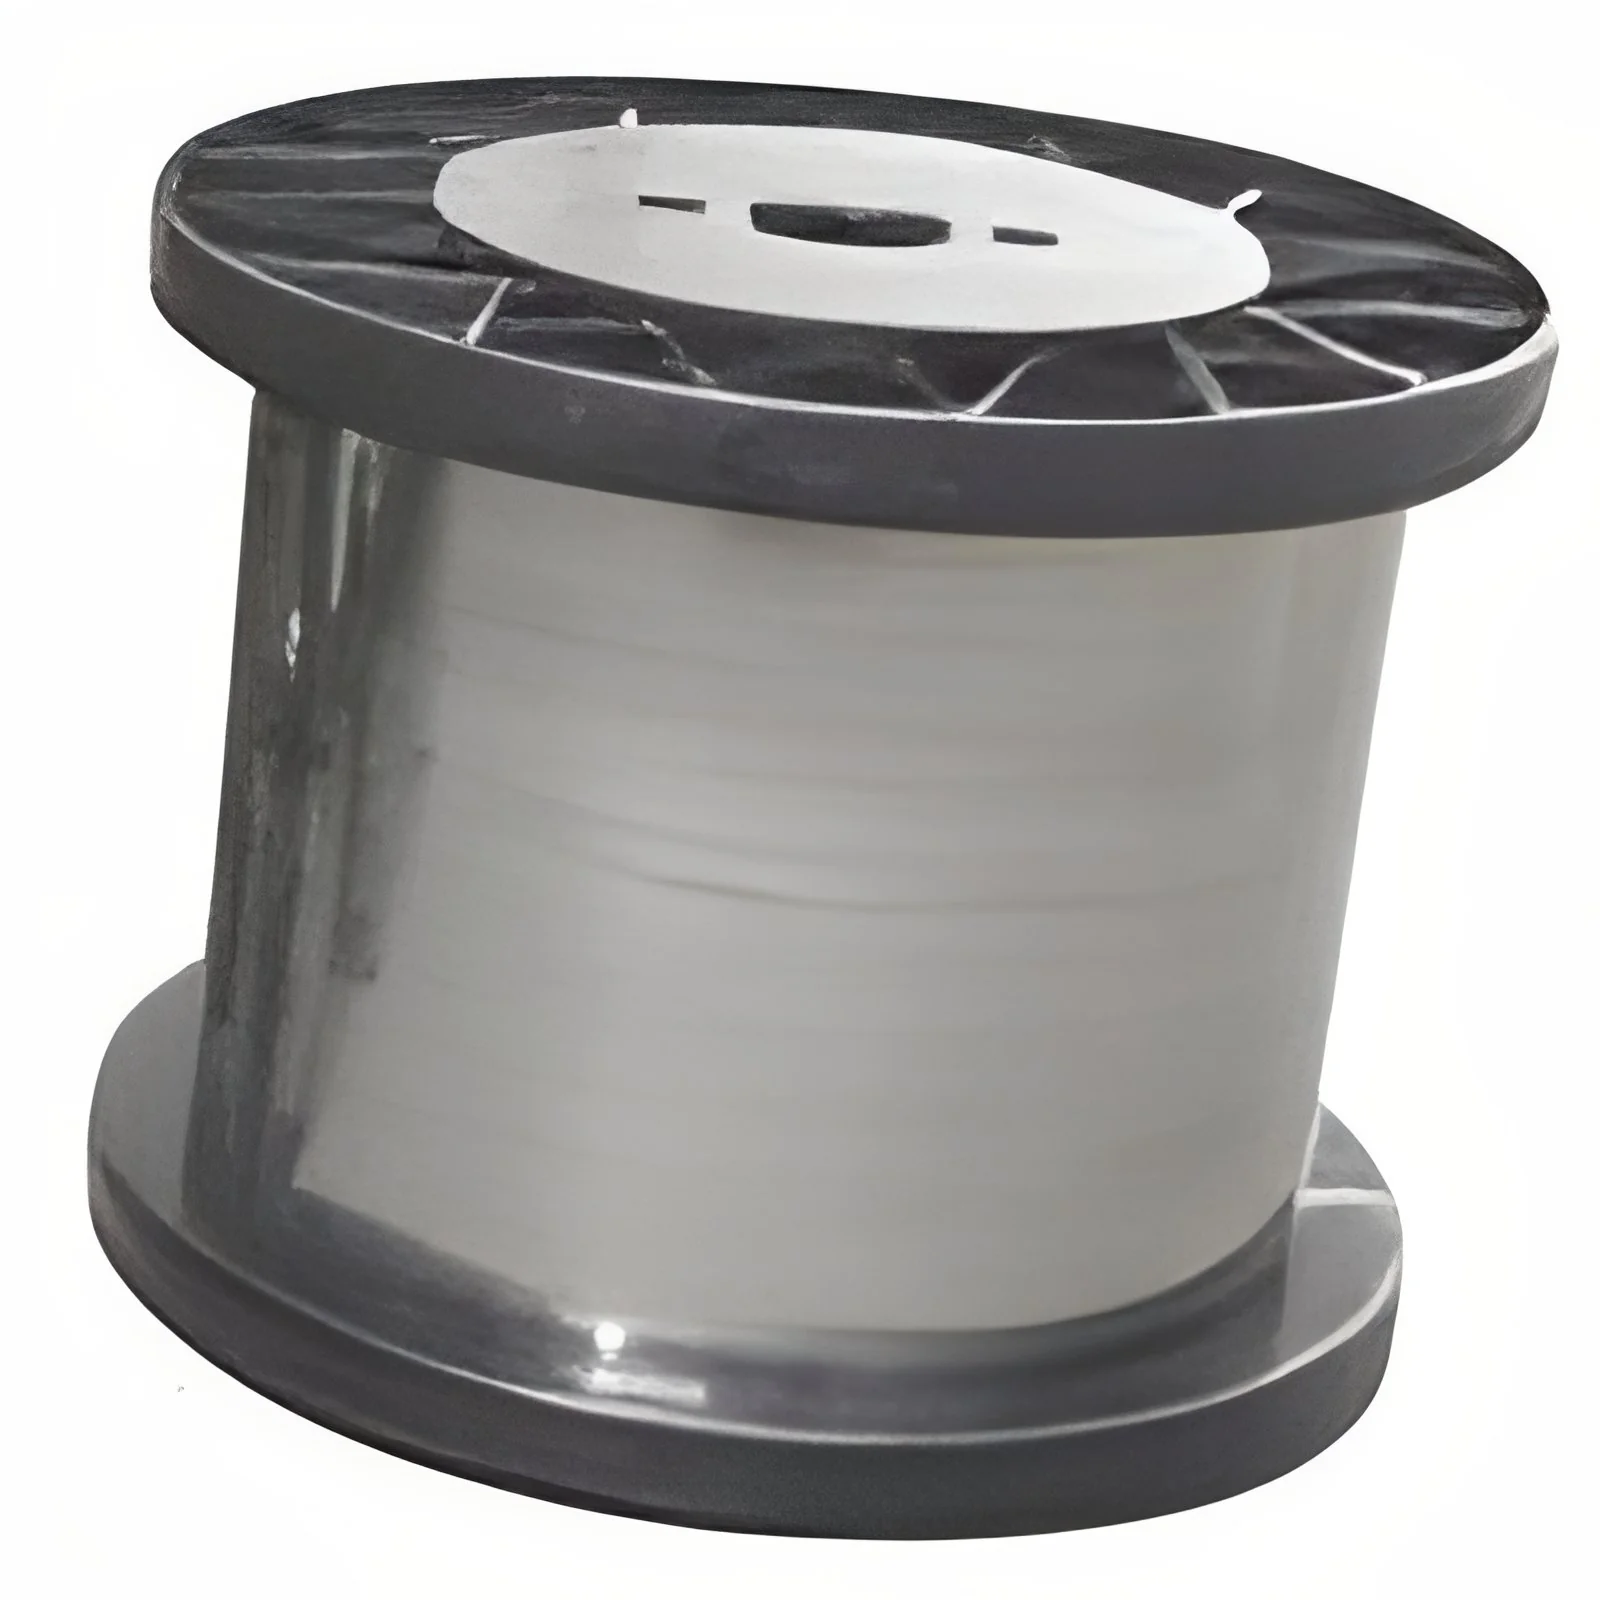
Our FeCrAl alloy resistance wire represents a premium solution for high-temperature industrial heating applications, specifically designed to withstand extreme thermal conditions while maintaining consistent electrical performance. This advanced alloy combines iron, chromium, and aluminum to create a wire that offers exceptional durability and reliability in temperatures up to 1400°C. The material's unique composition provides excellent oxidation resistance, ensuring long service life even in demanding atmospheric conditions where conventional resistance wires would deteriorate quickly. This makes it the preferred choice for applications involving repeated heating and cooling cycles where operational reliability is absolutely essential for maintaining production efficiency and product quality.

This resistance wire serves critical functions across multiple industrial sectors including manufacturing, automotive, electronics, and specialized equipment production. Industrial furnace manuf...
Our FeCrAl alloy resistance wire represents a premium solution for high-temperature industrial heating applications, specifically designed to withstand extreme thermal conditions while maintaining consistent electrical performance. This advanced alloy combines iron, chromium, and aluminum to create a wire that offers exceptional durability and reliability in temperatures up to 1400°C. The material's unique composition provides excellent oxidation resistance, ensuring long service life even in demanding atmospheric conditions where conventional resistance wires would deteriorate quickly. This makes it the preferred choice for applications involving repeated heating and cooling cycles where operational reliability is absolutely essential for maintaining production efficiency and product quality.

This resistance wire serves critical functions across multiple industrial sectors including manufacturing, automotive, electronics, and specialized equipment production. Industrial furnace manufacturers utilize it for heating elements that require consistent thermal output and extended operational life without degradation. The automotive industry incorporates it into various heating components and sensor systems, while electronics manufacturers rely on its stable resistance properties for precision heating applications. Equipment producers value its consistent performance in testing environments and thermal management systems where material failure is not an option. The wire's versatility and reliability make it suitable for diverse high-temperature applications across different industries, supporting efficient production processes and quality outcomes.

Businesses choose our FeCrAl alloy wire for its proven reliability and operational efficiency, delivering significant value through reduced maintenance requirements and extended service intervals. The wire's superior surface load capacity ensures optimal performance in critical heating applications while minimizing energy consumption and operational costs. Its exceptional oxidation resistance properties translate to longer operational life and reduced downtime, providing manufacturers with a dependable solution that enhances production efficiency and product consistency. The material's stable electrical resistance maintains precision in temperature control applications, ensuring repeatable results and reducing quality control issues. This reliability translates to lower total cost of ownership and improved operational performance for businesses relying on high-temperature heating solutions.

Key Features:
- Excellent oxidation resistance for extended service life in high-temperature environments
- High surface load capacity for optimal heating performance and efficiency
- Stable electrical properties maintained under extreme temperature conditions
- Structural integrity preserved up to 1400°C for reliable operation
- Consistent performance through repeated heating and cooling cycles

Benefits:
- Reduced maintenance requirements and extended operational life
- Consistent thermal output for improved product quality and process control
- Energy-efficient performance through optimal surface load capacity
- Reliable operation in demanding industrial environments
- Lower total cost of ownership through durable construction
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This FeCrAl alloy resistance wire is engineered for demanding industrial heating applications where consistent thermal output and material longevity are critical. Its superior oxidation resistance and stable electrical properties ensure reliable operation in extreme temperature environments up to 1400°C, making it ideal for continuous industrial processes where conventional materials would degrade rapidly. The wire maintains structural integrity through repeated heating cycles, providing manufacturers with a dependable solution for precision heating requirements across various sectors.
Industrial manufacturers rely on this high-grade resistance wire for applications requiring precise temperature control and extended operational life. Its excellent surface load capacity and thermal stability make it suitable for critical heating systems in manufacturing, processing, and equipment production. The alloy's composition ensures consistent performance in atmospheric conditions where other materials fail, supporting efficient production processes and reducing maintenance requirements. This reliability translates to improved operational efficiency and product quality for businesses using high-temperature heating solutions.
- Heating elements for industrial furnaces and thermal processing equipment
- Electrical components in manufacturing and production machinery
- Automotive industry applications including sensors and heating systems
- Laboratory and testing equipment requiring precise temperature control
- Thermal management systems in specialized industrial equipment
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
ALF Heaters Manufacturing, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Southeast Asia
Industrial Heating FeCrAl Alloy Resistance Wire High Temperature
Premium FeCrAl alloy resistance wire for high-temperature industrial heating elements and electrical components, offering excellent oxidation resistance, long service life, and high surface load capacity for reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ALF Heaters Manufacturing
 Maharashtra, India
Industrial Equipment & MachineryManufacturer