IN
₹
Apparel & Fashion
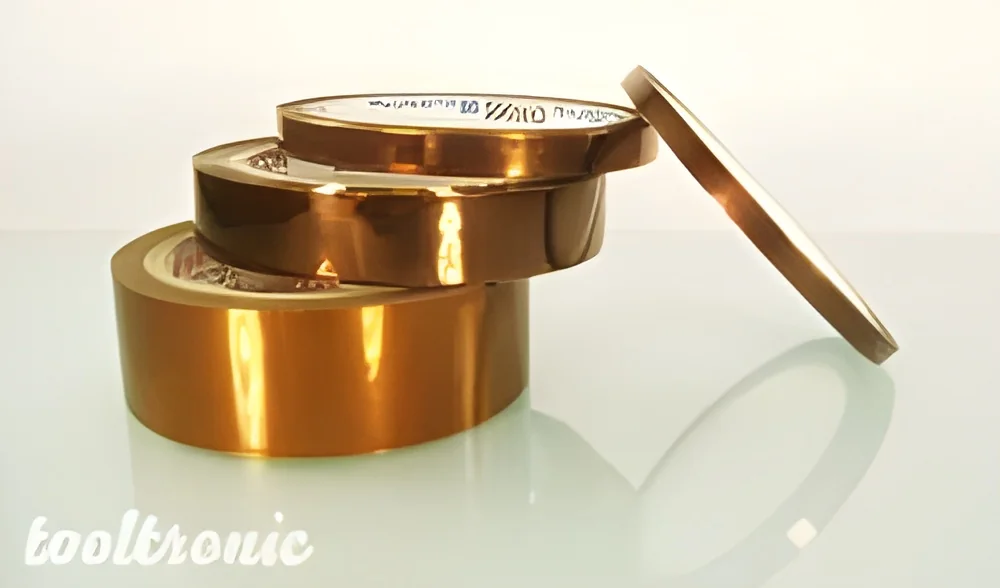
Description
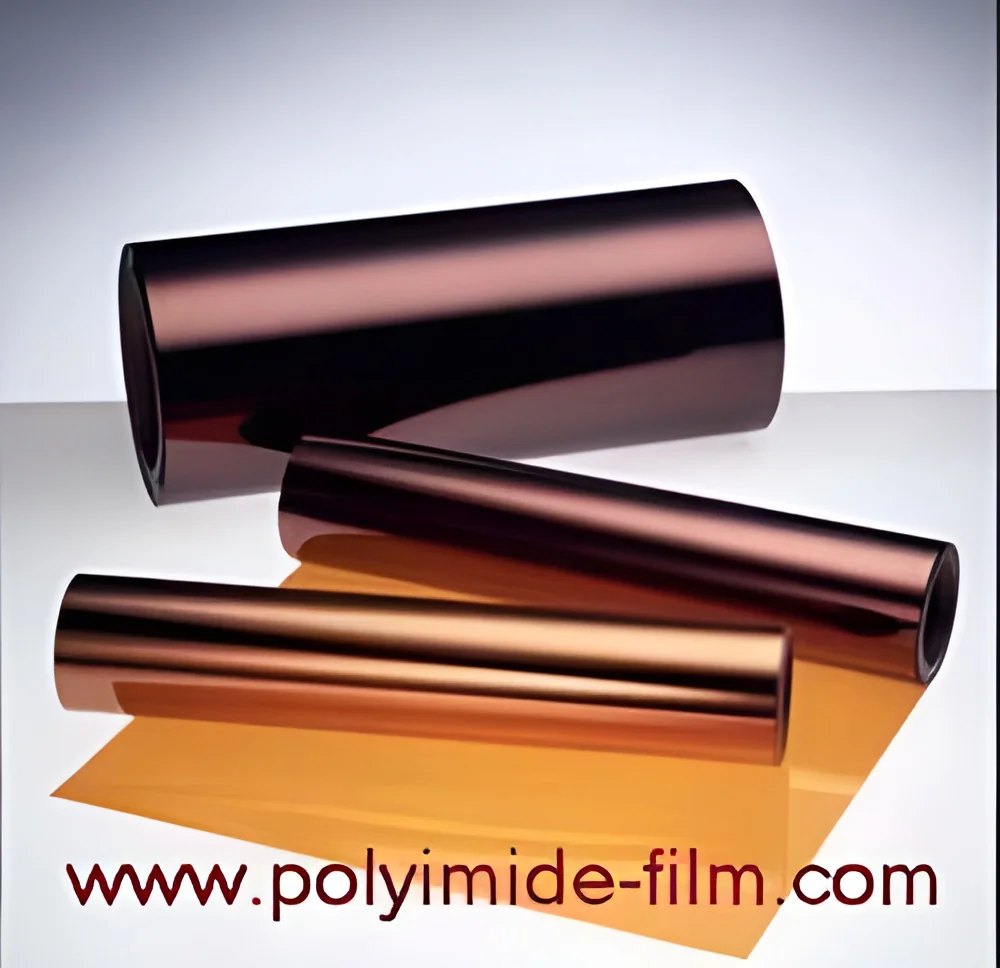
High Temperature Polyimide Kapton Film represents a premium polymer solution engineered for extreme environment applications where conventional materials cannot perform. This advanced material maintains exceptional stability across an impressive temperature spectrum from -269°C to 400°C, delivering superior dielectric strength with minimal thermal expansion characteristics. The film demonstrates inherent flame-resistant properties while exhibiting excellent resistance to chemicals, radiation, and mechanical wear. These combined attributes establish Kapton as the preferred choice for critical applications where reliability and performance cannot be compromised. The material's flexibility and durability enable utilization in dynamic systems, while consistent quality ensures dependable performance across diverse industrial requirements and challenging operational conditions.

Multiple industries depend on Polyimide Kapton for its unmatched performance characteristics in demanding applicat...
High Temperature Polyimide Kapton Film represents a premium polymer solution engineered for extreme environment applications where conventional materials cannot perform. This advanced material maintains exceptional stability across an impressive temperature spectrum from -269°C to 400°C, delivering superior dielectric strength with minimal thermal expansion characteristics. The film demonstrates inherent flame-resistant properties while exhibiting excellent resistance to chemicals, radiation, and mechanical wear. These combined attributes establish Kapton as the preferred choice for critical applications where reliability and performance cannot be compromised. The material's flexibility and durability enable utilization in dynamic systems, while consistent quality ensures dependable performance across diverse industrial requirements and challenging operational conditions.

Multiple industries depend on Polyimide Kapton for its unmatched performance characteristics in demanding applications. The aerospace sector utilizes this material extensively for wiring insulation, thermal blankets, and satellite components where lightweight properties and radiation resistance are essential. Automotive manufacturers incorporate Kapton in electric vehicle battery insulation, motor systems, and under-hood applications where elevated temperatures are consistently present. Electronics producers integrate this film into flexible circuits, printed circuit boards, and semiconductor processing equipment for its excellent dielectric properties and thermal management capabilities. Additionally, the energy sector employs Kapton in solar panels, wind turbines, and nuclear facilities where insulation and protection against harsh environmental conditions are necessary for sustained operation.

The business value of Polyimide Kapton film lies in its capacity to enhance product longevity, reduce operational downtime, and improve safety standards in critical applications. Its proven reliability ensures consistent performance under extreme stress conditions, significantly minimizing failure risks and associated costs. For procurement professionals, this translates to reduced total cost of ownership, increased operational efficiency, and compliance with rigorous industry standards. The material's consistent quality allows businesses to meet specific technical requirements effectively, providing competitive advantages in markets demanding precision and durability. By selecting Kapton, companies invest in a verified solution that supports innovation, sustainability, and long-term operational success across various industrial applications.

Key Features:
- Exceptional thermal stability maintaining performance from -269°C to 400°C
- High dielectric strength with excellent electrical insulation capabilities
- Superior chemical resistance against oils, solvents, and acidic compounds
- Inherent flame resistance with self-extinguishing characteristics
- Consistent quality and reliable performance across all production batches

Benefits:
- Enhanced product longevity and reduced maintenance requirements
- Improved safety standards in high-temperature applications
- Reduced operational downtime through reliable performance
- Compliance with stringent industry regulations and standards
- Lower total cost of ownership through extended service life
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Polyimide Kapton film serves critical functions in electronics manufacturing, particularly for flexible printed circuits, wire insulation, and semiconductor processing. Its outstanding dielectric properties and thermal endurance withstand extreme temperatures from -269°C to 400°C, making it essential for high-performance applications where alternative materials typically fail. This reliability ensures consistent operation in demanding electronic environments where precision and durability are paramount requirements for successful manufacturing outcomes.
In aerospace and automotive sectors, Kapton provides vital insulation for wiring harnesses, motor systems, and thermal protection systems. The material's lightweight characteristics combined with exceptional resistance to radiation, chemicals, and mechanical stress guarantee long-term reliability in challenging operational conditions. These properties significantly enhance safety measures and operational efficiency across various industrial sectors, supporting continuous performance in environments where failure is not an option for business operations.
- Flexible printed circuit insulation for consumer electronics and medical devices
- High-temperature wire and cable wrapping in aerospace and automotive systems
- Thermal and radiation shielding for satellite and spacecraft components
- Heater elements and insulation within industrial equipment and processes
- Adhesive tapes and masking materials for semiconductor and PCB manufacturing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arizona Tech- Zeal, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
High Temperature Polyimide Kapton Film For Electronics And Aerospace
High Temperature Polyimide Kapton Film provides exceptional thermal stability, electrical insulation, and chemical resistance for demanding electronics, aerospace, and industrial applications with reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arizona Tech- Zeal
 Maharashtra, India
Industrial Equipment & MachineryTrading Company