IN
₹
Description
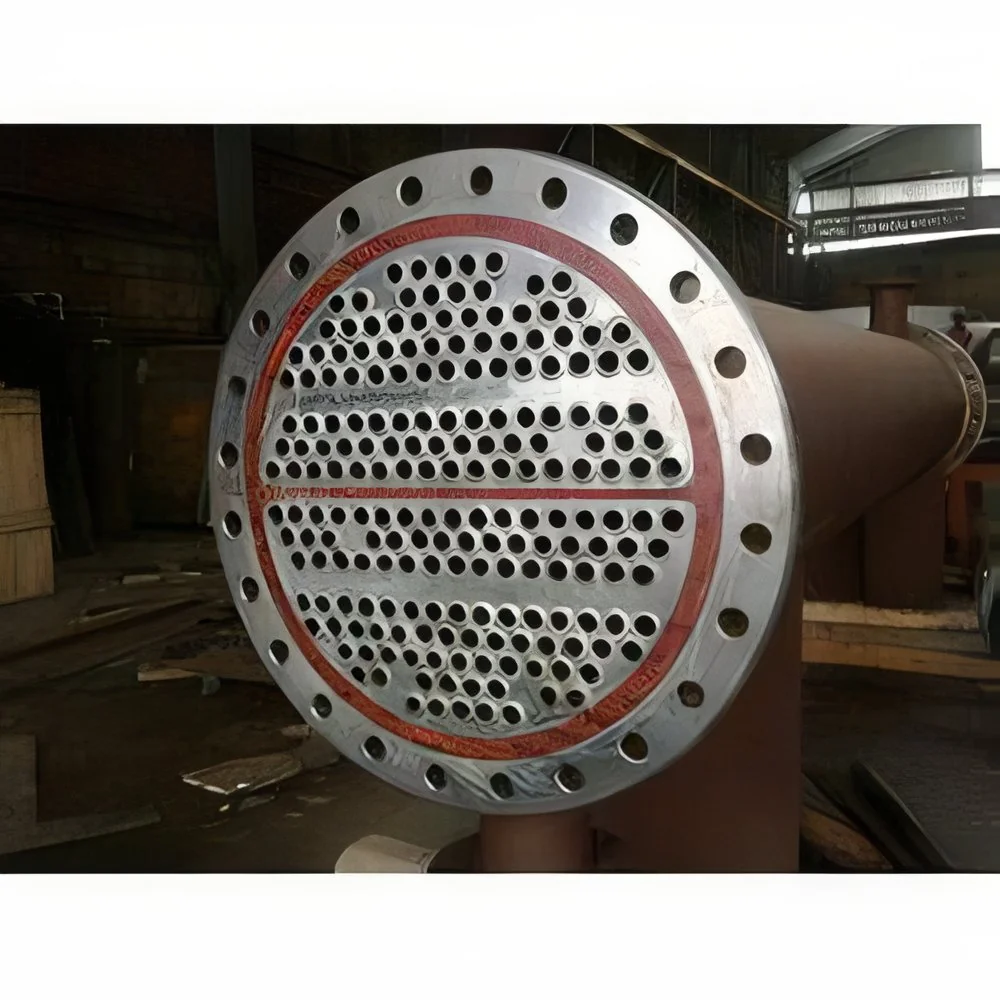
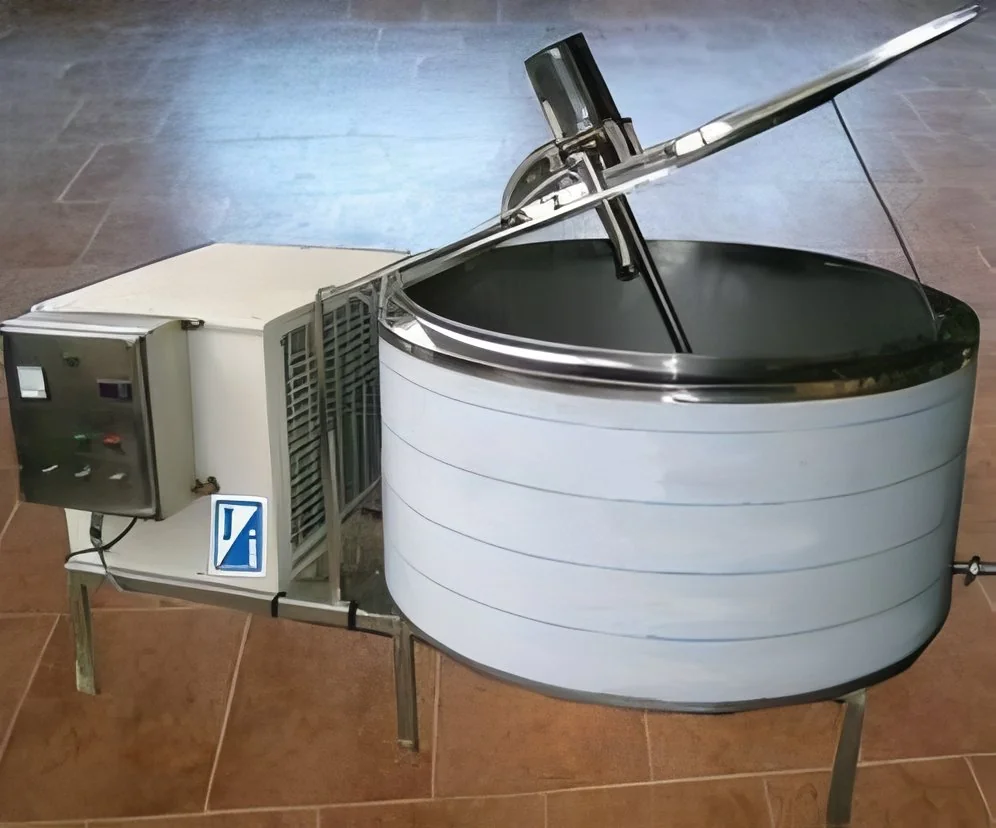
Our premium open type bulk milk coolers deliver essential rapid cooling for commercial dairy operations, available in capacities from 300 liters to an expansive 10,000 liters. Engineered specifically for the demanding cycles of dairy farming and processing, these units are designed to preserve milk quality from the moment of collection. They utilize efficient cooling technology to quickly lower milk temperature, inhibiting bacterial growth and maintaining the product's natural state. Built with industrial-grade durability, they ensure reliable performance in continuous-use environments, making them a fundamental component for any operation focused on quality preservation and operational flow. Their design prioritizes hygiene and ease of use, integrating seamlessly into existing dairy workflows to support both small and large-scale production needs.

These cooling systems are deployed across the entire dairy supply chain, serving critical functions at multiple stages. Large commercial d...
Our premium open type bulk milk coolers deliver essential rapid cooling for commercial dairy operations, available in capacities from 300 liters to an expansive 10,000 liters. Engineered specifically for the demanding cycles of dairy farming and processing, these units are designed to preserve milk quality from the moment of collection. They utilize efficient cooling technology to quickly lower milk temperature, inhibiting bacterial growth and maintaining the product's natural state. Built with industrial-grade durability, they ensure reliable performance in continuous-use environments, making them a fundamental component for any operation focused on quality preservation and operational flow. Their design prioritizes hygiene and ease of use, integrating seamlessly into existing dairy workflows to support both small and large-scale production needs.

These cooling systems are deployed across the entire dairy supply chain, serving critical functions at multiple stages. Large commercial dairy farms implement them directly in milking parlors for immediate cooling, which is vital for meeting quality standards. Milk collection and cooperative centers use them to aggregate and chill milk from multiple sources before bulk transport. Processing plants rely on them for holding raw milk at safe temperatures prior to pasteurization and further manufacturing. Their robust design also makes them suitable for educational and research institutions with dairy programs, as well as for operations that require dependable, high-capacity temperature control for raw agricultural products.

The investment in a reliable bulk milk cooler translates directly into tangible business value through quality preservation and operational efficiency. By rapidly stabilizing milk temperature, these units significantly reduce spoilage and waste, protecting your product's value and your revenue. Their durable construction minimizes maintenance interruptions and extends equipment lifespan, lowering total cost of ownership. Energy-efficient operation helps control ongoing utility expenses, while their reliable performance ensures consistent output quality, supporting brand reputation and compliance with food safety regulations. This combination of preservation, durability, and efficiency makes them a strategic asset for improving profitability and securing the quality of your dairy products.

Key Features:
- Available in a wide capacity range from 300L to 10000L to suit various operational scales
- Rapid cooling technology designed to quickly lower milk temperature for optimal preservation
- Constructed with durable, hygienic materials suitable for demanding dairy environments
- Engineered for reliable, continuous operation with consistent performance
- Designed with efficiency in mind to support operational workflows and hygiene standards

Benefits:
- Preserves milk quality and nutritional value by rapidly inhibiting bacterial growth
- Reduces product spoilage and waste, directly protecting profitability and revenue
- Provides reliable, durable performance that minimizes downtime and maintenance costs
- Supports compliance with food safety and quality standards through consistent temperature control
- Offers scalable capacity solutions to match the specific needs of different dairy operations
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Open type bulk milk coolers are engineered for immediate post-milking temperature control, crucial for maintaining milk quality and safety. They serve as the first line of defense against bacterial growth, rapidly chilling milk to preserve its natural properties and nutritional value from farm to processing. These systems are built for the rigorous demands of agricultural and industrial settings, providing reliable cooling performance that supports food safety compliance and operational efficiency for serious dairy operations.
Designed for continuous use in medium to large-scale dairy environments, these coolers handle substantial volumes with consistent performance. Their robust construction withstands daily farming operations while maintaining precise temperature control. This makes them ideal for facilities where hygiene, reliability, and capacity are non-negotiable, supporting everything from individual farm storage to centralized collection points before further processing or transport.
- Immediate milk cooling and short-term storage at commercial dairy farms after milking
- Centralized bulk milk chilling and holding at cooperative collection centers
- Temporary storage and temperature maintenance at dairy processing plants before pasteurization
- Preserving milk quality during transfer and logistics between farm and facility
- Large-volume milk aggregation and cooling at milk production and handling units
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Jaya Industries, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Dairy Farm Bulk Milk Coolers 300L To 10000L Rapid Cooling
Premium open type bulk milk coolers from 300L to 10000L capacities ensure rapid cooling for dairy farms and processing units, preserving milk quality with durable, efficient performance for demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Jaya Industries
 West Bengal, India
Industrial Equipment & MachineryManufacturer