IN
₹
Description
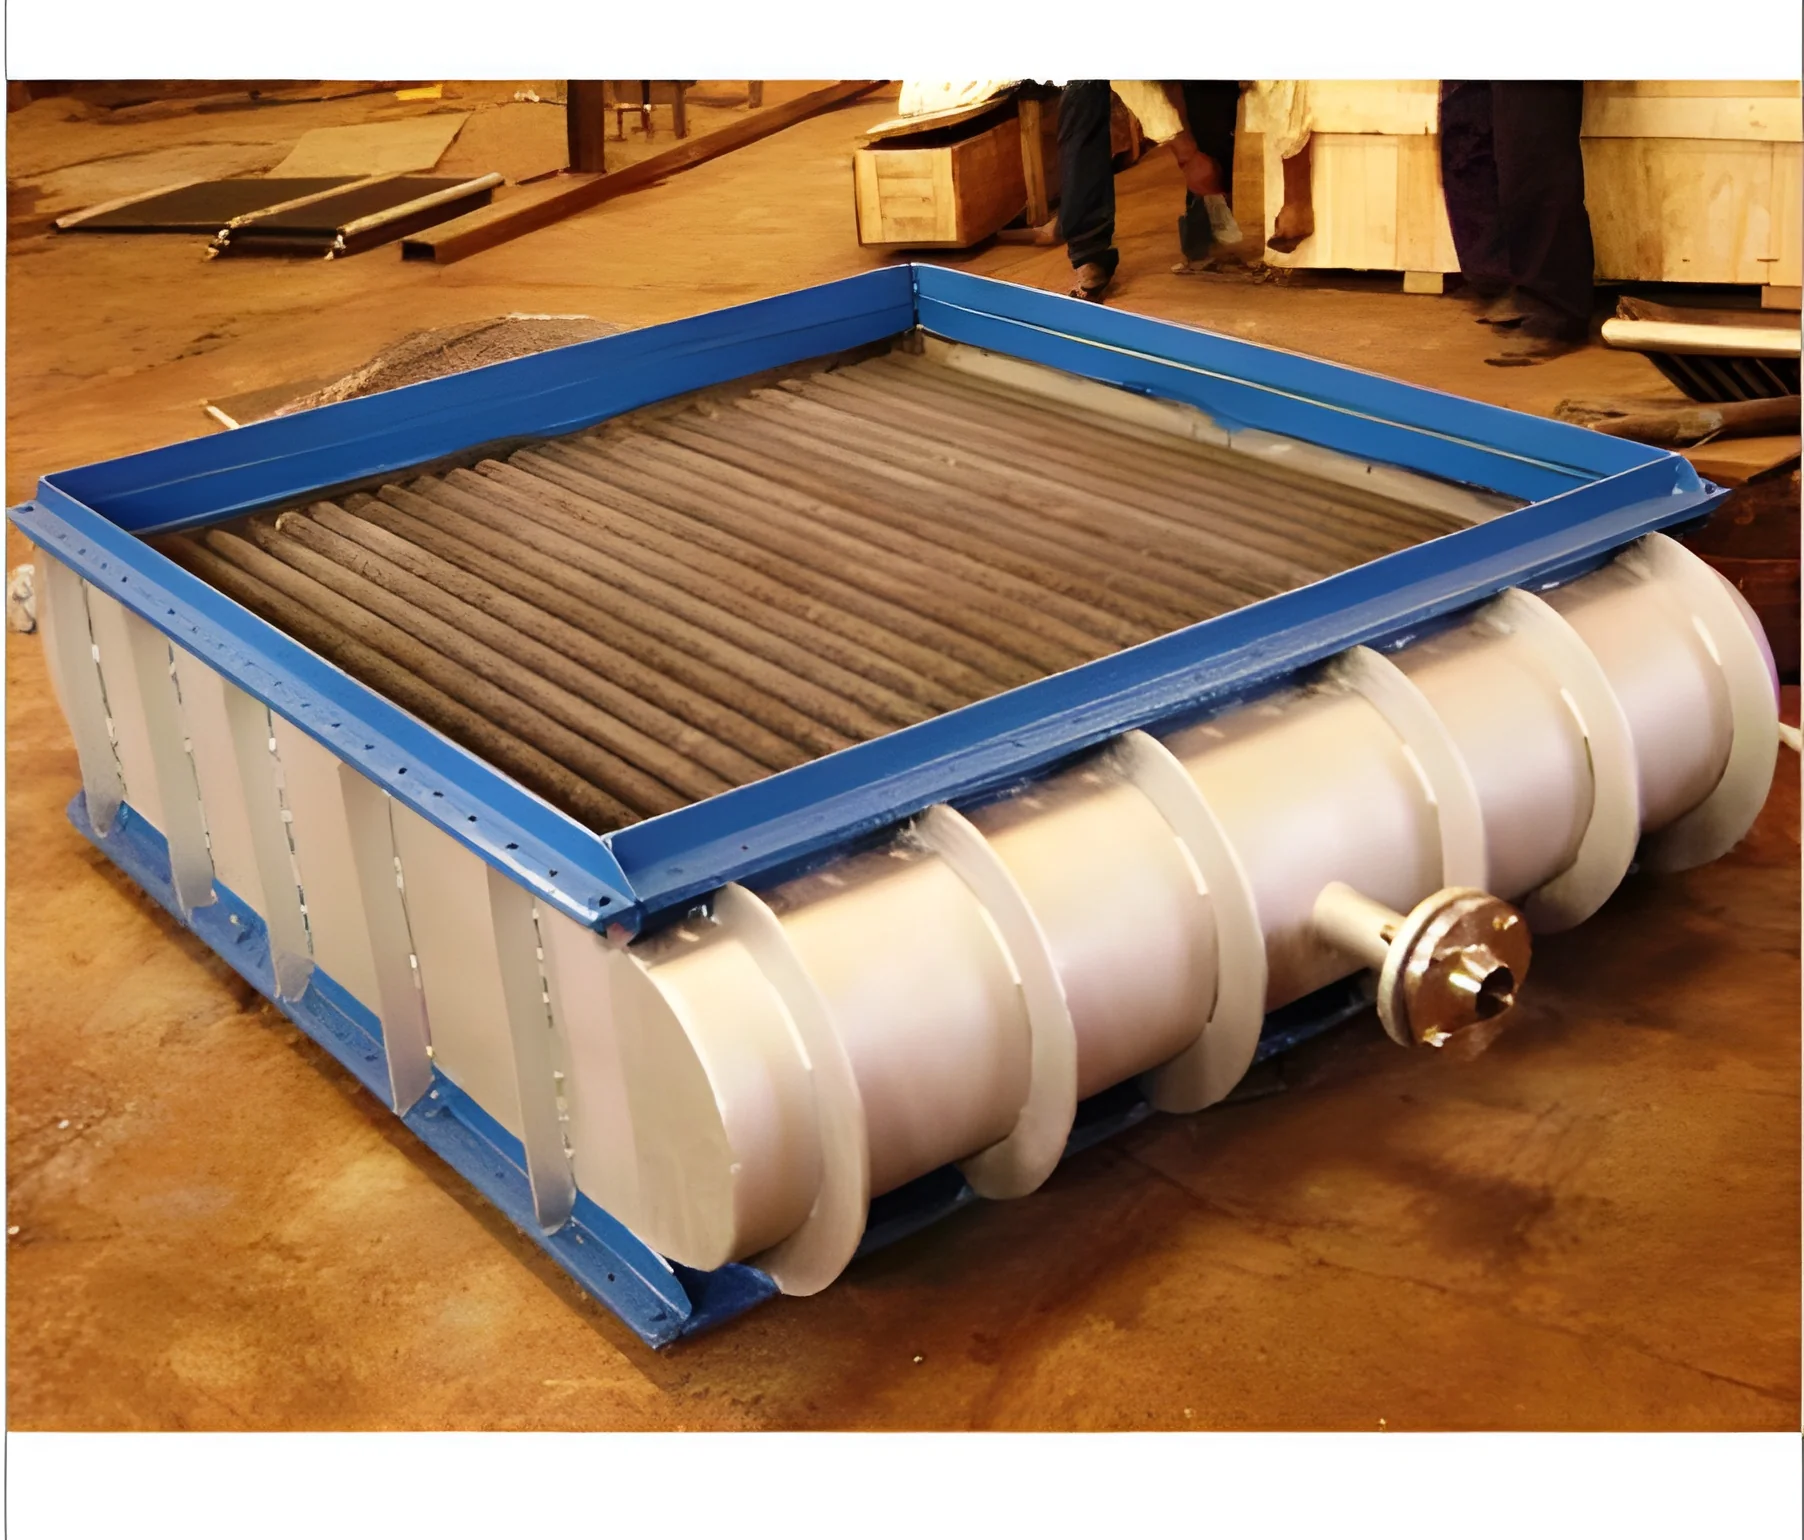
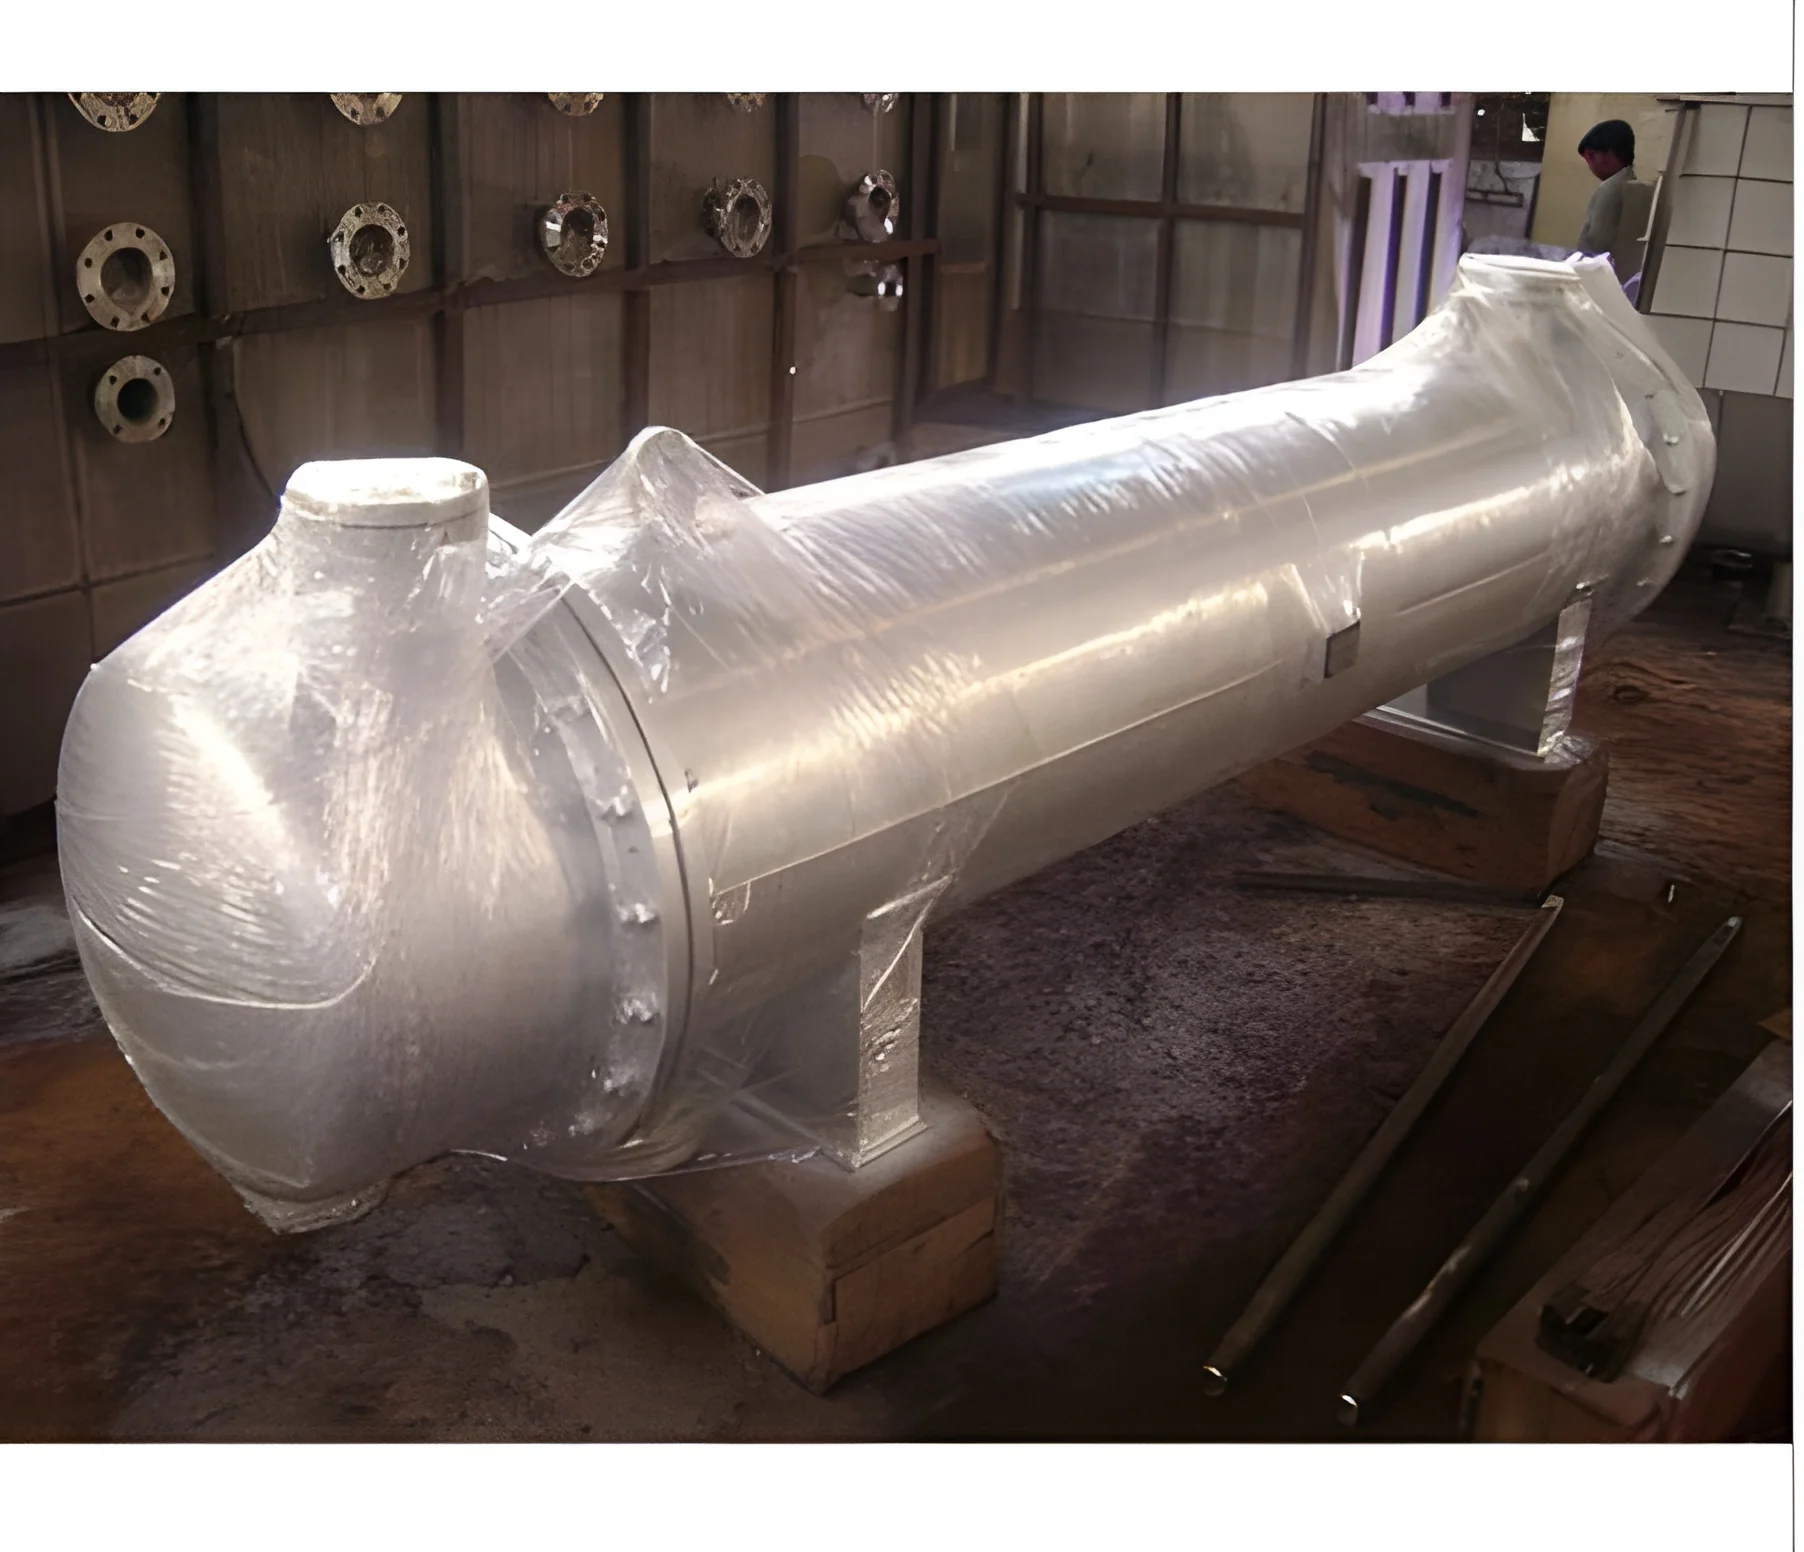
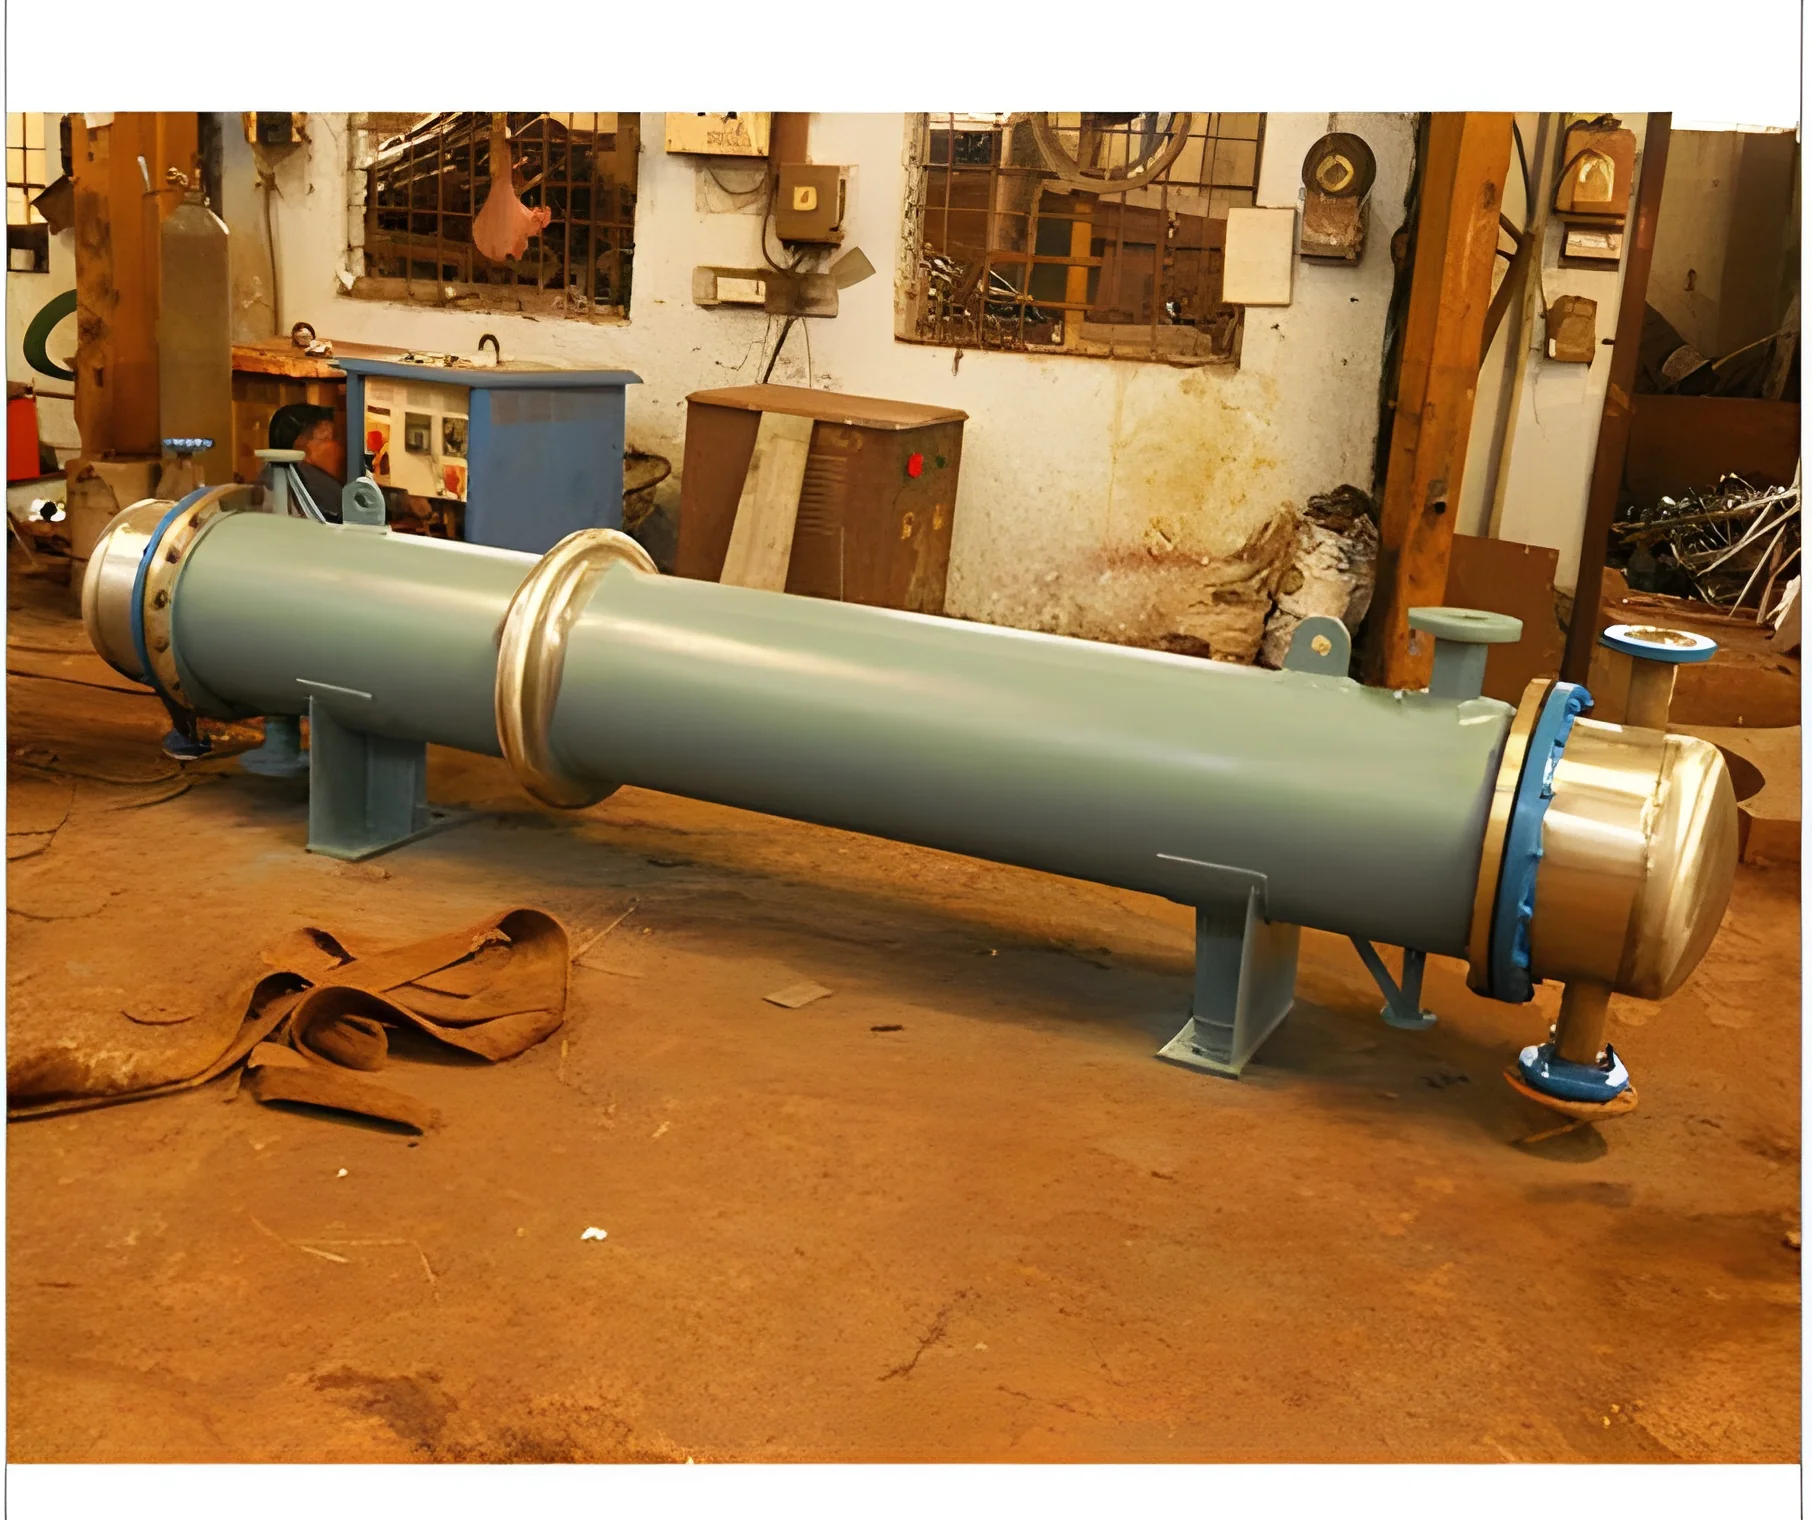
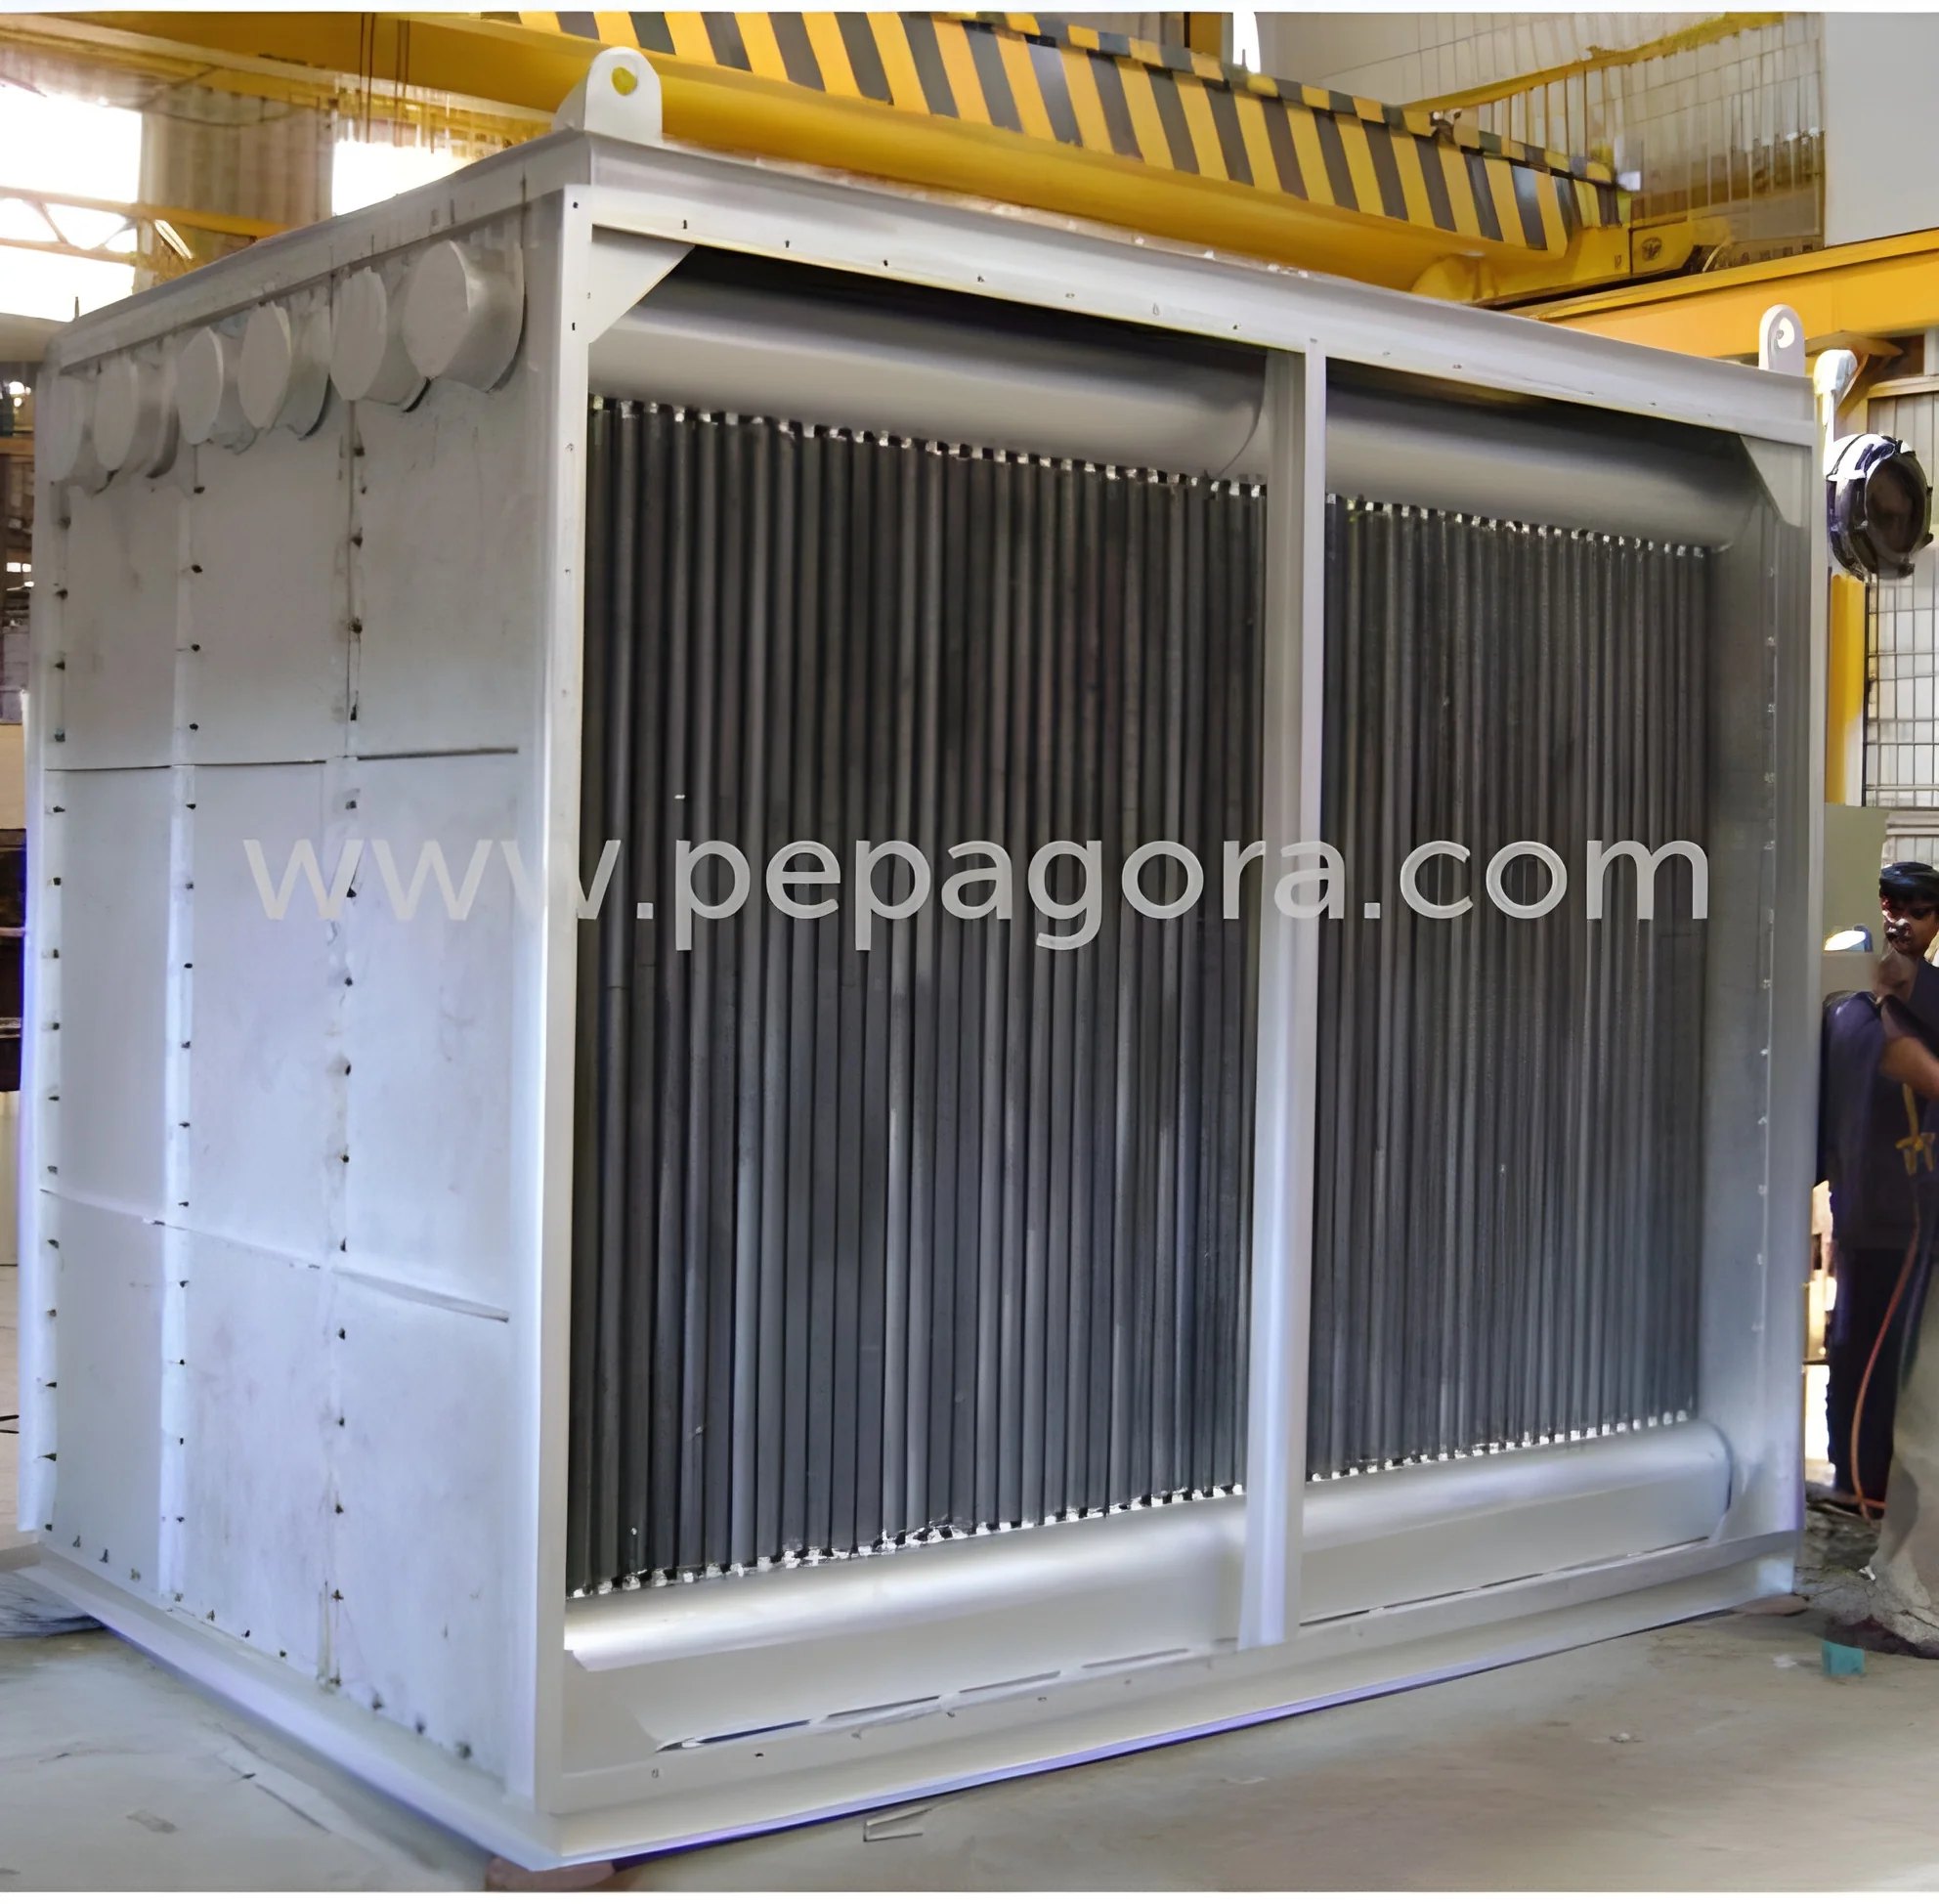
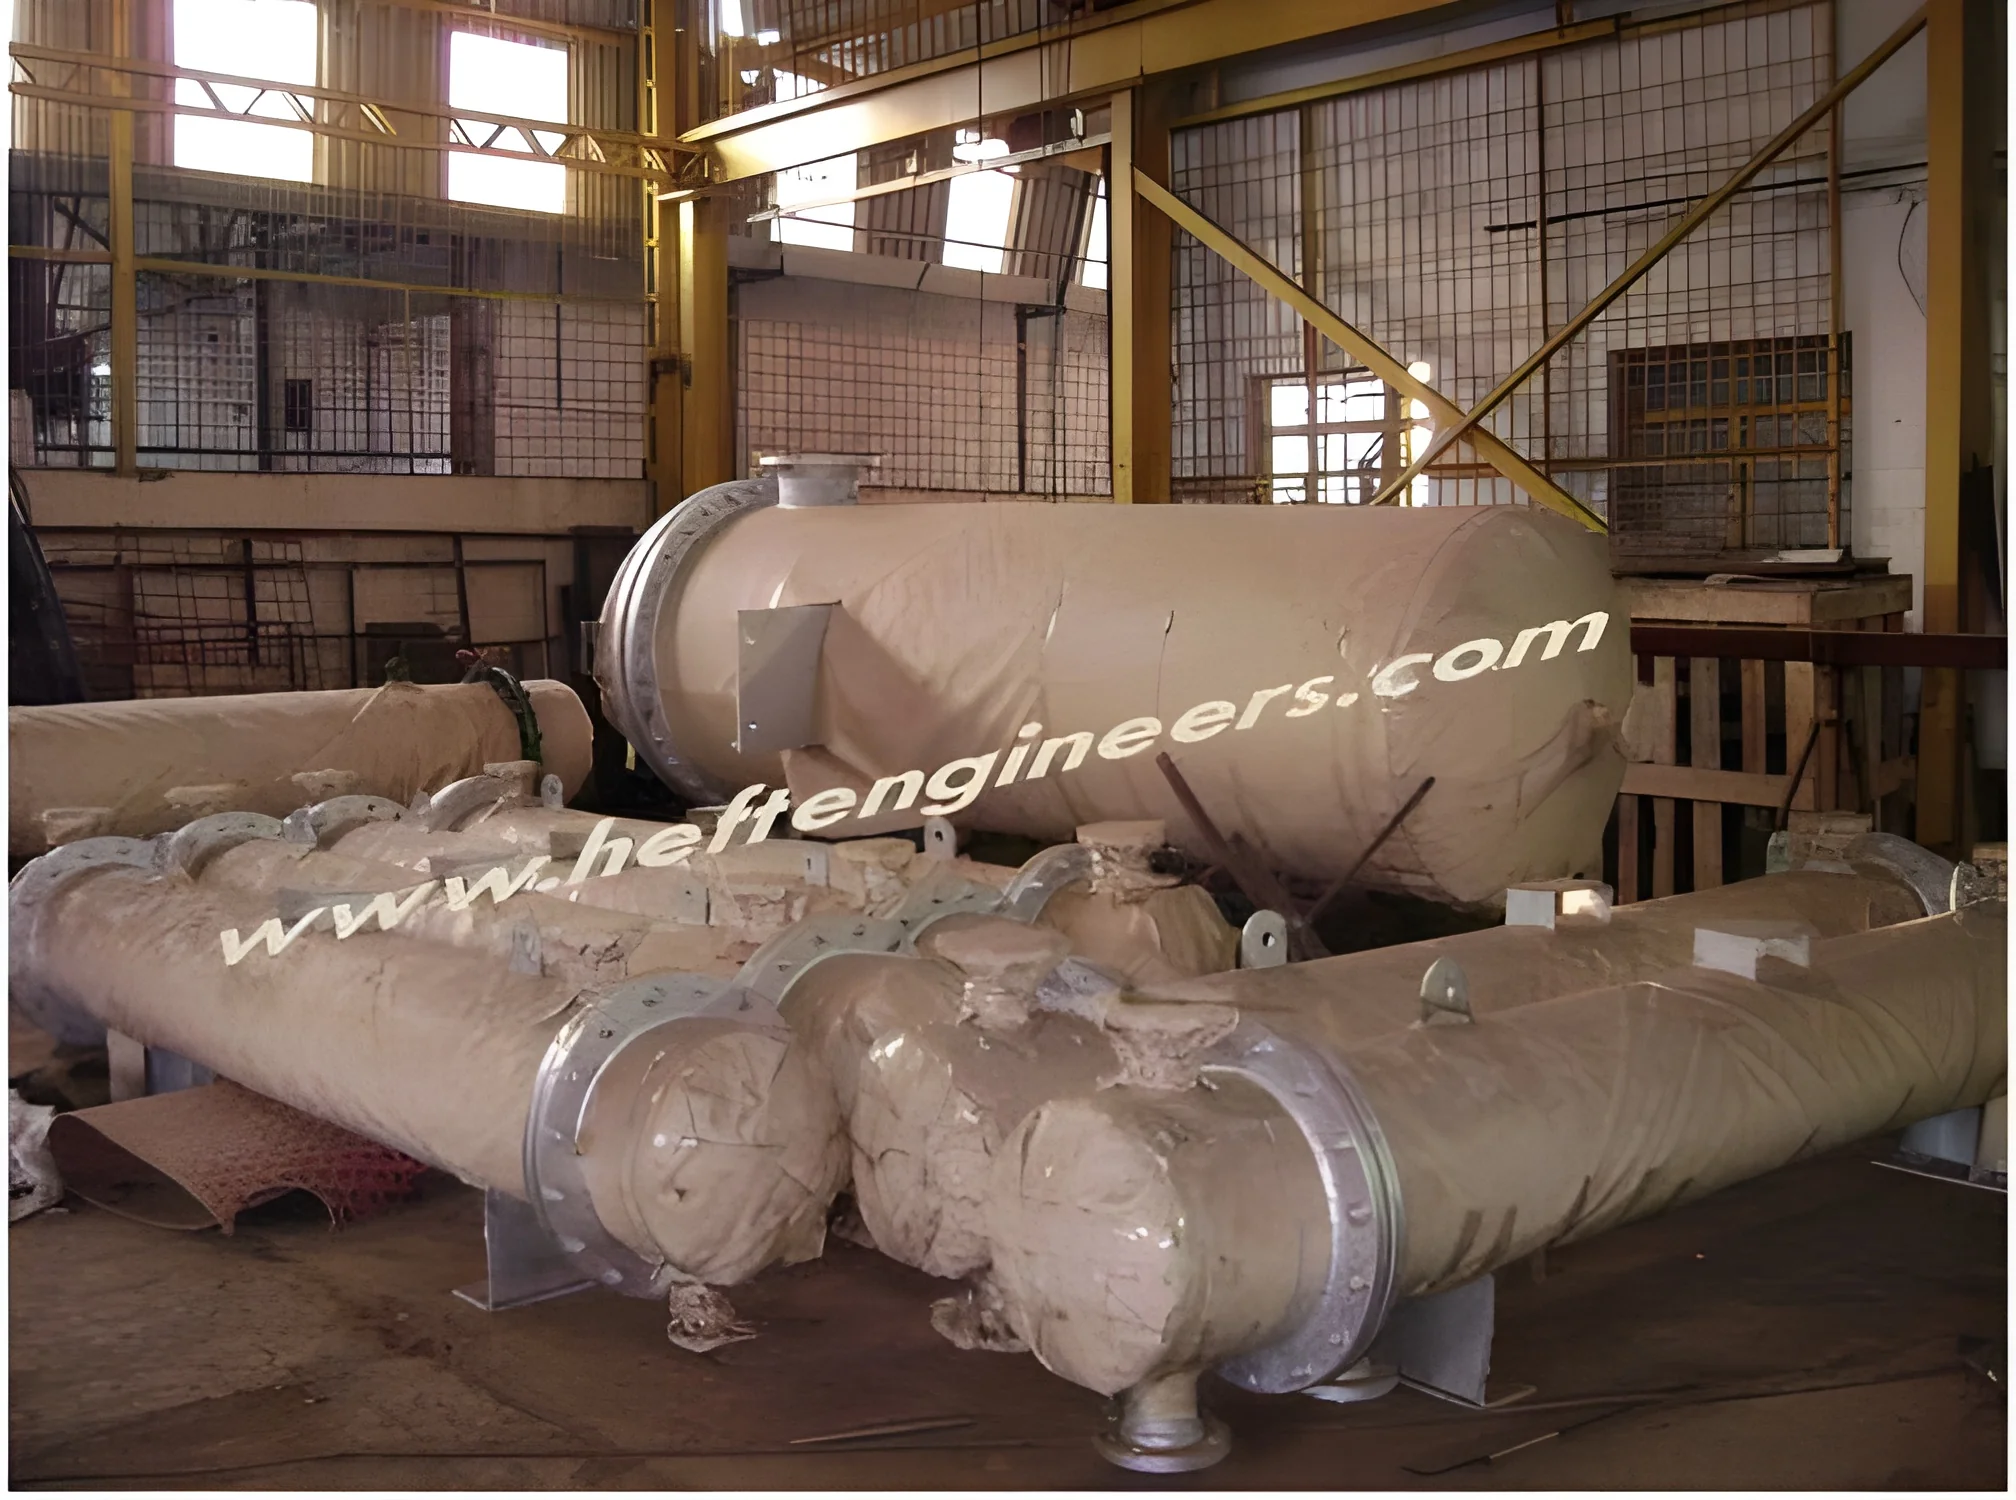
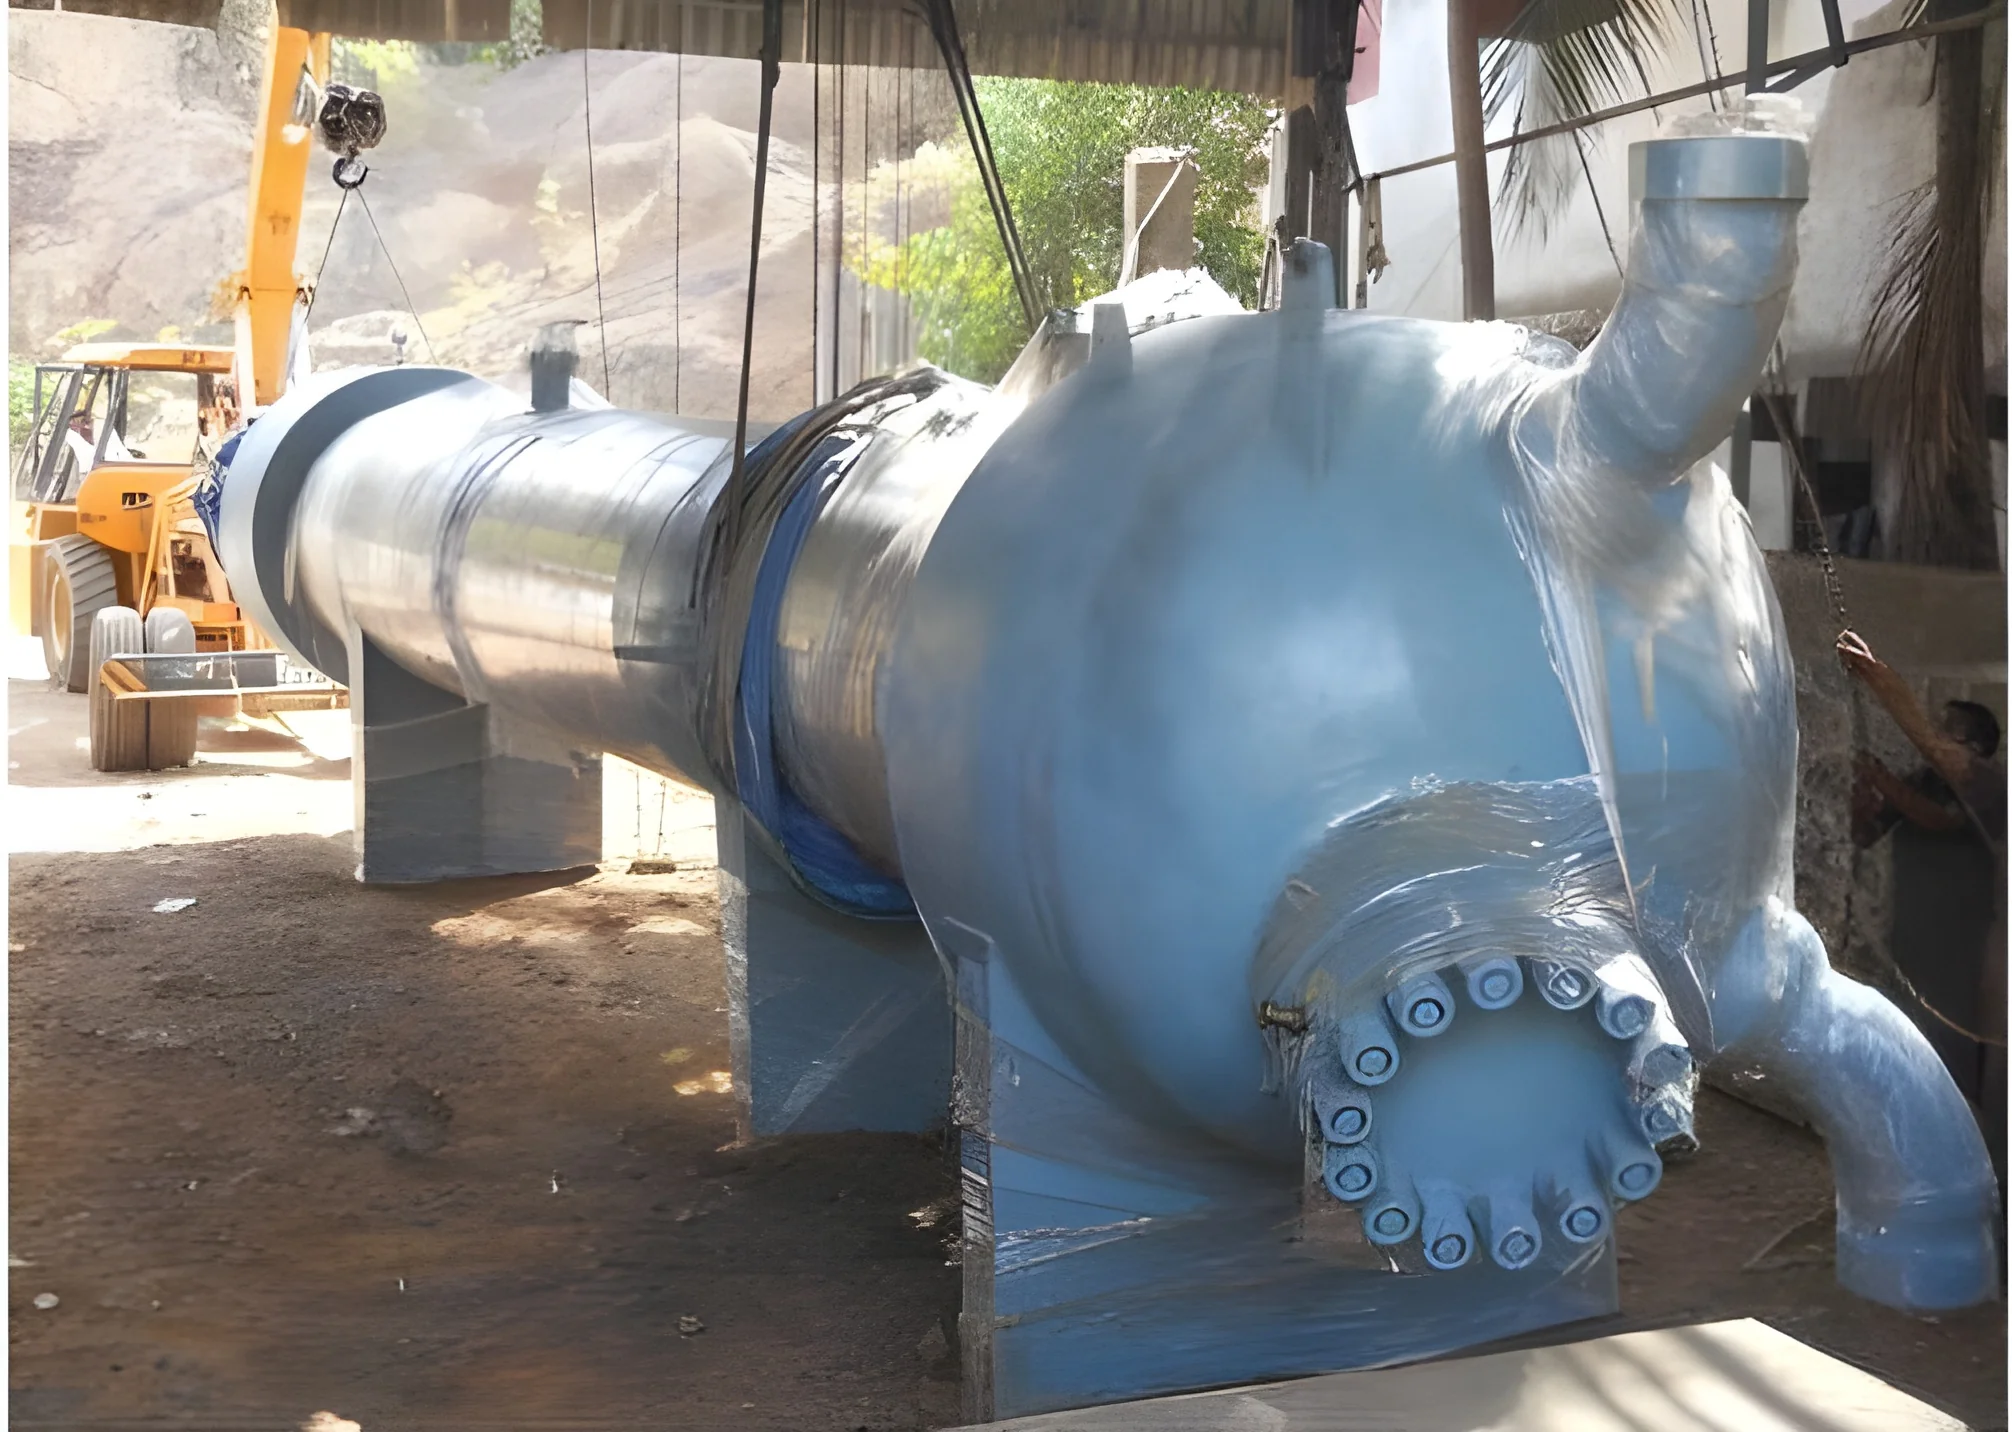
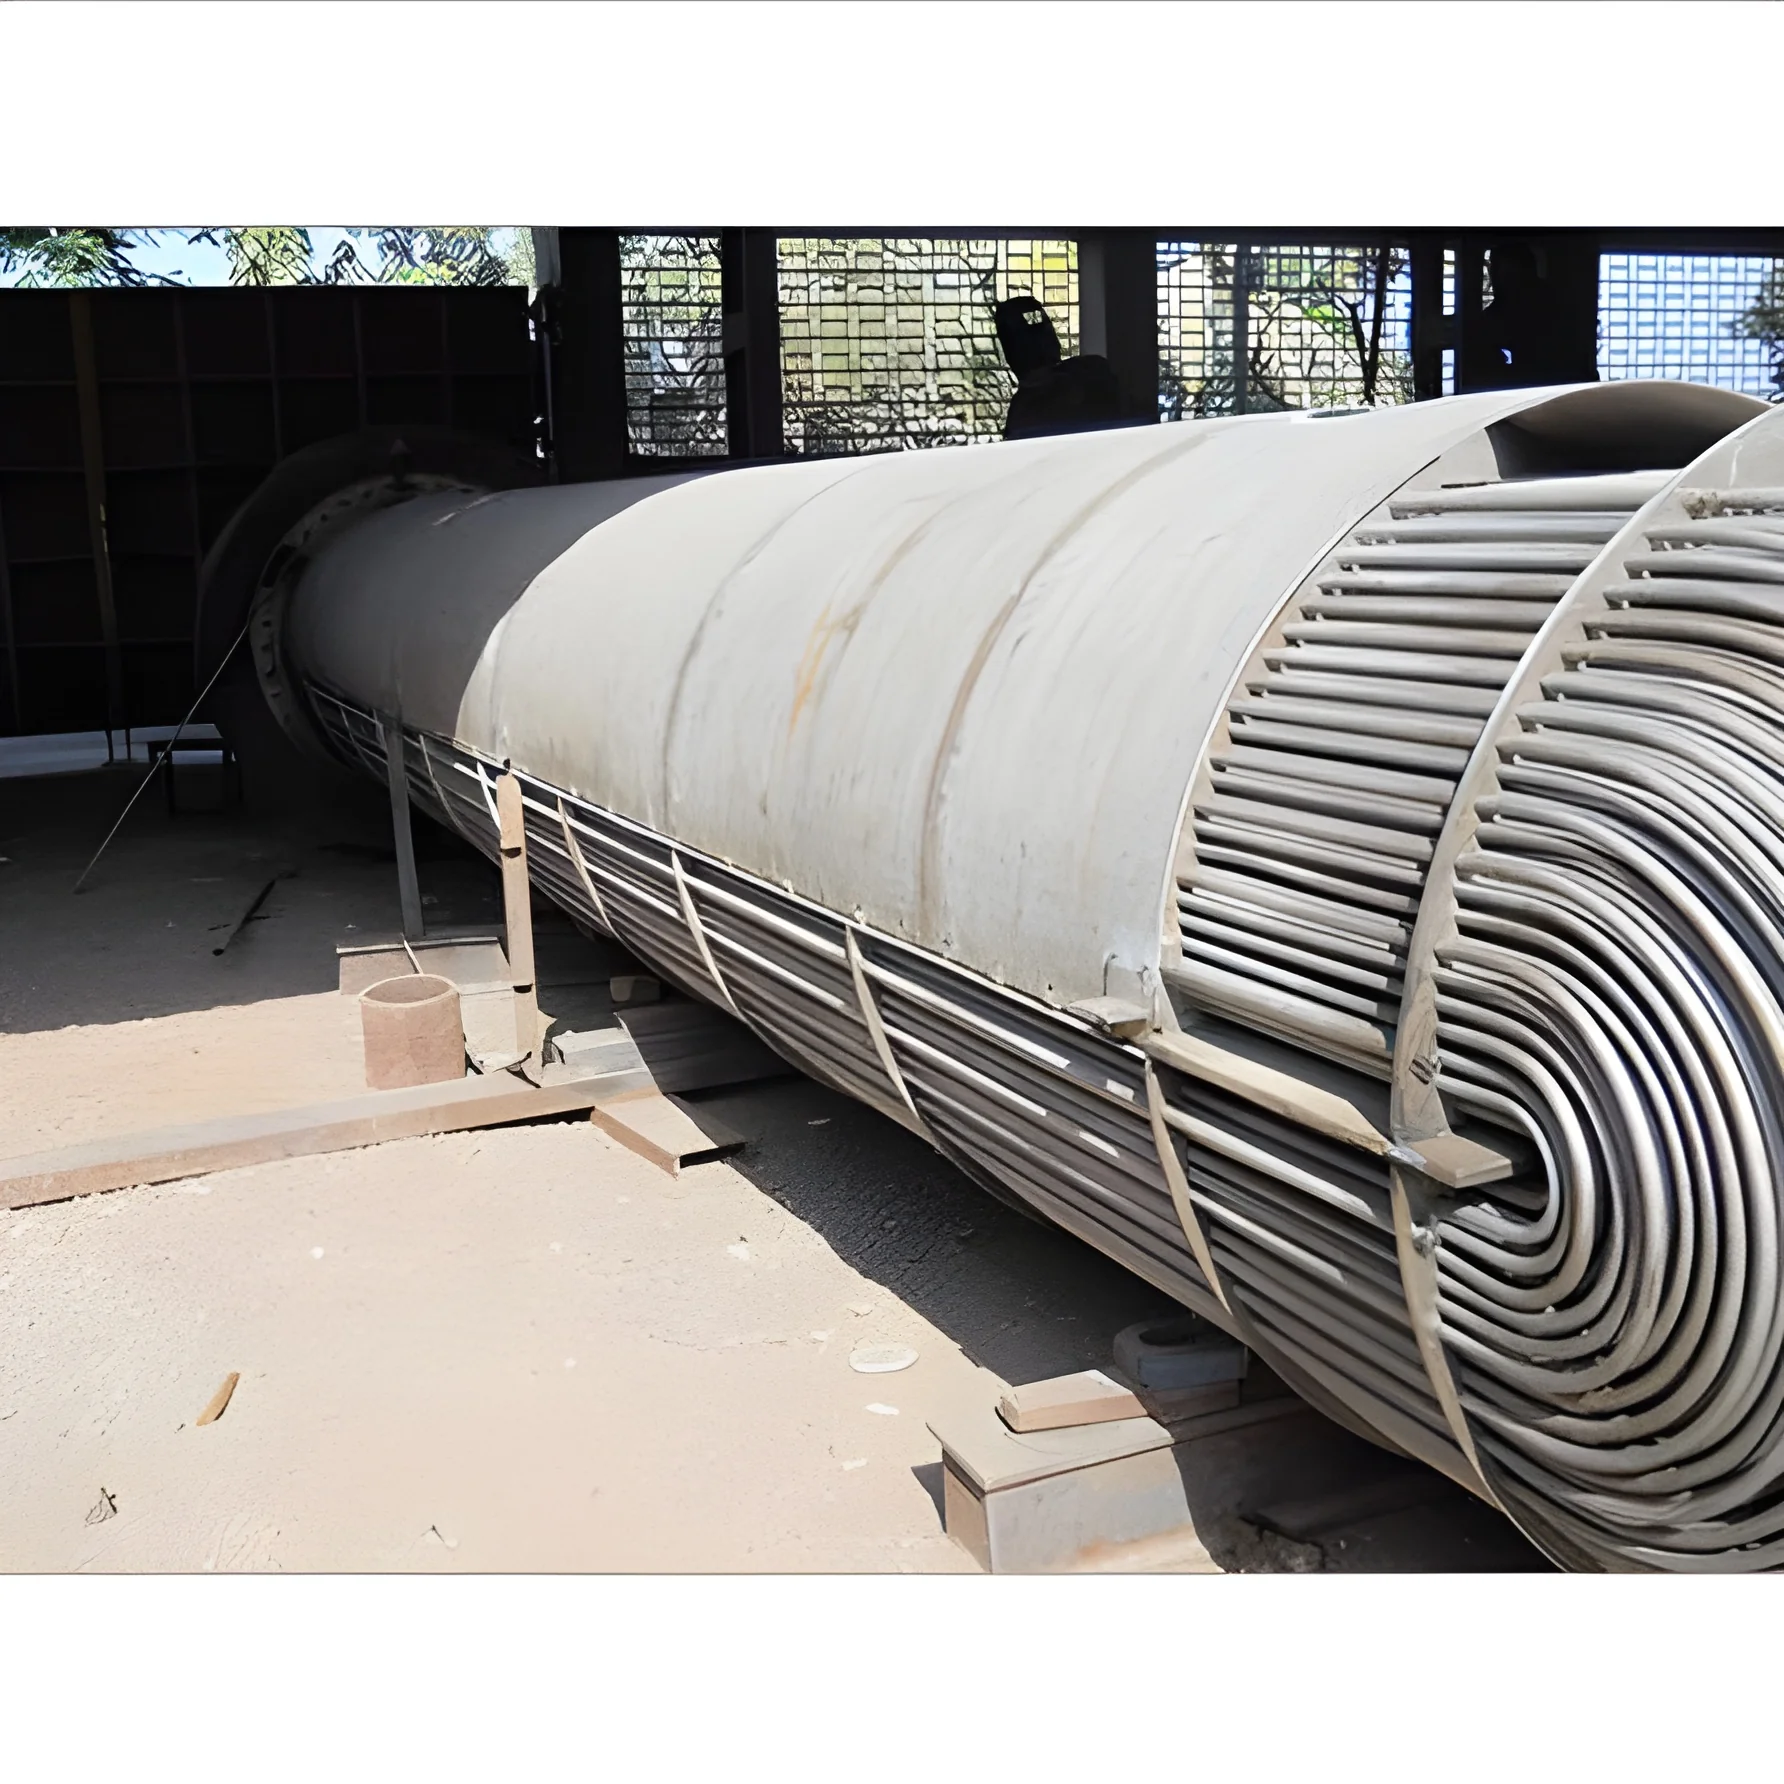
Engineered for superior performance in demanding environments, our industrial tube heat exchangers represent advanced thermal management technology. These units facilitate efficient heat transfer between liquids and gases through a sealed tube system, preventing fluid mixing while maximizing thermal conductivity. Each exchanger undergoes rigorous testing and holds certifications from TUV, EIL, Campro, and Bax Counsel, ensuring compliance with international quality and safety standards. The construction utilizes corrosion-resistant materials and optimized heat transfer surfaces, delivering reliable operation where temperature control is essential for process integrity and equipment protection.

These heat exchangers serve vital functions across multiple sectors. In chemical processing plants, they handle reactor cooling, condenser duties, and temperature regulation of sensitive compounds. Power generation facilities rely on them for turbine oil cooling, feedwater heating, and waste heat...
Engineered for superior performance in demanding environments, our industrial tube heat exchangers represent advanced thermal management technology. These units facilitate efficient heat transfer between liquids and gases through a sealed tube system, preventing fluid mixing while maximizing thermal conductivity. Each exchanger undergoes rigorous testing and holds certifications from TUV, EIL, Campro, and Bax Counsel, ensuring compliance with international quality and safety standards. The construction utilizes corrosion-resistant materials and optimized heat transfer surfaces, delivering reliable operation where temperature control is essential for process integrity and equipment protection.

These heat exchangers serve vital functions across multiple sectors. In chemical processing plants, they handle reactor cooling, condenser duties, and temperature regulation of sensitive compounds. Power generation facilities rely on them for turbine oil cooling, feedwater heating, and waste heat recovery systems. The HVAC industry integrates these units for large-scale climate control and energy-efficient heat exchange in commercial buildings. Manufacturing operations utilize them for machinery cooling and process temperature maintenance, while the food and beverage sector depends on them for sanitary thermal processing of ingredients and final products.

Choosing our tube heat exchangers delivers measurable operational advantages through enhanced energy efficiency and reduced lifecycle costs. The robust design minimizes maintenance requirements and extends service intervals, lowering total cost of ownership. The certified quality ensures consistent performance under varying pressure and temperature conditions, reducing process variability and production downtime. This reliability translates to improved system uptime and predictable thermal management, supporting continuous operation in critical applications. The engineering focus on durability and efficiency provides long-term value through sustained performance and operational stability.

Key Features:
- Certified by TUV, EIL, Campro, and Bax Counsel for verified quality and safety standards
- High thermal efficiency design with optimized surface area for maximum heat transfer
- Robust construction using corrosion-resistant materials suitable for harsh environments
- Engineered for specific pressure, temperature, and flow rate requirements
- Accessible design with removable components for straightforward maintenance

Benefits:
- Enhanced energy efficiency reduces operational costs through optimal heat recovery
- Certified reliability ensures consistent performance in critical thermal processes
- Durable construction minimizes maintenance needs and extends equipment lifespan
- Precise temperature control improves process consistency and product quality
- Proven design reduces system downtime and supports continuous operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial tube heat exchangers provide efficient, reliable heat transfer for high-pressure and high-temperature operations in closed-loop systems. Their robust design ensures precise temperature control and energy recovery, making them essential for processes where thermal management is critical to productivity and safety. These units are engineered for minimal maintenance and long service life across diverse industrial environments. The construction prioritizes durability and consistent performance, handling various fluid types and flow conditions with proven reliability in continuous operation.
Real-world applications:
- Cooling hydraulic oil and lubricants in heavy machinery and manufacturing equipment
- Heating process fluids in chemical and pharmaceutical production lines
- Condensing steam and recovering waste heat in power generation plants
- Regulating temperature in HVAC systems for large commercial and industrial buildings
- Preheating feedwater and other inputs in food, beverage, and dairy processing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Heft Engineers, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Tube Heat Exchangers For High Efficiency Thermal Transfer
Premium industrial tube heat exchangers deliver maximum thermal efficiency and durability for demanding applications. Certified by TUV, EIL, Campro, and Bax Counsel for superior quality and reliable performance across chemical, power, and HVAC systems.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Heft Engineers
 Maharashtra, India
Industrial Equipment & MachineryImporter / Exporter