IN
₹
Description
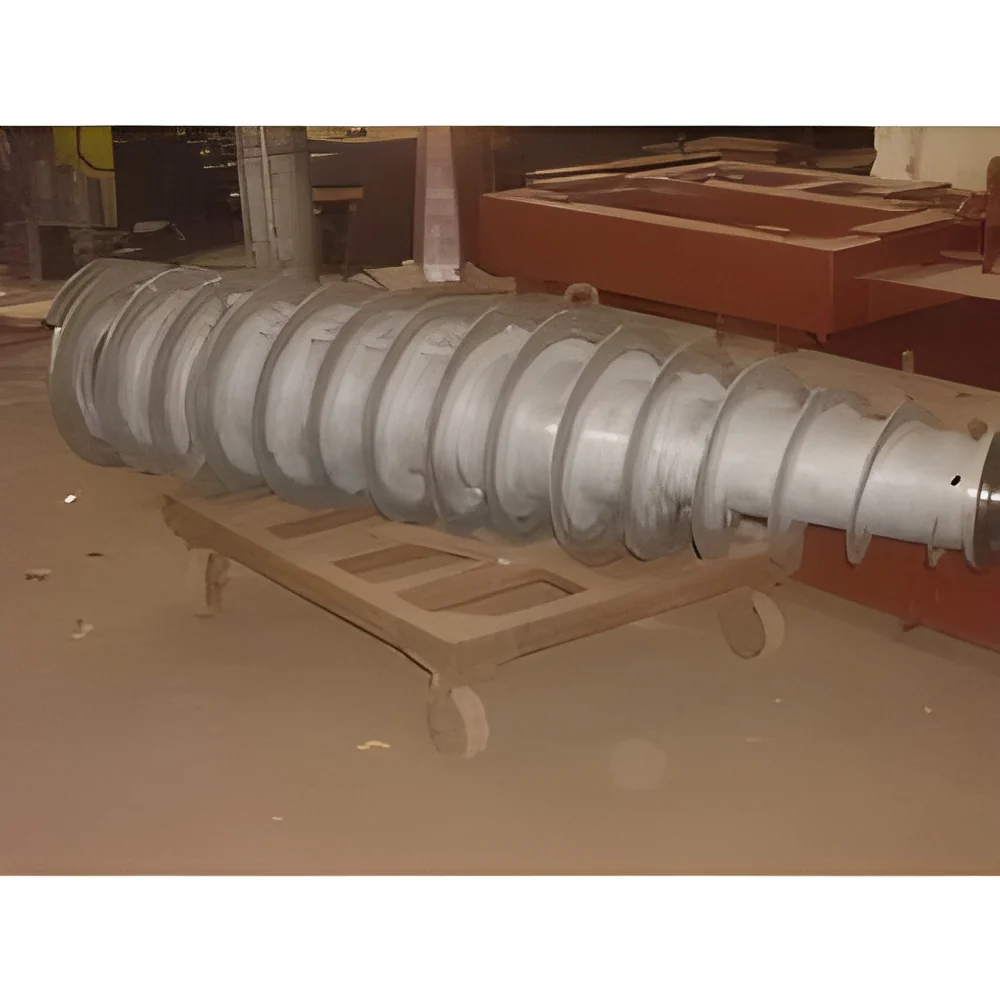
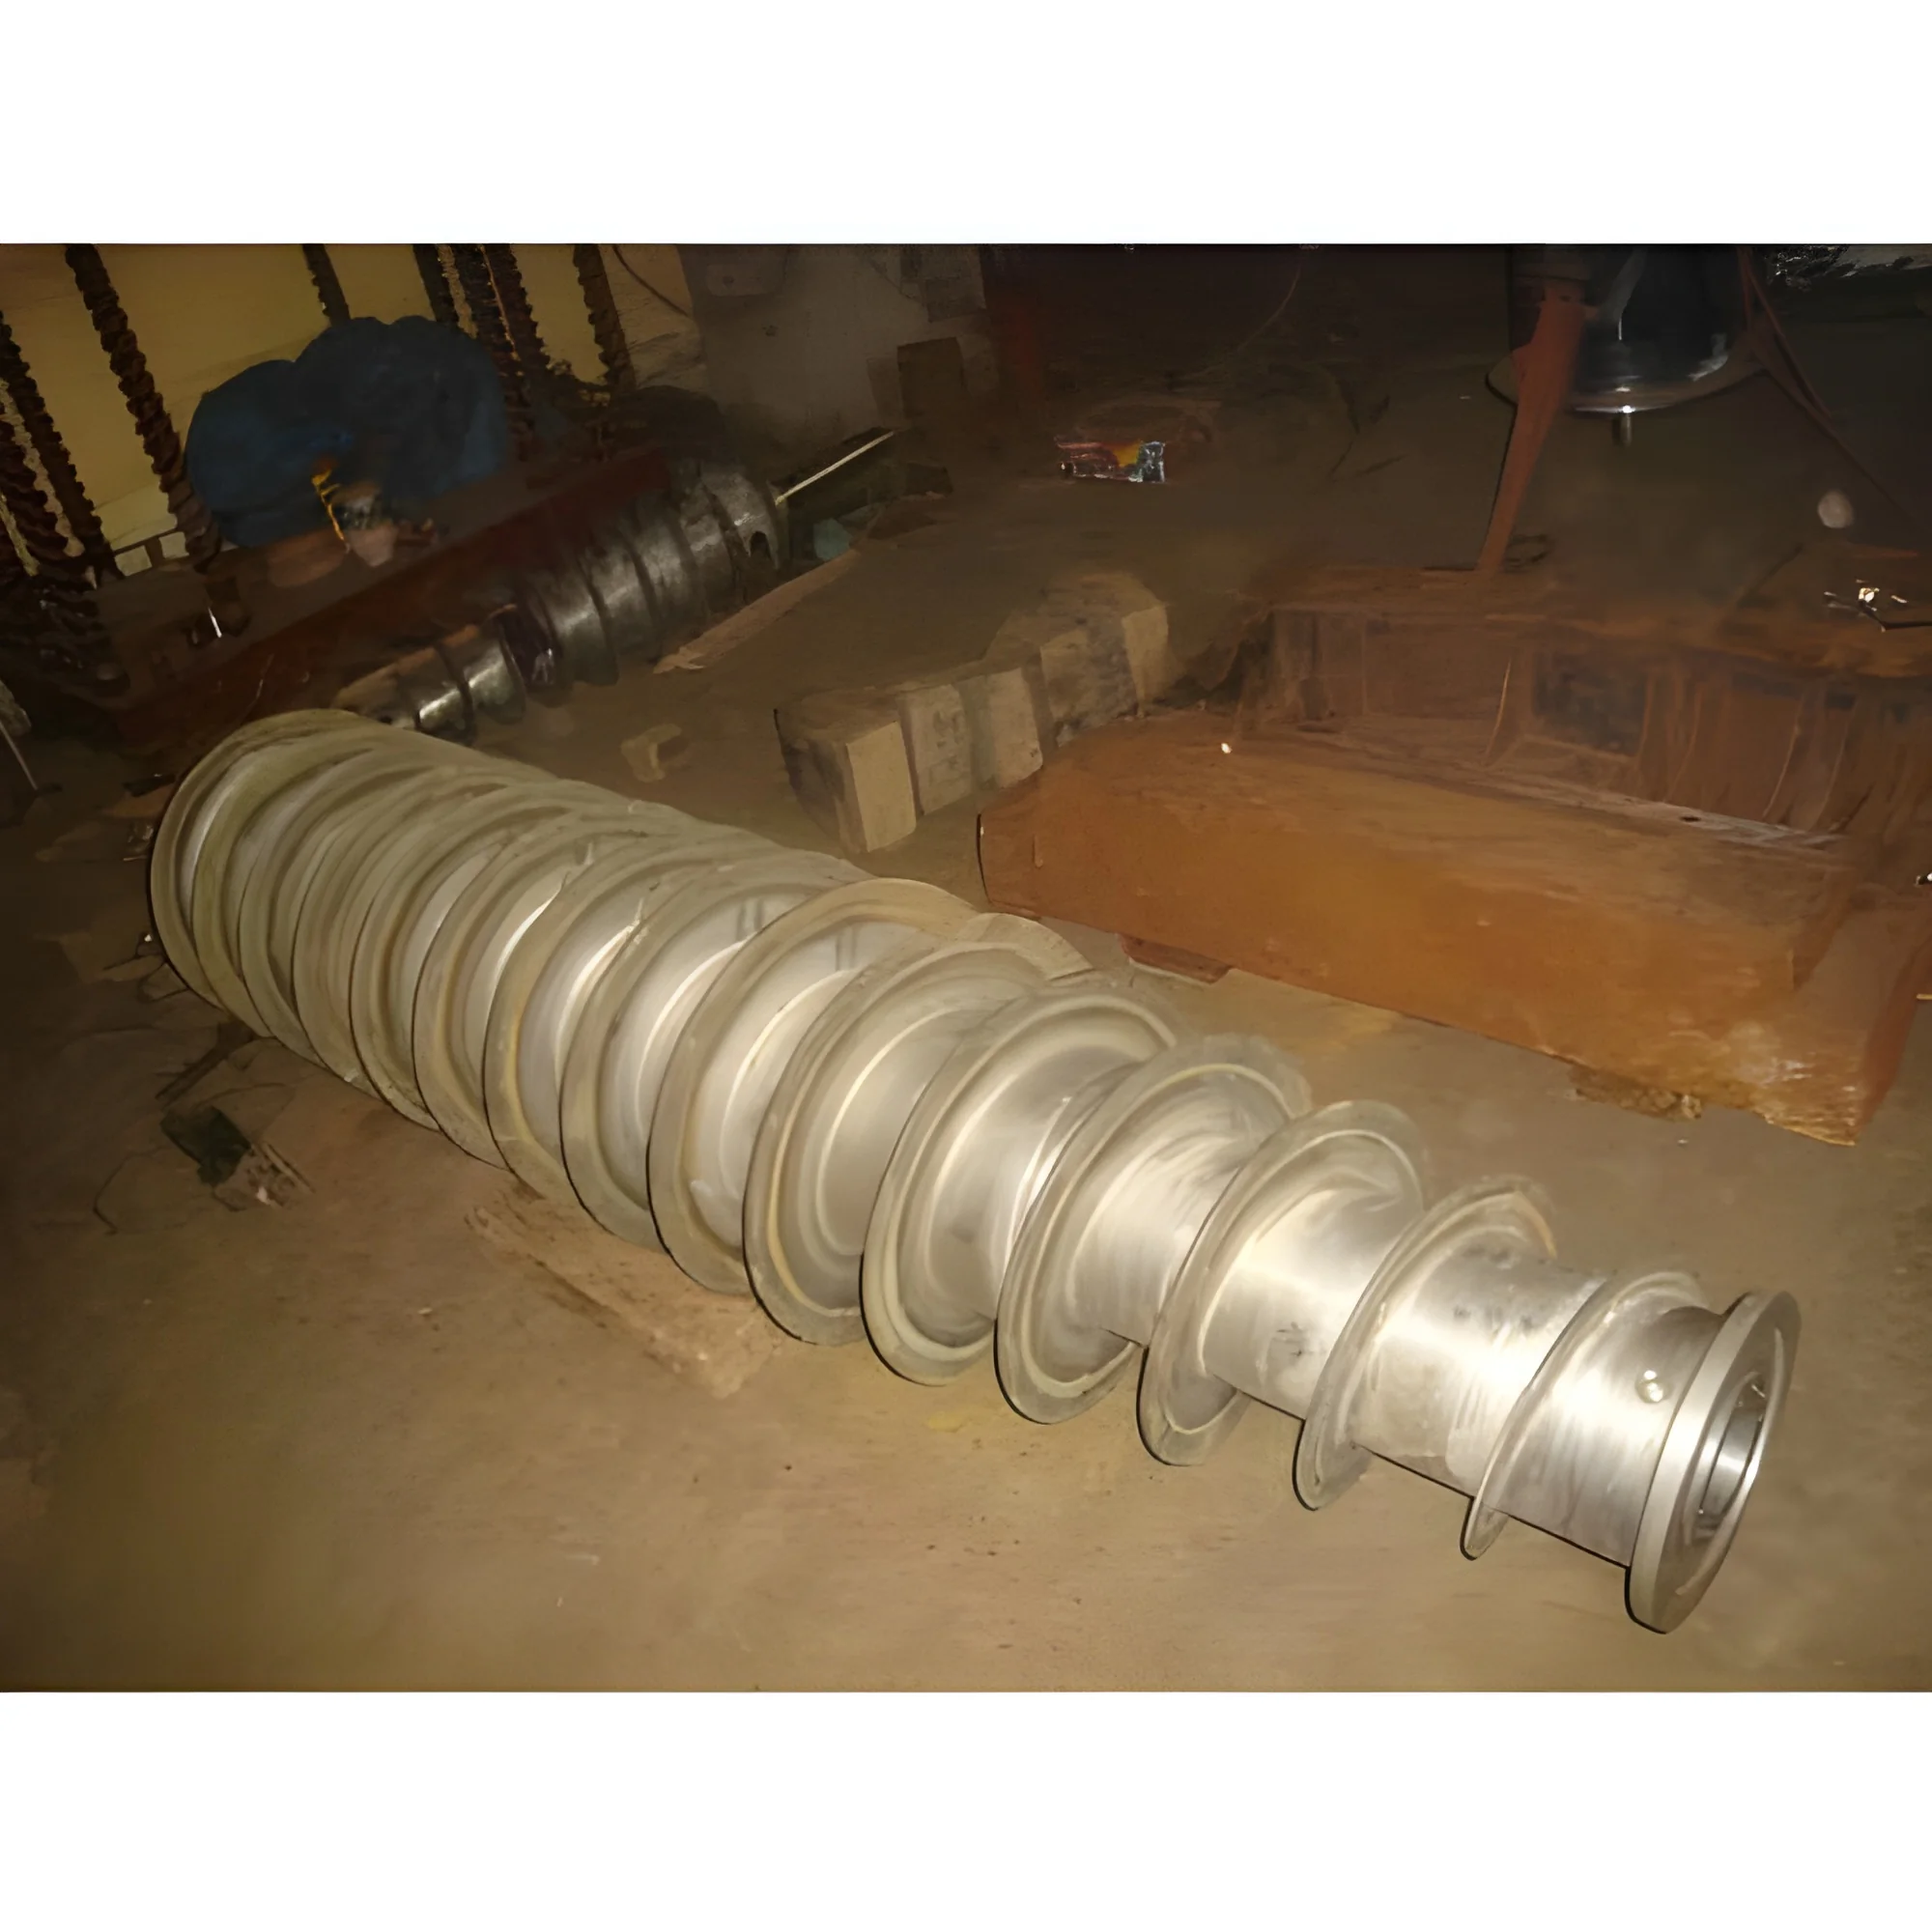
Our industrial centrifuge machine spares represent precision engineering and manufacturing excellence for demanding industrial environments. These replacement components are crafted from premium-grade materials that withstand rigorous operational conditions while maintaining perfect compatibility with original equipment specifications. Each spare part undergoes stringent quality control measures to ensure reliable performance, extended service life, and seamless integration with your existing centrifuge systems, providing confidence for maintenance managers and plant operators across various industries that depend on continuous separation processes.

These high-performance spares serve critical roles across multiple industries including chemical processing plants for solvent recovery systems, pharmaceutical manufacturing for active ingredient separation, and environmental services for waste treatment applications. The food processing sector utilizes them for product purification in dai...
Our industrial centrifuge machine spares represent precision engineering and manufacturing excellence for demanding industrial environments. These replacement components are crafted from premium-grade materials that withstand rigorous operational conditions while maintaining perfect compatibility with original equipment specifications. Each spare part undergoes stringent quality control measures to ensure reliable performance, extended service life, and seamless integration with your existing centrifuge systems, providing confidence for maintenance managers and plant operators across various industries that depend on continuous separation processes.

These high-performance spares serve critical roles across multiple industries including chemical processing plants for solvent recovery systems, pharmaceutical manufacturing for active ingredient separation, and environmental services for waste treatment applications. The food processing sector utilizes them for product purification in dairy and beverage production, while mining operations employ these components for mineral classification. Oil refineries and various industrial facilities use them for separation processes, demonstrating their versatility across diverse applications requiring reliable separation technology.

Businesses choose our centrifuge spares for their exceptional reliability and significant operational value. The precision manufacturing ensures each component delivers consistent performance under heavy industrial loads, reducing maintenance frequency and associated costs. These spares offer a cost-effective alternative to full equipment replacement while maintaining original performance standards. Their durability translates to extended equipment lifespan and improved process efficiency, providing excellent return on investment through reduced downtime and lower total cost of ownership for industrial operations that cannot afford unexpected breakdowns.

Key Features:
- Precision-engineered for perfect OEM compatibility
- Manufactured from premium-grade industrial materials
- Stringent quality control and testing procedures
- Designed for heavy-duty operational environments
- Ensures reliable performance under demanding conditions

Benefits:
- Reduces equipment downtime and maintenance costs
- Extends overall equipment lifespan significantly
- Maintains original equipment performance standards
- Provides seamless integration with existing systems
- Delivers consistent operation in challenging environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial centrifuge machine spares maintain continuous operations in industries where separation and clarification processes are critical. These components ensure equipment operates at peak efficiency while minimizing production disruptions and maintaining consistent output quality across demanding environments. These precision spares replace worn or damaged parts in centrifuges used for liquid-solid separation and chemical processing. They restore original equipment performance while providing enhanced durability and reliability for extended service intervals in challenging industrial conditions.
Real-world applications:
- Chemical manufacturing plants for precise separation processes
- Pharmaceutical production facilities for ingredient purification
- Wastewater treatment plants for efficient sludge dewatering
- Food processing units for product clarification and purification
- Mining operations for accurate material classification and recovery
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anna Company, West Bengal
 West Bengal, India
Services & Support•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Centrifuge Machine Spares For Chemical Pharmaceutical Wastewater
Premium industrial centrifuge machine spares ensure reliable performance and extended equipment life for chemical, pharmaceutical, and wastewater treatment applications with precision-engineered replacement parts.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anna Company
 West Bengal, India
Services & SupportManufacturer