IN
₹
Apparel & Fashion
Description
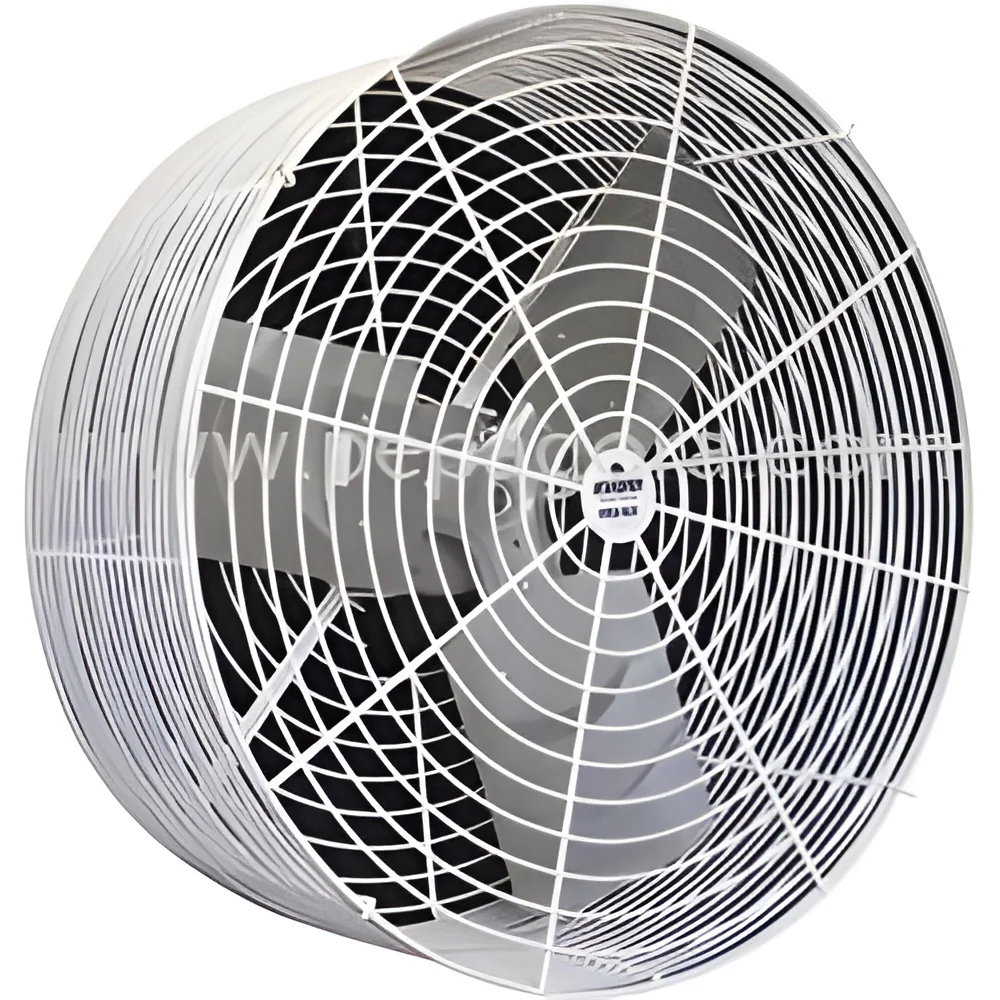
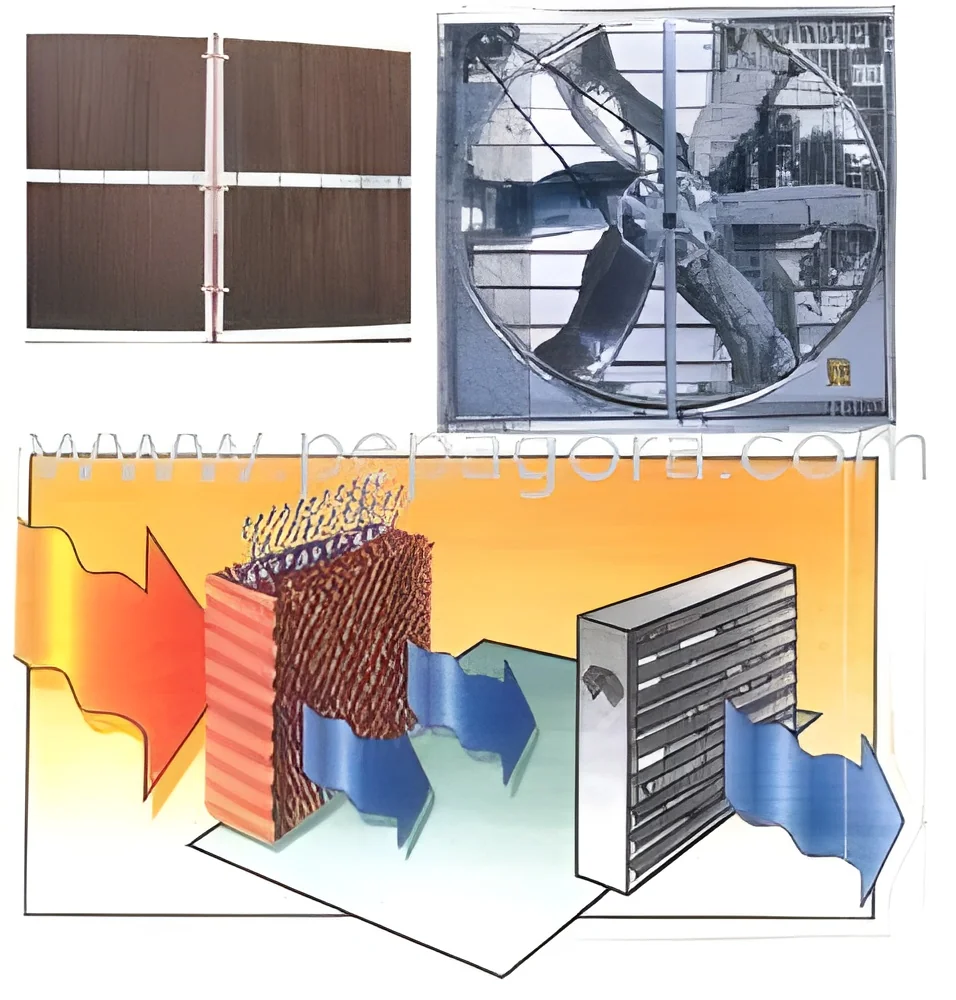
Our premium humidity control equipment provides precise environmental management for critical applications where moisture control directly impacts product quality and operational efficiency. Manufactured using high-grade corrosion-resistant materials and advanced sensor technology, these systems deliver consistent performance and long-term reliability even in the most demanding conditions. The equipment features intelligent control systems that maintain exact humidity levels while optimizing energy consumption, making them ideal for businesses that require dependable environmental control solutions for their valuable products and processes.

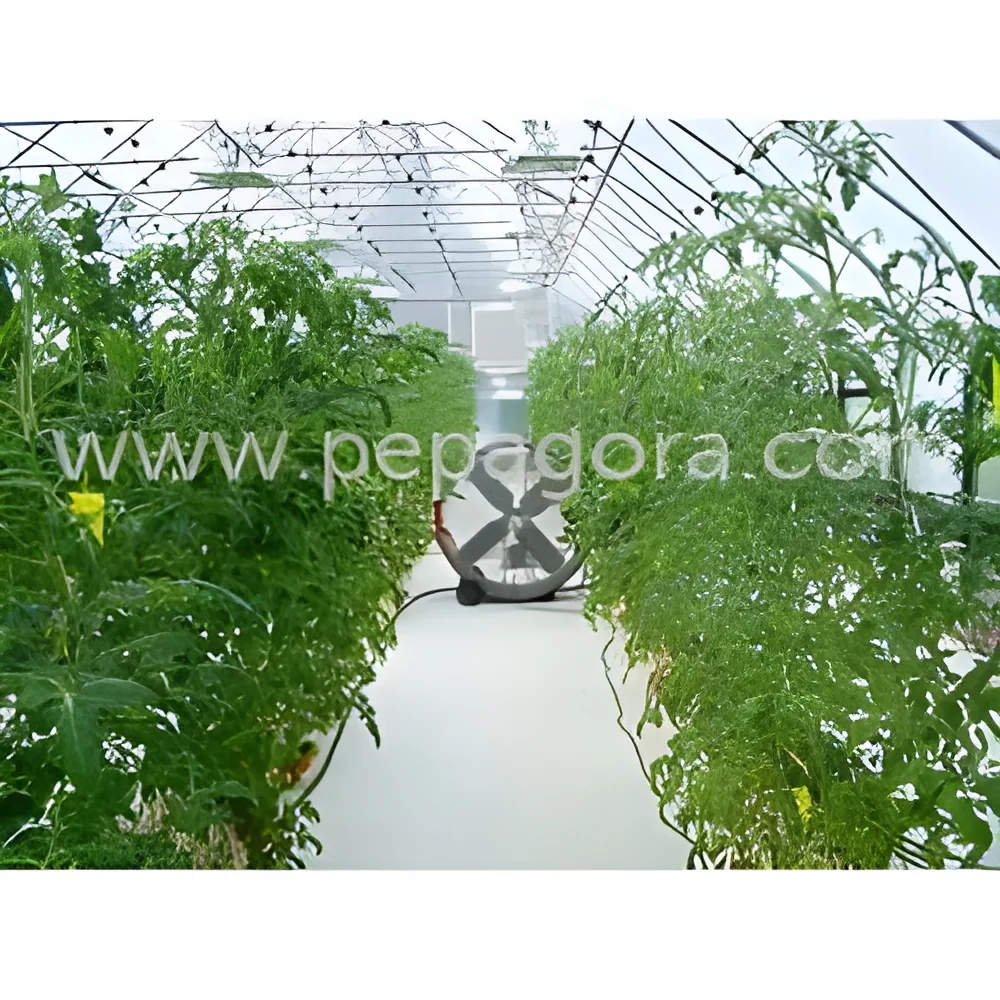
This humidity control equipment serves multiple industries including food storage and preservation facilities where it prevents spoilage and extends shelf life, agricultural operations for proper drying and storage of produce, pharmaceutical manufacturing environments that require strict climate control, laboratory settings needing precise atmosphe...
Our premium humidity control equipment provides precise environmental management for critical applications where moisture control directly impacts product quality and operational efficiency. Manufactured using high-grade corrosion-resistant materials and advanced sensor technology, these systems deliver consistent performance and long-term reliability even in the most demanding conditions. The equipment features intelligent control systems that maintain exact humidity levels while optimizing energy consumption, making them ideal for businesses that require dependable environmental control solutions for their valuable products and processes.

This humidity control equipment serves multiple industries including food storage and preservation facilities where it prevents spoilage and extends shelf life, agricultural operations for proper drying and storage of produce, pharmaceutical manufacturing environments that require strict climate control, laboratory settings needing precise atmospheric conditions, and industrial manufacturing processes where humidity affects production quality. The systems are designed to meet the specific requirements of each sector, ensuring compliance with industry standards and maintaining optimal conditions for various materials and products.

We deliver reliable humidity control solutions that protect your investments and enhance operational efficiency. Our equipment combines robust construction with user-friendly interfaces and adaptable configurations to meet diverse industrial needs. The systems are engineered for hassle-free performance with minimal maintenance requirements, providing businesses with cost-effective environmental management that reduces energy consumption while ensuring consistent product quality and compliance with regulatory standards.

Key Features:
- Advanced sensor technology for precise humidity monitoring
- High-grade corrosion-resistant construction materials
- Intelligent control systems for automated operation
- Energy-efficient operation with optimized consumption
- User-friendly interface for easy monitoring and control

Benefits:
- Prevents product spoilage and extends shelf life
- Reduces energy consumption and operational costs
- Ensures consistent product quality and compliance
- Minimizes maintenance requirements and downtime
- Provides reliable performance in demanding conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our humidity control equipment maintains exact moisture levels in critical environments, ensuring product integrity and preventing spoilage across various industries. These systems are engineered for reliability and consistent performance in demanding operational conditions where accurate humidity regulation is essential for quality preservation and process efficiency.
Designed for food storage facilities, agricultural operations, and industrial applications, our equipment delivers solutions that meet specific environmental requirements. The systems provide optimal conditions for perishable goods, manufacturing processes, and sensitive materials while offering energy-efficient operation and minimal maintenance needs for long-term cost savings.
- Food storage warehouses and cold storage facilities
- Agricultural produce drying and storage operations
- Pharmaceutical manufacturing and clean room environments
- Laboratory climate control and research facilities
- Industrial manufacturing and processing plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Venkateshwara Agrotech Industries, Maharashtra
 Maharashtra, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Humidity Control Equipment For Food Storage Agriculture Industrial
Premium humidity control equipment for precise environmental management in food storage, agriculture, and industrial applications. Built with high-quality materials for reliable performance and consistent operation.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Venkateshwara Agrotech Industries
 Maharashtra, India
Electronics & ElectricalManufacturer