
 IN
₹
Apparel & Fashion
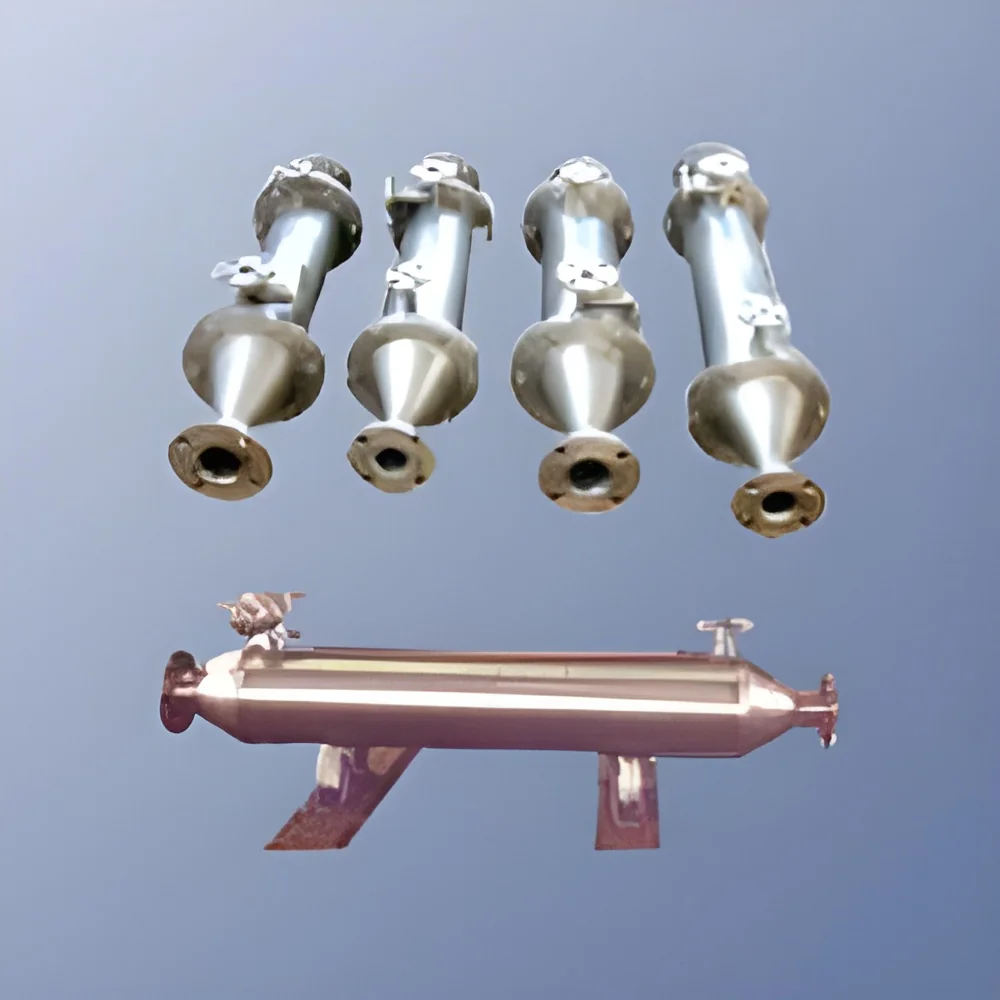
Description
Our industrial shell and tube heat exchangers represent the pinnacle of thermal management technology, engineered specifically for demanding industrial environments. Fabricated from premium stainless steel grades including SS 304, SS 316, and SS 316L, these heat exchangers deliver exceptional performance with superior resistance to heat, corrosion, abrasion, and rust. The robust construction ensures long-term operational reliability while maintaining optimal heat transfer efficiency between process fluids. Designed to meet rigorous industry standards, they provide dependable operation with straightforward installation procedures and minimal maintenance requirements, making them the ideal thermal management solution for businesses seeking equipment that performs consistently under challenging conditions.

These heat exchangers find extensive application across multiple industries where precise temperature control is essential for operational success. In chemical and pharmaceutical secto...
Our industrial shell and tube heat exchangers represent the pinnacle of thermal management technology, engineered specifically for demanding industrial environments. Fabricated from premium stainless steel grades including SS 304, SS 316, and SS 316L, these heat exchangers deliver exceptional performance with superior resistance to heat, corrosion, abrasion, and rust. The robust construction ensures long-term operational reliability while maintaining optimal heat transfer efficiency between process fluids. Designed to meet rigorous industry standards, they provide dependable operation with straightforward installation procedures and minimal maintenance requirements, making them the ideal thermal management solution for businesses seeking equipment that performs consistently under challenging conditions.

These heat exchangers find extensive application across multiple industries where precise temperature control is essential for operational success. In chemical and pharmaceutical sectors, they facilitate critical processes including heating, cooling, and condensation while maintaining product integrity and purity standards. The food processing industry relies on them for pasteurization, sterilization, and various thermal processing applications where hygiene and efficiency are non-negotiable requirements. Power generation facilities utilize them for steam production and cooling systems, while manufacturing plants depend on them for precise process temperature regulation. Their versatility and adaptability make them suitable for virtually any industrial application requiring reliable thermal management solutions.

The business value of our shell and tube heat exchangers lies in their proven reliability and operational efficiency, directly contributing to reduced operational downtime and lower maintenance expenditures. Their durable construction ensures extended service life, providing exceptional return on investment through consistent performance over many years of operation. The design flexibility allows for seamless integration into existing systems, optimizing workflow efficiency and process outcomes. These units are engineered for trouble-free operation with simplified installation processes, minimizing implementation time and associated costs. The combination of premium materials, innovative engineering, and demonstrated performance makes them a trustworthy investment for businesses seeking industrial equipment that delivers both immediate operational benefits and long-term value.

Key Features:
- Constructed with premium SS 304, SS 316, and SS 316L stainless steel materials
- Superior resistance to heat, corrosion, abrasion, and rust for extended durability
- Robust construction ensuring long-term reliability in demanding environments
- Straightforward installation process with minimal maintenance requirements
- Adaptable design to accommodate specific operational and industry needs

Benefits:
- Enhanced operational efficiency through optimal heat transfer performance
- Reduced maintenance costs and extended equipment service life
- Reliable performance in high-pressure and high-temperature applications
- Versatile application across multiple industrial sectors and processes
- Cost-effective thermal management solution with excellent ROI
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Shell and tube heat exchangers provide efficient thermal management in demanding industrial environments by transferring heat between liquids and gases without mixing. Their robust construction handles high pressures and temperatures while maintaining precise temperature control, making them essential for processes where reliability is critical and operational downtime must be minimized across various industrial sectors and applications requiring consistent thermal performance.
These versatile heat exchangers serve vital functions in chemical processing, power generation, food production, and pharmaceutical manufacturing. They efficiently perform heating, cooling, condensation, and evaporation processes while maintaining strict operational parameters. The adaptable design allows for optimization to meet specific process requirements, ensuring peak performance across diverse industrial systems from large-scale manufacturing operations to specialized processing applications requiring precise thermal control.
- Chemical processing plants for reactor temperature control and fluid heating/cooling
- Food and beverage industry for pasteurization, sterilization, and product heating
- Power generation facilities for steam systems and turbine cooling applications
- Pharmaceutical manufacturing for maintaining precise temperatures in production
- Industrial HVAC systems for large commercial and manufacturing facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Delpro Equipments Private Ltd., Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Shell And Tube Heat Exchanger SS 304/316/316L
Industrial shell and tube heat exchangers in SS 304/316/316L deliver superior heat transfer and corrosion resistance for chemical, pharmaceutical, and food processing applications with reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Delpro Equipments Private Ltd.
 Maharashtra, India
Industrial Equipment & MachineryManufacturer


