IN
₹
Apparel & Fashion
Description
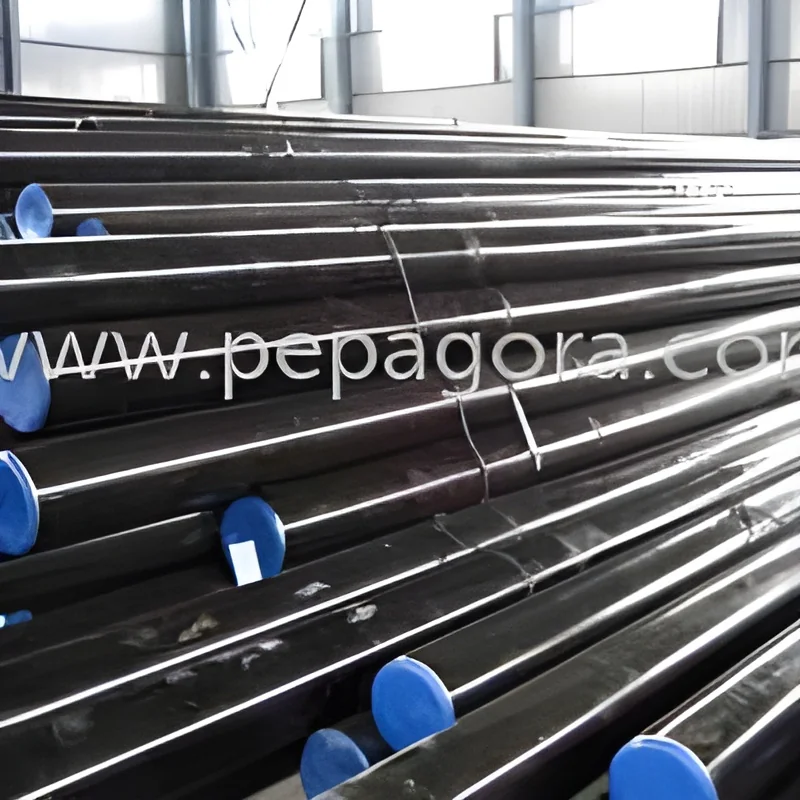
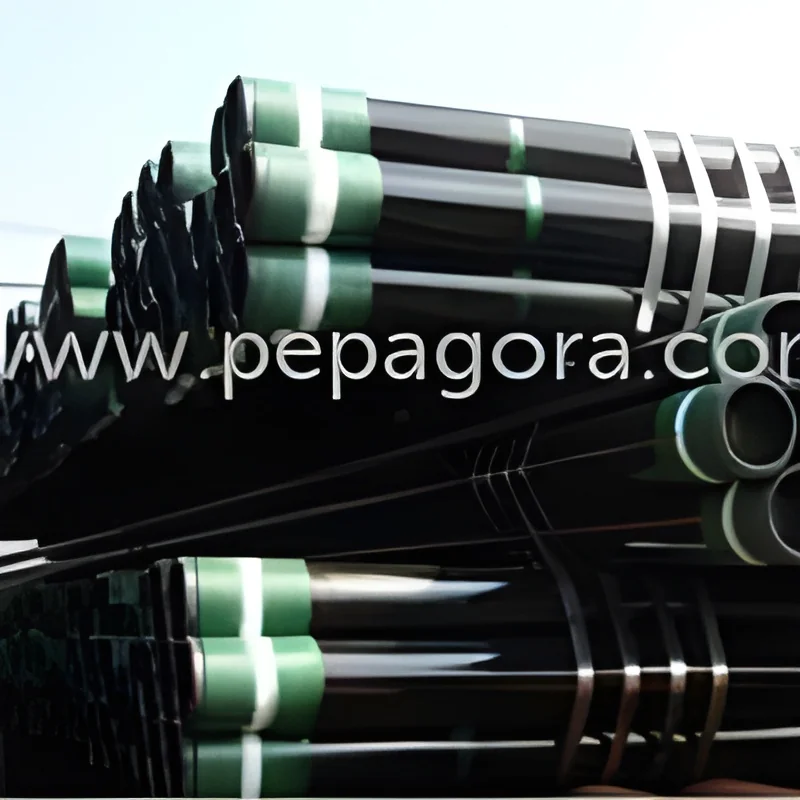
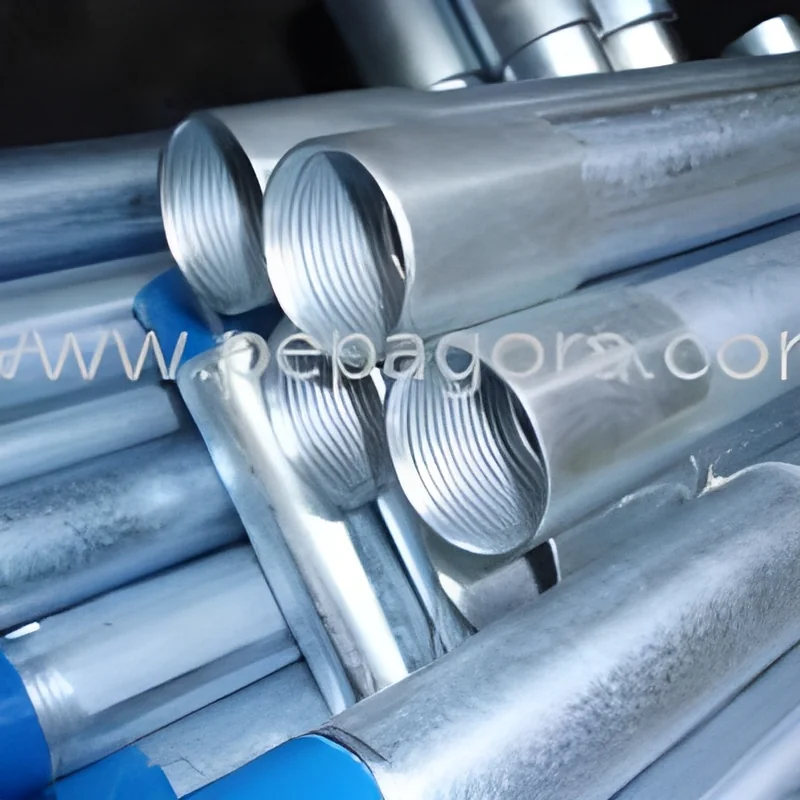
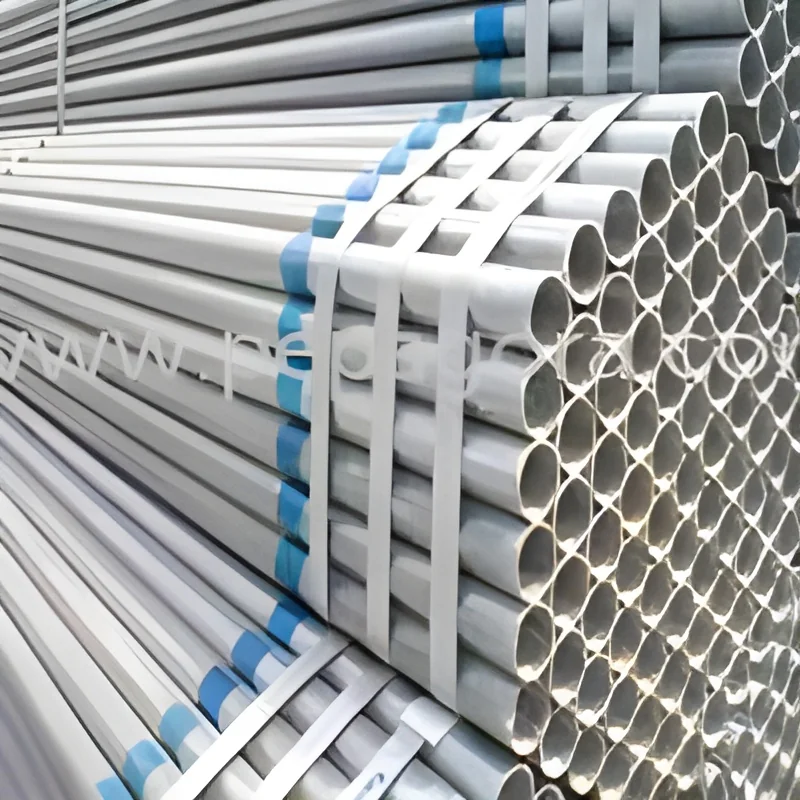
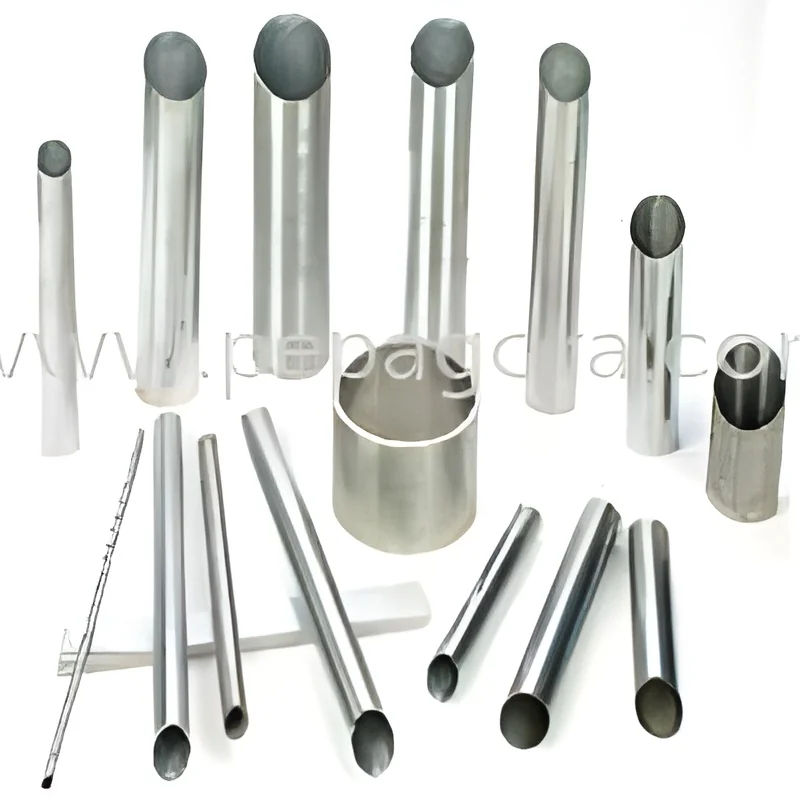
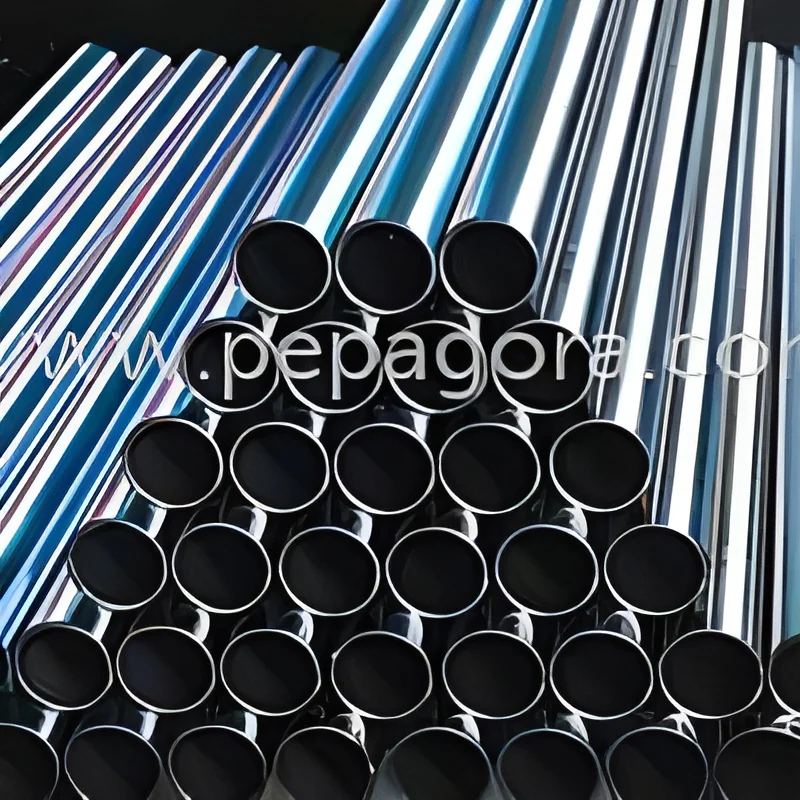
Our industrial heat exchanger steel tubes are precision-engineered for demanding thermal management applications. Crafted from high-grade corrosion-resistant steel, they ensure optimal heat transfer efficiency under extreme temperatures and pressures. Designed for durability and long service life, these tubes meet rigorous international standards, providing a reliable component for critical heat exchange systems. They are trusted by global industries for consistent performance, reducing operational risks and enhancing system longevity in the most challenging environments.

These tubes are indispensable across heavy industries including power generation, chemical processing, oil and gas, HVAC, and marine engineering. In power plants, they facilitate efficient steam condensation and heat recovery. Chemical plants rely on their corrosion resistance for handling aggressive fluids and exothermic reactions. Oil refineries utilize them in crude oil heating, cooling, and fractionation processe...
Our industrial heat exchanger steel tubes are precision-engineered for demanding thermal management applications. Crafted from high-grade corrosion-resistant steel, they ensure optimal heat transfer efficiency under extreme temperatures and pressures. Designed for durability and long service life, these tubes meet rigorous international standards, providing a reliable component for critical heat exchange systems. They are trusted by global industries for consistent performance, reducing operational risks and enhancing system longevity in the most challenging environments.

These tubes are indispensable across heavy industries including power generation, chemical processing, oil and gas, HVAC, and marine engineering. In power plants, they facilitate efficient steam condensation and heat recovery. Chemical plants rely on their corrosion resistance for handling aggressive fluids and exothermic reactions. Oil refineries utilize them in crude oil heating, cooling, and fractionation processes. HVAC systems benefit from their thermal efficiency in large-scale climate control, while marine applications depend on their robustness for engine cooling and heat management in harsh saltwater conditions.

The business value of these heat exchanger tubes lies in their ability to lower operational costs through enhanced energy efficiency and reduced maintenance needs. Their corrosion-resistant construction ensures extended service life, minimizing downtime and replacement expenses. Engineered for reliability under high pressure and temperature, they provide a trusted solution for serious buyers seeking quality and performance. This makes them a strategic investment for businesses aiming to optimize thermal processes, ensure process safety, and achieve sustainable operational excellence.

Key Features:
- High thermal conductivity for efficient heat transfer in industrial systems.
- Corrosion-resistant steel construction ensuring longevity in harsh environments.
- Precision engineering for consistent performance under extreme pressure and temperature.
- Compliance with international quality standards for reliability and safety.
- Durable design for reduced maintenance and long service life.

Benefits:
- Enhances energy efficiency, lowering operational costs and energy consumption.
- Reduces maintenance frequency and downtime due to corrosion resistance and durability.
- Provides reliable performance in critical applications, ensuring process safety and continuity.
- Offers long service life, delivering a strong return on investment over time.
- Suitable for integration into diverse industrial systems for versatile thermal management.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial-grade heat exchanger steel tubes are engineered for superior thermal transfer in high-pressure and high-temperature systems. They provide reliable performance where efficiency and durability are critical, ensuring stable operations across various demanding sectors. Their robust construction and precise engineering make them suitable for diverse industrial environments that require exact thermal management and consistent heat exchange under extreme conditions.
These tubes serve essential functions in power generation, chemical processing, oil and gas refining, HVAC systems, and marine applications. They are designed to handle aggressive fluids, high thermal loads, and corrosive atmospheres, offering a dependable solution for maintaining process integrity and operational safety in complex industrial setups.
- Power generation plants for steam condensation, heat recovery, and boiler systems.
- Chemical processing units handling corrosive fluids, high-temperature reactions, and heat transfer.
- Oil refineries for crude oil heating, cooling, fractionation, and heat exchanger networks.
- HVAC systems in large commercial buildings and industrial facilities for efficient climate control.
- Marine engineering applications including shipboard cooling systems and engine heat management.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Eminent Exports India, Uttar Pradesh
 Uttar Pradesh, India
Construction•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Heat Exchanger Steel Tubes High Thermal Efficiency Corrosion Resistant
Industrial heat exchanger steel tubes deliver high thermal efficiency and corrosion resistance for power plants, refineries, and chemical processing. Trusted for reliability in demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Eminent Exports India
 Uttar Pradesh, India
ConstructionManufacturer