IN
₹
Description
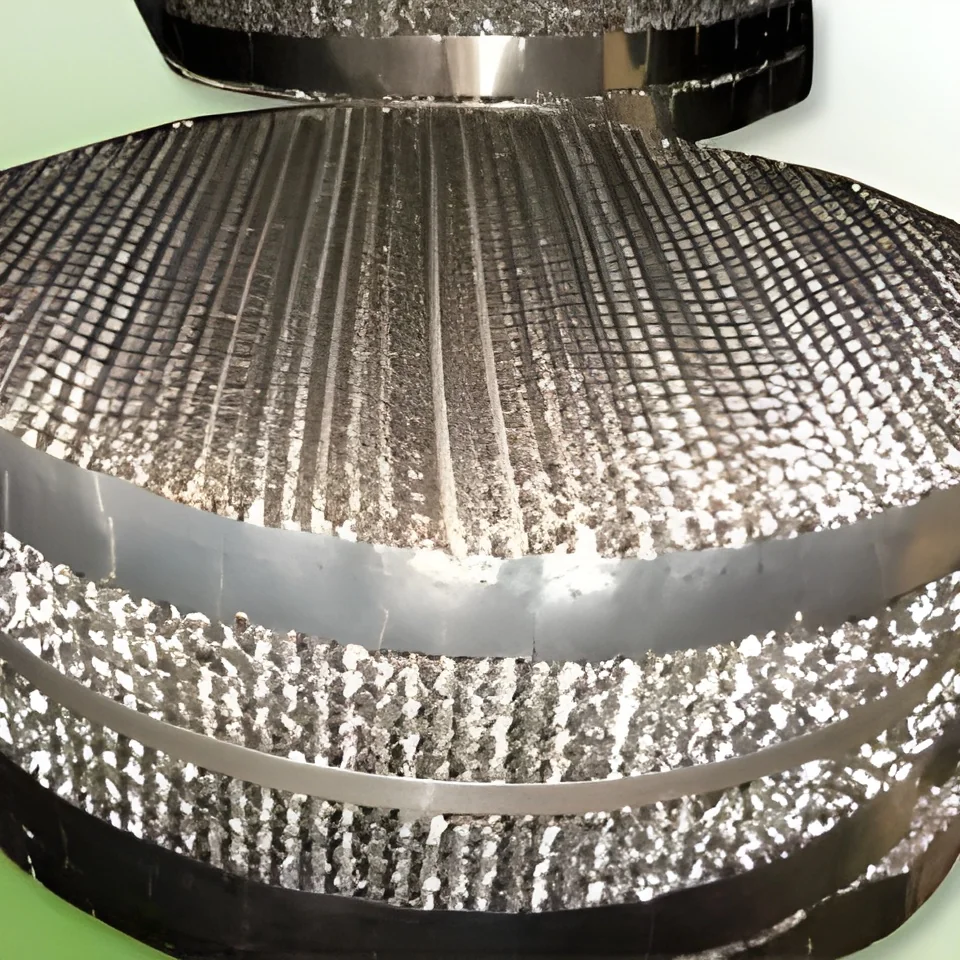
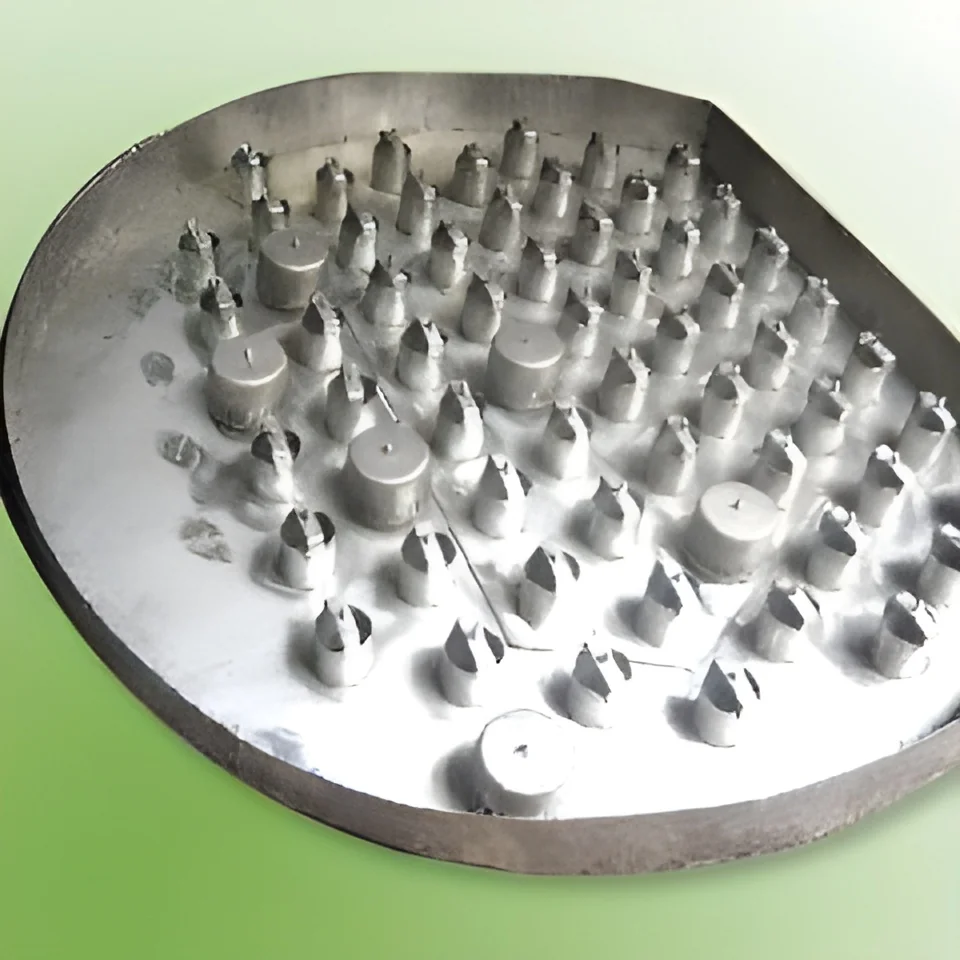
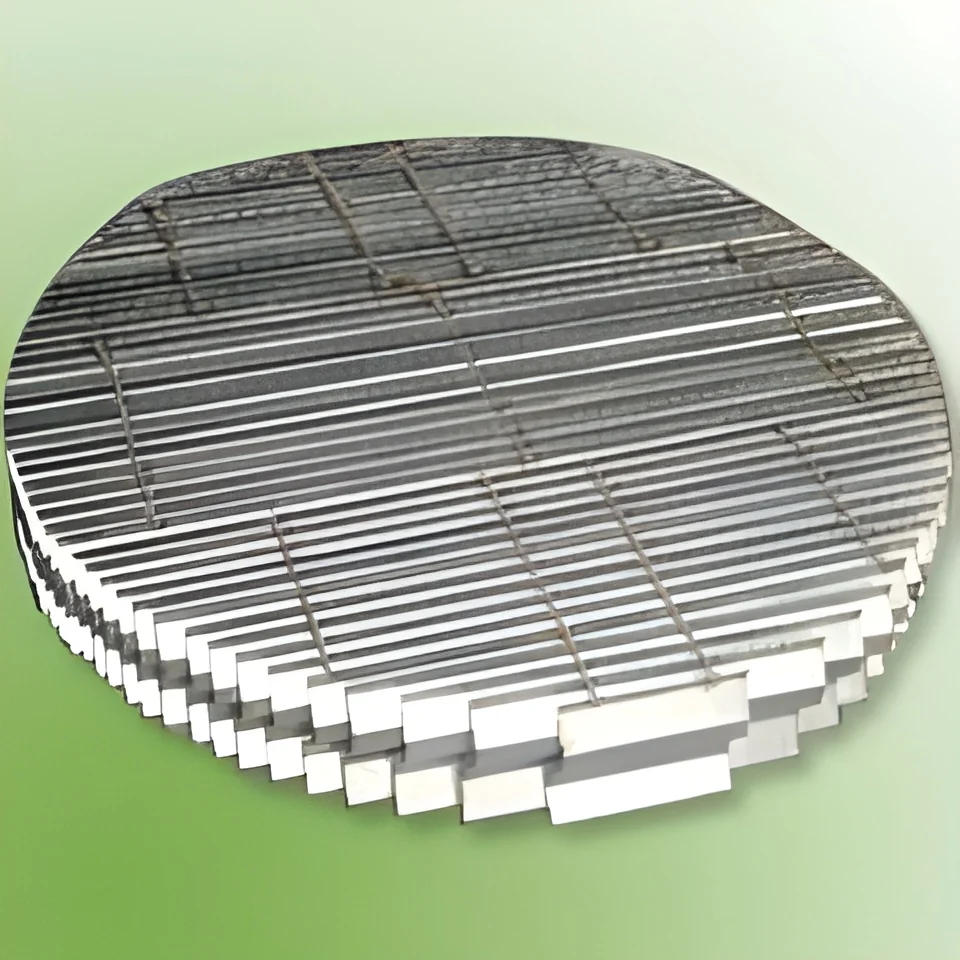
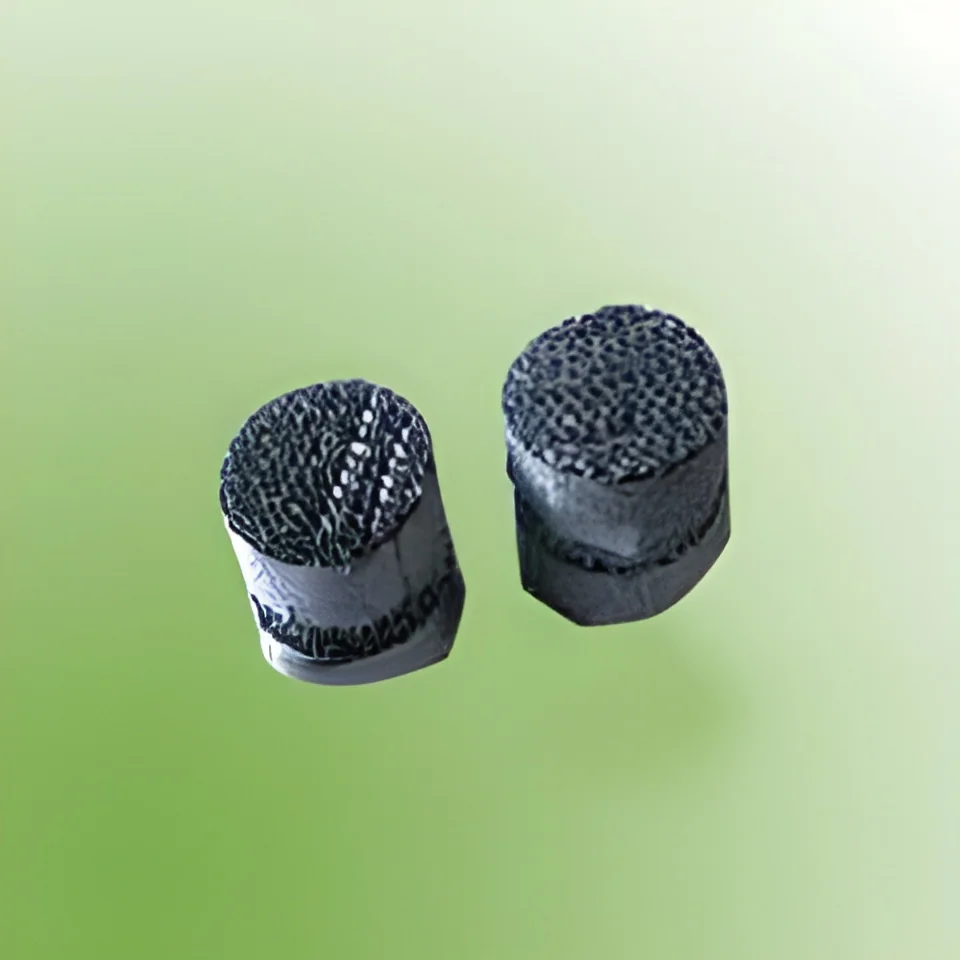
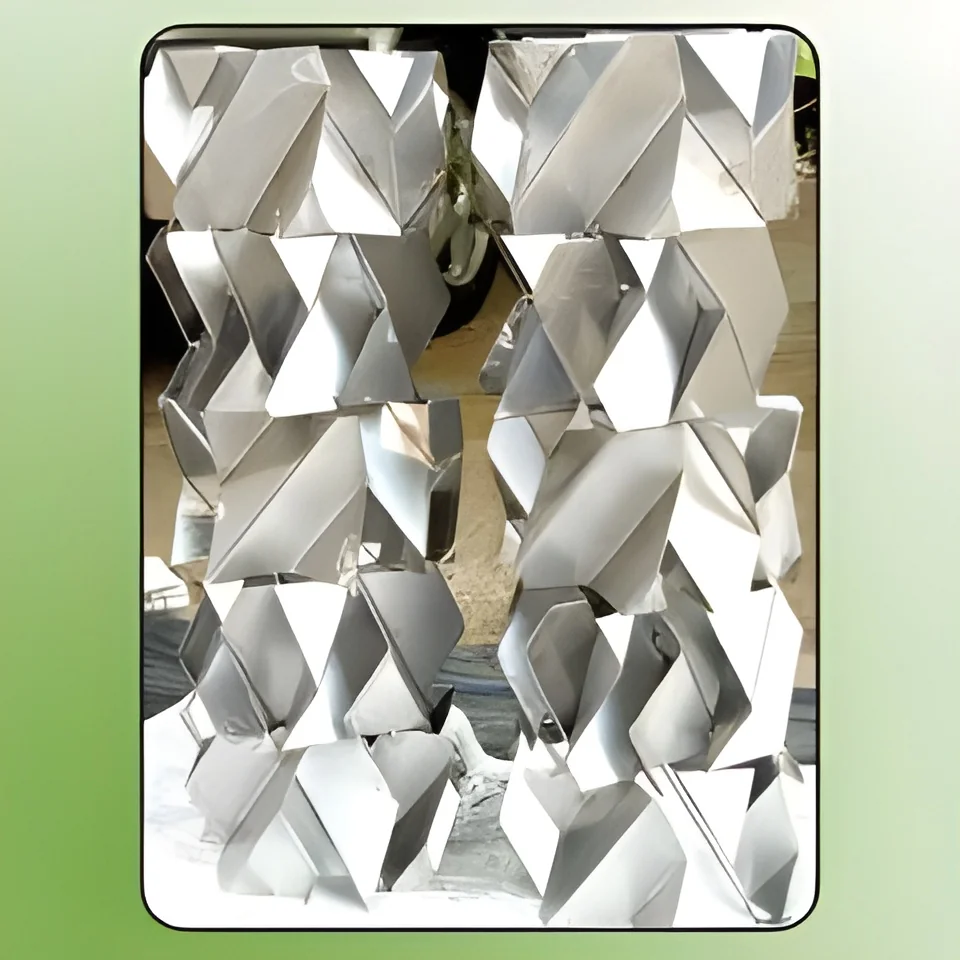
Industrial Liquid Liquid Extraction Packing represents advanced separation technology designed for efficient mass transfer between immiscible liquids in extraction columns. Manufactured from high-quality stainless steel with superior anti-corrosive properties, these packings provide exceptional durability in aggressive chemical environments. Their engineered structure maximizes interfacial contact area, enabling more effective separation while allowing for shorter column designs and more compact plant layouts. This optimization reduces overall system footprint and installation complexity while maintaining high extraction efficiency across various processing conditions and fluid combinations.

Multiple industries depend on these extraction packings for critical separation processes that demand reliability and precision. Pharmaceutical manufacturers utilize them for extracting active pharmaceutical ingredients from natural sources and synthetic reaction mixtures, ensuring high purity yie...
Industrial Liquid Liquid Extraction Packing represents advanced separation technology designed for efficient mass transfer between immiscible liquids in extraction columns. Manufactured from high-quality stainless steel with superior anti-corrosive properties, these packings provide exceptional durability in aggressive chemical environments. Their engineered structure maximizes interfacial contact area, enabling more effective separation while allowing for shorter column designs and more compact plant layouts. This optimization reduces overall system footprint and installation complexity while maintaining high extraction efficiency across various processing conditions and fluid combinations.

Multiple industries depend on these extraction packings for critical separation processes that demand reliability and precision. Pharmaceutical manufacturers utilize them for extracting active pharmaceutical ingredients from natural sources and synthetic reaction mixtures, ensuring high purity yields. Chemical production facilities employ these packings in purification systems for intermediates and specialty chemicals, while petrochemical operations integrate them into solvent recovery and impurity removal systems. The food processing sector applies them in decaffeination and flavor extraction processes, and environmental management systems utilize them for wastewater treatment and valuable resource recovery from industrial effluents.

The business value of these extraction packings lies in their proven reliability, operational efficiency, and long-term cost-effectiveness. Their durable stainless steel construction ensures extended service life even in corrosive environments, significantly reducing replacement frequency and maintenance expenses. The optimized design minimizes pressure drop and energy consumption while enhancing processing throughput, directly contributing to lower operational costs. The high-efficiency mass transfer capabilities ensure consistent output quality and improved extraction yields, providing dependable performance that supports continuous production schedules and process optimization goals across various industrial applications.

Key Features:
- Constructed from durable stainless steel for longevity in harsh environments
- Anti-corrosive properties resistant to aggressive chemicals and high temperatures
- High surface area-to-volume ratio for efficient mass transfer performance
- Reduces required column height and overall plant footprint
- Engineered for stable performance in continuous extraction processes

Benefits:
- Extended service life reduces replacement and maintenance costs
- Improved separation efficiency enhances product purity and yield
- Lower energy consumption through optimized flow characteristics
- Space-saving design reduces installation and facility costs
- Reliable performance ensures consistent processing outcomes
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These stainless steel extraction packings deliver superior performance in liquid-liquid separation processes by maximizing surface area contact between immiscible fluids. Their robust anti-corrosive construction ensures consistent operation in challenging chemical environments, maintaining efficiency while reducing maintenance requirements and operational downtime across various industrial settings.
Engineered for precision separation tasks, these packings support diverse industrial applications where reliable extraction is critical. The durable stainless steel material withstands aggressive chemicals and high-temperature conditions, making them suitable for continuous processing operations in demanding environments while ensuring long-term performance stability and process consistency.
- Pharmaceutical manufacturing for extracting active ingredients from natural and synthetic sources
- Chemical production facilities for purifying intermediates and separating organic compounds
- Petrochemical operations for solvent recovery and impurity removal processes
- Food processing industry for decaffeination and essential oil extraction
- Environmental management systems for wastewater treatment and metal recovery
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Yogi Structured Packings & Engineering, Maharashtra
 Maharashtra, India
Tools & Hardware•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Liquid Liquid Extraction Packing Stainless Steel Anti Corrosive
Industrial Liquid Liquid Extraction Packing offers high-efficiency separation with durable stainless steel anti-corrosive construction, ideal for chemical, pharmaceutical, and petrochemical processing applications requiring reliable mass transfer performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Yogi Structured Packings & Engineering
 Maharashtra, India
Tools & HardwareManufacturer