IN
₹
Apparel & Fashion

Description
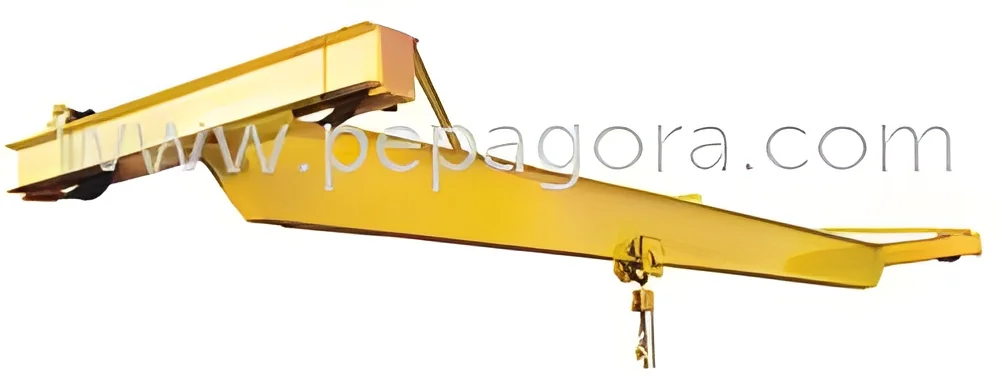
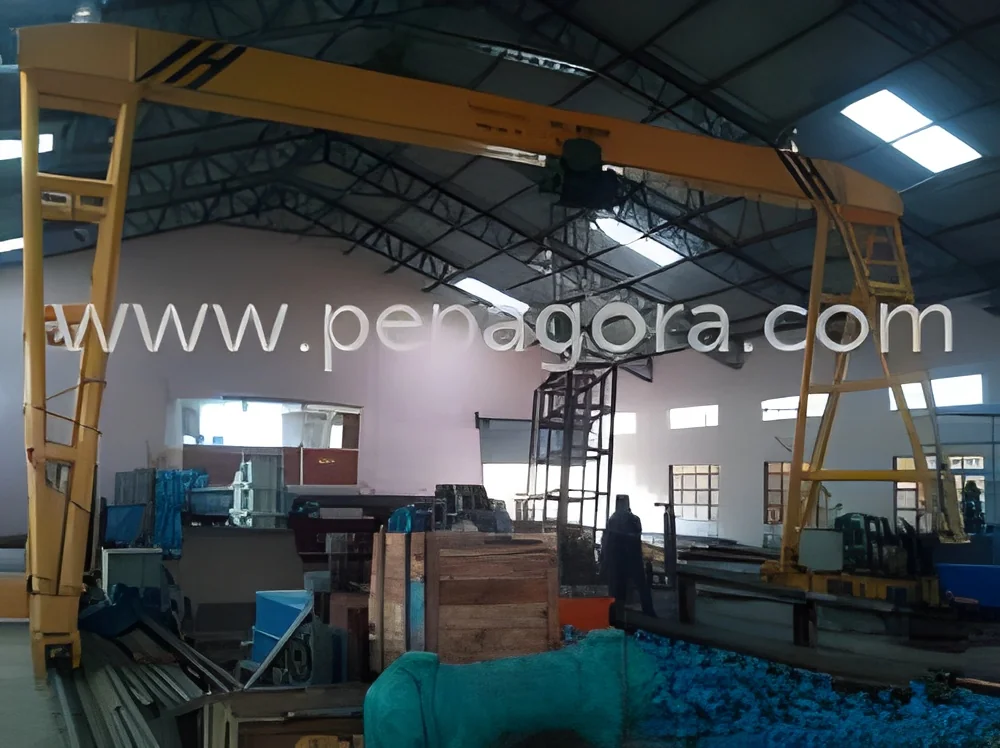
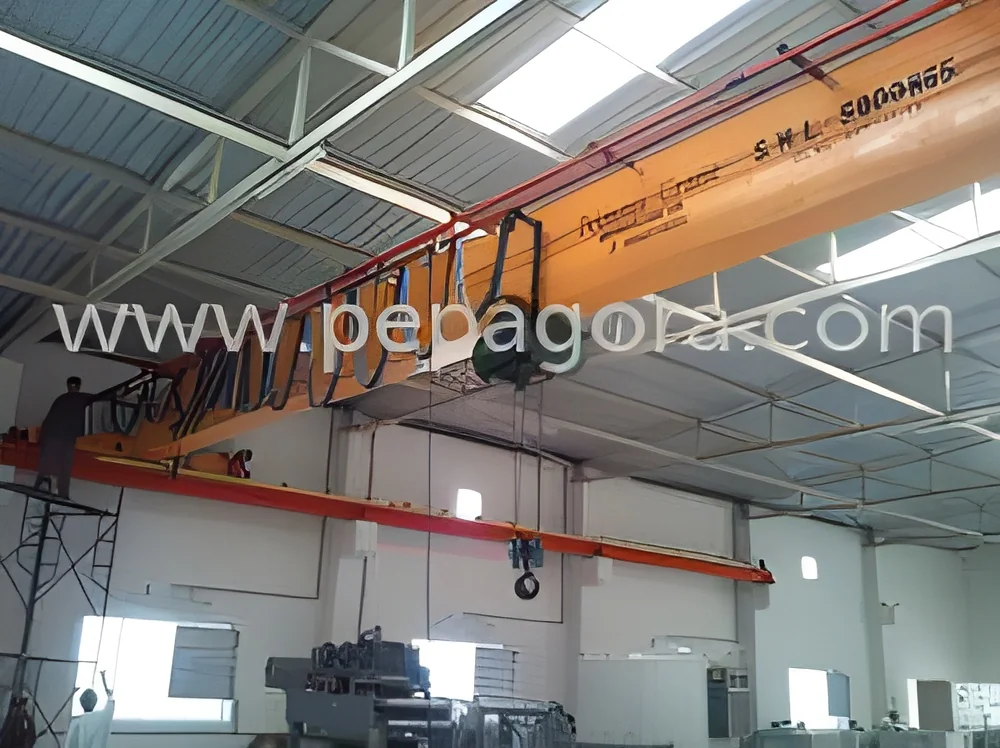
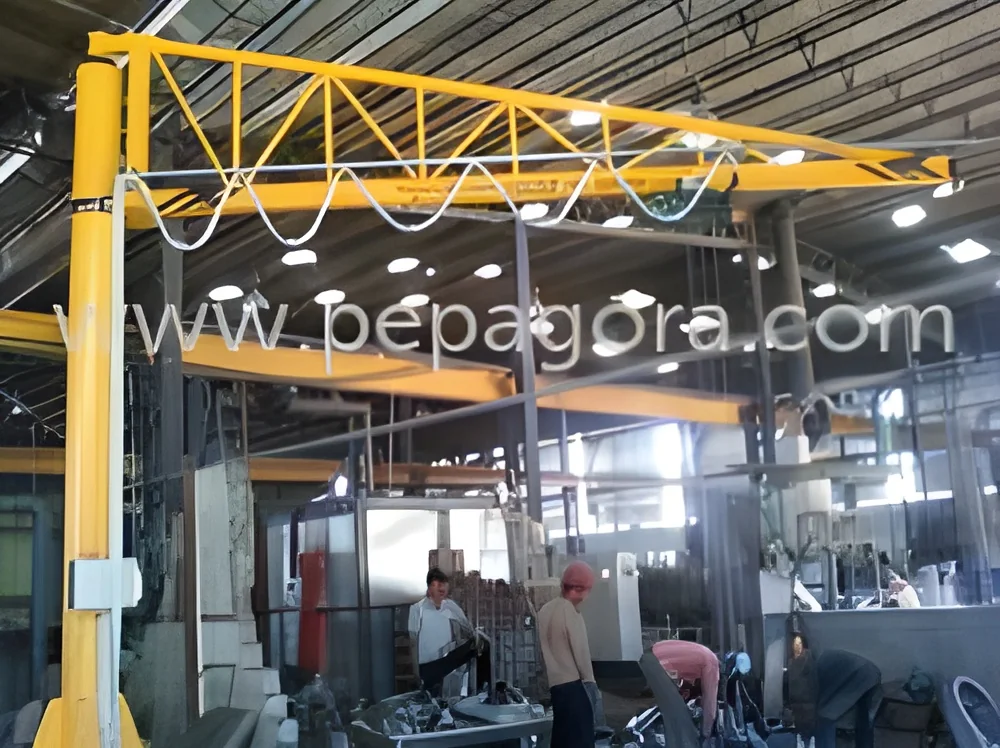
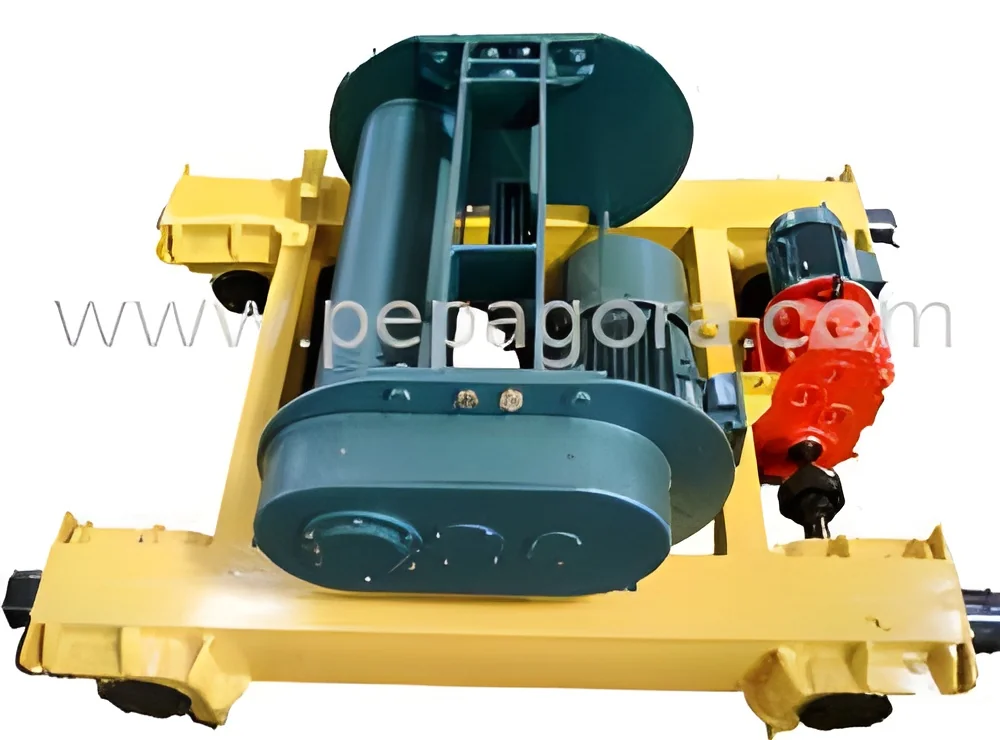
Heavy industrial cranes represent the pinnacle of material handling engineering, specifically designed for demanding applications in construction and manufacturing sectors. Built with robust steel structures and precision-engineered components, these cranes deliver reliable performance under extreme loads and challenging working conditions. Each unit undergoes rigorous quality testing and complies with international safety standards, ensuring unmatched durability and operational efficiency for industrial operations requiring heavy lifting capabilities and precise load positioning in various work environments.

These cranes serve vital roles across multiple industrial sectors, including construction sites for lifting structural elements, manufacturing facilities for assembly line operations, warehouses for inventory management, and ports for cargo handling operations. They prove particularly valuable in infrastructure development projects, steel manufacturing plants, automotive producti...
Heavy industrial cranes represent the pinnacle of material handling engineering, specifically designed for demanding applications in construction and manufacturing sectors. Built with robust steel structures and precision-engineered components, these cranes deliver reliable performance under extreme loads and challenging working conditions. Each unit undergoes rigorous quality testing and complies with international safety standards, ensuring unmatched durability and operational efficiency for industrial operations requiring heavy lifting capabilities and precise load positioning in various work environments.

These cranes serve vital roles across multiple industrial sectors, including construction sites for lifting structural elements, manufacturing facilities for assembly line operations, warehouses for inventory management, and ports for cargo handling operations. They prove particularly valuable in infrastructure development projects, steel manufacturing plants, automotive production facilities, and logistics centers where heavy lifting capacity and accurate positioning are essential operational requirements. The adaptability of these cranes makes them suitable for both indoor factory settings and outdoor construction environments, providing versatile material handling solutions across diverse industrial applications and operational scenarios.

Investing in industrial cranes delivers significant business value through improved operational efficiency, reduced labor costs, and enhanced workplace safety protocols. These cranes are engineered for long-term reliability with minimal maintenance requirements, ensuring continuous operation and maximum uptime for production schedules and project timelines. The robust engineering and quality assurance behind each crane provide dependable performance that supports business growth and operational scalability, making them a strategic investment for companies looking to enhance their industrial capabilities and maintain competitive advantage in their respective markets.

Key Features:
- Robust steel construction designed for heavy-duty industrial applications
- High load capacity suitable for demanding lifting requirements
- Precision control systems enabling accurate load positioning
- Compliance with international safety standards and quality certifications
- Adaptable configurations for diverse industrial environments

Benefits:
- Enhanced operational efficiency through reliable performance
- Reduced labor costs with automated heavy lifting capabilities
- Improved workplace safety with built-in safety features
- Long-term reliability with minimal maintenance requirements
- Versatile application across multiple industrial settings
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heavy industrial cranes deliver essential material handling capabilities across construction projects and manufacturing facilities. These robust systems enable safe lifting and precise positioning of heavy loads, significantly reducing manual labor while improving workflow efficiency in demanding industrial environments. Their durable construction ensures consistent performance under heavy usage conditions across various operational settings.
These cranes serve critical functions in assembly line operations, warehouse management, and infrastructure development projects. Their versatile design makes them suitable for both indoor manufacturing plants and outdoor construction sites, ensuring seamless integration into existing workflows while maintaining high productivity and safety standards across diverse industrial applications.
- Lifting structural steel beams and concrete panels at construction sites
- Assembling heavy machinery components in manufacturing plants
- Loading and unloading cargo containers in ports and logistics yards
- Supporting maintenance operations in large industrial facilities
- Handling raw materials and finished products in warehouse storage
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Pegasus Technocrats, Karnataka
 Karnataka, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Industrial Cranes for Construction and Manufacturing
Heavy industrial cranes provide reliable lifting solutions for construction and manufacturing with high load capacity and precision handling for demanding operational environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Pegasus Technocrats
 Karnataka, India
Industrial Equipment & MachineryManufacturer