IN
₹
Apparel & Fashion

Description
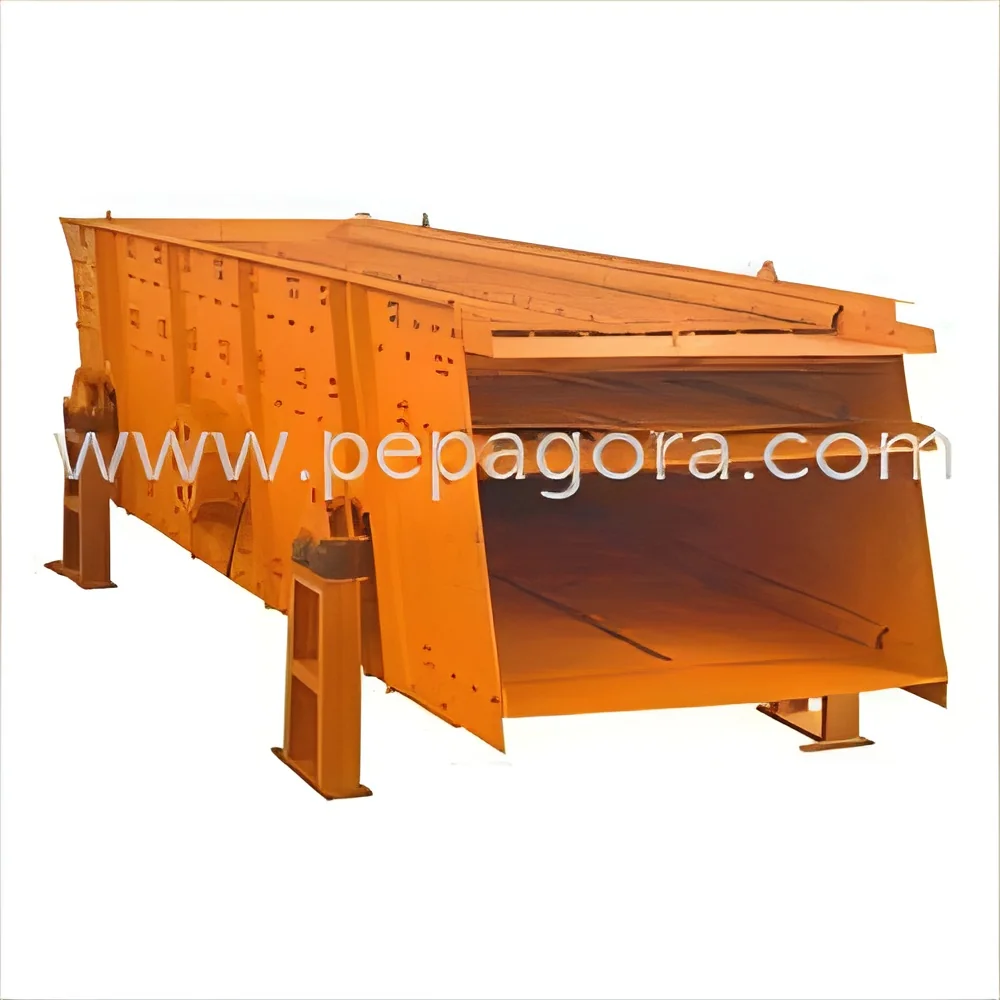
Industrial circular vibrating screens are engineered for precise particle separation across demanding industrial applications. Utilizing a circular motion vibration mechanism, these screens efficiently separate materials by size while minimizing common issues like blinding and clogging. Built with durable components and robust construction, they deliver consistent performance in continuous operation environments. The design focuses on reliability and efficiency, ensuring accurate grading of powders, granules, and other materials essential for quality control in various processing operations. These machines represent a practical solution for businesses requiring dependable screening equipment that maintains performance under heavy use conditions.

These screening systems serve critical functions across multiple industries where particle size control directly impacts product quality. In food processing, they ensure consistent ingredient grading while meeting hygiene requirements. Pharmac...
Industrial circular vibrating screens are engineered for precise particle separation across demanding industrial applications. Utilizing a circular motion vibration mechanism, these screens efficiently separate materials by size while minimizing common issues like blinding and clogging. Built with durable components and robust construction, they deliver consistent performance in continuous operation environments. The design focuses on reliability and efficiency, ensuring accurate grading of powders, granules, and other materials essential for quality control in various processing operations. These machines represent a practical solution for businesses requiring dependable screening equipment that maintains performance under heavy use conditions.

These screening systems serve critical functions across multiple industries where particle size control directly impacts product quality. In food processing, they ensure consistent ingredient grading while meeting hygiene requirements. Pharmaceutical manufacturers rely on them for accurate separation in drug formulation processes. The chemical industry utilizes circular screens for powder classification and impurity removal, while mining operations depend on them for sorting crushed materials efficiently. Recycling facilities benefit from their ability to separate different materials, making them essential tools for operations requiring precise material separation and quality assurance.

The business value of these circular vibrating screens extends to operational reliability and long-term efficiency gains. Their durable construction reduces maintenance requirements and minimizes unexpected downtime, supporting continuous production schedules. Precise screening capabilities improve product consistency while reducing material waste, directly impacting operational costs. The equipment's efficient design optimizes energy usage while maintaining high throughput levels. This combination of reliability, precision, and efficiency makes circular screens a practical investment for businesses seeking to enhance their material processing operations with dependable equipment.

Key Features:
- Circular motion vibration mechanism for efficient material separation and movement
- Durable construction with industrial-grade materials for long service life
- Precise screening action ensuring accurate particle size classification
- Robust design capable of handling continuous high-volume operations
- Efficient operation with minimal energy consumption requirements

Benefits:
- Consistent particle separation improves product quality and process control
- Reduced maintenance needs lower operational costs and minimize downtime
- High throughput capacity supports efficient material processing operations
- Durable construction ensures reliable performance in demanding environments
- Energy-efficient design contributes to overall operational cost savings
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Circular vibrating screens deliver accurate particle separation essential for maintaining product quality and process efficiency. Their robust design handles continuous operation with consistent performance, making them ideal for high-volume industrial settings where material grading is critical. The precise screening action ensures uniform particle size distribution, which directly impacts downstream processing quality and final product specifications.
These versatile screening systems support diverse material handling requirements across multiple sectors. From ensuring food ingredient consistency to meeting pharmaceutical purity standards, circular screens provide the reliability needed for compliance-driven industries. Their efficient operation minimizes material waste while maximizing throughput, creating value through improved process control and reduced operational costs in demanding production environments.
- Food processing for grading grains, flour, spices, and powders to ensure consistent texture and quality
- Pharmaceutical manufacturing for precise separation of active ingredients and excipients in tablet production
- Chemical industry for classifying powders and removing impurities from industrial compounds
- Mining operations for sorting crushed ores and minerals by particle size and density
- Aggregate processing for separating sand, gravel, and crushed stone in construction materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Nishi Technosys, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Circular Vibrating Screens For Particle Separation
Industrial circular vibrating screens provide precise particle separation for food, pharmaceutical, chemical, and mining industries. Durable construction ensures reliable grading and sieving performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Nishi Technosys
 Maharashtra, India
Industrial Equipment & MachineryManufacturer