IN
₹

Description
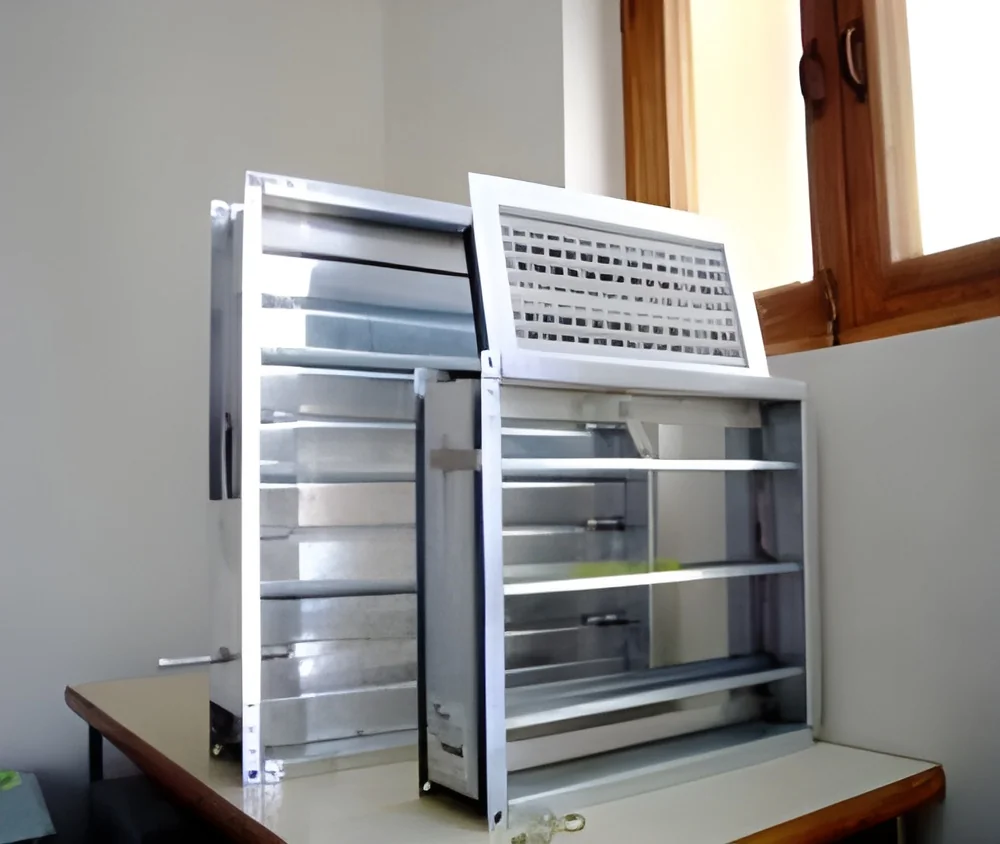
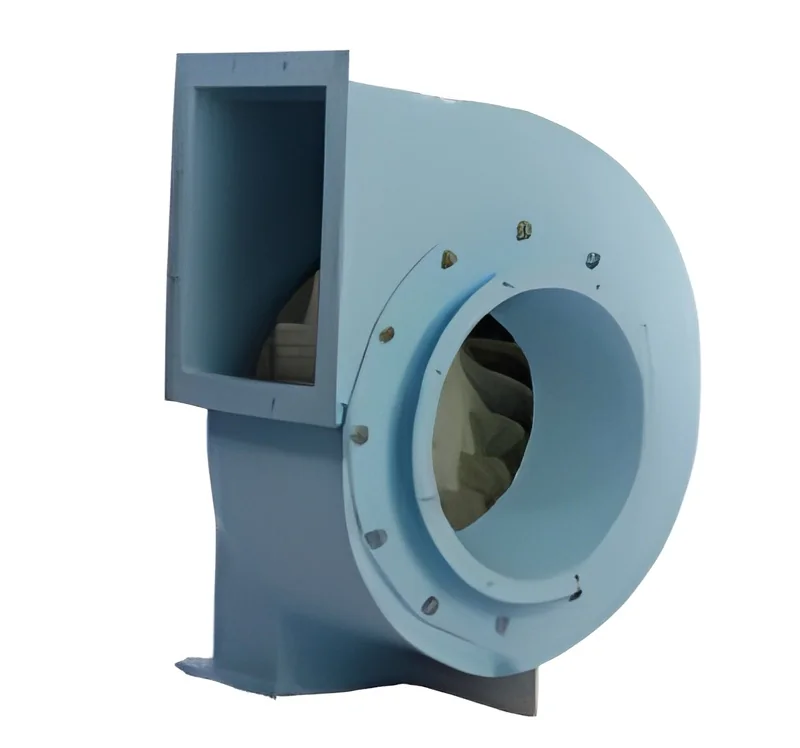
Our industrial wet dust collectors represent advanced air filtration technology specifically engineered for challenging moisture-laden environments. Unlike conventional dry collection systems that struggle with damp particulate matter, these units utilize water-based separation to effectively capture and contain moist, sticky, and hygroscopic dust particles. Manufactured from premium-grade corrosion-resistant materials and rigorously tested against industry standards, these systems deliver exceptional performance where traditional filters would clog or fail. The efficient water circulation system ensures optimal particle capture while preventing re-entrainment, providing thorough contamination control for the most demanding industrial applications.

These specialized filtration systems serve critical roles across multiple industrial sectors where moisture presents significant filtration challenges. In material handling and processing plants, they effectively manage dust from conveyor t...
Our industrial wet dust collectors represent advanced air filtration technology specifically engineered for challenging moisture-laden environments. Unlike conventional dry collection systems that struggle with damp particulate matter, these units utilize water-based separation to effectively capture and contain moist, sticky, and hygroscopic dust particles. Manufactured from premium-grade corrosion-resistant materials and rigorously tested against industry standards, these systems deliver exceptional performance where traditional filters would clog or fail. The efficient water circulation system ensures optimal particle capture while preventing re-entrainment, providing thorough contamination control for the most demanding industrial applications.

These specialized filtration systems serve critical roles across multiple industrial sectors where moisture presents significant filtration challenges. In material handling and processing plants, they effectively manage dust from conveyor transfer points, loading stations, and processing equipment where environmental humidity complicates dust control. Metalworking and foundry operations rely on them for capturing grinding dust and cooling mist generated during machining and finishing processes. Chemical manufacturing facilities utilize these systems to control powder emissions during mixing, blending, and packaging operations where moisture-sensitive materials are processed. The food industry benefits from their ability to handle hygroscopic materials like sugar, flour, and starch without the clogging issues that plague dry collection systems.

The business value of our wet dust collectors extends beyond regulatory compliance to deliver tangible operational advantages and cost savings. Their robust construction and corrosion-resistant materials ensure minimal downtime and reduced maintenance costs, while the efficient dust control improves workplace safety and protects expensive machinery from abrasive particle damage. The reliable performance under continuous operation conditions translates to consistent production quality and reduced operational interruptions. These systems not only meet but exceed industry air quality standards, helping businesses maintain regulatory compliance while enhancing their environmental stewardship and workplace safety credentials. The long service life and dependable operation provide excellent return on investment through reduced replacement costs and maintenance requirements.

Key Features:
- Corrosion-resistant construction for durability in harsh environments
- Water-based filtration system for effective moist dust capture
- Scalable design accommodating various industrial requirements
- Efficient particle separation preventing system clogging
- Robust components ensuring reliable continuous operation

Benefits:
- Prevents clogging issues common with dry collection systems
- Reduces maintenance requirements and operational downtime
- Improves workplace air quality and safety standards
- Protects machinery from abrasive particle damage
- Ensures consistent performance in high-moisture environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial wet dust collectors excel in environments where conventional dry systems fail due to moisture content. These specialized filtration units use water-based separation to capture moist, sticky, and hygroscopic dust particles that would otherwise clog standard filters. Their unique design prevents particle re-entrainment while handling high-humidity airstreams, making them essential for processes involving slurry, mist, or damp particulate matter that challenges ordinary collection methods.
These robust systems serve diverse industrial sectors requiring reliable air quality control under demanding conditions. Material handling facilities utilize them for conveyor transfer points and loading stations where dust generation meets environmental moisture. Manufacturing plants benefit from their corrosion-resistant construction when processing abrasive or chemically active particles. Their scalable design accommodates various airflow requirements while maintaining consistent filtration efficiency across different operational scales and space constraints.
- Metal grinding and polishing operations capturing cool mist and metallic dust
- Fertilizer production facilities controlling hygroscopic powder emissions
- Food processing plants handling sticky materials like sugar and flour
- Cement manufacturing managing abrasive particles with moisture content
- Chemical processing containing powder emissions during mixing operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Access Envirotech Engineers Private Limited, New Delhi
 New Delhi, India
Manufacturer•Trading Company
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Wet Dust Collectors For Moist Air Filtration
Industrial wet dust collectors provide reliable moisture-laden dust filtration for material handling, mixing, and muller applications. Engineered with high-grade components for long service life and efficient separation in challenging industrial environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Access Envirotech Engineers Private Limited
 New Delhi, India
Manufacturer