IN
₹
Apparel & Fashion
Description
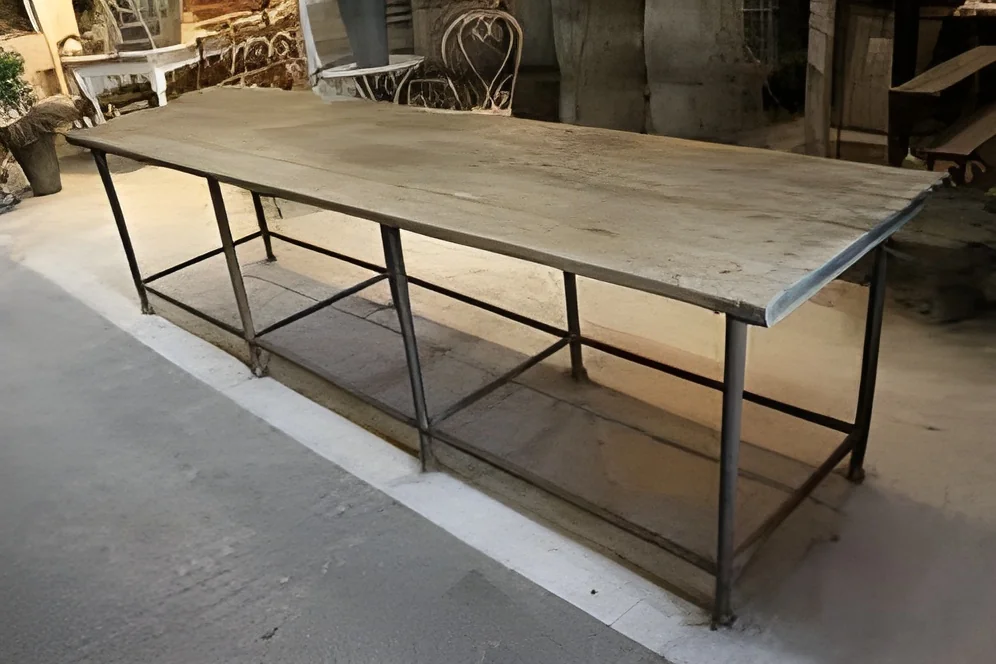
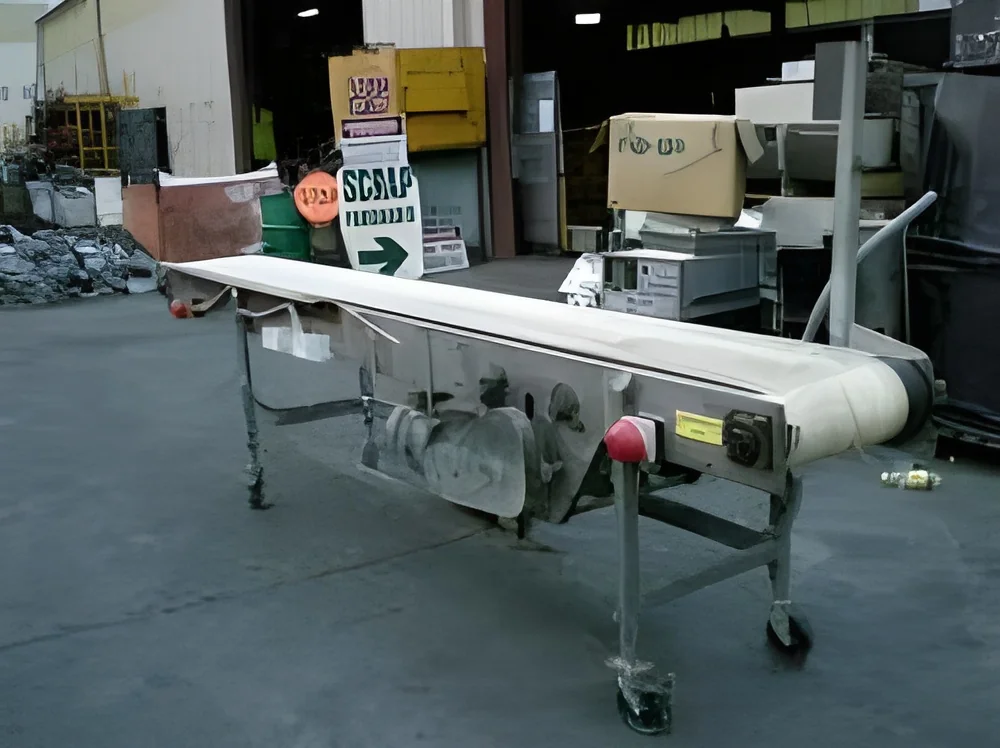
Our industrial stainless steel conveyor systems are precision-engineered for demanding applications in food, pharmaceutical, and manufacturing environments. Constructed from premium-grade stainless steel, these conveyors deliver exceptional resistance to corrosion, abrasion, and extreme temperature variations. Designed to handle substantial loads while maintaining consistent operational performance, they feature customizable specifications including adjustable speeds, varying widths, and specialized belt configurations to match specific application requirements. The easy-to-clean design and low-maintenance requirements make these systems ideal for industries where hygiene standards are paramount. With robust construction and reliable components, our conveyors ensure long-term operational durability and minimal production downtime.

These conveyor systems serve critical roles across multiple industrial sectors including food and beverage processing, pharmaceutical manufacturing, chemica...
Our industrial stainless steel conveyor systems are precision-engineered for demanding applications in food, pharmaceutical, and manufacturing environments. Constructed from premium-grade stainless steel, these conveyors deliver exceptional resistance to corrosion, abrasion, and extreme temperature variations. Designed to handle substantial loads while maintaining consistent operational performance, they feature customizable specifications including adjustable speeds, varying widths, and specialized belt configurations to match specific application requirements. The easy-to-clean design and low-maintenance requirements make these systems ideal for industries where hygiene standards are paramount. With robust construction and reliable components, our conveyors ensure long-term operational durability and minimal production downtime.

These conveyor systems serve critical roles across multiple industrial sectors including food and beverage processing, pharmaceutical manufacturing, chemical production, and packaging operations. In food processing environments, they safely transport products through washing, cooking, and packaging stages while maintaining strict sanitary compliance. Pharmaceutical manufacturers utilize these conveyors for moving sensitive products within controlled sterile environments. Chemical processing facilities rely on their superior resistance to harsh substances and corrosive materials. Logistics and distribution centers implement these systems for efficient sorting and shipping operations, while automotive and electronics manufacturers integrate them into automated assembly lines for precise component handling.

Investing in our stainless steel conveyor systems delivers substantial business value through enhanced operational efficiency, reduced labor requirements, and improved product safety. The reliable performance minimizes operational disruptions and lowers maintenance costs over the system's lifespan. Customizable features ensure seamless integration into existing production workflows, significantly boosting overall productivity. The hygienic design substantially reduces contamination risks while ensuring compliance with industry regulations and quality standards. These conveyors are engineered for long-term durability, providing excellent return on investment by supporting continuous, high-volume operations without compromising performance quality or operational reliability.

Key Features:
- Premium stainless steel construction for superior corrosion resistance
- Customizable dimensions and operational speeds for specific requirements
- Hygienic design with easy cleaning and maintenance capabilities
- Heavy-duty construction ensuring long-term durability and reliability
- Seamless integration with existing automation and control systems

Benefits:
- Enhanced operational efficiency through reliable material handling
- Reduced contamination risks with hygienic stainless steel surfaces
- Lower maintenance requirements and operational downtime
- Improved compliance with industry regulations and standards
- Long service life providing excellent return on investment
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Stainless steel conveyors provide essential hygienic material transport for industries requiring strict cleanliness standards and corrosion resistance. These systems excel in food processing, pharmaceutical production, and manufacturing environments where contamination prevention and durability are critical operational priorities. They ensure smooth, efficient movement of materials while maintaining compliance with rigorous sanitary regulations and industry standards.
These conveyor systems support automated operations across packaging lines, assembly processes, and sorting applications. They significantly reduce manual handling requirements while minimizing contamination risks and enhancing overall workflow efficiency. Industries including logistics, automotive manufacturing, and electronics production depend on these conveyors for seamless material flow and scalable operational capabilities.
- Food processing facilities for transporting baked goods, meats, and packaged food items
- Pharmaceutical manufacturing plants for moving tablets, capsules, and sterile medical supplies
- Chemical processing operations for handling powders, granules, and corrosive materials
- Packaging and distribution centers for automated boxing, labeling, and sealing operations
- Manufacturing facilities for assembly line part transportation and product handling
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Arjun Plastic Engineers, Rajasthan
 Rajasthan, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Stainless Steel Conveyor Systems For Food And Pharmaceutical
Industrial stainless steel conveyor systems for food and pharmaceutical sectors deliver reliable, hygienic material handling with heavy-duty performance and customizable configurations for specific operational requirements.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arjun Plastic Engineers
 Rajasthan, India
Electronics & ElectricalManufacturer