IN
₹
Apparel & Fashion
Description
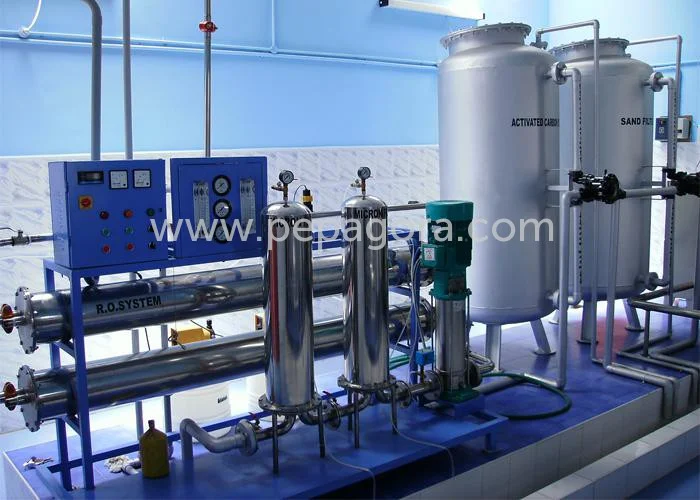
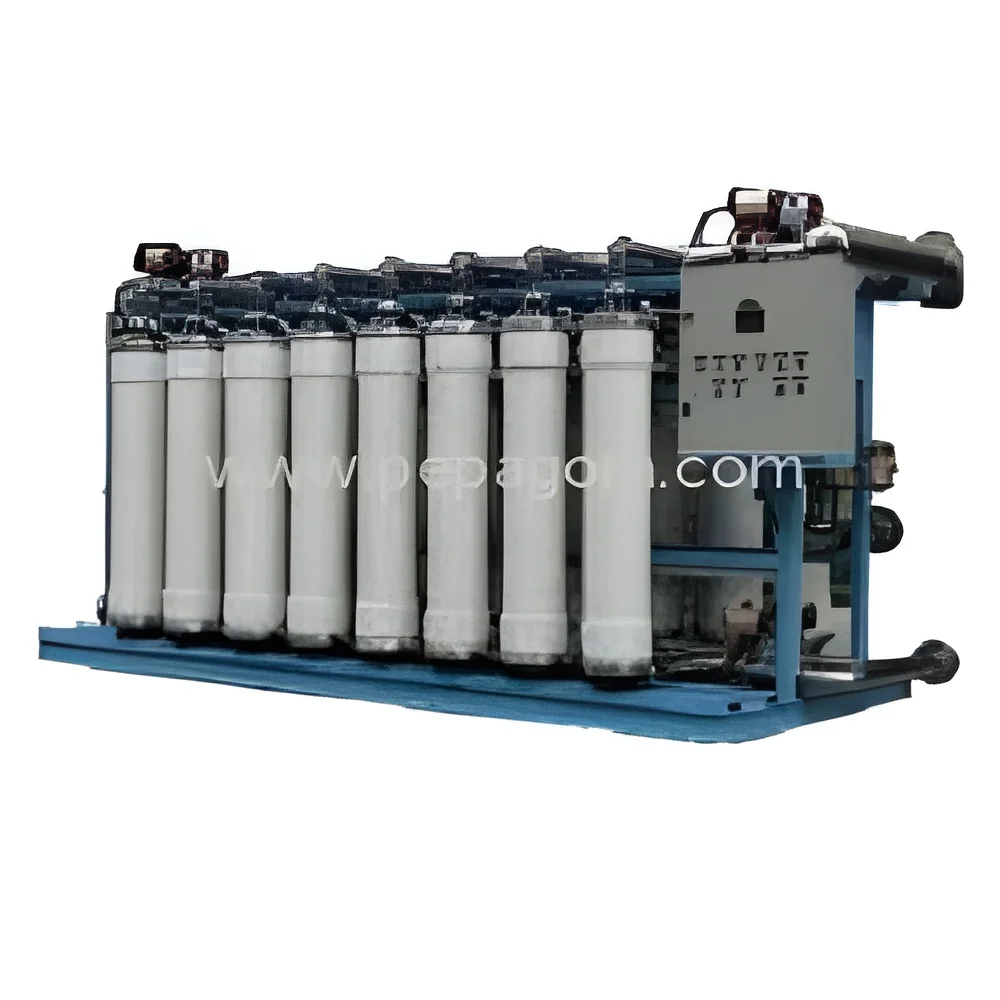
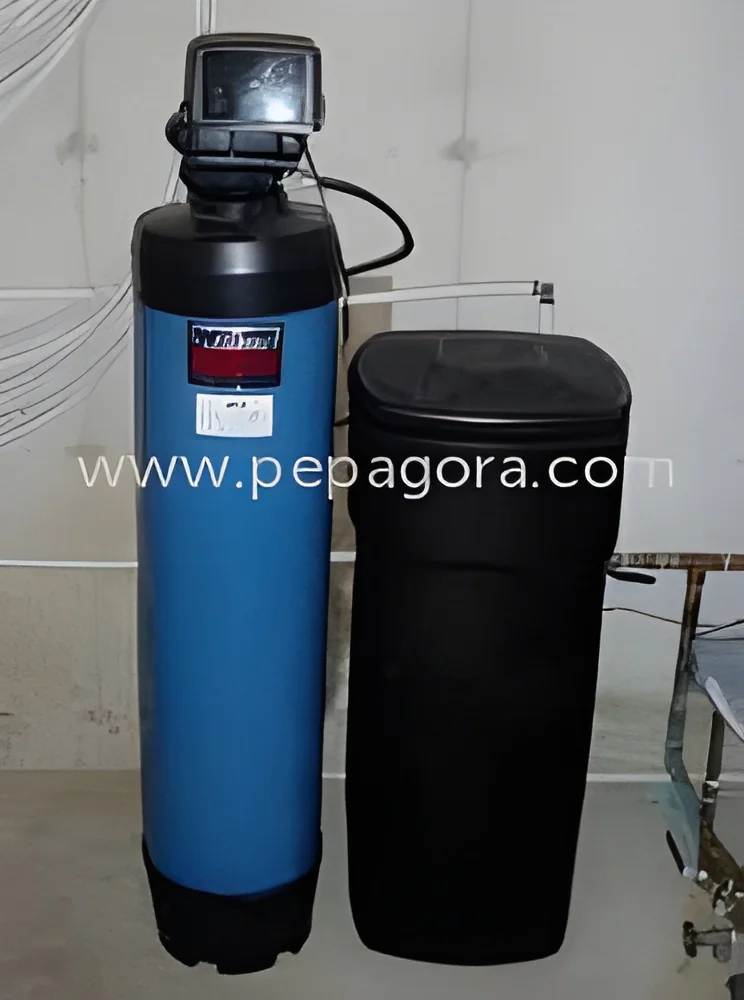
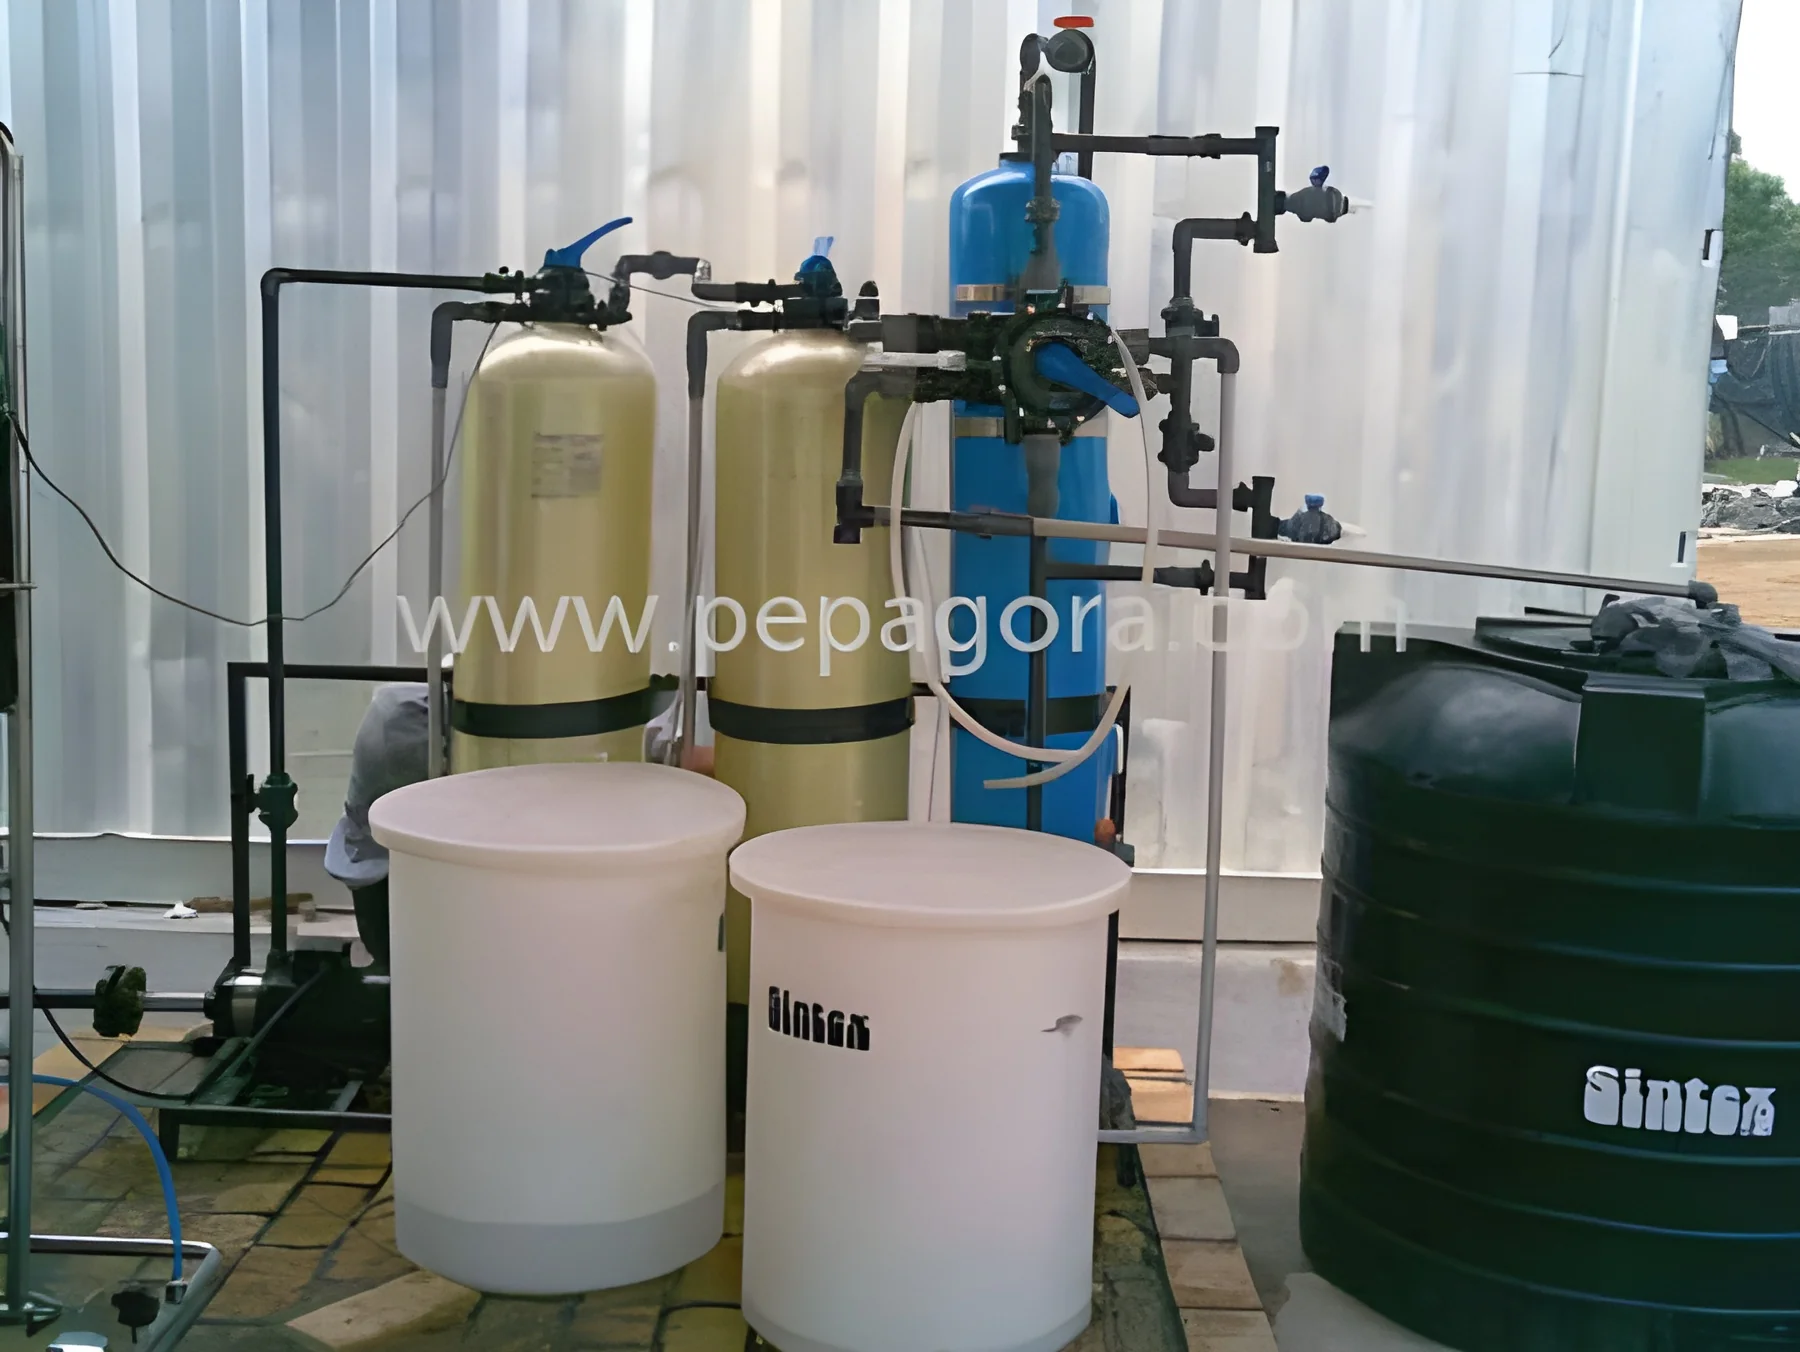
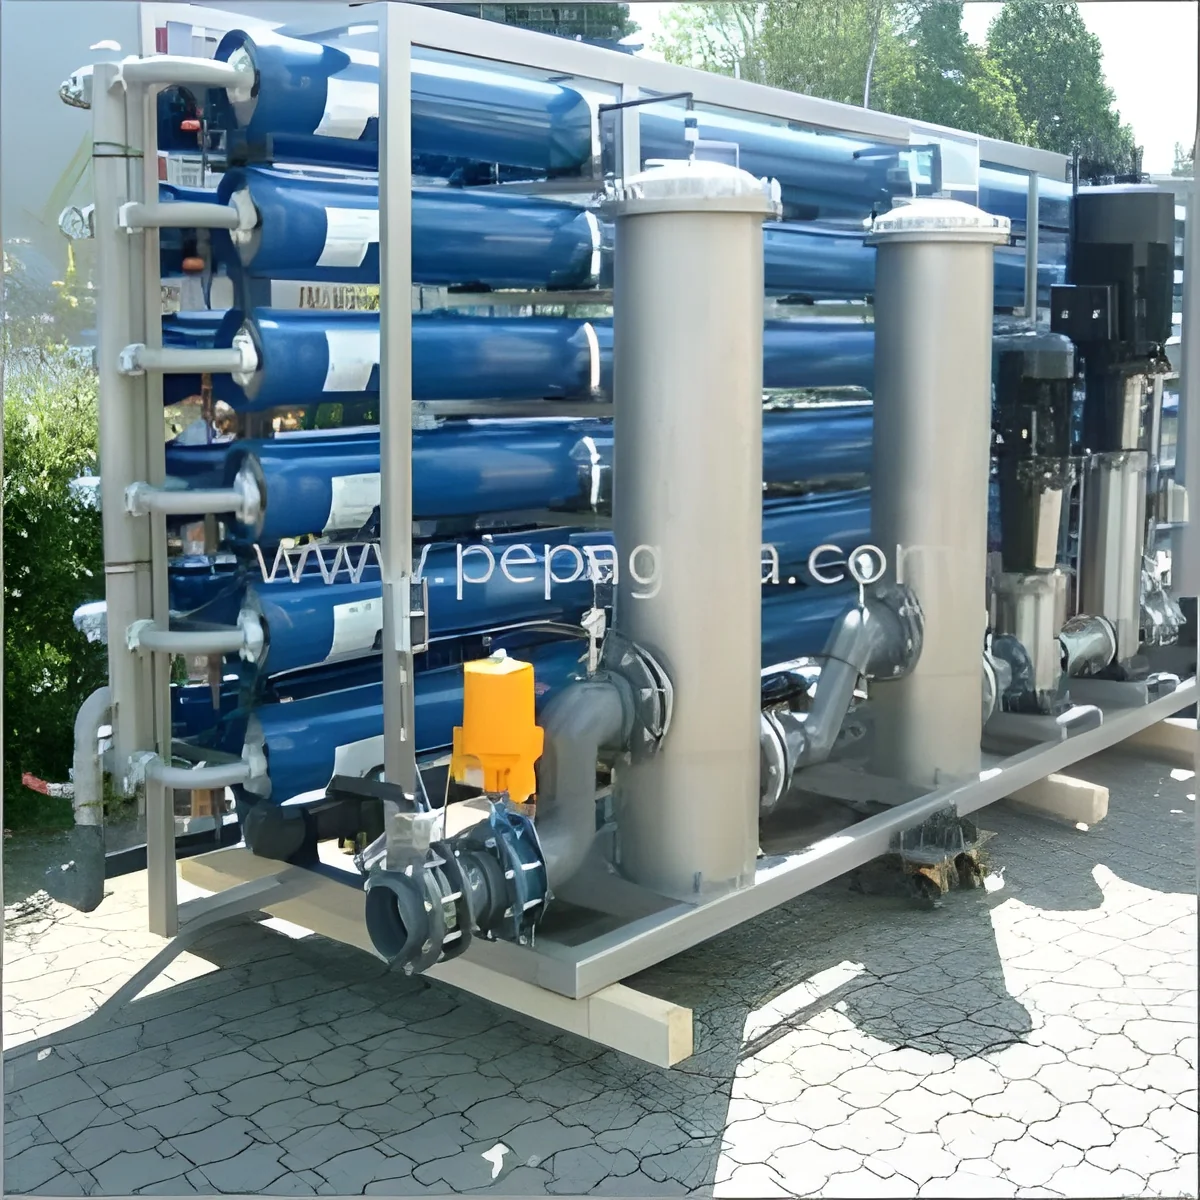
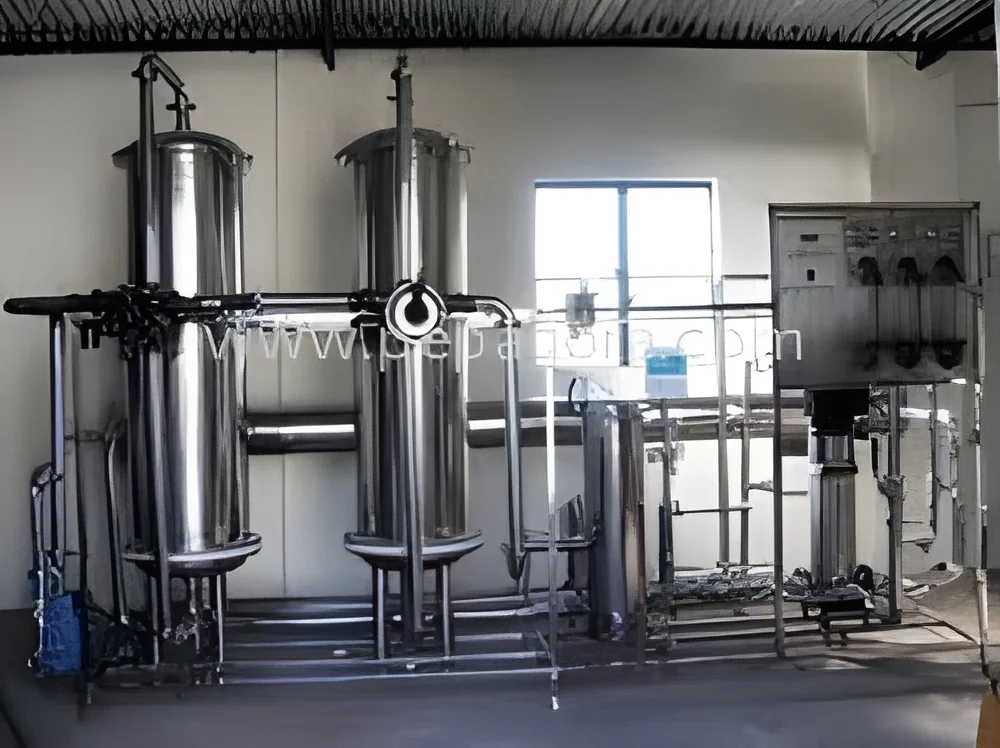
Our industrial water treatment plant represents advanced water processing technology designed for operations demanding uncompromising quality and reliability. This standard OEM system consistently delivers 100% water purity through sophisticated treatment processes, ensuring your operations maintain the highest water quality standards. The plant features robust construction with high tensile strength materials and superior corrosion resistance, capable of handling demanding industrial environments. With low noise operation and minimal maintenance requirements, this solution provides continuous performance without disrupting workplace environments. The straightforward installation process allows for quick implementation, enabling facilities to benefit from purified water almost immediately after delivery.

This water treatment system serves numerous industries that depend on high-quality water for critical operations. Manufacturing facilities utilize it for process water purification, e...
Our industrial water treatment plant represents advanced water processing technology designed for operations demanding uncompromising quality and reliability. This standard OEM system consistently delivers 100% water purity through sophisticated treatment processes, ensuring your operations maintain the highest water quality standards. The plant features robust construction with high tensile strength materials and superior corrosion resistance, capable of handling demanding industrial environments. With low noise operation and minimal maintenance requirements, this solution provides continuous performance without disrupting workplace environments. The straightforward installation process allows for quick implementation, enabling facilities to benefit from purified water almost immediately after delivery.

This water treatment system serves numerous industries that depend on high-quality water for critical operations. Manufacturing facilities utilize it for process water purification, ensuring consistent product quality and manufacturing standards. The pharmaceutical sector relies on its 100% purity output for sensitive applications where water quality is non-negotiable. Power plants and refineries implement this system for cooling tower water treatment, preventing scale buildup and corrosion damage. Textile and chemical industries benefit from its water recycling capabilities, supporting sustainability initiatives while maintaining production efficiency. Food processing operations use it to ensure water meets stringent safety and quality standards throughout manufacturing processes.

The operational value of this industrial water treatment plant extends beyond basic water purification to deliver measurable business advantages. It provides significant cost savings through reduced maintenance requirements, lower energy consumption, and decreased operational downtime. The system's reliability ensures consistent water quality, protecting equipment from scale and corrosion while maintaining product quality standards. With guaranteed on-time delivery and OEM supply capabilities, operations can trust that their water treatment needs will be met without production interruptions. The negotiable pricing structure makes this advanced technology accessible to operations of various scales, delivering exceptional return on investment through improved efficiency and reduced operational expenses.

Key Features:
- Corrosion-resistant construction ensuring long-term durability
- High tensile strength materials providing structural integrity
- Low noise operation suitable for diverse workplace environments
- Standard OEM design for straightforward integration
- 100% water purity output meeting rigorous quality standards

Benefits:
- Reduced maintenance costs and operational downtime
- Enhanced equipment protection through consistent water quality
- Lower energy consumption during operation
- Quick implementation with easy installation processes
- Sustainable water management supporting environmental compliance
Specifications
| Key Attributes | |
|---|---|
| Type | Plant |
| Supply Type | OEM |
| Standard or Nonstandard | Standard |
| Price | Negotiable |
| Advantage | Ease to Install |
| Application | Industrial Applications |
| resistance | Corrosion Resistance |
| Noise | Low |
| Delivery | On Time Delivery |
| Performance | Good |
| Maintenance | Low |
| Use | Water Treatments |
| Purity | 100% |
| Feature | High Tensile Strength |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial water treatment plant is engineered for demanding manufacturing and processing environments where water quality directly impacts operational efficiency and product standards. The system consistently delivers 100% purity output while maintaining low noise levels and minimal maintenance requirements, making it ideal for continuous operation across diverse industrial settings requiring reliable water treatment solutions.
Built with exceptional corrosion resistance and high tensile strength construction, this standard OEM plant ensures long-term reliability even in challenging operating conditions. With straightforward installation processes and guaranteed on-time delivery, facilities can quickly integrate this solution into existing infrastructure without significant downtime or complex modifications, providing immediate water treatment capabilities.
- Purifying process water for manufacturing and production operations
- Treating industrial wastewater to meet environmental compliance standards
- Providing high-purity water for pharmaceutical manufacturing processes
- Supporting cooling tower systems in power generation facilities
- Enabling water recycling in textile processing and chemical production
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Hydro India, Tamil Nadu
 Tamil Nadu, India
Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Water Treatment Plant With Corrosion Resistance And Low Maintenance
Industrial water treatment plant delivers 100% pure water with corrosion-resistant construction, low maintenance, and easy installation for reliable industrial water processing applications requiring dependable performance.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Hydro India
 Tamil Nadu, India
Manufacturer