IN
₹
Apparel & Fashion
Description
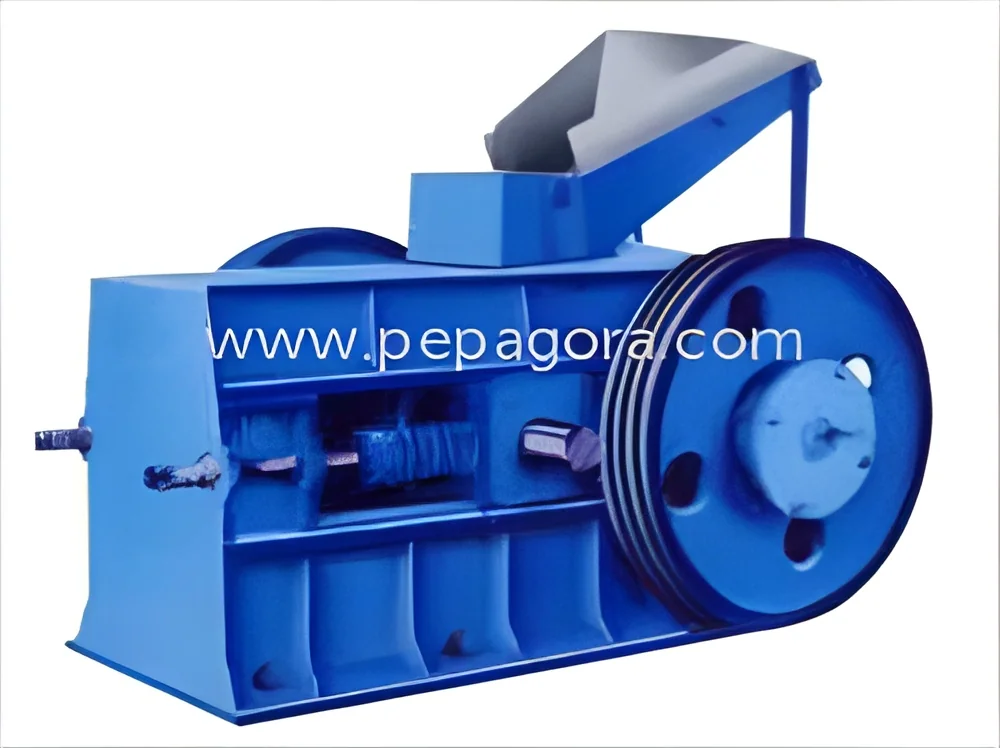
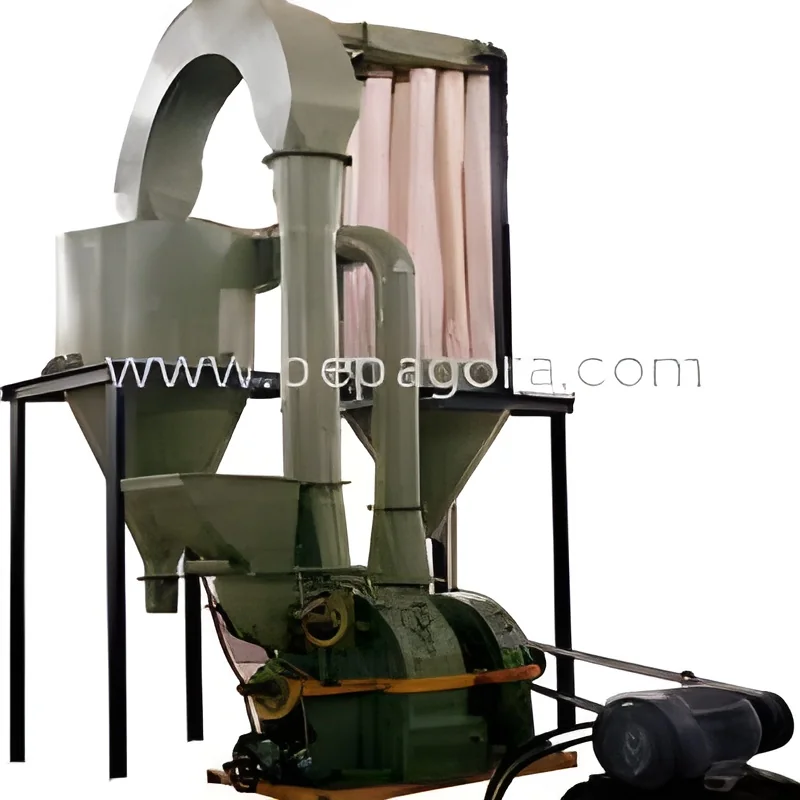
The Industrial Superior Impact Pulverizer represents advanced engineering in industrial grinding technology, specifically designed for fine particle size reduction across various materials. This robust machine utilizes powerful impact forces to pulverize minerals, chemicals, and spices into fine powders with consistent particle size distribution. Built with durable components and superior manufacturing techniques, it ensures reliable performance even under continuous heavy-duty operation. The pulverizer features an efficient yet straightforward design that enables easy maintenance and operation, making it suitable for diverse industrial environments. Its exceptional versatility allows processing of multiple material types requiring fine grinding, delivering consistent results that meet strict quality standards. With a focus on operational excellence and efficiency, this machine provides outstanding value for businesses seeking dependable pulverizing solutions that stand the test of tim...
The Industrial Superior Impact Pulverizer represents advanced engineering in industrial grinding technology, specifically designed for fine particle size reduction across various materials. This robust machine utilizes powerful impact forces to pulverize minerals, chemicals, and spices into fine powders with consistent particle size distribution. Built with durable components and superior manufacturing techniques, it ensures reliable performance even under continuous heavy-duty operation. The pulverizer features an efficient yet straightforward design that enables easy maintenance and operation, making it suitable for diverse industrial environments. Its exceptional versatility allows processing of multiple material types requiring fine grinding, delivering consistent results that meet strict quality standards. With a focus on operational excellence and efficiency, this machine provides outstanding value for businesses seeking dependable pulverizing solutions that stand the test of time.

Multiple industries rely on Impact Pulverizers for their specific grinding requirements and production needs. Mineral processing plants extensively use these machines for pulverizing limestone, calcite, and various minerals into fine powders essential for manufacturing processes and industrial applications. The chemical industry depends on them for uniform particle size reduction of pigments, dyes, and raw materials where consistency is critical. Food processing operations utilize these pulverizers for grinding spices, grains, and other food products into fine powders while maintaining product integrity. Pharmaceutical manufacturers employ them for precise size reduction of active ingredients and excipients to meet stringent quality standards. Agricultural sectors also benefit from these machines for processing agricultural products and animal feed ingredients, demonstrating the equipment's broad cross-industry applicability and versatility in handling diverse materials.

Businesses investing in this Industrial Superior Impact Pulverizer gain substantial operational advantages through enhanced productivity and minimized maintenance requirements. The machine's reliable performance ensures consistent output quality, directly influencing final product quality and customer satisfaction levels. Its durable construction significantly reduces downtime and extends service life, providing long-term value and excellent return on investment. The reasonable pricing combined with superior quality makes it an economically viable solution for both established operations and growing enterprises. The combination of reliability, efficiency, and value makes this pulverizer a strategic investment for serious buyers seeking competitive advantages in their respective markets through improved processing capabilities and consistent product quality.

Key Features:
- Superior quality construction using durable materials for extended service life
- Efficient impact-based grinding mechanism for consistent particle size reduction
- Robust design capable of handling various materials including minerals and chemicals
- Simple operational design facilitating easy maintenance and reduced downtime
- Various design options available to meet specific industrial requirements

Benefits:
- Long service life through durable construction and quality materials
- Consistent particle size reduction for uniform product quality
- Versatile performance across multiple materials and industries
- Reduced operational downtime through easy maintenance design
- Reliable performance in demanding industrial environments
Specifications
| Key Attributes | |
|---|---|
| Quality | Superior |
| Feature | Durable, Reliable |
| Type | Pulverizer |
| Condition | New |
| Strength | Great |
| Service Life | Long |
| Design | Various |
| Price | Reasonable |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The Industrial Superior Impact Pulverizer excels in high-performance grinding across multiple processing sectors. Its robust construction and efficient pulverizing mechanism make it ideal for processing minerals, chemicals, food products, and pharmaceuticals into fine powders with consistent particle size distribution. This machine ensures uniformity and quality output for diverse manufacturing requirements while handling abrasive and hard materials effectively.
Industries depend on this pulverizer for its versatility and durability in demanding operational environments. From large-scale mineral processing facilities to specialized spice grinding operations, it maintains consistent performance while reducing downtime and maintenance costs. The design prioritizes operational efficiency, maximizing productivity for businesses seeking reliable size reduction solutions that deliver consistent results day after day.
- Grinding minerals like limestone, calcite, and dolomite into fine powders for industrial manufacturing
- Pulverizing chemicals and pigments to achieve uniform particle size in production processes
- Processing spices and food products into fine powders for packaging and distribution
- Crushing agricultural products including grains and pulses for food processing operations
- Size reduction of pharmaceutical ingredients to meet specific formulation requirements
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Coimbatore |
Company Profile
Sandhiya Engineering, Tamil Nadu
 Tamil Nadu, India
Tools & Hardware
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Superior Impact Pulverizer For Fine Grinding Minerals Chemicals Spices
Industrial Superior Impact Pulverizer delivers efficient fine grinding of minerals, chemicals, and spices. Durable construction ensures reliable performance and long service life for various industrial processing applications.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Sandhiya Engineering
 Tamil Nadu, India
Tools & Hardware