IN
₹
Apparel & Fashion
Description
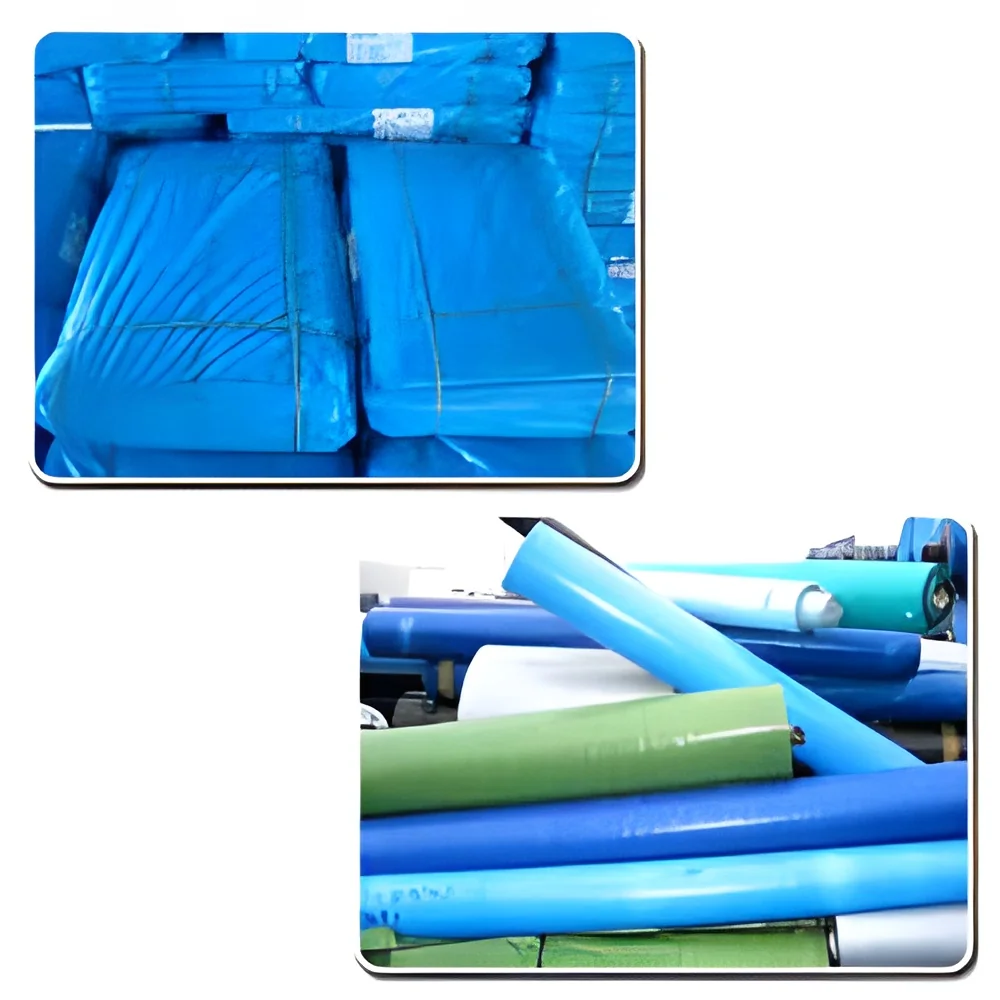
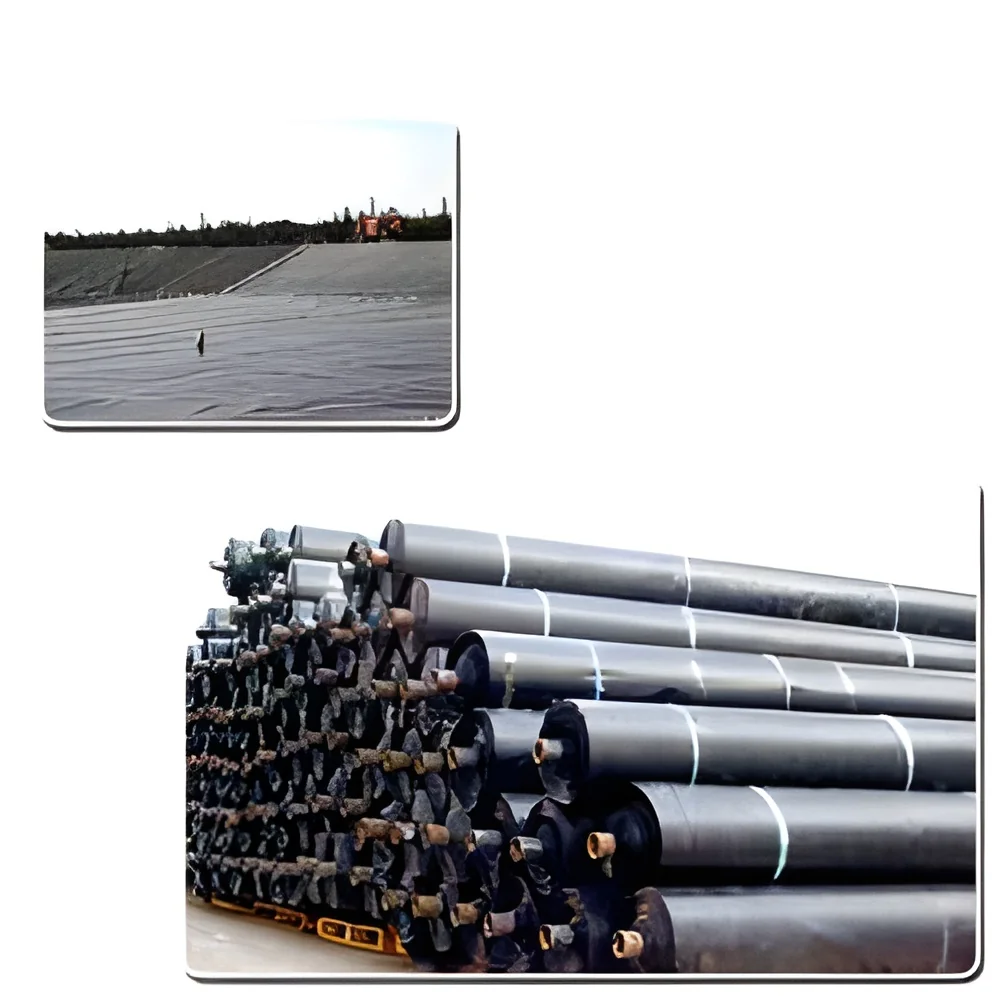
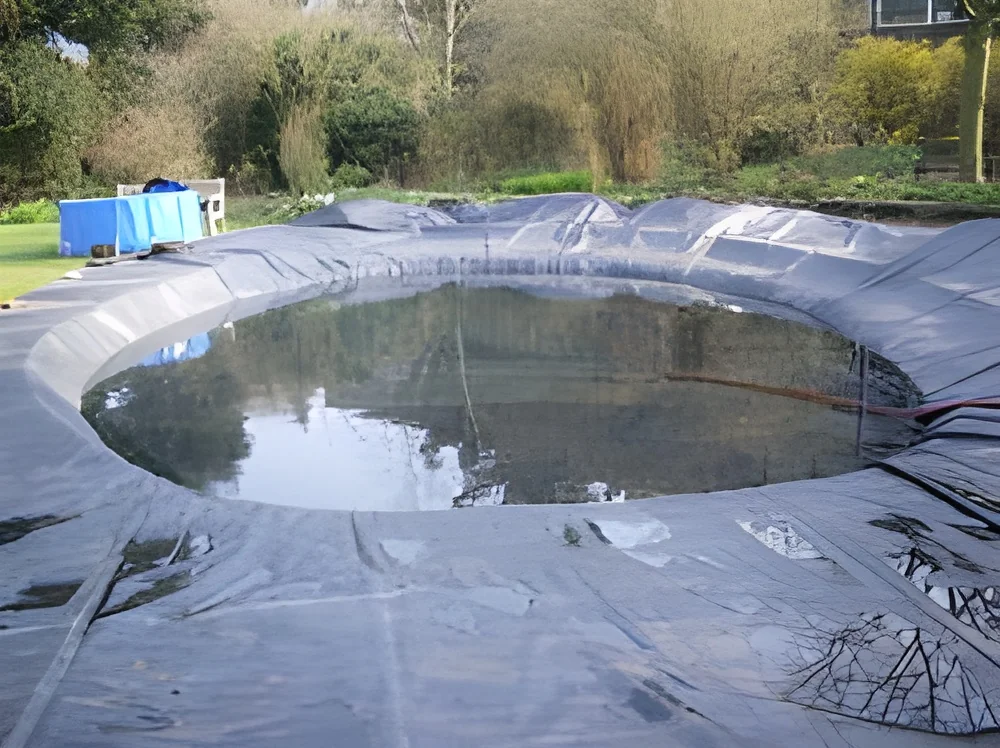
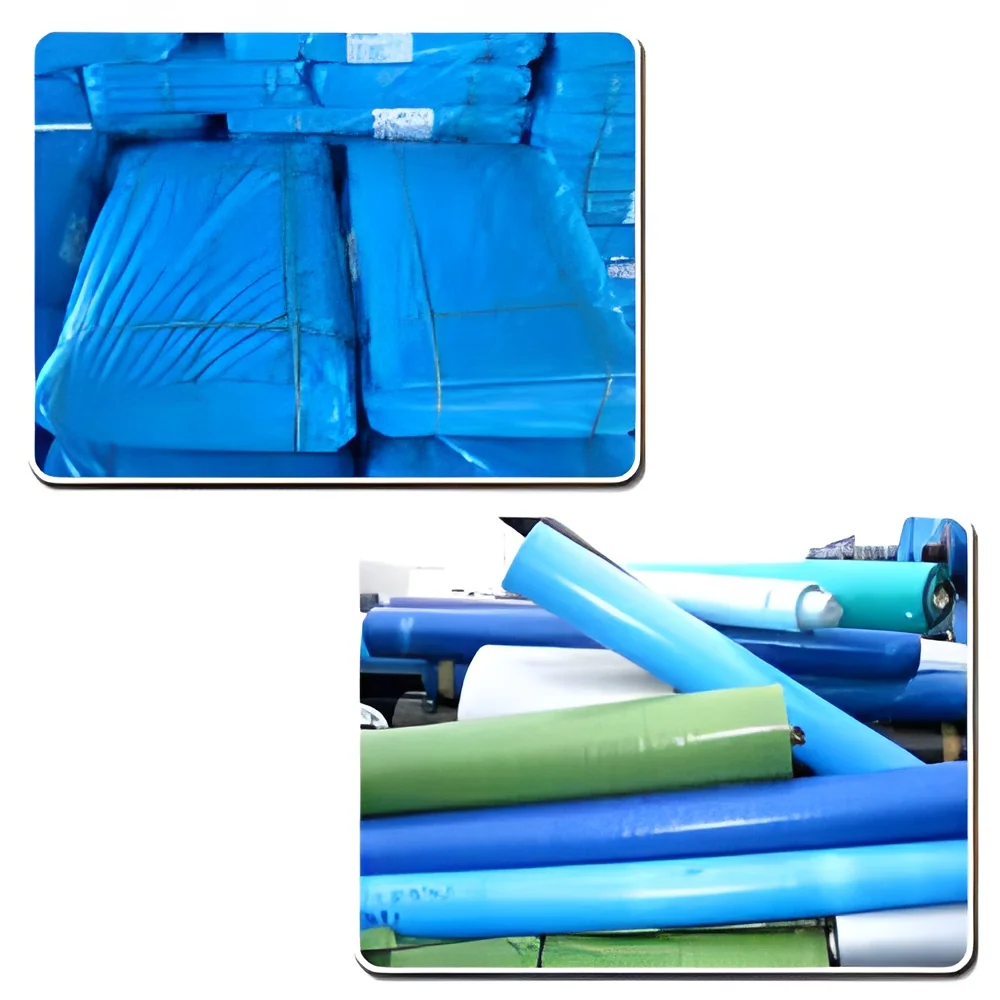
Industrial HDPE laminated fabric is a high-performance packaging material designed for superior protection. It combines high-density polyethylene with a specialized lamination process to create a fabric that is exceptionally durable and completely waterproof. Available in both single and double-sided lamination, this material offers a reliable solution for safeguarding goods against moisture, tears, and environmental factors during storage and transportation. Its strength and resilience make it an ideal choice for businesses that require packaging capable of enduring demanding handling and extended shelf life without compromising on protection.

This packaging fabric serves a wide range of industries that depend on secure and moisture-proof containment. In agriculture, it is used for packaging fertilizers, pesticides, and harvested produce. The construction sector relies on it for bagging cement, sand, and other aggregates. Chemical manufacturers utilize it for safely transporting powd...
Industrial HDPE laminated fabric is a high-performance packaging material designed for superior protection. It combines high-density polyethylene with a specialized lamination process to create a fabric that is exceptionally durable and completely waterproof. Available in both single and double-sided lamination, this material offers a reliable solution for safeguarding goods against moisture, tears, and environmental factors during storage and transportation. Its strength and resilience make it an ideal choice for businesses that require packaging capable of enduring demanding handling and extended shelf life without compromising on protection.

This packaging fabric serves a wide range of industries that depend on secure and moisture-proof containment. In agriculture, it is used for packaging fertilizers, pesticides, and harvested produce. The construction sector relies on it for bagging cement, sand, and other aggregates. Chemical manufacturers utilize it for safely transporting powders and granular materials, while distributors in food and retail use it for bulk commodities. Its universal applicability stems from its ability to provide a consistent, high-barrier protection that is critical for maintaining product quality and safety across different market segments and logistical challenges.

Investing in this HDPE laminated fabric translates to tangible business value through enhanced reliability and reduced losses. Its durability minimizes the risk of packaging failure, which protects against product damage, spoilage, and associated financial costs. The material's resistance to rot and mildew ensures long-term storage viability, eliminating waste. By providing a dependable first line of defense for goods, it streamlines supply chain operations, builds trust with end customers, and supports a professional market presence through consistent delivery of intact products.

Key Features:
- Constructed from high-density polyethylene (HDPE) for maximum strength
- Available with single or double-sided waterproof lamination
- Engineered to be tear-resistant and durable under heavy loads
- Provides complete moisture and water ingress protection
- Offers resistance to rot, mildew, and environmental degradation

Benefits:
- Ensures product safety and integrity during transit and storage
- Reduces risk of loss from damaged or compromised packaging
- Provides long-lasting protection suitable for extended shelf life
- Offers a reliable and consistent performance for supply chain efficiency
- Delivers cost-effectiveness by minimizing replacement and waste
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This HDPE laminated fabric delivers essential protection where moisture resistance and durability are non-negotiable. It is engineered to withstand rigorous handling throughout the supply chain, safeguarding contents from environmental damage and physical stress during transit. Its robust construction ensures product integrity from the point of packing to final destination, making it a trusted choice for demanding logistics.
The material's versatility meets the needs of agriculture, construction, chemical, and bulk goods sectors. It provides a dependable barrier against humidity, water ingress, and rough handling, which is crucial for domestic shipping and international exports. Businesses select this fabric for its proven performance in preserving the quality and safety of sensitive or heavy-duty products across diverse operational environments.
- Packaging for agricultural inputs like fertilizers, seeds, and crop protection products
- Secure containment and transport of construction materials including cement, sand, and aggregates
- Storage and shipping of industrial chemicals, powders, and granular compounds
- Bulk packaging for food commodities such as grains, sugar, and flour
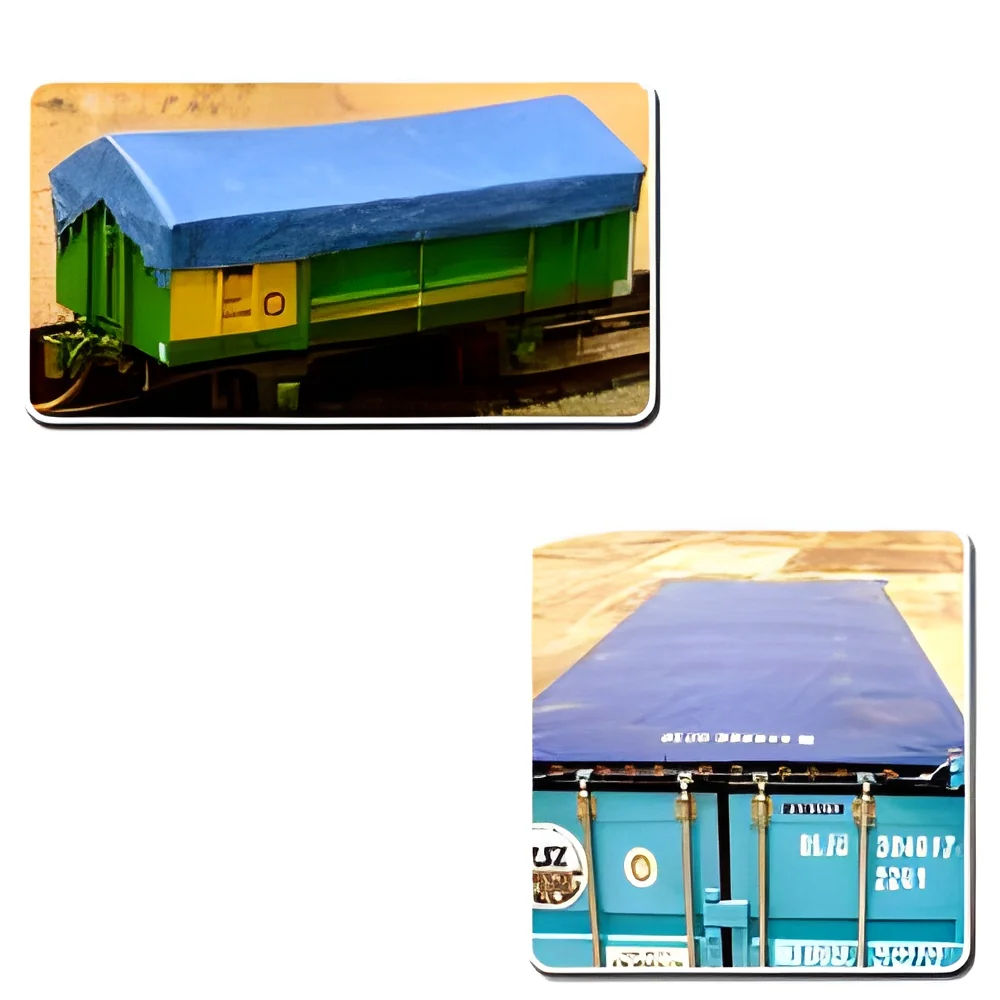
- Protective covering and packaging for retail wholesale goods and manufactured products
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arihant Tarpaulin Pvt. Ltd, Gujarat
 Gujarat, India
Apparel & Fashion•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial HDPE Laminated Fabric For Durable Waterproof Packaging
Industrial HDPE laminated fabric provides durable, waterproof packaging material for reliable protection of goods during storage and transport. Available in single or double-sided lamination options.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arihant Tarpaulin Pvt. Ltd
 Gujarat, India
Apparel & FashionManufacturer