IN
₹
Apparel & Fashion
Description
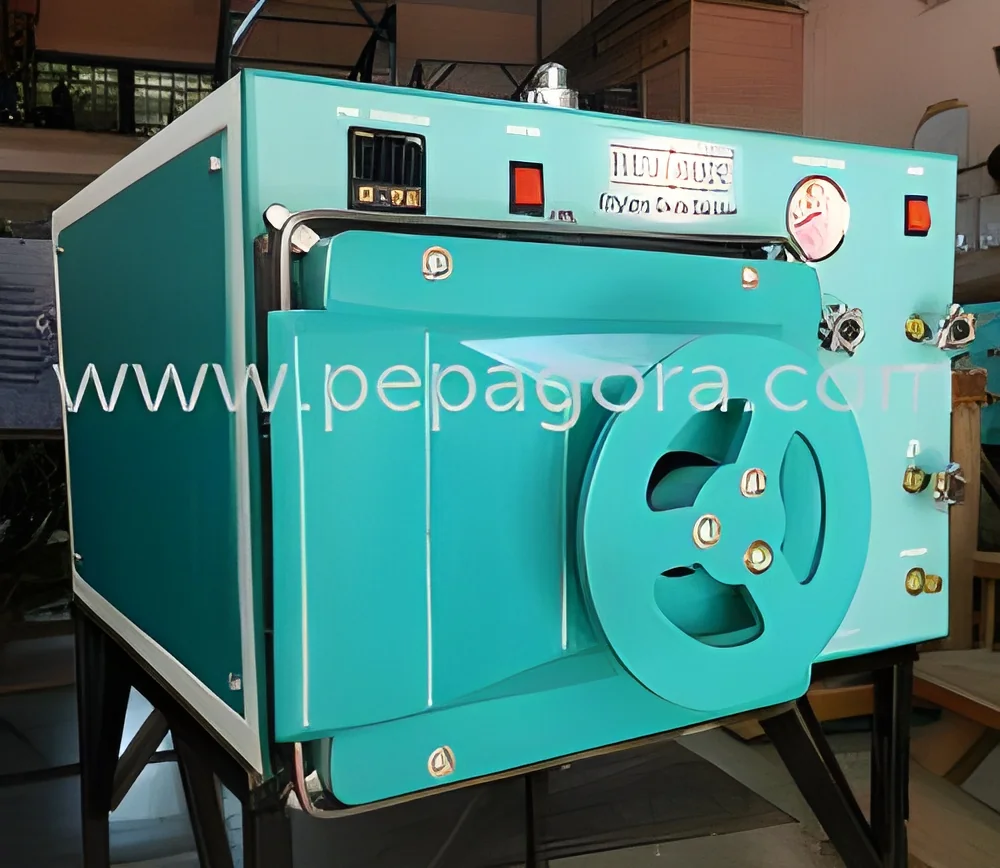
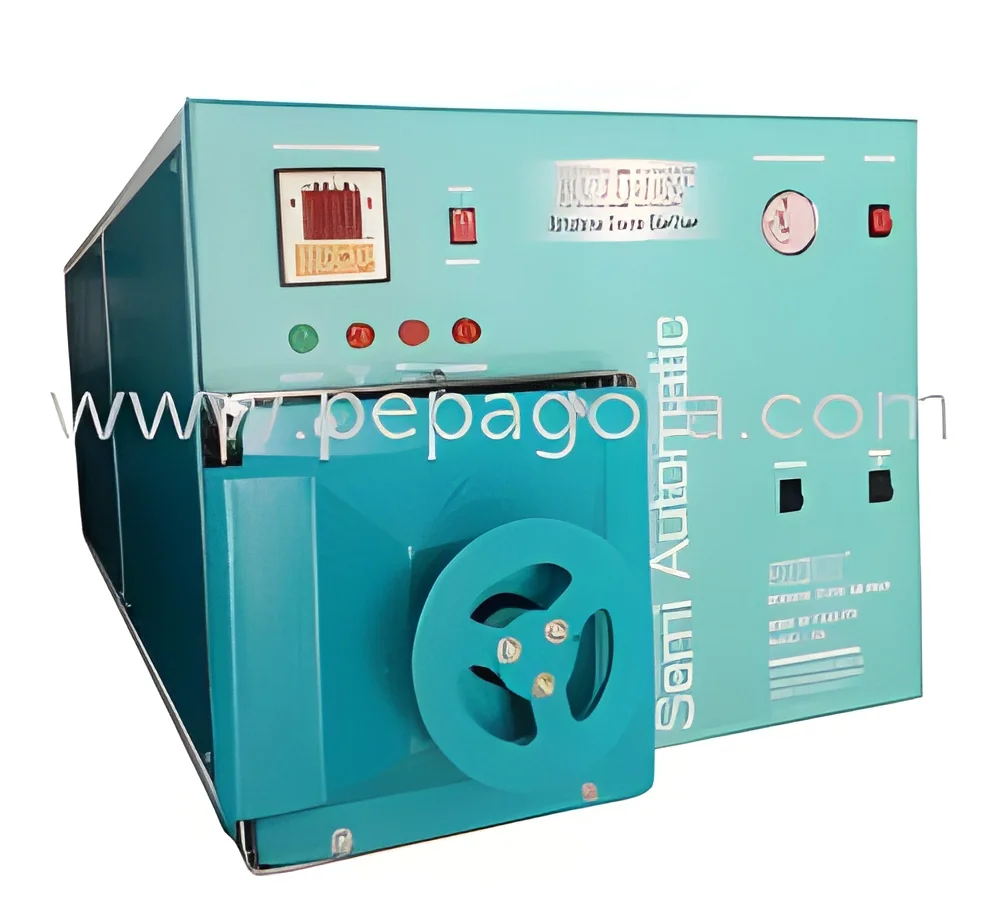
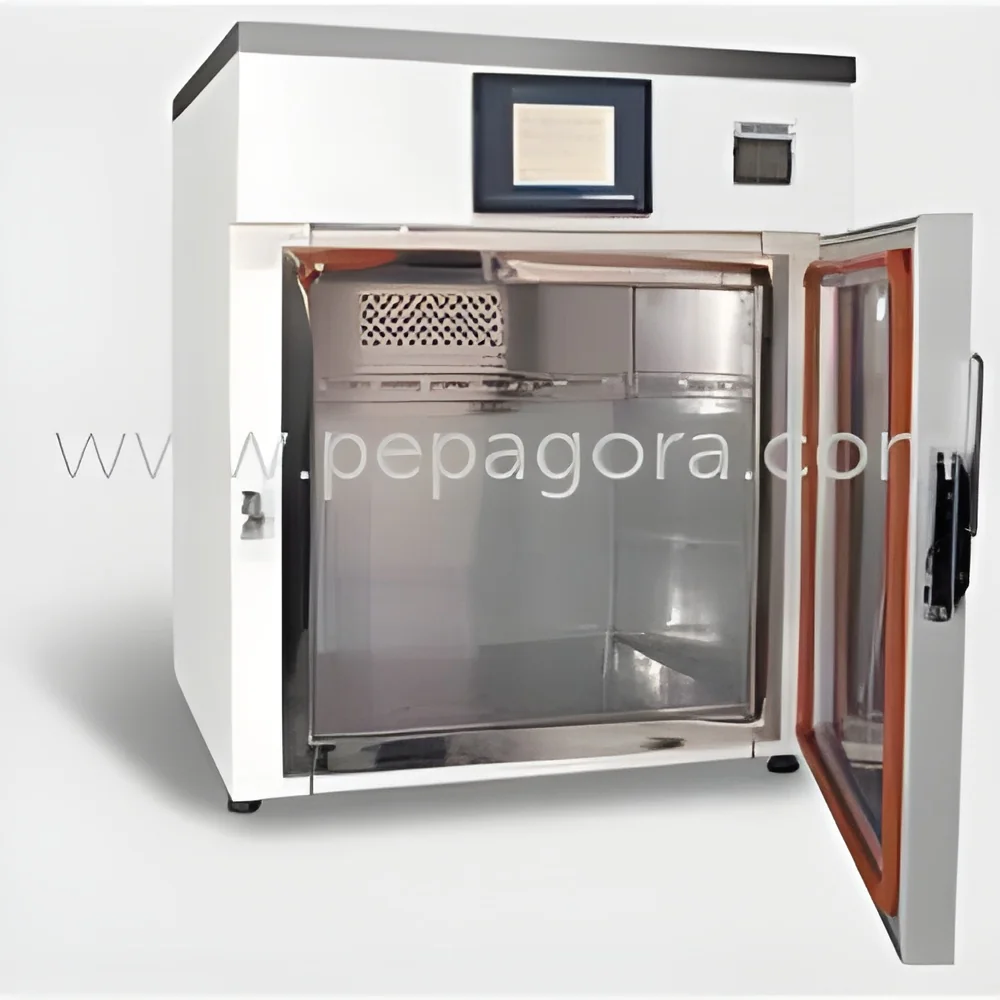
Industrial ETO (Ethylene Oxide) Gas Sterilizers represent a cornerstone technology for achieving terminal sterility for products that are sensitive to heat and moisture. These robust systems utilize a controlled concentration of ETO gas within a sealed chamber, effectively penetrating complex geometries and porous materials to eradicate all viable microorganisms. Engineered with precision controls for gas concentration, temperature, humidity, and exposure time, they deliver a repeatable and validated sterilization process. This reliability is critical for manufacturers who must guarantee that every batch meets stringent international standards for sterility assurance, making these sterilizers a trusted and essential piece of industrial equipment for serious production environments.

These sterilizers are the equipment of choice across several high-stakes industries. Medical device manufacturers rely on them to process everything from intricate surgical implants and wound dressings to c...
Industrial ETO (Ethylene Oxide) Gas Sterilizers represent a cornerstone technology for achieving terminal sterility for products that are sensitive to heat and moisture. These robust systems utilize a controlled concentration of ETO gas within a sealed chamber, effectively penetrating complex geometries and porous materials to eradicate all viable microorganisms. Engineered with precision controls for gas concentration, temperature, humidity, and exposure time, they deliver a repeatable and validated sterilization process. This reliability is critical for manufacturers who must guarantee that every batch meets stringent international standards for sterility assurance, making these sterilizers a trusted and essential piece of industrial equipment for serious production environments.

These sterilizers are the equipment of choice across several high-stakes industries. Medical device manufacturers rely on them to process everything from intricate surgical implants and wound dressings to complete procedural kits. Pharmaceutical companies utilize them for sterilizing bulk drugs, ointments, and powder-filled containers. Furthermore, they are fundamental in biotechnology for sterilizing fermentation equipment, in research institutions for labware, and in large healthcare facilities for reprocessing certain durable medical equipment. Their use ensures that products are safe for human use, comply with regulatory submissions, and maintain their functional integrity throughout their shelf life.

Investing in a high-quality ETO gas sterilizer translates directly into business value through operational reliability and risk mitigation. A well-designed system minimizes cycle times and utility consumption, optimizing throughput and reducing long-term operating costs. Built with durable, corrosion-resistant materials like stainless steel and featuring advanced monitoring with data logging, these units ensure consistent performance and simplify compliance with audits from bodies like the FDA, ISO, and other national regulators. This operational dependability protects your brand reputation, prevents costly recalls or batch rejections, and provides peace of mind, allowing you to focus on core business activities without sterilization-related disruptions.

Key Features:
- Advanced ethylene oxide gas delivery and aeration system for complete microbial eradication.
- Precision automated controls for cycle parameters including gas concentration, temperature, and humidity.
- Robust chamber construction using high-grade, corrosion-resistant stainless steel for durability.
- Designed and validated to comply with major international standards (e.g., ISO 11135, FDA 21 CFR).
- Integrated data recording and documentation features for process traceability and quality assurance.

Benefits:
- Enables safe sterilization of heat- and moisture-sensitive materials without damage.
- Provides deep penetration for sterilizing complex device assemblies and packaged products.
- Delivers a validated, repeatable process that meets strict regulatory requirements for sterility.
- Reduces operational risk and protects product quality, preventing contamination-related losses.
- Offers a reliable, industrial-grade solution that ensures consistent uptime and production flow.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
ETO gas sterilizers are engineered for the critical sterilization of heat-sensitive medical devices, pharmaceuticals, and laboratory equipment. Their precise ethylene oxide gas technology effectively eliminates all microbial life, including bacteria, viruses, and spores, while preserving the delicate structure and functionality of materials that cannot withstand high-temperature steam. This makes them indispensable in environments where absolute sterility is a mandatory requirement for safety and regulatory approval, ensuring products are free from contamination before reaching end-users.
These systems are vital beyond core medical manufacturing, serving advanced industries that demand the highest hygiene standards. They are used for sterilizing pharmaceutical packaging, biotechnology research tools, and complex surgical kits. Their application extends to facilities processing single-use devices, dental instruments, and veterinary medical supplies, providing a versatile and reliable solution for any operation that cannot compromise on the sterility of its products or components.
- Sterilizing single-use and reusable heat-sensitive medical devices like catheters, stents, and surgical implants.
- Ensuring the sterility of pharmaceutical products, active ingredients, and their primary packaging materials.
- Decontaminating sensitive laboratory equipment, bioreactors, and research instruments in biotech and life sciences.
- Processing surgical instrument sets and dental tools in hospital central sterile supply departments (CSSD).
- Supporting the production of sterile packaging and supplies for the veterinary medicine and animal health industries.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Kaustubh Enterprises, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial ETO Gas Sterilizers For Medical Devices And Pharmaceuticals
Industrial ETO Gas Sterilizers from reliable manufacturers provide safe, reliable sterilization for medical devices, pharmaceuticals, and lab equipment, ensuring compliance and material integrity for sensitive applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Kaustubh Enterprises
 Maharashtra, India
Industrial Equipment & MachineryManufacturer