IN
₹
Apparel & Fashion
Description
Choco Flavor Fly represents advanced chocolate flavoring technology developed specifically for industrial food production. This premium flavoring agent delivers authentic chocolate characteristics with remarkable consistency across manufacturing batches. Created through sophisticated food technology processes, it maintains the rich, complex profile of premium cocoa while offering superior stability and handling properties. Manufactured under rigorous quality control standards, every batch meets the highest industry specifications for purity and performance. The versatile formulation allows easy integration into both liquid and dry mix production systems, providing manufacturers with a reliable chocolate flavor solution that performs consistently in various applications and processing conditions.

Multiple food industry sectors benefit from incorporating Choco Flavor Fly into their manufacturing processes. The confectionery industry utilizes it for chocolate bars, candies, and coated pr...
Choco Flavor Fly represents advanced chocolate flavoring technology developed specifically for industrial food production. This premium flavoring agent delivers authentic chocolate characteristics with remarkable consistency across manufacturing batches. Created through sophisticated food technology processes, it maintains the rich, complex profile of premium cocoa while offering superior stability and handling properties. Manufactured under rigorous quality control standards, every batch meets the highest industry specifications for purity and performance. The versatile formulation allows easy integration into both liquid and dry mix production systems, providing manufacturers with a reliable chocolate flavor solution that performs consistently in various applications and processing conditions.

Multiple food industry sectors benefit from incorporating Choco Flavor Fly into their manufacturing processes. The confectionery industry utilizes it for chocolate bars, candies, and coated products where maintaining consistent flavor is crucial. Bakeries depend on its stable performance in baked goods requiring heat processing. Beverage manufacturers appreciate its excellent solubility and clarity in liquid applications. Dairy producers incorporate it into chocolate milk, yogurts, and ice creams for reliable flavor delivery. The prepared foods industry uses it in desserts, sauces, and ready-to-eat products where shelf-stable chocolate flavor is essential. This broad industry applicability demonstrates the product's versatility and reliability across different food manufacturing segments.

Businesses selecting Choco Flavor Fly gain significant competitive advantages through improved product consistency and reduced production variables. The reliability of this flavoring agent translates to fewer batch rejections and consistent end-product quality that strengthens brand reputation. Its consistent performance ensures manufacturers can maintain their product quality standards while optimizing production efficiency. The product's stability reduces waste and ensures longer shelf life for finished goods. Companies benefit from working with a supplier that understands industrial-scale production requirements and provides dependable supply chain reliability. This partnership approach ensures manufacturers receive appropriate technical support and formulation guidance tailored to their specific production needs and challenges.

Key Features:
- Consistent flavor profile maintained across all production batches
- High stability under various temperature processing conditions
- Excellent solubility in both water-based and fat-based systems
- Long shelf life with maintained flavor integrity
- Versatile application across multiple food manufacturing processes

Benefits:
- Reduced production variables and batch rejections
- Consistent end-product quality strengthening brand reputation
- Extended shelf life for finished products reducing waste
- Simplified production planning and inventory management
- Reliable supply chain with technical support availability
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Choco Flavor Fly integrates seamlessly into various food manufacturing processes, providing uniform flavor distribution and thermal stability. Its consistent performance ensures reliable results across different production environments, from cold mixing to high-temperature baking applications. This versatility makes it suitable for diverse manufacturing requirements while maintaining flavor integrity throughout processing stages.
Manufacturers value this flavoring agent for its excellent compatibility with other ingredients and consistent batch-to-batch quality. The product maintains its chocolate profile without interfering with texture or consistency, making it ideal for large-scale production where uniformity is essential. Its reliable performance helps maintain brand quality standards while simplifying production planning and inventory management for food producers.
- Chocolate bar and confectionery production for enhanced cocoa flavor consistency
- Bakery goods manufacturing including cakes, cookies, and pastry items
- Beverage production for chocolate drinks, milkshakes, and nutritional beverages
- Dairy product formulations including chocolate milk, yogurts, and ice cream
- Ready-to-eat dessert manufacturing for puddings, mousses, and chocolate treats
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Anil Food Industries, New Delhi
 New Delhi, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
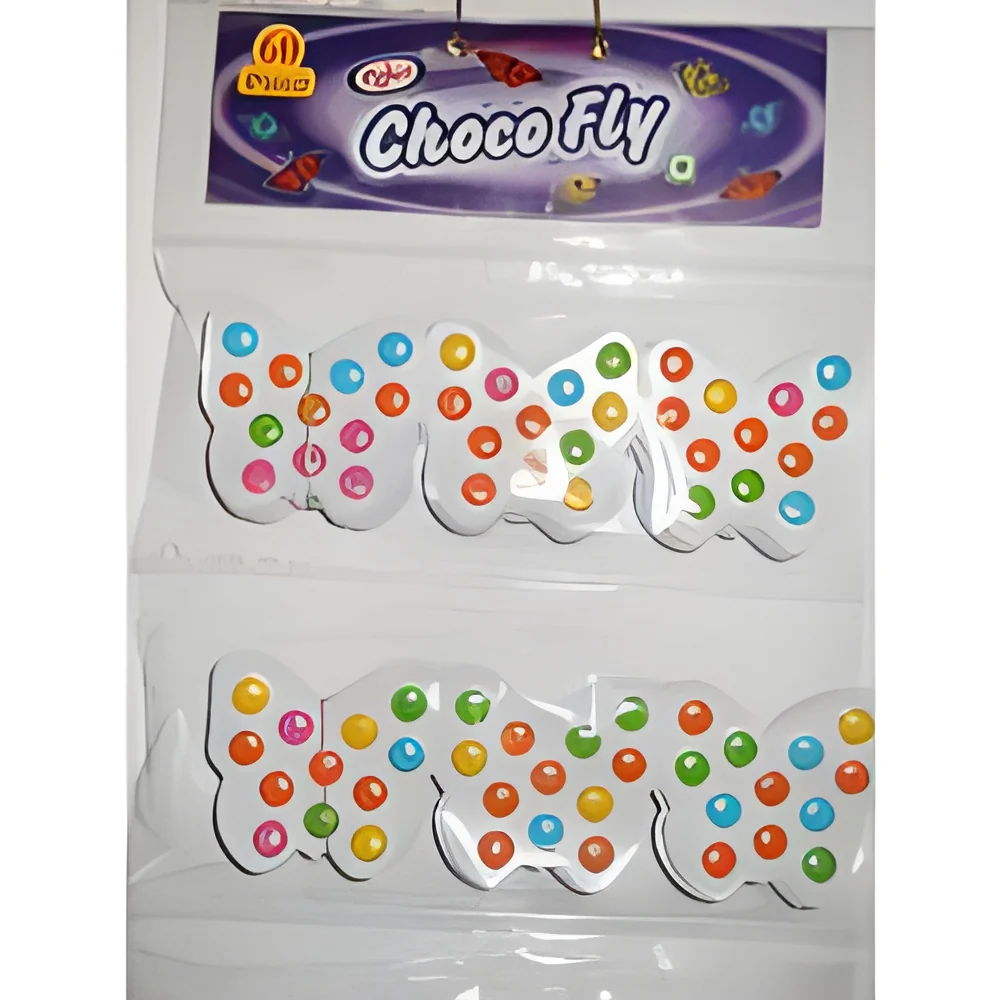
Food Manufacturing Choco Flavor Fly Premium Chocolate Flavoring Agent
Choco Flavor Fly premium chocolate flavoring agent delivers consistent quality and reliable supply for confectionery, bakery, and beverage manufacturing with authentic chocolate taste and excellent stability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anil Food Industries
 New Delhi, India
Raw Materials & ChemicalsManufacturer