IN
₹
Apparel & Fashion
Description
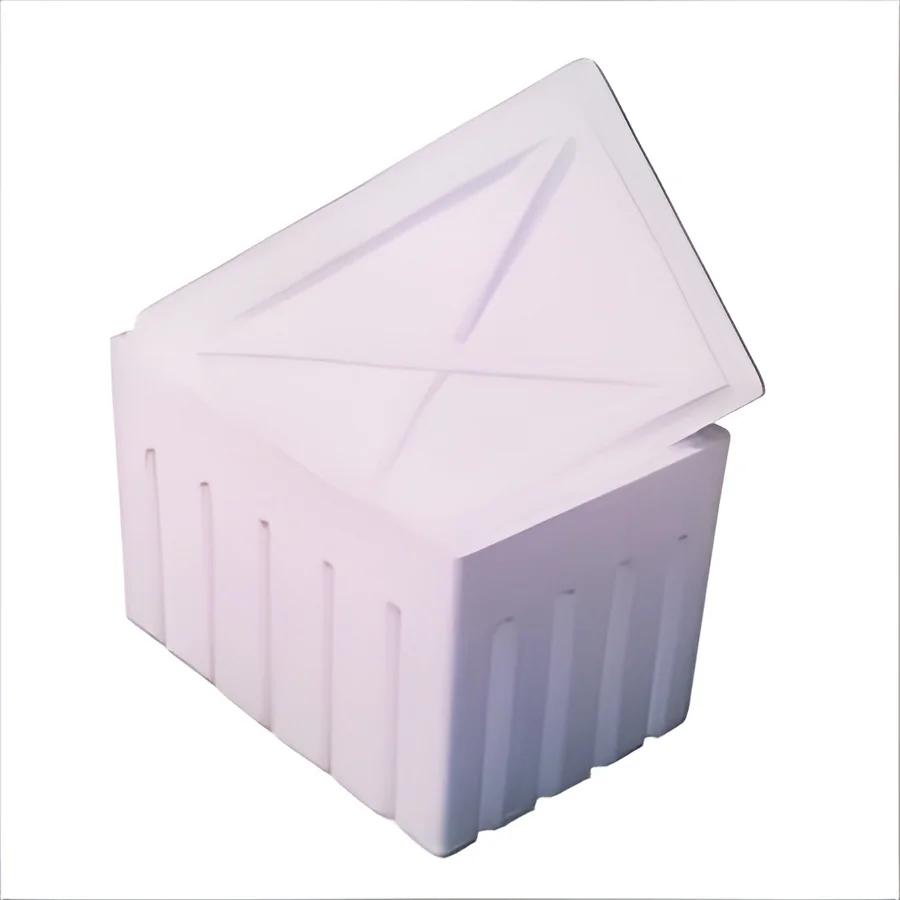
The Industrial Military Commercial Armour Box represents a specialized protective solution engineered for safeguarding sensitive electronic equipment against the most demanding environmental challenges. Constructed from premium impact-resistant materials, this protective enclosure is designed to withstand rigorous handling, accidental drops, and continuous exposure to harsh conditions. It provides comprehensive protection against physical shocks, dust infiltration, water ingress, and temperature extremes that could compromise electronic functionality. Whether utilized for transportation between sites, secure storage, or deployment in field operations, this armour box ensures your valuable equipment remains protected, functional, and immediately available for critical tasks. The design incorporates advanced sealing technologies and structural integrity that meet the exacting standards required by professionals across multiple sectors.

This protective solution finds extensive applicatio...
The Industrial Military Commercial Armour Box represents a specialized protective solution engineered for safeguarding sensitive electronic equipment against the most demanding environmental challenges. Constructed from premium impact-resistant materials, this protective enclosure is designed to withstand rigorous handling, accidental drops, and continuous exposure to harsh conditions. It provides comprehensive protection against physical shocks, dust infiltration, water ingress, and temperature extremes that could compromise electronic functionality. Whether utilized for transportation between sites, secure storage, or deployment in field operations, this armour box ensures your valuable equipment remains protected, functional, and immediately available for critical tasks. The design incorporates advanced sealing technologies and structural integrity that meet the exacting standards required by professionals across multiple sectors.

This protective solution finds extensive application across industries where equipment reliability directly impacts operational success and safety. In military and defense contexts, it protects sophisticated communication gear, surveillance systems, and electronic countermeasure devices during tactical operations. Industrial sectors employ these boxes to shield automation controllers, data acquisition systems, and precision instruments in manufacturing environments with high vibration and particulate contamination. Telecommunications providers rely on them for outdoor network equipment protection, while energy companies use them for field monitoring devices in remote locations. Medical professionals transport sensitive diagnostic equipment securely, and broadcast teams protect expensive production gear during location shoots. This wide-ranging utility demonstrates the product's fundamental role in maintaining operational continuity across professional fields.

Investing in this Armour Box delivers substantial business value through reduced equipment downtime, lower maintenance costs, and extended asset lifespan. By providing reliable protection against environmental damage, these cases prevent costly repairs and replacements while ensuring consistent equipment performance. The robust construction using high-grade materials offers long-term durability that translates to excellent return on investment through years of dependable service. The product's design prioritizes both protection and practicality, with features that enhance usability without compromising security. For importers, distributors, and wholesalers, this represents a trusted product with proven reliability that meets the exacting requirements of professional users across multiple sectors, creating satisfied customers and repeat business opportunities.

Key Features:
- Constructed from high-grade impact-resistant polypropylene composite materials for exceptional durability.
- Advanced multi-point sealing system providing IP67-rated protection against dust and water ingress.
- Reinforced corner protection and shock-absorbing internal padding to withstand substantial impacts.
- Integrated pressure equalization valve to prevent vacuum lock and moisture buildup during altitude changes.
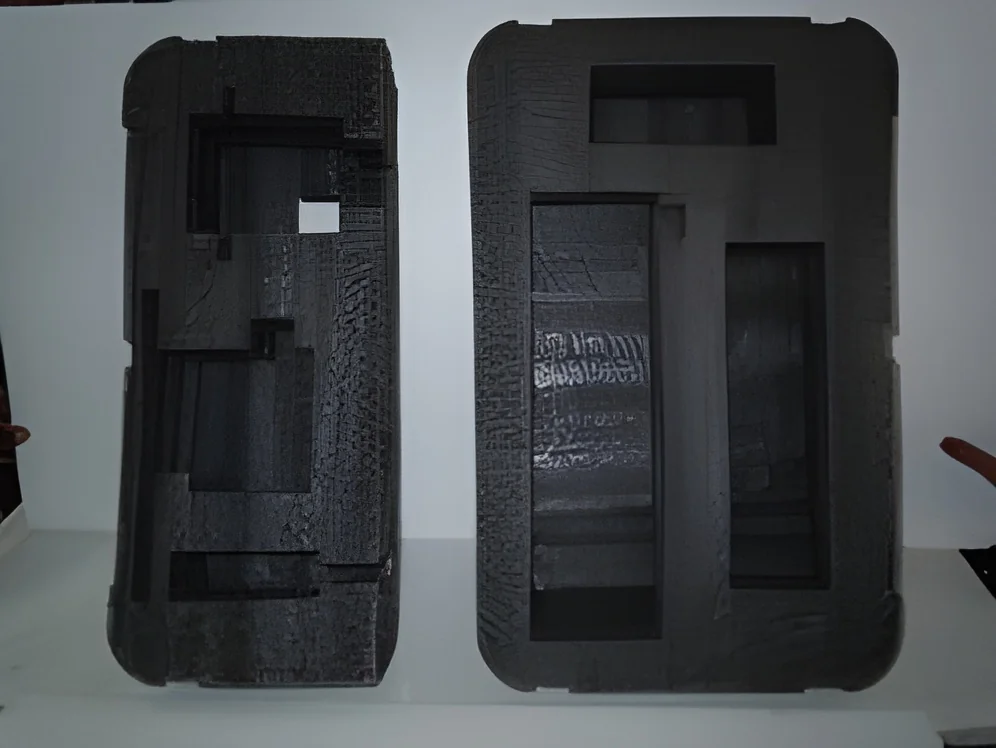
- Modular interior with customizable foam inserts that securely cradle equipment of various shapes and sizes.

Benefits:
- Significantly reduces equipment failure rates and maintenance costs by providing reliable environmental protection.
- Extends the operational lifespan of valuable electronic assets through consistent damage prevention.
- Ensures equipment readiness and availability for critical operations by preventing transport-related damage.
- Enhances operational efficiency by eliminating downtime caused by equipment malfunctions from environmental factors.
- Provides peace of mind through proven reliability in demanding conditions across multiple professional sectors.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The Industrial Military Commercial Armour Box delivers essential protection for valuable electronic equipment operating in challenging conditions. Its robust construction shields devices from physical shocks, dust intrusion, moisture, and extreme temperature variations during transportation, field deployment, or long-term storage. This ensures your critical electronics remain fully operational and undamaged, maintaining performance reliability when it matters most.
Engineered for versatility, these protective cases serve numerous professional sectors where equipment security is paramount. From military field operations to industrial automation and telecommunications infrastructure, the armour box adapts to diverse requirements. Its reliable design provides peace of mind for professionals managing sensitive devices, offering consistent protection that reduces operational risks and equipment failures across various demanding applications.
- Military and defense operations: Protecting tactical communication systems, surveillance drones, and electronic warfare equipment during field deployments and transport.
- Industrial automation and manufacturing: Shielding programmable logic controllers, precision sensors, and measurement instruments in harsh factory environments with vibration and particulate contamination.
- Telecommunications infrastructure: Securing network switches, fiber optic terminals, and remote transmission equipment for outdoor installations exposed to weather elements.
- Medical and healthcare equipment: Safeguarding portable diagnostic devices, patient monitors, and laboratory instruments during inter-facility transport and mobile medical services.
- Energy and utility sector: Housing monitoring equipment, testing devices, and communication gear for power grid maintenance, oil field operations, and renewable energy installations.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Aakar Thermocole Packaging, Gujarat
 Gujarat, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Military Commercial Armour Box For Electronics Protection
Industrial Military Commercial Armour Box provides heavy-duty protection for sensitive electronics against impact, dust, and harsh environments. Ideal for secure transport and storage across demanding sectors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Aakar Thermocole Packaging
 Gujarat, India
Raw Materials & ChemicalsManufacturer