IN
₹
Description
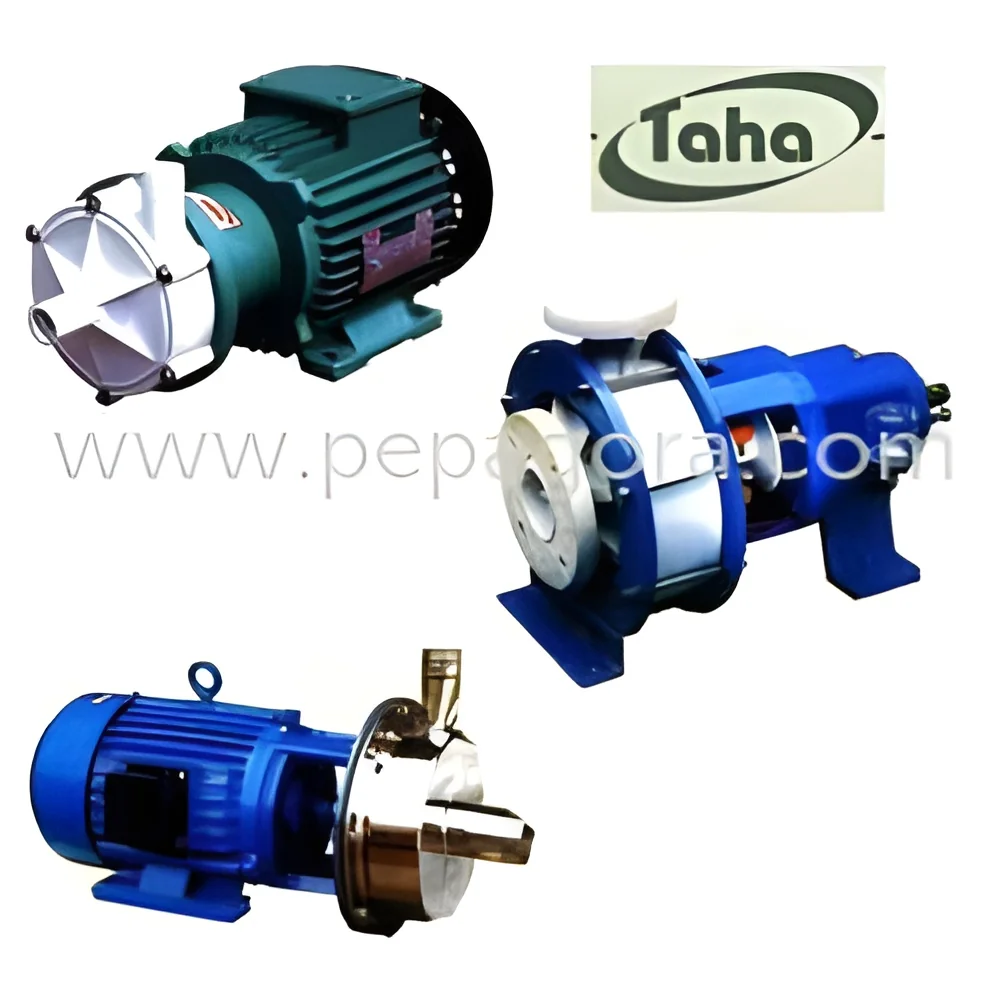
The Industrial Chemical Transfer Pump represents professional-grade equipment designed for reliable chemical handling across various industrial settings. With flow rates ranging from 15 to 300 liters per minute, this pump ensures safe transfer of diverse chemicals, aggressive fluids, and solvents while maintaining operational integrity. The robust construction and precision engineering provide consistent performance in demanding environments where chemical compatibility and transfer accuracy are critical. Designed for continuous operation, this pump minimizes downtime and maintenance requirements, offering a dependable solution for facilities that prioritize equipment reliability and process efficiency in their fluid handling operations.

This chemical transfer pump serves essential functions across multiple industrial sectors including chemical manufacturing, water treatment facilities, agricultural operations, and industrial processing plants. In chemical production environments, it ...
The Industrial Chemical Transfer Pump represents professional-grade equipment designed for reliable chemical handling across various industrial settings. With flow rates ranging from 15 to 300 liters per minute, this pump ensures safe transfer of diverse chemicals, aggressive fluids, and solvents while maintaining operational integrity. The robust construction and precision engineering provide consistent performance in demanding environments where chemical compatibility and transfer accuracy are critical. Designed for continuous operation, this pump minimizes downtime and maintenance requirements, offering a dependable solution for facilities that prioritize equipment reliability and process efficiency in their fluid handling operations.

This chemical transfer pump serves essential functions across multiple industrial sectors including chemical manufacturing, water treatment facilities, agricultural operations, and industrial processing plants. In chemical production environments, it safely handles corrosive substances and intermediate products during manufacturing processes. Water treatment facilities rely on it for accurate dosing of treatment chemicals and additives. Agricultural operations utilize the pump for transferring fertilizers, pesticides, and other agricultural chemicals. Manufacturing and processing plants depend on its capabilities for various process fluids, while other sectors like pharmaceuticals and automotive maintenance benefit from its precise fluid handling capabilities for quality control and operational efficiency.

The business value of this chemical transfer pump lies in its operational reliability, reduced maintenance requirements, and efficiency that directly impact operational costs and productivity. Built to withstand aggressive chemicals and continuous operation, this pump minimizes downtime and replacement expenses compared to standard equipment. Its consistent performance ensures accurate fluid transfer, reducing material waste and improving process control. The durable construction means fewer breakdowns and lower lifetime ownership costs, while the safe transfer technology maintains workplace safety standards. For operations seeking to optimize their chemical handling processes, this pump offers a reliable solution that enhances productivity while ensuring compliance with industry regulations and safety protocols.

Key Features:
- Flow capacity range from 15 to 300 liters per minute for versatile applications
- Robust construction designed to handle aggressive chemicals and corrosive substances
- Reliable operation with consistent performance in continuous use environments
- Safe transfer technology that prevents contamination and leakage risks
- Durable components that withstand demanding industrial conditions and extend service life

Benefits:
- Versatile flow capacity accommodates various operational scales and requirements
- Chemical-resistant construction ensures long-term reliability with aggressive substances
- Consistent performance reduces operational downtime and maintenance costs
- Safe operation minimizes contamination risks and enhances workplace safety
- Durable design extends equipment lifespan and reduces replacement frequency
Specifications
| Key Attributes | |
|---|---|
| Capacity | 15 LPM- 300 LPM |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial chemical transfer pump delivers reliable performance in demanding environments where safe fluid handling is essential. Engineered to manage flow rates from 15 to 300 LPM, it efficiently transfers various chemicals, solvents, and aggressive liquids without contamination risks. The robust design ensures consistent operation, making it suitable for continuous industrial processes that require precision and dependability in chemical management.
Versatile enough for multiple sectors, this pump handles everything from corrosive substances in chemical plants to fertilizers in agricultural settings. Its durable construction withstands harsh operating conditions, providing long-lasting service across different applications. The pump's adaptability makes it ideal for facilities needing reliable transfer solutions for diverse liquids, ensuring operational continuity and safety compliance in various industrial scenarios.
- Transferring acids, alkalis, and chemical solvents in manufacturing facilities
- Moving agricultural chemicals like fertilizers and pesticides in farming operations
- Handling water treatment chemicals in purification and wastewater plants
- Dispensing industrial lubricants, fuels, and process fluids in maintenance operations
- Processing chemical ingredients in pharmaceutical and production facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Shabis Enterprises, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Chemical Transfer Pump 15 300 LPM Flow Rate
Industrial Chemical Transfer Pump with 15-300 LPM flow rate for safe chemical handling in manufacturing, agriculture, and water treatment sectors. Durable construction ensures reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Shabis Enterprises
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer